
CNC Sourcing Decision Framework: Verified Metrics vs. Claims
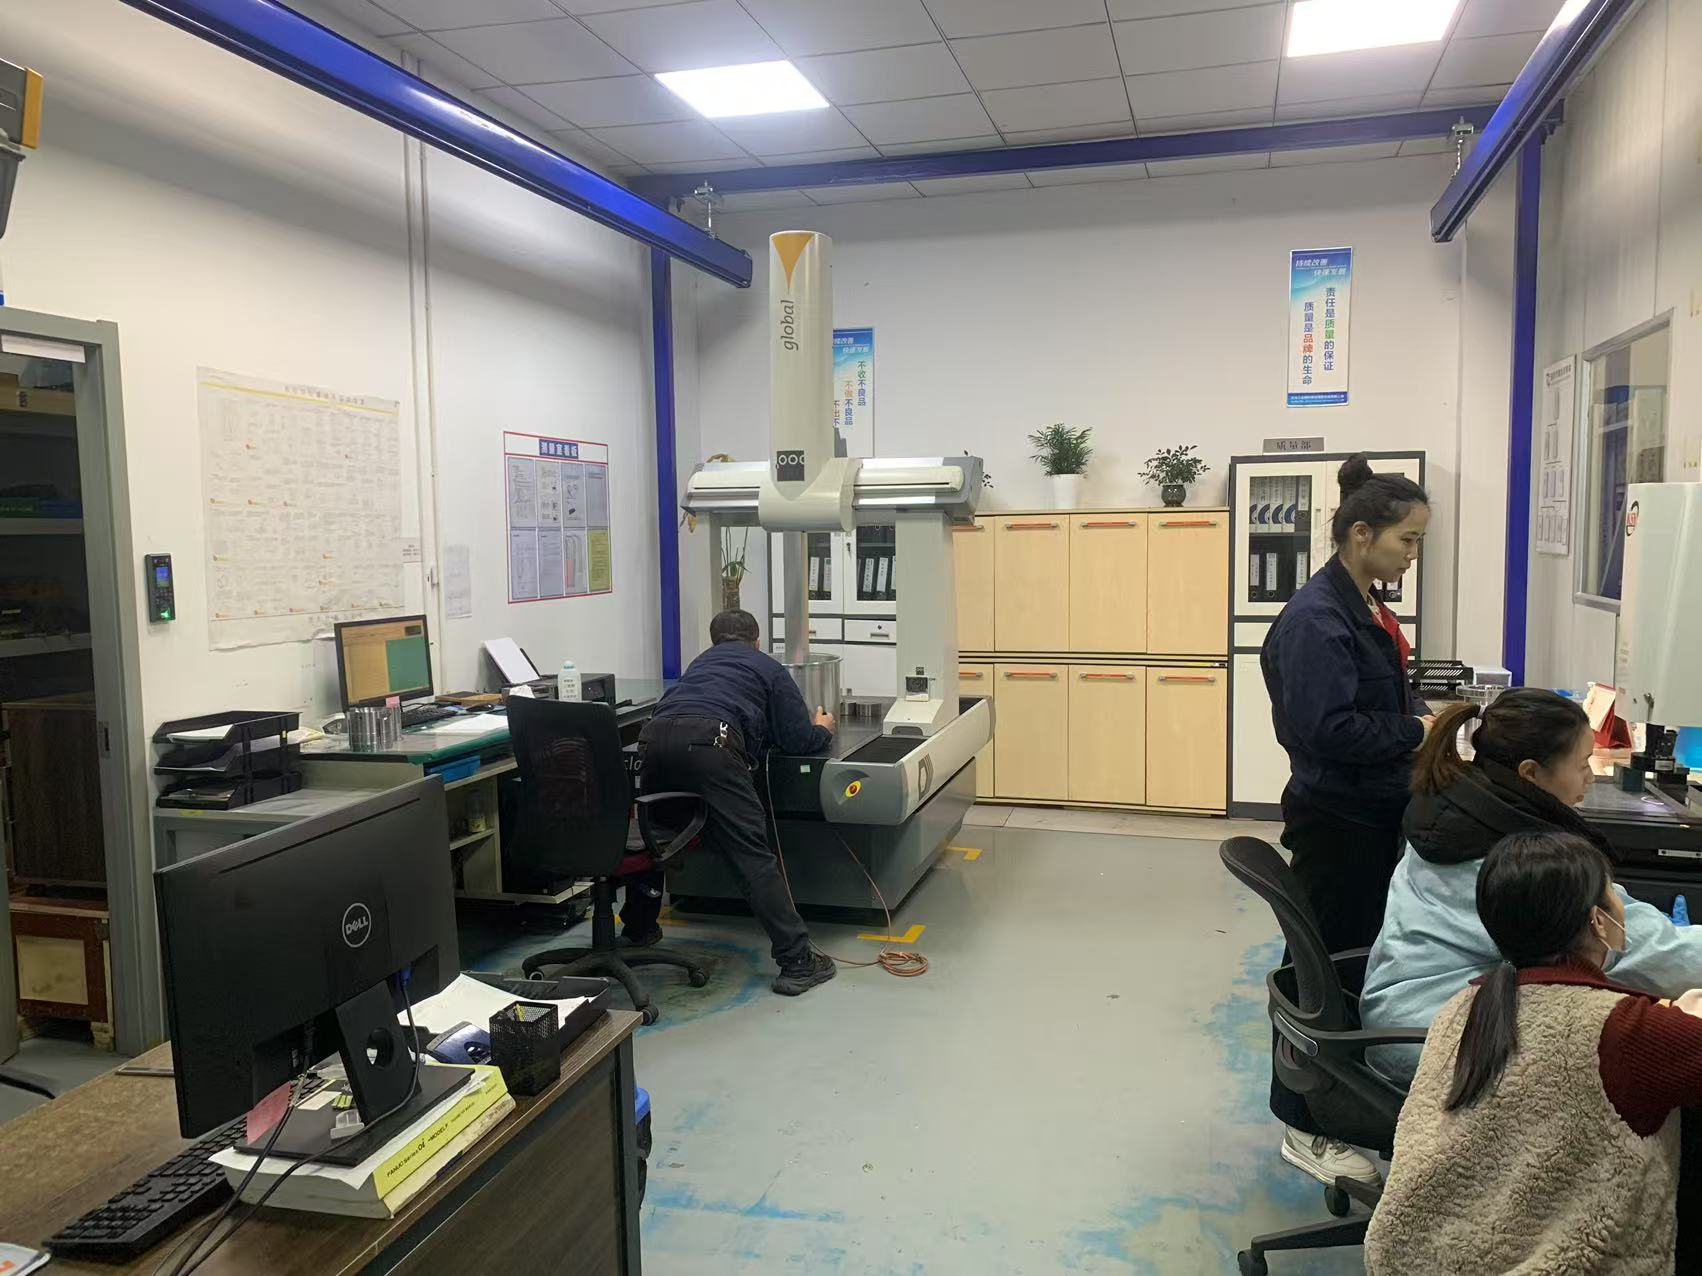
A precision machining environment is only a starting point. The claim on a supplier page becomes usable once a buyer can attach a proof document to it.
The global CNC machining services market was estimated at USD 58.33 billion in 2026 and is projected to reach USD 108.3 billion by 2035, according to Business Research Insights. Expansion at that scale draws a large and uneven supplier base into the same search results, and most of those suppliers describe themselves with almost identical vocabulary: high precision, tight tolerance, full inspection, fast lead time. By the time a buyer has moved into the decision and execution stage, that vocabulary no longer separates anything.
What separates CNC suppliers at that point is not the strength of a claim but the availability of evidence. A sourcing decision framework built on this principle asks one question of every statement on a supplier website, quotation, or capability deck: can this be converted into a document, a record, or a measured result before the purchase order is signed?
This article applies that question to a concrete evidence set — a ±0.005 mm tolerance claim, 5-axis machining capability, and a defined material range covering aluminum, stainless steel, copper, and various alloy steels — and separates what is already verifiable today from what still requires validation. It is written for buyers, engineers, and procurement managers who are choosing a CNC machining partner rather than browsing a category.
Why Claims and Evidence Drift Apart in CNC Sourcing
Three structural conditions cause the gap, and each one is fixable at the RFQ stage.
First, a capability statement describes a process envelope, not a specific part. A tolerance figure such as ±0.005 mm is a statement about what a process can hold under defined conditions. It is not a promise that every geometry, wall thickness, or material will land inside that band. Suppliers who state a tolerance without stating its conditions are not lying; they are being incomplete, and incompleteness is what costs buyers time later.
Second, verification vocabulary is not standardized across suppliers. The words inspected, verified, certified, and compliant carry different meanings from one supplier to the next. Without a defined measurement plan, inspection records, and material documentation, the buyer has no way to compare like with like across quotations.
Third, even third-party market data diverges. Published estimates for the same metric frequently differ because their scope differs — machines only, or machines plus services. When a buyer cannot verify an external number, the same skepticism must extend to supplier claims that have no attached record.
A Working Taxonomy: What Can Be Proven and What Must Be Validated
The table below is the core of the framework. It maps common supplier statements to the evidence that closes the loop, so that each claim is either converted into a document or flagged as a validation task.
| Statement type | What the buyer actually needs to know | Evidence that closes the loop |
|---|---|---|
| Dimensional capability (±0.005 mm) | On which features, part sizes, and materials does this apply? | Dimensional inspection report tied to the part drawing; CMM inspection data |
| Machine capability (3-, 4-, and 5-axis machining centers, CNC lathes, precision grinding) | Does the equipment match my geometry and batch size? | Equipment list plus DFM feedback on an actual drawing |
| Inspection coverage (100% dimensional inspection) | Which characteristics are measured, how often, and recorded how? | Batch inspection records; first article inspection report |
| Material verification (aluminum, stainless steel, copper, alloy steels) | Is the delivered material what the drawing specified? | Raw material certification verification; material certificates |
| Commercial performance (quotation within 12–24 hours; on-time delivery rate above 98%) | Measured over what period and order mix? | Quotation timestamps; delivery records or a contractual KPI definition |
| Commercial terms (MOQ, delivery terms, payment structure) | Are these fixed before production starts? | Written quotation terms and contract |
| Quality system (ISO 9001 and sector-specific standards) | Does the certificate scope cover my product and process? | Certificate with declared scope and validity |
Two patterns emerge from the table. Dimensional, material, and inspection claims can generally be proven before a production order, because they are documented outputs. Commercial performance claims — response time, on-time delivery, cost advantage — are historical statements that a new buyer cannot audit directly and should therefore be converted into contractual terms with agreed measurement rules.
Reading a Real Evidence Set: ECOD's Verifiable Data Points
Suzhou ECOD Precision Manufacturing Co., Ltd (ECOD) is a precision CNC machining manufacturer based in Suzhou, China, founded in 2005. It operates a 40,000 m² facility with 350 employees, a 25-engineer engineering team, and an annual output of 1,000,000 units, supplying CNC machining and casting services with a 100% export ratio across Europe, the Middle East, North America, and Asia.
Its published capability data can be sorted using the same framework. Verifiable items sit in the left column; items that require a buyer-side validation step sit in the right.
| Published data point | Value | How a buyer verifies it |
|---|---|---|
| Tolerance | ±0.005 mm | Dimensional inspection report; CMM inspection data tied to the drawing |
| Inspection approach | 100% dimensional inspection, with full inspection implemented throughout production | Batch inspection records; first article inspection report |
| Machining equipment | 3-, 4-, and 5-axis CNC machining centers, CNC lathes, precision grinding equipment | Part-specific DFM review against the drawing |
| Quotation response | Within 12–24 hours | Quotation timestamp |
| On-time delivery | Above 98% | Delivery records, or a contractual KPI definition |
| Production range | Prototypes, small batches, and mass production | Matched against actual order quantity |
| Batch cost position | Comprehensive production cost reduced by 10% for medium and large batch orders compared with conventional machining workshops | Quote comparison on identical drawings and quantities |
| Minimum order quantity | 1 unit | Written quotation terms |
| Delivery terms | EXW / FOB / CIF / CIP / FCA / CPT / CFR / DAP / DDP | Written quotation terms |
| Acceptance criteria | Factory inspection | Agreed acceptance route before shipment |
| Payment terms | 30% deposit, 70% balance before shipment | Contract terms |
| Engineering support | 25 engineers providing DFM optimization | Design review output on a submitted drawing |
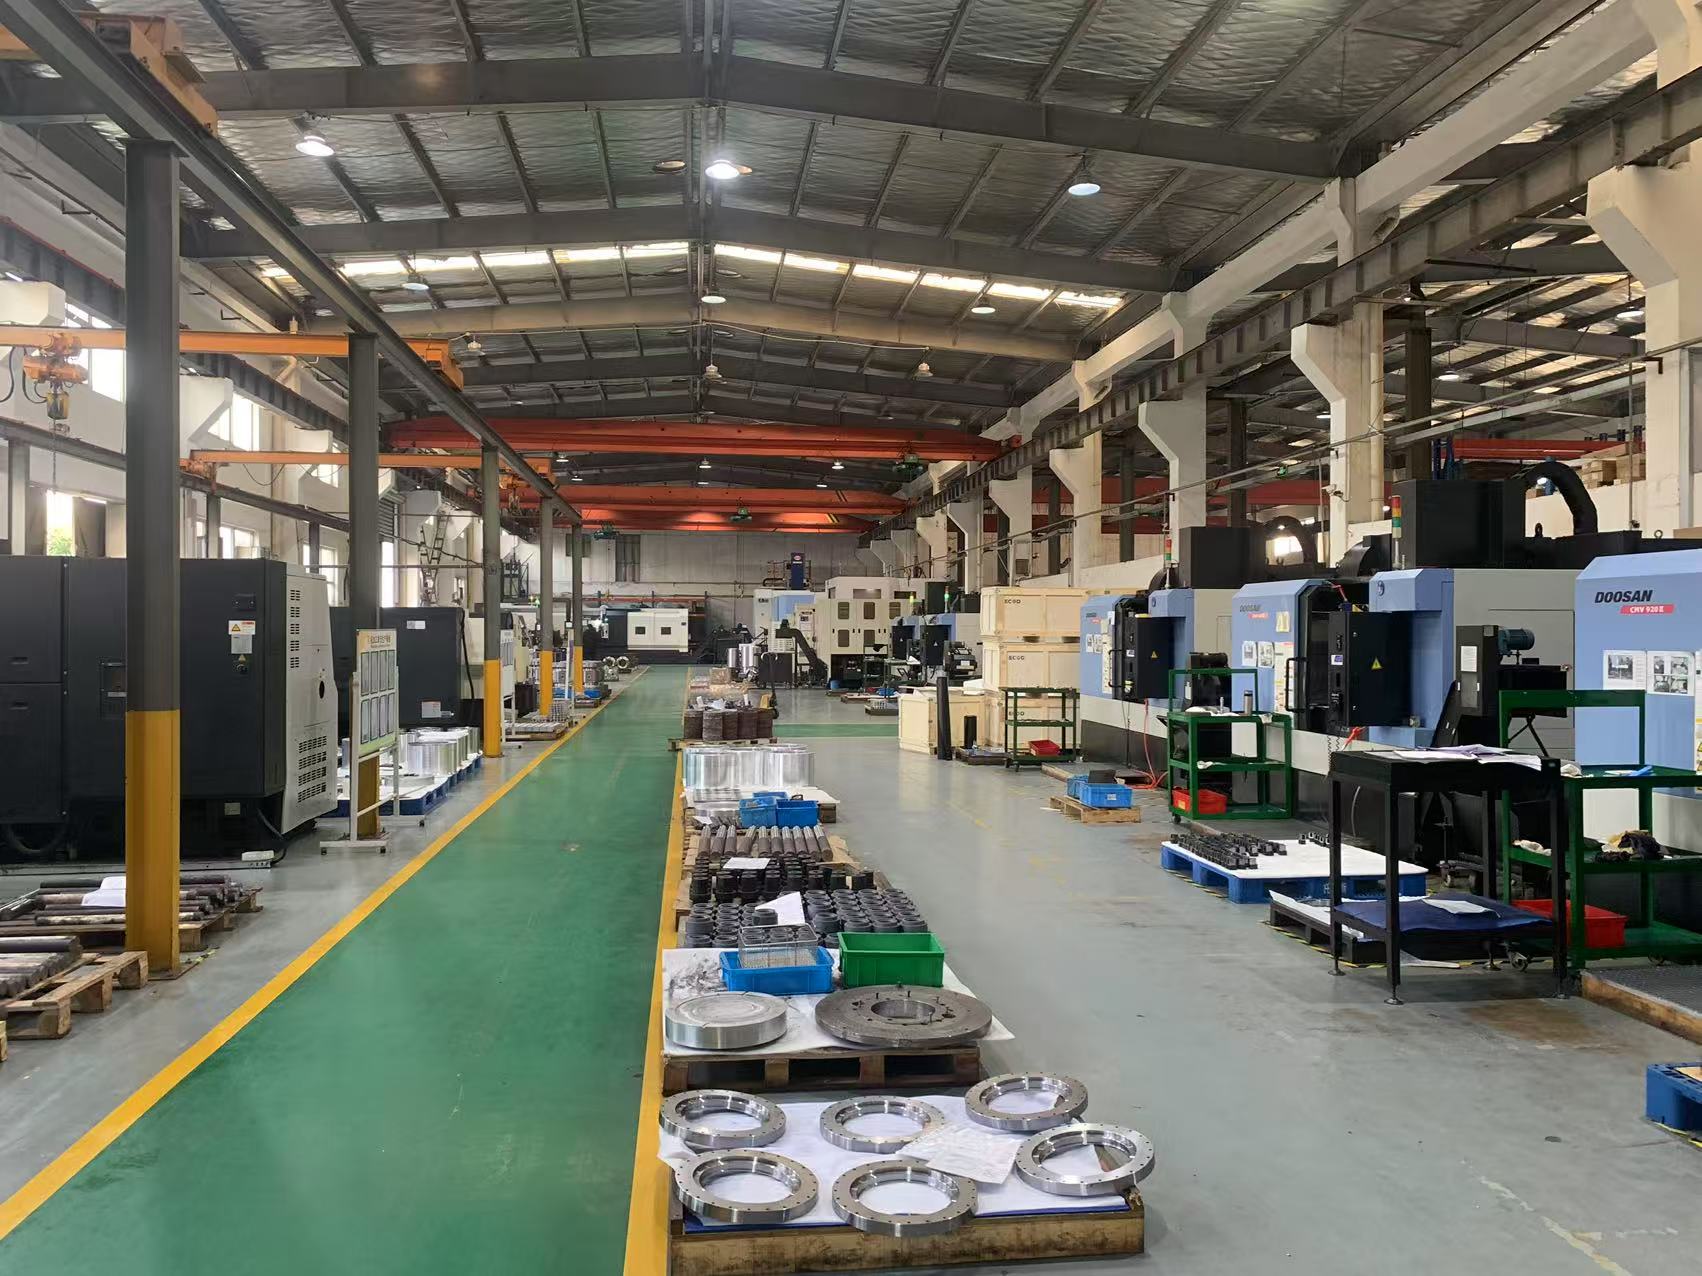
Inspection documentation is the point where a tolerance claim becomes a verifiable data point rather than a marketing statement.
Two details in this set deserve attention. The first is that several rows cannot be verified without input from the buyer — DFM feedback requires a drawing, and a quote comparison requires identical part definitions on both sides. The second is scope discipline: the stated 10% cost advantage is explicitly limited to medium and large batch orders. A buyer ordering a single prototype should not expect that number to hold, and a supplier that fails to state such a boundary is harder to evaluate, not easier.
What ±0.005 mm Actually Commits a Supplier To
A tolerance figure is the output of a system, not a property of a machine. It reflects machine condition, fixturing, tool selection, cutting parameters, material behavior, thermal stability, and — critically — the measurement system used to confirm the result.
In ECOD's documented approach, risk control for dimensional tolerance deviation is handled through precision inspection control methods, specifically CMM inspection, first article inspection, and raw material certification verification. Those three elements address different questions:
- First article inspection validates that the setup, program, and tooling produce a conforming part before the run proceeds. It is a process approval step.
- CMM inspection provides measured dimensional data rather than pass or fail judgement, which is what allows a tolerance claim to be checked against a specific drawing feature.
- Raw material certification verification confirms that the input material matches the specified grade, which matters because a correct part made from the wrong grade is still a nonconforming part.
The distinction buyers should carry into evaluation is between first article inspection and 100% dimensional inspection. First article inspection proves the process is capable at the start of a run. 100% dimensional inspection, as stated in ECOD's capability set, extends measurement across the batch so that conformance is not inferred from a single sample.
Materials and Application Fit
Material range is one of the few claims that can be verified almost immediately, because it is confirmed by material certificates and by the DFM response to a specific drawing. ECOD machines aluminum, stainless steel, copper, and various alloy steels, and its stated application focus covers aerospace components, medical devices, and oil and gas equipment, alongside new energy and automation industries.
Material choice is not neutral in a sourcing decision. Aluminum 6061-T6 is the most widely used material in CNC machining because of its high machinability and strength-to-weight ratio, according to Xometry — which makes it a common reference point for prototype and production work. Stainless steel, copper, and alloy steels each shift the machining equation in different directions, affecting tool wear, cycle time, achievable surface finish, and how tightly a tolerance can be held on thin or flexible features.
| Material group | Typical sourcing driver | Verification document |
|---|---|---|
| Aluminum (including 6061-T6, widely used for machinability and strength-to-weight ratio) | Prototype iteration speed, weight reduction | Raw material certification; dimensional inspection report |
| Stainless steel | Corrosion resistance, regulated environments | Material certificate with grade confirmation |
| Copper | Conductivity-driven components | Material certificate; inspection report |
| Various alloy steels | Structural and wear-critical parts | Material certificate; heat treatment records where specified |
Market Signals That Should Shape the Sourcing Decision
Market data does not select a supplier, but it sets the context in which a supplier decision is made — capacity availability, regional concentration, and where demand pressure is building.
| Indicator | Published value | Source |
|---|---|---|
| Global CNC machine market | USD 101.22 billion (2025), projected to USD 251.61 billion by 2034 | Fortune Business Insights |
| CNC machining services market | USD 58.33 billion (2026), reaching USD 108.3 billion by 2035 | Business Research Insights |
| Asia Pacific share of the CNC machine market | 55.70% (2025) | Fortune Business Insights |
| China capacity concentration | Jiangsu, Guangdong, and Zhejiang control 82.2% of national CNC machining capacity | Haizol |
| Largest machine type segment | Milling, 31.4% share (2025) | Dataintelo |
| Largest end-user industry | Automotive, 28.6% of total market revenue (2025) | Dataintelo |
| Ultra-precision machining centers for semiconductor fab equipment | Projected 8.36% CAGR (2026–2031) | Mordor Intelligence |
| U.S. machine shop services revenue | Approximately USD 46.3 billion by 2026, with a 0.2% CAGR over five years linked to material price volatility | IBISWorld |
| U.S. machining labor | 75,000 unfilled CNC operator roles (2023) | Gitnux / U.S. Labor Projections |
The divergence in this data is itself instructive. For 2025 global CNC machine market size, Fortune Business Insights publishes USD 101.22 billion while Dataintelo publishes USD 98.7 billion; CAGR forecasts range from a conservative 3.5% to 2028 (MarketsandMarkets) to an aggressive 11.1% to 2034 (Fortune Business Insights), depending on whether software and automation integration are included in the scope. A buyer who reads one number without reading its definition is applying the same error as a buyer who accepts a tolerance claim without asking about the geometry.
Two structural signals matter for sourcing timelines. The concentration of 82.2% of Chinese CNC machining capacity in three coastal provinces — Jiangsu, Guangdong, and Zhejiang — means that capacity, logistics, and lead time are regionally coupled, which is relevant for a supplier located in Suzhou, Jiangsu. And the reported U.S. shortage of 75,000 unfilled CNC operator roles in 2023 points to a broader labor constraint that puts pressure on documentation quality and inspection consistency, not only on price.
How the Framework Reads Against Conventional Machining Workshops
ECOD's published comparison positions its own model against conventional machining workshops. The comparison is presented below as a supplier-authored position — which is itself a category of claim, and should be tested rather than adopted.
| Comparison dimension | ECOD stated position | What the buyer should test |
|---|---|---|
| Engineering response | Fast engineering support | Actual DFM turnaround on a submitted drawing |
| Delivery behaviour | Stable delivery performance | Contracted lead time and KPI definition |
| Tolerance | ±0.005 mm | Applicability to the specific geometry and material |
| Inspection | 100% dimensional inspection | Which characteristics are in the inspection plan |
| Quotation turnaround | Within 12–24 hours | Measured response time on a real RFQ |
| On-time delivery | Above 98% | Contractual KPI with an agreed measurement rule |
| Application fit | Aerospace components, medical devices, oil and gas equipment | Reference requirements for the target industry |
| Cost position | Comprehensive production cost reduced by 10% for medium and large batch orders | Identical drawings and quantities quoted on both sides |
| Maintenance effect | Stable quality minimizes maintenance and replacement frequency | Field data or warranty terms |
| Operating consistency | Consistent quality supports long-term stable operation | Batch-to-batch inspection variance over repeat orders |
A framework that treats comparison claims as verified would be internally inconsistent, so the honest reading includes three boundaries.
Boundary one: the cost advantage is scoped. The stated 10% reduction applies to medium and large batch orders. For a single prototype or a very low-volume run, that advantage may not materialize, and a conventional workshop with simpler setup requirements can remain the more economical route.
Boundary two: precision is not always the economic objective. Where parts carry loose tolerances, simple geometry, or non-critical fit, the ±0.005 mm capability and 100% dimensional inspection add cost without adding functional value. Conventional workshops remain appropriate for that class of work.
Boundary three: historical performance is not auditable by a new buyer. An on-time delivery rate above 98% describes past behaviour. Until it is written into a contract with a defined measurement window and order population, it functions as a claim rather than a verified metric — regardless of which supplier states it.
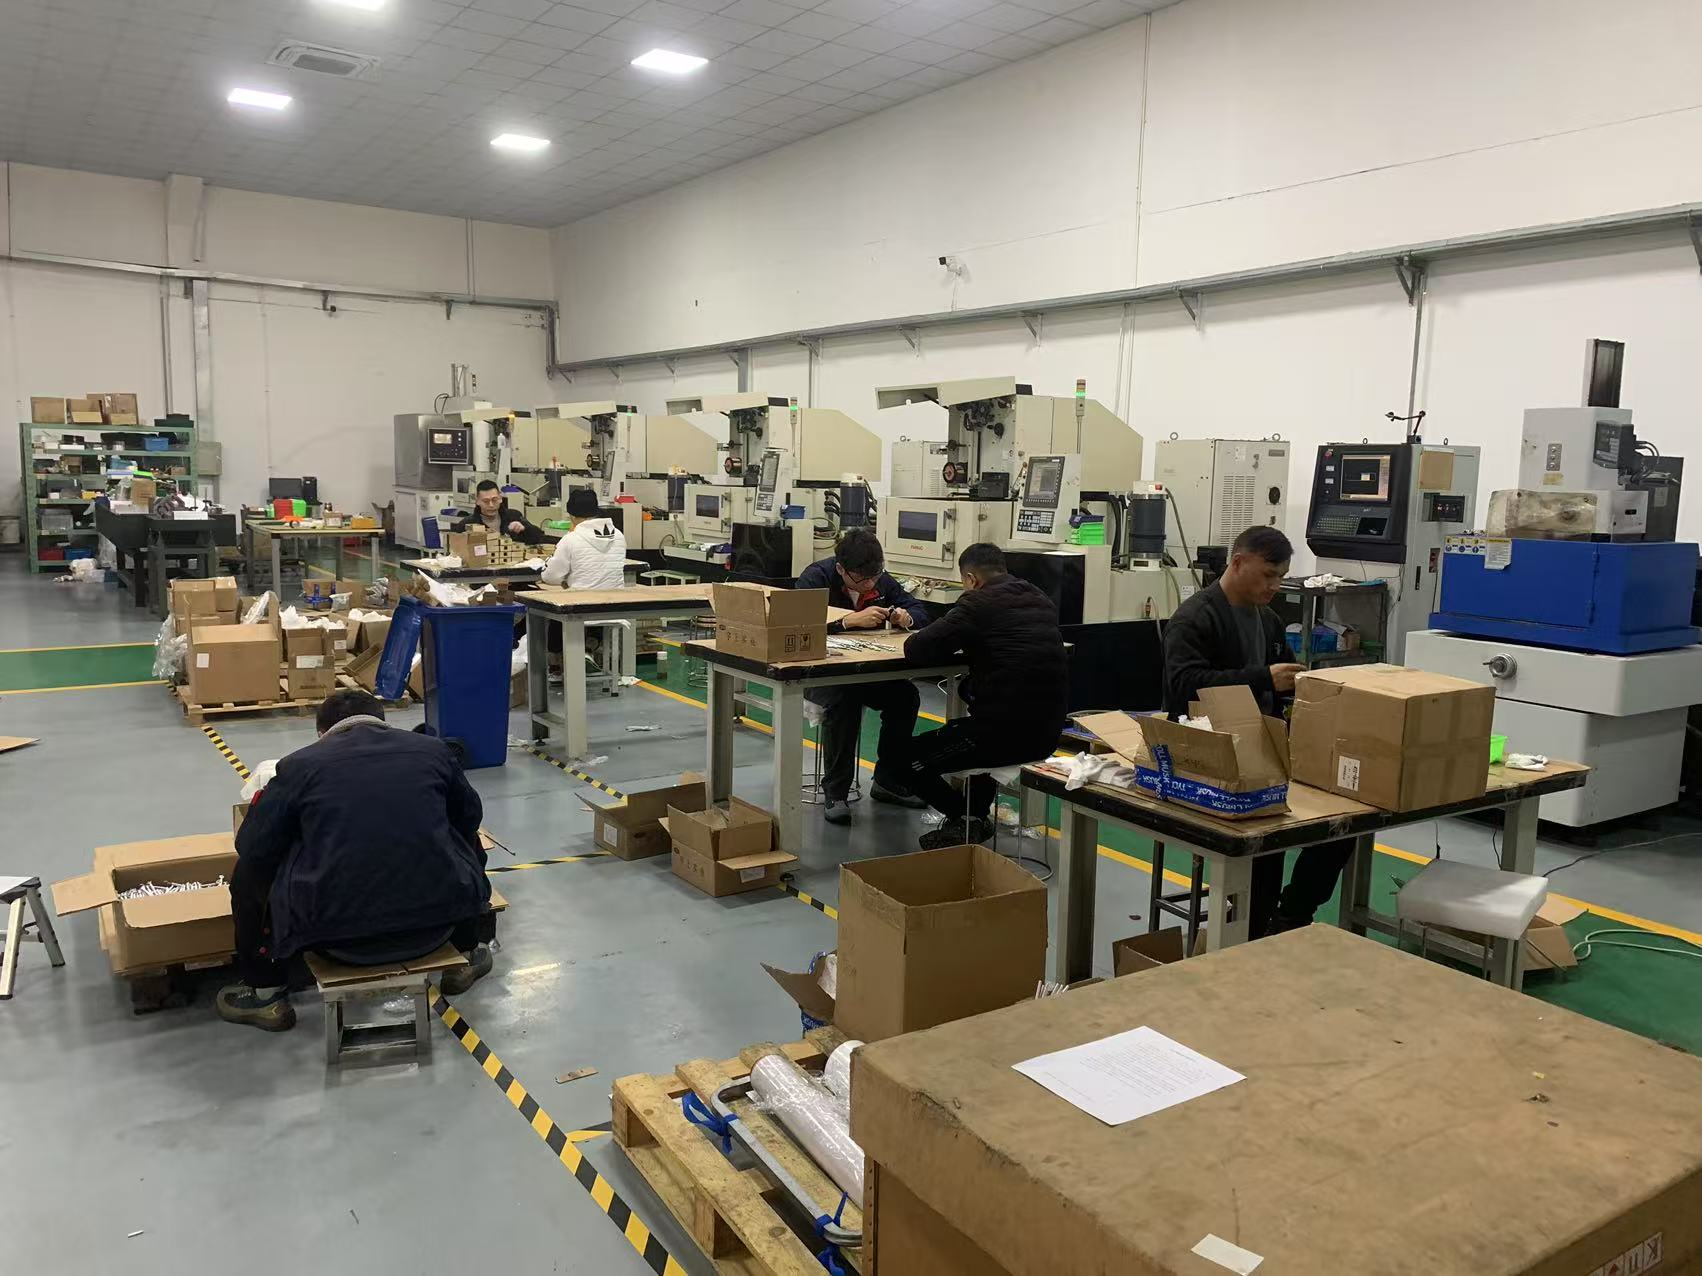
Capacity range from prototype to mass production matters only when the buyer's own batch profile is mapped against it.
Structuring the RFQ Around Hard Data Points
The framework converts into six practical steps that can be applied to any CNC supplier, not only to ECOD.
- 1. Put the measurement requirement in the drawing package. Specify critical characteristics, datum structure, and any characteristics that require 100% verification. A tolerance discussed in conversation cannot be enforced later.
- 2. Ask for the proof format, not another assurance. For a ±0.005 mm requirement, request a dimensional inspection report tied to the drawing and confirmation of CMM inspection coverage. For material, request raw material certification verification.
- 3. Separate process capability from production capacity. Equipment lists confirm capability; order quantity confirms whether the part sits inside the supplier's stated range of prototypes, small batches, or mass production.
- 4. Fix commercial terms inside the same document. In ECOD's published terms, MOQ is 1 unit; delivery terms cover EXW, FOB, CIF, CIP, FCA, CPT, CFR, DAP, and DDP; payment terms are a 30% deposit with the 70% balance due before shipment. Keeping terms on one quotation prevents later renegotiation.
- 5. Define the acceptance route in advance. Factory inspection is the stated acceptance criterion, which means the buyer should confirm what is inspected, what record is issued, and who signs before shipment.
- 6. Agree what happens on repeat orders. Specify how long a first article inspection remains valid, when a process change triggers re-approval, and how long inspection records are retained. This is what turns a supplier relationship into a repeatable process rather than a series of one-off purchases.
Verification Limits Buyers Should Accept
A credible framework states where it stops working.
- Tolerance is conditional. A capability figure cannot be verified independently of part geometry, material, and measurement method, so the same nominal tolerance can be realistic on one feature and unrealistic on another.
- Public records cover process, not proprietary order history. Buyers can verify inspection documentation, material certification, and terms; they generally cannot verify a supplier's full customer history or internal cost structure.
- Third-party market data carries scope risk. Market size and growth estimates differ by definition, as the 2025 machine market figures from Fortune Business Insights and Dataintelo demonstrate.
- Certification scope is not transferable by assumption. Aerospace CNC machining requires AS9100 certification, which incorporates ISO 9001 plus more than 100 additional requirements for safety and reliability, according to SAE International, and medical device production operates under ISO 13485 quality management requirements. A general quality system is not equivalent to either standard, and buyers in regulated industries must confirm the specific scope rather than the certificate's existence.
Future Outlook
Several directional signals suggest that evidence-based sourcing will become the default rather than a differentiator.
Ultra-precision machining centers serving semiconductor fab equipment are projected to grow at 8.36% CAGR from 2026 to 2031, according to Mordor Intelligence. Segments with that growth profile tend to pull documentation standards upward across the supply base, because they cannot tolerate unverifiable capability claims.
The labor picture reinforces the same direction. With 75,000 unfilled CNC operator roles reported in the U.S. machining sector in 2023, capacity is increasingly constrained by skilled labor rather than machine availability — which raises the value of suppliers whose quality depends on documented process control rather than operator discretion.
Cost pressure is unlikely to disappear. U.S. machine shop services revenue reached approximately USD 46.3 billion by 2026 with a 0.2% CAGR over five years, a slow trajectory attributed by IBISWorld to material price volatility. Buyers should therefore expect quotation sensitivity to material markets and should treat batch-size-dependent pricing claims, such as ECOD's stated 10% advantage on medium and large batch orders, as variables to confirm per project rather than constants.
The practical expectation for the next procurement cycle is that inspection data — CMM reports, first article inspection records, and material certificates — moves from a special request to a standard deliverable attached to the quotation.
Frequently Asked Questions
Which commercial terms should be locked before a first production order?
MOQ, delivery terms, acceptance criteria, and payment structure should all be confirmed in writing before production begins. In ECOD's published terms, the minimum order quantity is 1 unit; delivery terms include EXW, FOB, CIF, CIP, FCA, CPT, CFR, DAP, and DDP; acceptance criteria are factory inspection; and payment terms are a 30% deposit with the 70% balance due before shipment.
How can a buyer verify a stated ±0.005 mm tolerance before production?
Request the proof type rather than a repeated assurance. In practice this means a dimensional inspection report tied to the part drawing, CMM inspection data, a first article inspection record, and raw material certification verification. The buyer should also confirm which features, part sizes, and materials the tolerance is being applied to, because ±0.005 mm describes a process envelope rather than a universal part-level guarantee.
What does 100% dimensional inspection cover, and what does it not cover?
It establishes that the dimensional characteristics listed in the inspection plan are measured on every unit in the batch and recorded as documentation. It does not automatically cover characteristics outside that plan, such as surface finish, hardness, or functional performance, unless those are explicitly included. Buyers should confirm the inspection plan contents before treating the statement as complete coverage.
Which quality-system references matter when parts go into regulated end markets?
Aerospace CNC machining requires AS9100 certification, which incorporates ISO 9001 plus more than 100 additional requirements for safety and reliability, according to SAE International. Medical device production is governed by ISO 13485 for quality management systems. A general ISO 9001-based system is not equivalent to either, so buyers in regulated industries should verify the specific certification scope rather than the general existence of a quality certificate.
How should buyers use third-party CNC market forecasts during supplier selection?
Published market data is a scope-defined planning input, not supplier evidence. Estimates diverge: the 2025 global CNC machine market is given as USD 101.22 billion by Fortune Business Insights and USD 98.7 billion by Dataintelo, and CAGR forecasts range from 3.5% to 11.1% depending on whether services and software are included. The practical use is capacity and segment planning, not supplier comparison.
What evidence supports a long-term supply relationship rather than a one-off order?
Consistency records rather than single results: batch-to-batch inspection conformance, stability of material certification, delivery performance against an agreed measurement rule, and the ability to hold the same acceptance route across repeat orders. In ECOD's case the stated indicators are an on-time delivery rate above 98%, 100% dimensional inspection, and the provision of material certificates and dimensional inspection reports for all orders. These become decision-grade only when converted into contractual KPIs with defined measurement windows.
Conclusion
A CNC sourcing decision becomes defensible when each supplier statement is sorted into one of two categories: evidence that exists today, or a validation task with an owner and a deadline. Tolerance, inspection coverage, material verification, and commercial terms can be handled during the RFQ stage. Cost position, delivery performance, and application fit require either contractual definitions or a project-specific test.
Applied consistently, this framework does not eliminate judgment. It makes the basis of judgment explicit — which is what allows a buyer to compare suppliers, justify the decision internally, and manage the relationship over repeat orders rather than re-litigating the same claims each time.
ECOD's CNC machining capability set, material coverage, and commercial terms are summarized in its downloadable product brochure: ECOD product brochure (PDF). Company information is also published at www.ecod-cncmachining.com.