
Compare Nonwoven Fabric Machine Lines: Buyer Scorecard
Compare Nonwoven Fabric Machine Lines: Buyer Scorecard
A side-by-side comparison of nonwoven fabric machine lines is only useful if every supplier is measured on the same basis. The practical method is to build a weighted scorecard before quotations arrive: define the reference product, normalize technical data to the same polymer, width, grammage and output conditions, grade the evidence behind each claim, write acceptance criteria into the inquiry, and score purchasing terms on the same matrix as machine performance. This framework does not rank manufacturers; it gives a decision-stage buyer a repeatable way to compare a spunbond nonwoven machine, an SMS nonwoven machine, a spunmelt nonwoven machine or a complete nonwoven production line without letting brochure language decide the outcome.
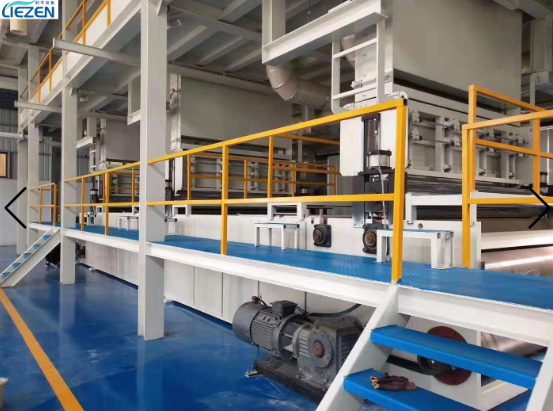
Why a side-by-side scorecard is different from a feature list
Feature lists are seller-shaped. They mix nameplate values, optional modules, different product targets and undefined test conditions. A scorecard is buyer-shaped: it starts with the product the buyer must make, then asks each supplier to prove the same claim under the same conditions. The difference matters because a nonwoven making machine is not a single interchangeable item. A line can be configured for single-S, SS, SSS, meltblown, SMS, SMMS or other layer combinations, and each configuration changes the commercial and technical comparison. The buyer's task is not to find the longest list. It is to find the line whose demonstrated configuration, flexibility and contract terms fit a defined product plan.
Step 1: Fix the comparison basis before any score is assigned
Comparisons fail when supplier A quotes at 12 gsm and supplier B quotes at 25 gsm, or when one speed is described as mechanical maximum and another as stable production speed. Before scoring, fix a reference basis and put it in the RFQ. Useful controls include: target product family and layer structure; polymer grade and melt index range; basis-weight band and the test points inside that band; finished roll width and edge trim; stated output basis, such as kg/h at a defined gsm and width; energy boundary, including extruder, heating, bonding, fans and utilities included in the figure; uptime definition and measurement period; and the product tests that will define acceptance.
The buyer should also assign an evidence grade to each data point. A supplier datasheet is a claim. A factory acceptance test record is stronger. A signed acceptance protocol with agreed sampling is stronger still. Scoring should reflect both the value and the quality of the evidence, because a precise number from an undefined test is not equivalent to a less precise number from a controlled test.
Step 2: Score machine configuration on normalized data
Machine configuration should be scored in modules, not as a single headline. The first module is line architecture: number of beams, layer structure, meltblown integration, bonding method and winding arrangement. The second is the extrusion and spin system: extruder capacity, filtration, spin-beam design, quenching and filament cooling. The third is web handling and bonding: forming belt or drum, calender or other bonding, tension control and edge trim. The fourth is winding and roll quality. Each module should be scored on the same reference product.
Width and speed belong in the scorecard only when they are tied to a stated gsm, polymer and quality result. A line that runs fast at a heavy basis weight may not hold the same speed at a light hygiene grade. Throughput should be recorded in kg/h with the calculation basis shown, not as an unqualified monthly capacity. Energy should be recorded at a defined boundary. If one supplier counts thermal energy and another counts only electrical power, the comparison is not like-for-like. The buyer can normalize by requesting a utility schedule with the same inclusions and by running a sensitivity check on energy price.
| Configuration field | What to request | Why it matters | Scoring rule |
|---|---|---|---|
| Layer architecture and bonding | Beam count, meltblown position, bonding method and winding type | Defines product capability and upgrade path | Score against the buyer's three target products, not the catalog maximum |
| Width and speed | Effective width; demonstrated speed at stated gsm, polymer and quality | Nameplate speed can mislead | Use the lowest demonstrated stable speed at the agreed quality point |
| Output | kg/h with gsm, width and efficiency basis | Capacity claims are not comparable without basis | Recalculate to the same width and gsm; show the formula |
| Polymer and formulation | PP or PE grade, melt index, additives and bicomponent option | Material changes output and quality | Score only the grades the buyer will actually run |
| Energy and utilities | Electrical, thermal, compressed air and water, with metering boundary | Different boundaries distort operating cost | Request the same boundary; apply the buyer's energy prices |
| Controls and data | Recipe management, alarms, trend logging and remote support | Affects changeover and troubleshooting | Score as verified functions, not brochure labels |
Step 3: Turn product flexibility into testable evidence
Flexibility is often scored from a catalog count: how many layer combinations, how many gsm, how many applications. That is weak evidence. A better method is to ask each supplier to run a product matrix against the buyer's actual portfolio. The matrix should include the three to five products that will matter in the first two years, not every product the line could theoretically make. For each product, record the target gsm, layer structure, polymer, additives, line speed, output, key quality attribute and the test method.
Then ask what changes during a product changeover: spin packs, screens, calender settings, winding parameters, recipe download and purge time. The score should reflect the number of target products that can be made within the declared quality window, not the number of combinations printed in a brochure. This is where a spunbond nonwoven machine, an SMS nonwoven machine and a wider spunmelt nonwoven machine diverge in practice. A line that is flexible on paper may require long changeover, high scrap or manual tuning that is not captured in the layer count.
The buyer should also define the commercial value of flexibility. If the business plan is a focused roll product at stable output, flexibility may carry modest weight. If the plan includes multiple grades or seasonal product changes, changeover time, repeatability and recipe control deserve more weight. An automotive interior nonwoven production line and a sanitary napkin nonwoven fabric machine may sit at different ends of this weighting decision. The first may place more value on dimensional stability and bonding consistency across lots; the second may place more value on roll quality and consistency at high output. The scorecard should make that trade-off explicit rather than treating flexibility as universally good.
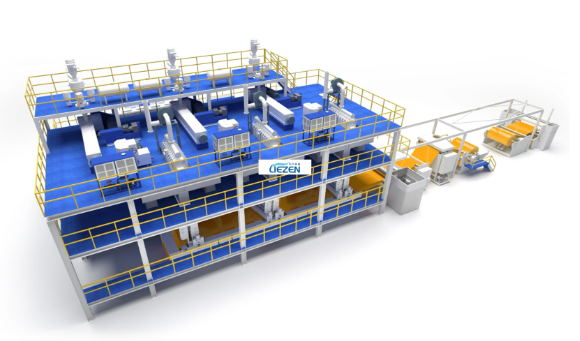
Step 4: Write acceptance criteria before negotiating price
Acceptance criteria are the bridge between a comparison and a contract. They should be written before price is finalized, because a low price with vague acceptance transfers technical risk to the buyer. The buyer should define a factory acceptance test and a site acceptance test with the same logic. The protocol should state the reference product, the test points, the sampling method, the measurement method, the pass rule and the consequence of a failed test.
ISO 9073 is the dedicated ISO series of test methods for nonwovens and provides a neutral vocabulary for fabric acceptance. It is a series, not a single document; individual part numbers and editions must be confirmed for each property before they are written into a contract. The acceptance plan should separate product properties from line performance. Product properties may include basis weight, thickness, tensile strength, elongation, air permeability, hydrostatic head or other attributes relevant to the end use. Line performance may include stable output at the reference product, start-up time, energy consumption at a defined boundary, waste rate during steady operation and changeover time.
The buyer should also define how the line will be run during the test: which polymer, which operating team, which utilities and which quality limits. Without those conditions, an acceptance test can become a negotiation after installation rather than a decision rule before it.
| Acceptance area | Criterion to define | Evidence | Contract effect |
|---|---|---|---|
| Reference product | gsm, width, layer structure and polymer | Product specification and sample | Defines the only product set used for acceptance |
| Test methods | Property-specific method and edition | ISO 9073 part or agreed internal method | Reduces post-test disputes about method |
| Sampling | Frequency, roll position and number of samples | Signed sampling plan | Makes pass or fail statistically defensible |
| Performance | Stable output, energy, waste and changeover | FAT and SAT records plus trend logs | Links payment or retention to demonstrated performance |
| Ramp-up | Time to stable quality after start | Commissioning plan | Clarifies responsibility for start-up losses |
Step 5: Use weights and evidence grades, not false precision
A weighted scorecard helps only if the weights are set before scores are visible. The buyer should start from the business plan, not from the supplier's strengths. A simple structure is: machine configuration and demonstrated performance; product flexibility against the target matrix; acceptance and quality control; purchasing and lifecycle terms; and service and spare-parts readiness. The weights should sum to 100%. They should be documented with the reason for each weight. Scores should use a defined scale, such as 1 to 5, with a written anchor for each point.
Each score should carry an evidence grade. One practical approach is to multiply the raw score by an evidence factor: for example, 1.0 for verified test or audit evidence, 0.8 for a documented supplier calculation that can be checked, and 0.6 for a brochure claim without supporting data. The factors are a buyer's policy choice, not an industry standard. Their purpose is to stop a well-written claim from outranking a weaker but more relevant fact.
The score formula can be stated as: total score equals the sum of criterion score multiplied by criterion weight multiplied by evidence factor. Show the weights, scores, factors and source of evidence in the same sheet. Keep notes on missing data. A missing value should be scored as missing, not as zero, because zero can punish a supplier for a data gap while hiding the reason. If a criterion is essential and the data is missing, the line should be held for clarification rather than ranked.
The buyer should then run a sensitivity check. If a line wins only when a low-weight criterion is set to an extreme, the result is fragile. The shortlist should be stable across reasonable weight changes. This is more useful than a single decimal score that implies precision the evidence does not support.
Step 6: Compare purchasing terms on the same matrix
Purchasing terms are part of the machine comparison, not a separate commercial negotiation. The buyer should build a scope matrix that shows what each offer includes and excludes. Typical lines of comparison include: process scope and interface batteries; civil works and utilities; installation and commissioning; training; spare parts; warranty; response time; remote support; performance guarantees; payment milestones; delivery and logistics; and customs classification.
The last item deserves early attention. Nonwoven line machinery may be declared under different HS headings depending on configuration and national customs practice. WCO HS 2022 heading 8444 covers machines for extruding, drawing, texturing or cutting man-made textile materials; heading 8445 covers machines for preparing textile fibres and producing yarns; heading 8477 covers machinery for working rubber or plastics. Spunbond and spunmelt equipment can involve more than one of these headings, and trade statistics across them are not additive. The buyer should ask the supplier for the proposed classification and confirm it with a customs broker before comparing landed cost.
On service, the offer should state the spare-parts list, recommended critical spares, warranty terms, response time and the division of responsibilities during commissioning. These items are not administrative details. They change the real cost of ownership and the risk of a line that meets the test but stops in the first year.
| Purchasing term | What to compare | Common trap |
|---|---|---|
| Scope of supply | Equipment, utilities, civil works, installation, commissioning and training | Comparing ex-works equipment with a turnkey offer |
| Spare parts | Critical list, wear parts, recommended stock and lead time | A low price with no critical spares |
| Warranty and response | Duration, coverage, response time and remote support | Warranty excludes consumables or performance |
| Payment | Milestones tied to delivery, FAT, SAT and ramp-up | Most payment released before acceptance |
| Logistics and HS | Incoterm, insurance and proposed HS heading | Landed cost compared on different classifications |
| Performance guarantees | Output, energy, quality and remedies | Guarantees without a test protocol |
Where side-by-side comparisons usually fail
Five failures are common. First, nameplate speed is compared with demonstrated speed. Second, different gsm or polymer is used for each offer. Third, flexibility is scored from a catalog rather than a product matrix. Fourth, acceptance is left to a general clause instead of a test protocol. Fifth, purchasing terms are compared after the technical choice, when the buyer has already anchored on one supplier.
A sixth failure is the missing-data problem: a blank cell is treated as a low score instead of an open question. Each failure can be controlled with the same discipline: define the basis, request the evidence, normalize the unit, grade the source and record the assumption. The scorecard should be an audit trail, not a beauty contest.
A decision rule for the shortlist
A defensible shortlist decision can be stated in four steps. First, eliminate any line that cannot meet the mandatory product and acceptance requirements. Second, compare the remaining lines on the weighted score. Third, run a sensitivity check on the weights and evidence factors. Fourth, review the purchasing terms and service model for the top two or three lines.
The output should identify the fit boundary for each line: the product range where it is strongest, the range where it needs confirmation, and the terms that must be resolved before commitment. This is more useful than a single winner because a nonwoven production line is a long-life asset with a specific product plan. The buyer should be able to explain why a line was shortlisted, what evidence supports the decision and what remains open. That explanation is also the basis for a fair negotiation.
Market context: why the scorecard deserves discipline
Market context supports the case for a disciplined comparison, but it should not replace the buyer's own product plan. Maximize Market Research valued the global non-woven fabric making machine market at USD 2.20 billion in 2025. A 2026 Dataintelo report estimates that spunbond technology held a 40% share of the nonwoven machinery market in 2025. Fortune Business Insights projects the spunbond nonwoven fabric market to grow from USD 15.6 billion in 2023 to USD 28.2 billion in 2033 at a 6.1% CAGR. These are source-reported figures, not a forecast of any individual supplier's results.
Their practical meaning is that spunbond and spunmelt configurations remain central to many investment decisions, and that a buyer who compares lines on normalized evidence is in a stronger position than one who compares headline capacity. The same discipline applies whether the project is a single-S PP spunbond nonwoven machine, an SMS line or a multi-beam spunmelt nonwoven machine.
FAQ
What should come first in a nonwoven fabric machine comparison?
Start with the reference product and acceptance basis, not the supplier list. Define the target gsm, width, layer structure, polymer and quality tests. Then ask every supplier to quote and prove performance on that same basis. This prevents a fast line at a heavy basis weight from being compared with a slower line at a light hygiene grade.
How can buyers compare product flexibility across nonwoven production lines?
Use a product matrix rather than a catalog count. List the three to five products the buyer expects to make in the first two years. For each product, request target gsm, layer structure, polymer, demonstrated speed, output, quality result and changeover requirements. Score the number of target products that can be made within the declared quality window. A long list of theoretical combinations is weaker evidence than a short list of demonstrated products.
Which acceptance criteria should be fixed before signing?
Fix the reference product, test methods, sampling plan, pass rule and consequences of failure. ISO 9073 is the dedicated ISO series of test methods for nonwovens, but it is a series, so the specific part number and edition must be confirmed for each property. Also define line-performance tests such as stable output, energy at a stated boundary, waste during steady operation and ramp-up time. The acceptance protocol should be part of the contract, not a post-installation discussion.
How should purchasing terms be weighted against machine performance?
Purchasing terms should be scored on the same matrix as technical performance, with weights set before offers are opened. Compare scope of supply, spare parts, warranty, response time, payment milestones, logistics and customs classification. A low equipment price can be offset by excluded installation, missing critical spares or a vague performance guarantee. The buyer should compare landed cost and lifecycle risk, not only the machine price.
Conclusion
A side-by-side comparison of nonwoven fabric machine lines is a decision process, not a spreadsheet exercise. The buyer needs a fixed reference product, normalized technical data, evidence-graded claims, a product-flexibility matrix, written acceptance criteria and a purchasing-term matrix that exposes scope and lifecycle risk. When those elements are in place, the scorecard can compare a spunbond nonwoven machine, an SMS nonwoven machine or a spunmelt nonwoven machine without relying on manufacturer labels. The result is a shortlist that can be explained, negotiated and defended long after the quotation stage.
This framework is vendor-neutral and does not rank or endorse any manufacturer. Its purpose is to make the buyer's comparison basis visible, testable and consistent across suppliers.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.