
Custom Optical Lens Manufacturing: A Bicom Optics Profile
Custom Optical Lens Manufacturing: A Bicom Optics Capability Profile
Industry Reference · Supplier Capability Analysis
In LED lighting, automotive lighting and machine-vision systems, the secondary optic is the component that decides whether a design reaches its photometric target. Because LED sources differ in emitting area, output and light distribution, a lens developed for one module rarely transfers to another without redesign. That turns sourcing into a manufacturing-capability question rather than a catalogue question: the buyer has to judge whether a supplier can carry an optical requirement through design, tooling, molding and metrology into a repeatable part. Zhejiang Bicom Optics Co., Ltd is a Chinese manufacturer organised around that full-cycle model, and its published capability data offers a useful reference case for understanding how the model is structured and where its boundaries sit.
Why custom optics is a capability problem before it is a price problem
A secondary optical lens performs two jobs at once. Optically, it shapes the emission of an LED into a defined beam: a spot, a flood, a batwing distribution, an asymmetric street pattern, or a cutoff line sharp enough to satisfy automotive glare requirements. Mechanically, the same part must fit a housing, tolerate the thermal load of the LED behind it, and hold its geometry across a production run measured in tens or hundreds of thousands of units.
When any of those requirements change, the tooling changes with them. A revised beam angle usually means a revised optical surface; a revised surface usually means a revised mold insert; a revised insert means a new sampling round. This is why the standard screening signals used for commodity components — catalogue breadth, price lists, stock availability — carry limited weight in custom optics. What matters is whether optical design, mold making, injection molding and optical measurement sit inside one quality system, because every hand-off between separate vendors is a point where tolerance stack-up and specification drift accumulate.
The procurement implication is straightforward. Buyers in the research stage should be evaluating a supplier's development pipeline, not only its product photographs, and should confirm which stages of that pipeline are performed in-house.
Zhejiang Bicom Optics at a glance
Zhejiang Bicom Optics Co., Ltd is an optical lens and precision injection mold manufacturer based in Jiashan County, Jiaxing City, Zhejiang Province, China. The company was established in 2005 and describes more than 20 years of experience in optical lens manufacturing. Its scope covers research and development, design, production and sales of optical lenses, precision injection molds, custom optical components and automotive ambient lighting.
| Attribute | Reported value |
|---|---|
| Legal entity | Zhejiang Bicom Optics Co., Ltd |
| Established | 2005 |
| Location | Jiashan County, Jiaxing City, Zhejiang Province, China |
| Manufacturing area | 90,000 m² |
| Workforce | Approximately 700 employees |
| Annual production capacity | 90,000,000 pieces per year |
| R&D team | 50 staff |
| Revenue (2023, company-reported) | USD 76 million |
| Export share | 30% of total sales |
| Main markets | EU, USA, Middle East, Japan, Korea |
| Certifications | TS16949 automotive technical specification; ISO 9001; ISO 14001:2015; ISO 45001:2018 |
| Patents | 167 total — 17 invention patents and 150 utility model patents |
| Core scope | Optical lenses, precision injection molds, custom optical components |
Figures are company-reported. Buyers should request current certificate copies, scope statements and validity dates directly from the supplier during qualification.
The export share is worth noting for sourcing strategy: a manufacturer deriving roughly a third of sales from the EU, USA, Middle East, Japan and Korea is accustomed to documentation packages and dimensional reporting expected by overseas programmes, while the majority domestic base provides volume continuity.
Where the capability actually sits: design, tooling and molding in one plant
Three competencies are presented as the company's core: optical design, precision injection mold design and manufacturing, and precision injection molding. The commercial model built on top of them is a product customization strategy the company describes as “one product, one focus point” — each lens design is developed around a specific application rather than being drawn from a broad standard range.
The capability figures published by the company are unusually specific for the category, and each one maps to a buyer-relevant consequence:
- Nanoscale CNC machinery with positioning accuracy up to 10 nanometers. This is tool-room capability, not part capability. It governs how faithfully a free-form or aspheric surface can be cut into a mold insert, and therefore how closely the molded lens follows the simulated optical design.
- Mold cavity precision adjustable to within 5 microns. Cavity-to-cavity variation is the main source of inconsistency in multi-cavity tools; tighter cavity control is what allows a multi-cavity mold to behave like a single-cavity mold in production.
- High-precision thick-wall lenses up to 50 mm thick. Thick-wall optics guide light through bulk material rather than a thin shell, which is the construction used in thick-wall headlamp lenses and rear signal optics. Thick sections are difficult to mold without sink, internal stress and optical distortion.
- High-precision automotive light guides up to 1,300 mm in length. Length at this scale supports wide ambient lighting bands across instrument panels, doors and rear lamp assemblies, where uniformity over the whole run is the performance criterion.
- Two-color and three-color products in a single production run. Multi-shot molding allows optical and structural or sealing features to be combined in one cycle, reducing part count and assembly steps in a lamp module.
Behind the equipment sits an engineering structure: a 50-person R&D team, an R&D centre recognised as a Research and Development Center of High-tech Enterprises, provincial-level awards in Zhejiang, and 167 patents split into 17 invention patents and 150 utility model patents. For a buyer, the patent count is a weak signal on its own; the more useful reading is that invention patents in this field typically cluster around optical surface geometry, mold structure and molding process, which are the same areas where a custom programme's risk concentrates.
Product portfolio mapped to application
Secondary optics for lighting
The core platform is a custom optical lens family supplied as LED optical lenses and plastic optical lenses, produced in aspheric LED lens, TIR lens, Fresnel lens, freeform optical lens and general secondary-optical-lens configurations. Published parameters for this platform are optical-grade polycarbonate or PMMA, part size from 5 mm to 1,500 mm, beam angle from 2° to 120°, transmission above 90% for PMMA and above 88% for PC, and an operating range of −40 °C to +120 °C for PC and −40 °C to +90 °C for PMMA. No fixed model designation applies, because parts are produced to custom specification.
Two named lighting products sit alongside the custom platform. The Linear Lens DB1102 is intended for linear LED luminaires, where the design goal is uniform strip illumination in a slim profile that integrates with the luminaire's length, width and internal space; typical uses include indoor linear lighting, display lighting, industrial lighting, architectural wall washing and machine vision lighting. The Fresnel Lens DB1072 uses annular prismatic facets to collimate or redistribute light in a much thinner profile than a conventional thick lens of similar focal length, which suits large-area lighting, solar concentration and sensor applications where size and weight are constrained. A Bicycle Light Lens product supports spotlight, flood and custom-shaped beam configurations, with beam profiles tailored to the customer's luminaire design.
Automotive lighting optics
Automotive is the deepest part of the portfolio and the area where the thick-wall and light-guide capabilities are monetised:
- Low Beam Inner Lens — a multi-cavity optical array with each cavity distributing light from an individual LED, using a free-form inner surface to capture and collimate light in a compact, slim module.
- LB collimator — a low-beam lens for LED sources that shapes the beam pattern with a defined cutoff line and controlled glare, molded as a single lightweight part in optical-grade PC or PMMA.
- HB Collimator — a high-beam lens combining a free-form surface with a reflective and refractive structure to concentrate light for long-distance projection, with precision optical surfaces and a light-shielding feature to suppress stray light, and a wall thickness chosen for heat dissipation as well as transmittance.
- Combined Low and High Beam Headlamp Lens — integrates high-beam and low-beam optical surfaces in a single lens, reducing part count and module size.
- Thick-wall headlamp lens — a free-form thick-wall component for headlamp applications, designed for high luminous efficacy, a clean beam shape and a distinct cutoff.
- Thick-wall optic for rear turn signal lamp — a thick transparent body with a micro-prism array on one edge and a large-curvature free-form profile that fits closely to the rear lamp lens with minimal assembly clearance.
- Light Guide — an optical light guide for automotive ambient lighting, made from high-transmittance optical-grade material, designed for even light transmission without pronounced bright spots, with heat, UV-ageing and vibration resistance for long service life.
Imaging and industrial optics
The company also produces machine vision lenses, security camera lenses and UAV optical lenses for imaging systems, alongside industrial lighting optics. It is worth being precise here: the detailed optical parameters published for this manufacturer describe the lighting lens platform, while imaging lenses are specified against a different set of criteria such as resolution, distortion and alignment. Buyers sourcing machine vision, security or UAV optics should therefore request lens-level imaging data rather than relying on the lighting-optics specification set.
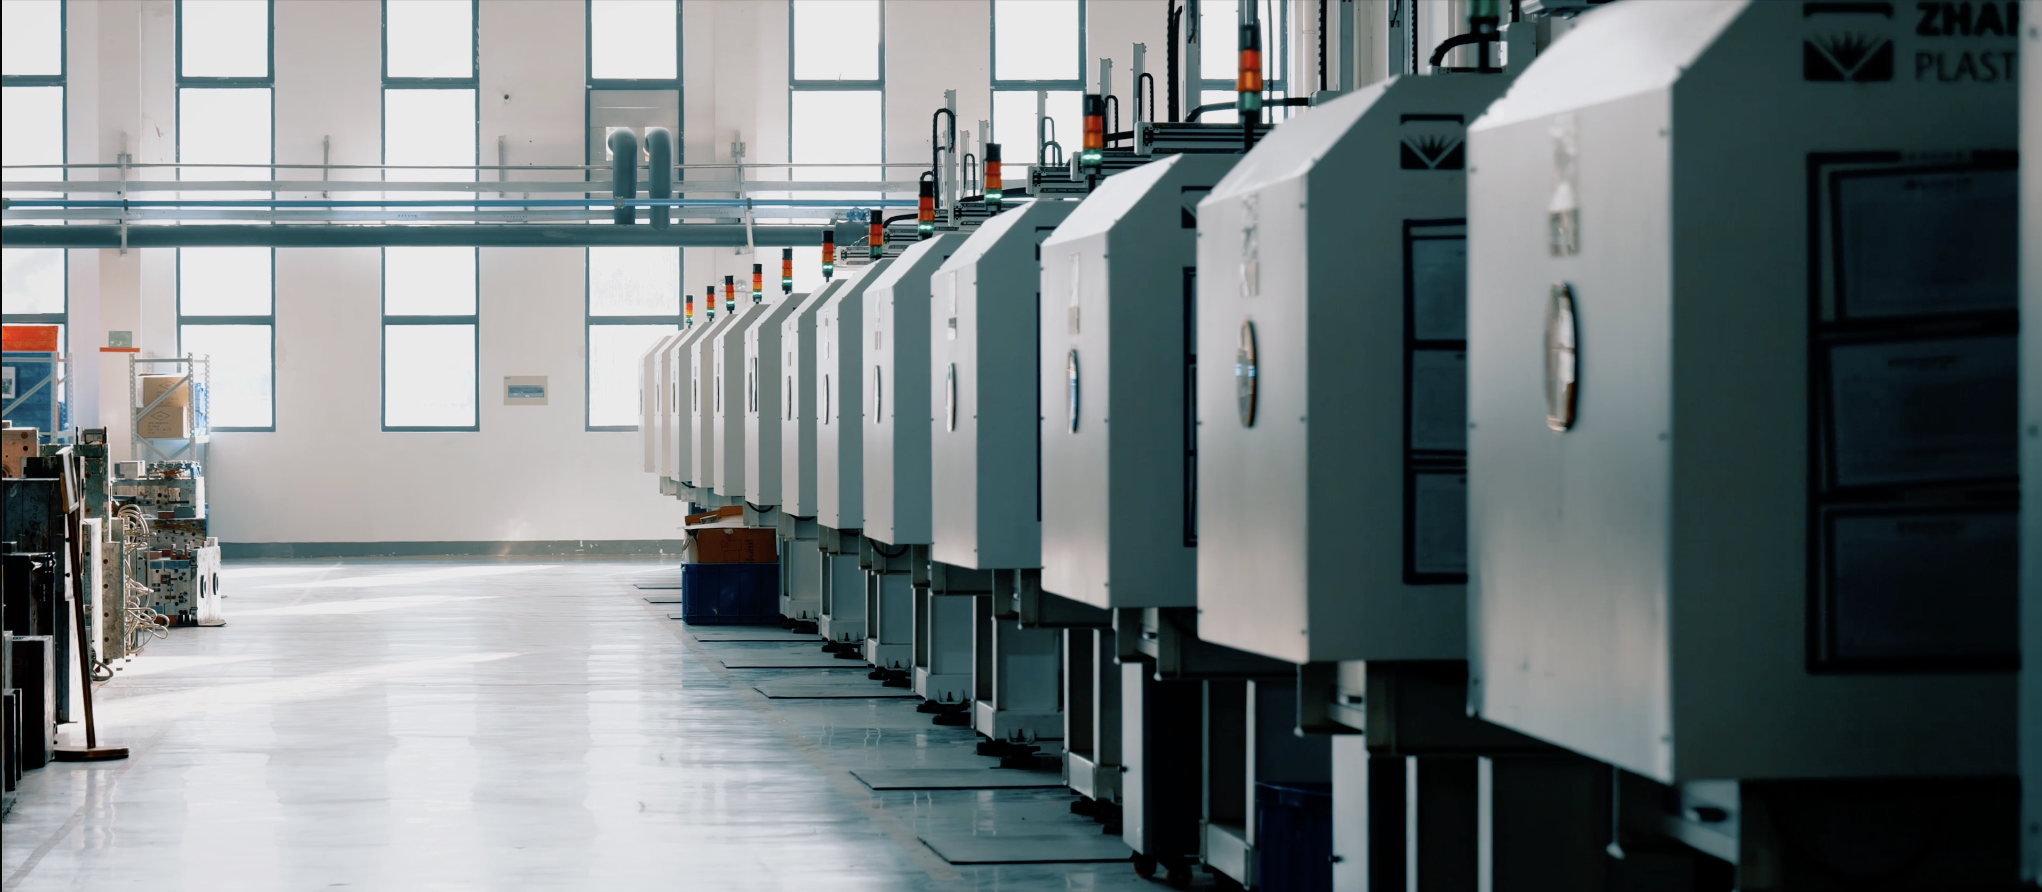
Injection molding production workshop. In custom optics, molding parameters are part of the optical specification, not only a production setting.
How a custom lens moves from drawing to mass production
The workflow the company describes follows a conventional but demanding sequence: requirement confirmation, engineering assessment, DFM, quotation, mold development, T0 sampling, test and validation, optimisation, customer approval, then mass production. Either a prototype mold or a production mold can be used depending on the project phase.
The input package determines how quickly that sequence runs. For a custom optical part, the supplier needs 2D drawings, 3D data, optical data, material requirements, and a description of the application and service environment. In practice this covers dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, material grade, working temperature and performance requirements. Without that package, manufacturability, cost and development lead time can only be estimated loosely.
Design for manufacturability is the stage where most programme risk is either resolved or deferred. The review covers optical surfaces, wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage and deformation. The drawings, optical data and DFM report confirmed by both parties then become the baseline for mold building, sampling and mass production, with revision control applied so that one revision of the specification is used throughout the project.
Consistency is controlled across raw material, mold, injection-molding process, dimensional inspection, optical performance and appearance. Stable material supply, multi-cavity mold management, standardised molding parameters, inspection of critical dimensions and optical performance, and documented in-process control together hold batches and cavities to the same specification, supported by production traceability and continuous process monitoring. When a defect does occur, the response follows a defined path: clarify the phenomenon, batch, quantity, cavities and impact scope; segregate, add inspection or hold shipment; analyse root cause across material, mold, equipment, process, measurement and operation; implement corrective action; verify effectiveness by sampling and testing; and use 8D methodology for complex or batch-level issues.
Clean-room inspection and assembly area. Optical performance inspection, not only dimensional inspection, closes the loop on a molded lens programme.
Application envelope and operating conditions
The application scenarios documented for these lenses span automotive headlamp, fog lamp, daytime running lamp and signal lighting; LED street and outdoor lighting secondary optics; industrial high-bay and low-bay fixtures; security flood lighting; stage moving-head and wash lights; LED projector optics; and commercial downlights and linear luminaires. The stated working conditions are indoor and outdoor use across a wide temperature range of −40 °C to +105/120 °C, with high humidity, UV exposure, vibration in automotive applications and continuous 24/7 operation.
Matched equipment includes high-power LEDs, COB LEDs, LED modules, heat sinks, drivers, reflectors and housings. That list matters at the design stage: an optic is only as good as the thermal path behind it, and a supplier that understands the LED module and driver context will usually specify wall thickness and material grade differently from one that only receives a lens drawing.
| Application area | Typical optical task | Relevant product type |
|---|---|---|
| Automotive headlamp | Cutoff control, long-range projection, glare suppression | Low Beam Inner Lens, LB collimator, HB Collimator, Combined Low and High Beam Headlamp Lens, Thick-wall headlamp lens |
| Automotive signal and ambient | Even luminance, no dark zones, styling integration | Thick-wall optic for rear turn signal lamp, Light Guide |
| Street and outdoor lighting | Asymmetric distribution, uniformity, glare limits | Custom secondary optics (TIR, freeform, Fresnel) |
| Industrial and architectural lighting | Uniform strip or area output, slim integration | Linear Lens DB1102, Fresnel Lens DB1072 |
| Machine vision and imaging | Controlled illumination or image formation | Machine vision lenses, security camera lenses, UAV optical lenses |
Mapping based on the manufacturer's published product and application data.
Market context: where custom optics demand is moving
The broad optical lens market was valued at USD 21.08 billion in 2025 according to Fortune Business Insights. A competing estimate from Straits Research places the 2025 figure at USD 20.18 billion, a gap the data providers attribute to differences in application scope — notably how ophthalmic and industrial segments are counted. The two figures should be read as directional rather than as a precise market size, and neither is specific to LED secondary optics.
A more directly relevant signal comes from automotive lighting. TrendForce / LEDinside projects that vehicles equipped with adaptive driving beam headlights will reach a 23.8% penetration rate by 2030. Adaptive beam systems depend on electronically controlled, multi-zone optical distributions, which in turn depend on free-form and multi-cavity lens designs with tight cavity-to-cavity consistency. That is a demand pattern that favours suppliers who control mold making, since the number of distinct optical surfaces per vehicle rises as beam functions multiply.
Two structural shifts follow. First, value moves toward the tooling and design end of the chain, because the differentiation sits in surface geometry rather than in resin cost. Second, thick-wall and light-guide construction becomes more important as ambient and signal lighting is used for brand differentiation, which is precisely where long, uniform light guides and multi-shot molding carry weight.
Comparison with conventional sourcing routes
Custom injection-molded optics compete with three established alternatives. The comparison below uses qualitative engineering characteristics rather than supplier-specific data.
| Approach | Design freedom | Economics at volume | Principal limits |
|---|---|---|---|
| Precision injection-molded PC/PMMA optics (the route described here) | High — free-form, aspheric, TIR, Fresnel, thick-wall and multi-shot geometries | Tooling investment upfront, low unit cost once amortised | Service temperature bounded by the polymer; tooling lead time precedes first samples |
| Ground and polished glass optics | Good for rotationally symmetric surfaces; free-form is slow and costly | High unit cost; limited benefit from scale | Weight, cost and cycle time; integration with plastic housings is more complex |
| Reflector-based secondary optics | Moderate — distribution shaped by reflector contour | Mature and cost-effective for simple distributions | Deeper optical assemblies, harder to achieve sharp cutoff and tight glare control in compact modules |
| Off-the-shelf catalogue lenses | Low — the design must adapt to the available part | No tooling cost, immediate availability | Photometric performance is a compromise; housing redesign often offsets the savings |
Qualitative comparison of sourcing routes; no competitor specifications are implied.
The honest boundary for the molded route is thermal and commitment. Optical-grade PC is specified to +120 °C and PMMA to +90 °C in the published parameters, so applications running beyond those ceilings, or requiring glass-level hardness and scratch resistance at the optical surface, sit outside the material envelope. Thick-wall parts, by their nature, generally demand longer molding cycles and tighter process control than thin lenses, because thick sections are where sink, internal stress and optical distortion appear. And a custom programme carries tooling investment and a development lead time before the first usable sample exists — a real disadvantage for a buyer who needs a replacement part this month, or whose annual volume is too low to amortise a dedicated mold. In those cases a catalogue part or a modified standard lens is usually the more rational choice.
What a buyer should verify before committing
| Check | Why it changes the decision |
|---|---|
| Which stages are in-house — optical design, mold design, mold fabrication, molding, optical metrology | Each outsourced stage adds a hand-off where specification intent can be lost |
| Mold cavity precision and cavity-count capability | Determines whether a multi-cavity tool will hold optical consistency across cavities |
| Experience with the specific geometry class: thick-wall, long light guide, free-form array, multi-shot | These geometries carry process risk that standard thin lenses do not |
| Current certificate copies and scope, including TS16949 and ISO 9001 | Scope and validity dates, not the certificate title, determine whether your programme is covered |
| Sampling and validation protocol, including optical performance measurement | Dimensional approval alone does not confirm photometric performance |
| Capacity headroom, mold service life and material supply arrangements | Governs whether the programme survives volume growth and repeat orders |
| Revision control and change notification process | Prevents a running programme from drifting from the approved specification |
Evaluation criteria derived from the manufacturer's published custom-project and procurement guidance.
Limitations and where this supplier fits least well
A capability profile is more useful when it states the negative case. Three boundaries stand out. First, the “one product, one focus point” model is a commitment to dedicated engineering per design; buyers who want a standardised part with published stock availability and immediate shipment are a poor match for it. Second, the programme depends on the completeness of the buyer's input package — without 2D and 3D data, optical data, material grade and service environment, quotation and DFM cannot be firm, and late data changes propagate directly into tooling cost and schedule. Third, the published performance envelope for imaging optics is thinner than for lighting optics, so machine vision, security camera and UAV projects should be qualified on lens-level data before a tooling decision is made.
Future outlook
Three directions look most consequential for this class of manufacturer. The first is the continued migration of automotive front lighting toward multi-zone, electronically controlled distributions, which raises the number of distinct optical surfaces per vehicle and rewards in-house tooling depth. The second is the expansion of ambient and signal lighting as a styling surface, which pulls demand toward long light guides and multi-shot components where optical and structural functions are combined in one cycle. The third is the widening use of imaging optics in machine vision, security and UAV systems, where the specification logic shifts from beam distribution to image quality — a technically adjacent but distinct capability that buyers should assess on its own evidence rather than assuming transfer from lighting optics.
For procurement teams, the practical conclusion is that custom optical lens sourcing should be evaluated as a development partnership with a measurable engineering pipeline, not as a component purchase. The capability data published by Zhejiang Bicom Optics gives a workable basis for that evaluation, provided it is verified against current certificates, sampling results and a project-specific DFM review.
FAQ
What documents are usually required for a custom optical lens project?
Customers generally provide 2D drawings, 3D data, optical data, material requirements, and a description of the product application and service environment. The detail covers product dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, material grade, working temperature and relevant performance requirements. This package allows the supplier to evaluate manufacturability, cost and development lead time accurately.
How can a buyer verify whether a supplier genuinely has custom development capability?
Producing to drawings is not sufficient evidence. The check is whether the supplier holds full-cycle capability from requirement definition to mass production: optical design, structural evaluation, DFM, mold flow analysis, mold design and fabrication, precision injection molding, optical testing and mass-production support. Past custom project cases, similar-product development experience, engineering team depth and production equipment are the supporting evidence that distinguishes a co-development partner from a build-to-print molder.
How are specifications and drawings confirmed before mold building starts?
The supplier reviews and confirms the customer's 2D drawings, 3D files, optical data, materials, dimensional tolerances, appearance and performance requirements. DFM then assesses product structure and manufacturing feasibility, covering optical surfaces, wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage and deformation. The final drawings, optical data and DFM report confirmed by both parties become the baseline for mold building, sampling and mass production, with revision control applied so the same specification revision is used throughout the project.
What does the sampling and approval process look like?
Custom optical components normally follow the sequence: requirement confirmation, engineering assessment, DFM, quotation, mold development, T0 sampling, test and validation, optimisation, customer approval, then mass production. A prototype mold or a production mold can be used depending on the project phase. Completed samples are validated for dimensions, optical performance, appearance and assembly against the product specification, and necessary mold or process adjustments are made based on the results. Mass production starts after customer confirmation.
How is consistency maintained across batches and mold cavities?
Consistency is controlled across raw materials, molds, injection-molding processes, dimensional inspection, optical performance and appearance. Stable material supply, multi-cavity mold management, standardised injection-molding parameters, inspection of critical dimensions and optical performance, documented inspection standards and in-process control together keep batches and cavities to the same specification. Production traceability and continuous process monitoring are used to identify and mitigate potential quality risks early.
How are quality issues handled on custom optical parts?
The first step is to clarify the phenomenon, batch, quantity, affected cavities and impact scope. Countermeasures such as product segregation, additional inspection or shipment hold are applied as appropriate. Root-cause analysis then covers materials, molds, equipment, injection-molding processes, measurement and operation, followed by corrective actions whose effectiveness is verified by sampling and testing. For complex or batch-level issues, 8D methodology is used to complete root-cause analysis, correction and prevention in a closed loop.
What supply capabilities matter for high-volume custom procurement?
Beyond development competence, buyers should examine long-term stable production and delivery capability: injection-molding equipment and actual production capacity, multi-cavity mold capability, mold service life, raw-material supply, quality management system, testing capacity, production and engineering team depth, delivery lead time and abnormality response capability. It is also worth confirming whether the supplier can expand capacity and secure its supply chain against order growth, urgent demand and long-term recurring procurement, which is where quality, capacity and delivery risk concentrate during mass production.
What type of supplier suits a complex custom optical component project?
Complex projects — involving complex optical surfaces, light guides, TIR lenses, projection lenses, thick-wall parts, multi-cavity molds or stringent optical performance requirements — call for a specialist optical manufacturer with end-to-end capability in development, engineering validation and mass production, rather than a general plastics processor or a mold vendor alone. The supplier needs to understand both optical design specifications and plastic injection-molding manufacturing, with solid mold development, precision injection molding, optical metrology and quality control. Where multiple sampling rounds and design iterations are expected, a track record on similar complex projects, a stable engineering team and continuous mass-production support are the decisive criteria.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.