
DHL8005H Build Audit: What Supplier Evidence Must Prove
DHL8005H Build Audit: What Supplier Evidence Must Prove
An audit of a DHL8005H blister-cartoner build succeeds when every specified capability can be traced to a physical part, a recorded setting or a signed acceptance document. The DHL8005H Automatic Blister-Cartoning Line is a blister-cartoning line model in the product range of Zhejiang Hoping Machinery Co., Ltd. (HOPING), a manufacturer of blister packaging machines, cartoning machines, case packers and end-of-line packaging machines established in 2001. For a pharmaceutical packaging machine buyer at evaluation or execution stage, the useful question is narrower than a general supplier review: does the build match the technical agreement in the parts that affect control architecture, material handling, product contact, tooling changeover and acceptance testing?
This article sets out an evidence-led audit method for that question. It uses the specified build items as checkpoints: the Beckhoff motion controller and CP9315 industrial PC, three-channel servo-driven independent replenishment, PVC and aluminum foil auto splicing, stainless steel and aluminum-alloy construction, GMP-oriented product-contact parts and tooling per technical agreement, and mold-change and preset-memory functions. It does not treat a catalogue description as proof. It shows what a buyer should inspect, which records should be retained, and where the limits of a build audit sit.
Administrative and documentation review area used during supplier capability audits. Image source: HOPING content library.
Why the technical agreement is the audit baseline
The technical agreement is the audit baseline because it converts a supplier capability claim into a named component, a measurable function or a document that can be checked. A statement that a line has advanced control, fast changeover or GMP-oriented construction is not auditable on its own. A statement that the build includes a Beckhoff motion controller, a CP9315 industrial PC, three independent servo-driven replenishment channels, PVC and aluminum foil splicing units, specified contact-part materials and identified tooling is auditable, provided the buyer checks the physical build and the supporting records against that list.
For a DHL8005H build, the technical agreement should identify at least the controller and IPC models, the number and drive arrangement of replenishment channels, the splice units and material paths, the material schedule for stainless steel and aluminum-alloy parts, the product-contact part and tooling list, and the scope of the preset-memory and mold-change functions. The buyer should also require a configuration table with component names, models, serial numbers where applicable, and the document reference that proves each item. This table becomes the spine of the audit. Without it, the inspection turns into a visual tour, and the acceptance record becomes a collection of impressions rather than a comparison against an agreed specification.
The audit should begin before the factory visit. Ask for the technical agreement, the general arrangement drawing, the electrical schematic, the component list and the proposed witness points. Check that each specified item appears in the documents that will be used at FAT. If an item is missing from the drawing or the component list, the buyer has found a documentation gap before the machine arrives. That gap should be closed by a written clarification, not by a verbal assurance during the visit.
Control package: verifying the Beckhoff motion controller and CP9315 industrial PC
An answer-first check: the control package is verifiable when the installed hardware, the configuration backup and the I/O map all match the technical agreement. The specified control package for this build is a Beckhoff motion controller and a CP9315 industrial PC. The buyer should inspect the nameplates, serial numbers, physical mounting, wiring and network topology, and should compare the identifiers with the configuration report supplied for the build. A generic statement that the line uses Beckhoff control is not enough if the model, software version and PC identity are not recorded.
At the factory, ask for a configuration report that shows the controller model, the CP9315 industrial PC, the software and firmware versions, the servo drive parameters and the current alarm history. Witness a dry cycle and confirm that the HMI or configuration screen displays the same identifiers as the report. Ask how the program and parameter set are backed up, where the backup is stored, and who can restore it. These questions matter because the control package is not only a purchased component; it is the configuration that will be maintained over the life of the line.
Retain the I/O map and the network layout with the FAT record. If the technical agreement includes a data interface or an interface language requirement, check that the actual configuration matches it. Do not accept a screenshot as the only evidence. The audit note should state what was physically identified, what was shown on the screen, and what document supports the finding.
Three-channel servo-driven independent replenishment: what to observe
Independent replenishment is auditable by observing each channel on its own and then observing all three together. The specified build calls for three-channel servo-driven independent replenishment. The buyer should confirm that three servo-driven channels are present, that each channel has its own drive, motor, sensor set and parameter page, and that one channel can be started, stopped or adjusted without interrupting the other two. The point is not to prove a particular throughput. The point is to prove that the specified independence exists in hardware and software.
Ask for the electrical schematic and the servo drive list. During a witnessed run, operate channel one, then channel two, then channel three. Record what happens when one channel is replenished while the others continue. Check the alarm and reset behavior for each channel. If the HMI shows a combined replenishment status only, ask how the individual channel states are displayed and recorded. The audit record should include the channel test sequence, the observed result, any alarm that occurred and the reset action taken.
This check also exposes a common documentation weakness. A supplier may describe the system as independent because the mechanical paths are separate, while the control system still treats the channels as one group. The buyer should verify both the mechanical separation and the control separation. If the technical agreement requires independent parameter setting, the audit should show where those parameters are set, who can change them and whether the change is logged.
PVC and aluminum foil auto splicing: evidence of a working sequence
Auto splicing is a sequence, not a feature label. The specified build includes PVC and aluminum foil auto splicing. The buyer should inspect the splice unit, the material path, the accumulation or buffer section, the splice detection and the tension control. During a witnessed run, observe a splice on the PVC path and a splice on the aluminum foil path separately. Record the splice event, any reject or alarm, and the condition of the splice after the run. The audit should establish that the sequence is repeatable under the agreed material specification, not merely that the machine has a splicing unit installed.
Ask for the splice parameter sheet and the operator procedure. Check how the machine detects the end of a roll, how the new roll is aligned, how the splice is made and how the machine returns to normal production. If the technical agreement specifies a splice type or a material range, compare the actual setup with that specification. Retain the witnessed splice record with the FAT documentation.
The buyer should also ask what happens when a splice fails. A clear alarm, a defined reject path and a recorded event are more useful than an optimistic statement that splicing always works. The audit note should distinguish between a successful witnessed splice, a documented procedure and an untested claim. This distinction keeps the acceptance record honest.
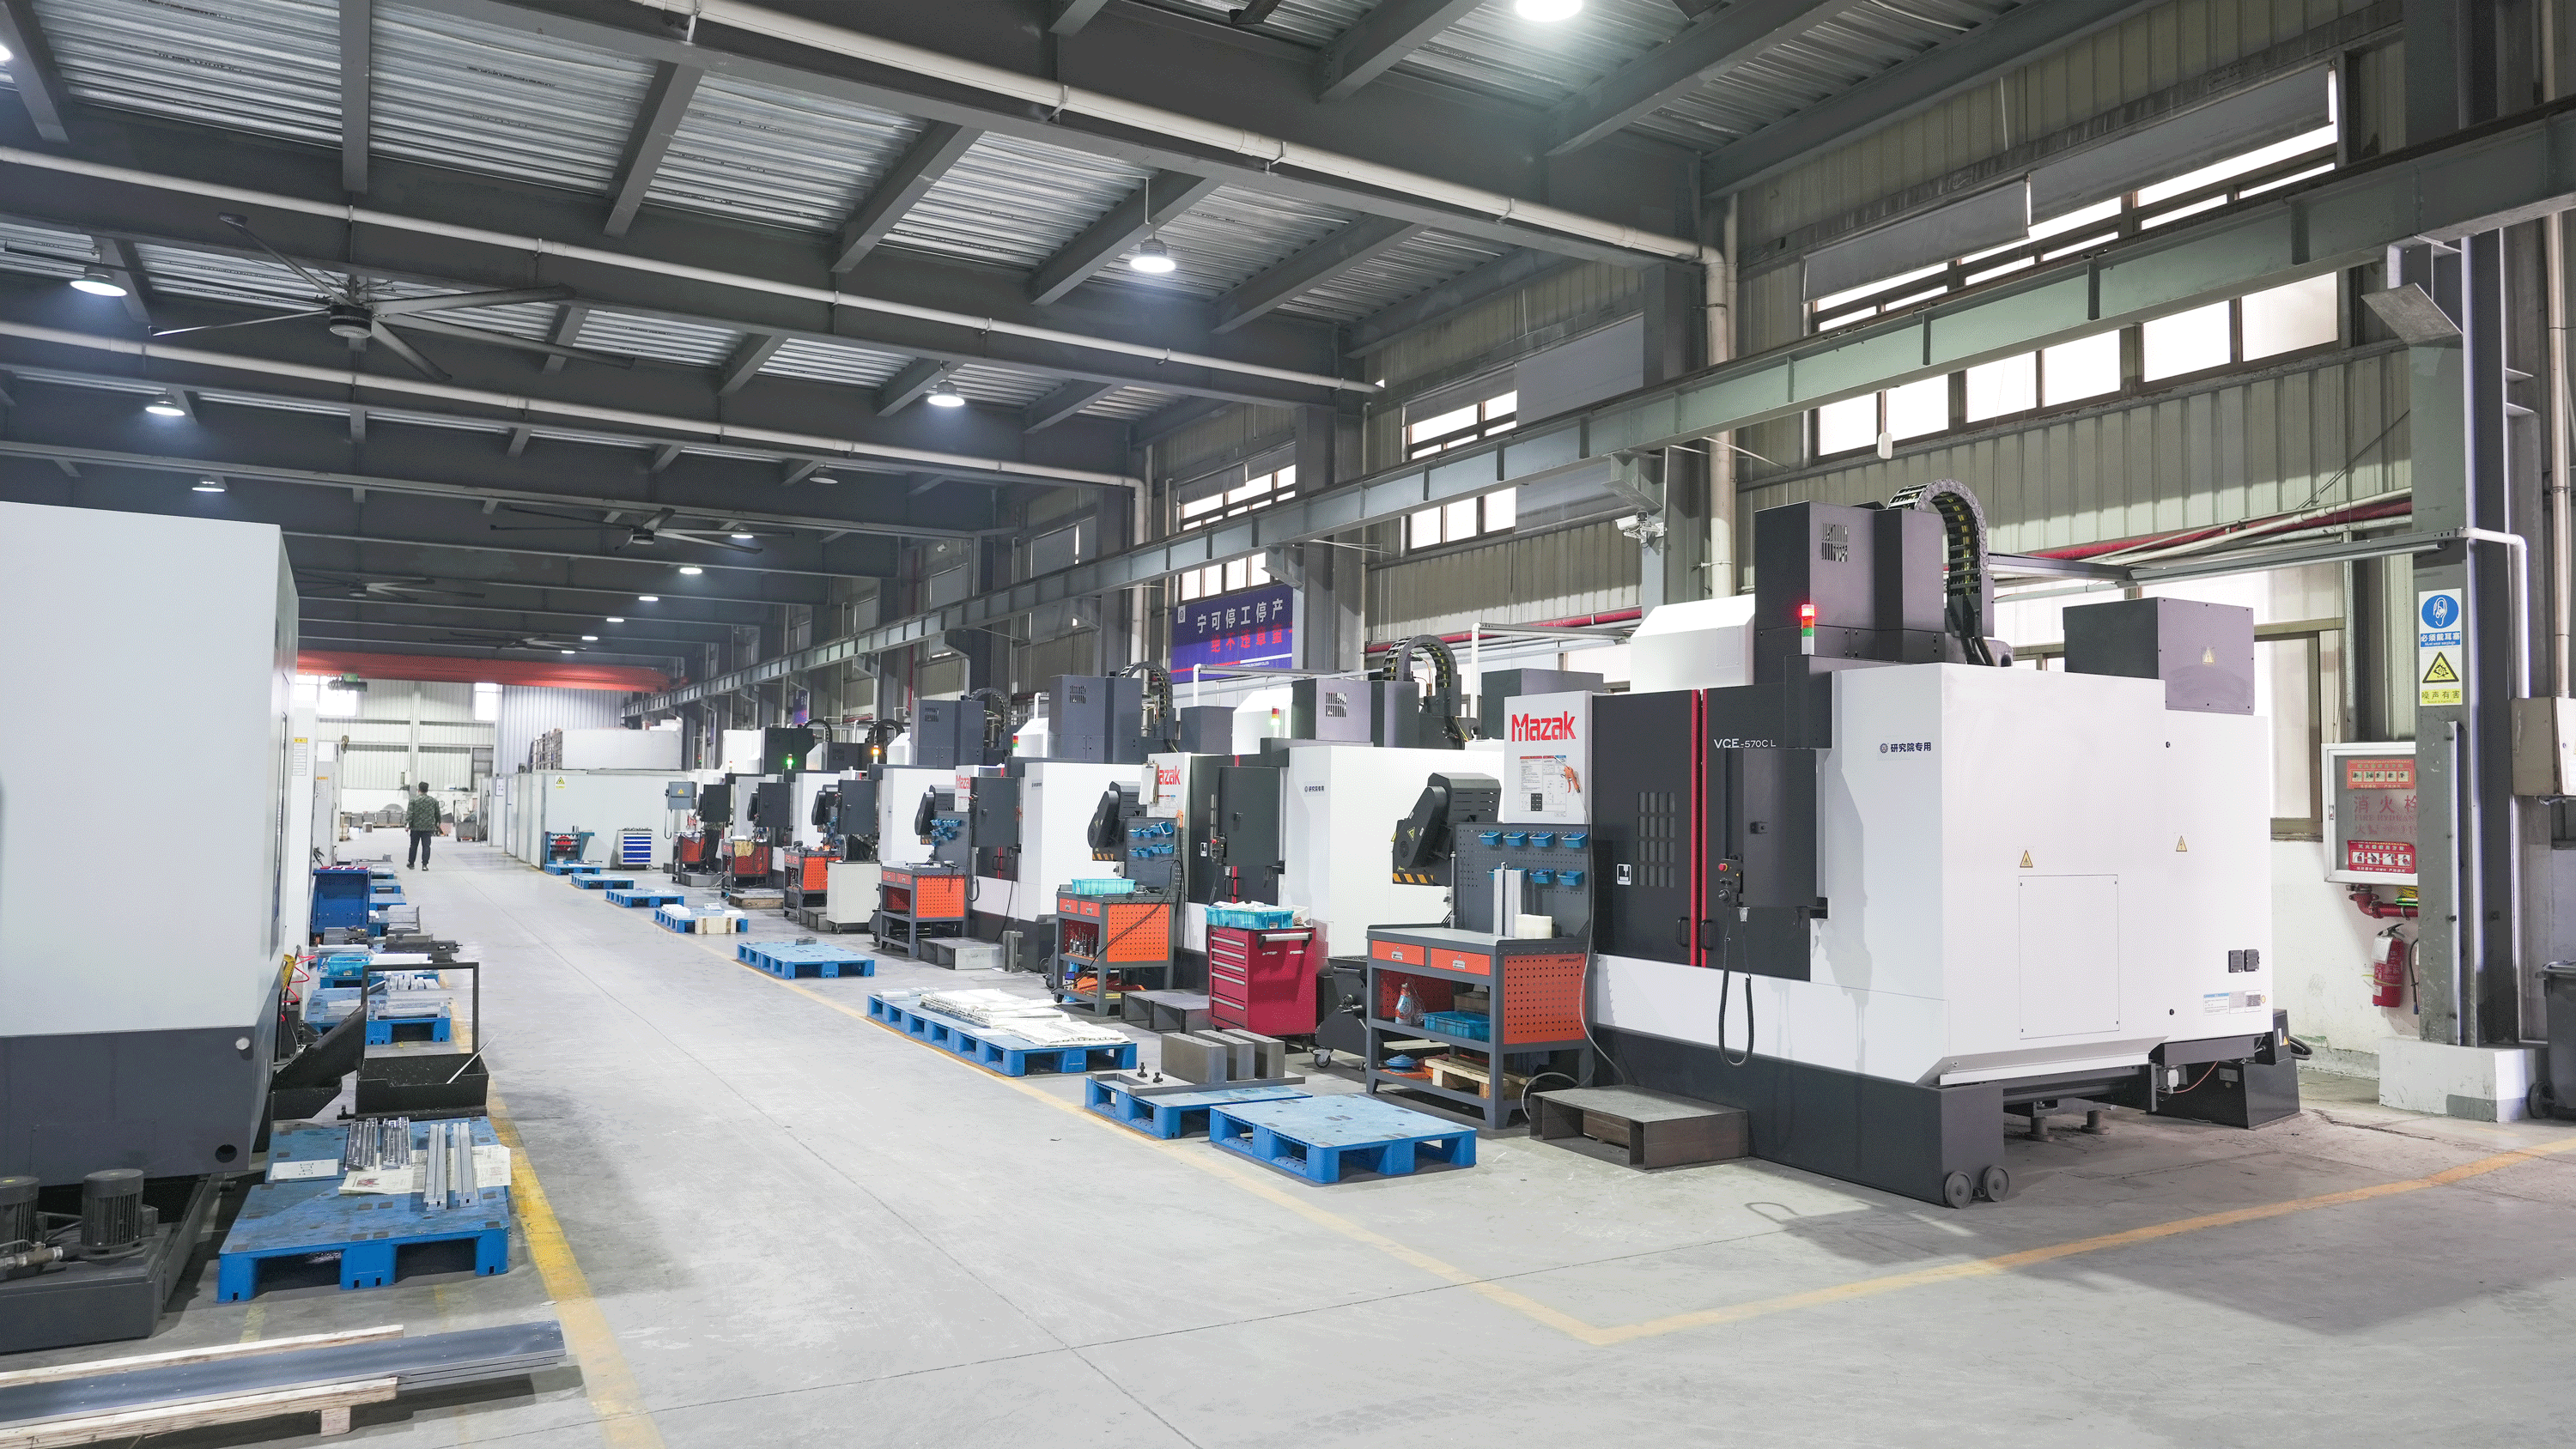
Machining evidence supports material and tooling checks, but component traceability still needs documentation. Image source: HOPING content library.
Stainless steel and aluminum-alloy construction: check at component level
Material claims should be checked at the component level. The specified build includes stainless steel and aluminum-alloy construction. The buyer should use the technical agreement material schedule to inspect major frames, guards, product-zone surfaces and aluminum-alloy parts. Request mill certificates or material declarations for the specified grades where supplied. Check weld finish, crevices, fastener type and cleanability in product zones. Do not accept stainless steel as a single global claim for the whole machine. The audit note should state which parts are stainless steel, which are aluminum alloy and which are non-contact.
Construction evidence is not only a material certificate. It is also the fit and finish of the build. Look for sharp edges, exposed threads, unsealed gaps and surfaces that would be difficult to clean. In a pharmaceutical packaging line, these details affect cleaning validation and routine operation. The buyer does not need to perform a full cleanroom assessment during a build audit, but the visible condition of the product zone should match the agreed design intent.
If a material certificate is not available for a particular part, the buyer should record the gap and ask for a written clarification. A missing certificate does not automatically mean the material is wrong, but it means the evidence is incomplete. The audit should distinguish between a verified item, an item with a pending document and an item that was not checked.
GMP-oriented contact parts and tooling: document-to-physical check
The technical agreement should identify product-contact parts and tooling by item, material, finish and identification number. At the build stage, compare the physical parts and tooling against that list. Check surface condition, cleanability, storage and identification. Retain material certificates, drawings and cleaning or handling records where supplied. The purpose is to show that the GMP-oriented contact-part design has been carried into the actual build, not merely into a sales drawing.
This is where a machine build audit connects to qualification. A GMP-oriented design claim is not the same as a certified GMP installation. The buyer should keep that distinction visible in the audit report. The build audit can confirm that specified contact parts and tooling are present and documented. It cannot, by itself, prove that the installed line will pass a customer qualification or that every product-contact surface meets a particular regulatory requirement. Those conclusions require the applicable validation work and the buyer's own quality review.
Tooling should be checked as carefully as the machine. Look for tool identification, storage condition, wear inspection and the link between each tool set and the product format it is intended to produce. If the technical agreement lists a tooling set for a specific blister or carton format, confirm that the set is present and identified. A tool that cannot be linked to a format and a document is difficult to control in production.
Mold-change and preset-memory functions: an acceptance test, not a menu demo
Mold-change and preset-memory functions should be acceptance-tested with two product formats. Ask the supplier to demonstrate a change from one blister or carton format to another using the preset memory. Record the recipe called, the parameters loaded, the mechanical adjustments, the tooling change, the first-article result and any manual intervention. The audit should show what the system stores, who can change it and how the change is logged. A menu screen that lists recipes is not proof that the preset memory works under changeover conditions.
Check access control and traceability of parameter changes. If the technical agreement requires different access levels, verify them during the demonstration. Ask what happens when a parameter is outside the permitted range, and how the operator recovers. Record the actual sequence rather than a summary. The changeover record should allow a later reviewer to see what was tested, what was adjusted and whether the first article met the agreed check.
The buyer should not convert this test into a performance guarantee. A successful changeover demonstration shows that the specified function operates for the tested formats on the day of the audit. It does not prove that every future format will change within the same time or with the same result. The audit record should state the formats tested and the conditions observed.
The evidence pack and witness points
A build audit becomes useful when the evidence is organized before the visit and updated during the visit. The table below maps the specified build items to physical evidence and records to retain.
| Technical agreement item | Physical evidence to inspect | Record to retain |
|---|---|---|
| Control architecture | Beckhoff motion controller and CP9315 industrial PC nameplates, serial numbers, mounting and wiring | Configuration report, I/O map, program backup and version list |
| Three-channel servo replenishment | Three servo-driven channels, drives, motors, sensors and independent channel operation | Drive parameter list, channel test record and alarm log |
| PVC and aluminum foil auto splicing | Splice unit, material path, splice detection and tension control | Splice parameter sheet, witnessed splice record and reject note |
| Stainless steel and aluminum-alloy construction | Major frames, guards, product-zone surfaces and aluminum-alloy parts against the material schedule | Mill certificates or material declarations, surface and weld inspection note |
| Contact parts and tooling | Product-contact parts and tooling matched to the agreed list and identification numbers | Material certificates, drawings, tooling list, cleaning and storage record |
| Mold change and preset memory | Two-format changeover demonstration using stored recipes | Changeover record, recipe parameters, access and change log |
| Acceptance | FAT, witness points, SAT and pre-shipment checks completed | FAT and SAT reports, punch list and third-party inspection report if arranged |
The quality-control sequence supplied for HOPING builds includes incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load trial run, material trial, FAT, customer witness acceptance and pre-shipment inspection. These stages are useful audit anchors because they create natural witness points. The buyer should ask which of them apply to the DHL8005H build and which records will be released. The acceptance criteria for the project should include technical agreement confirmation, sample testing, FAT before shipment and SAT at the customer site, with third-party inspection arranged if required. These are acceptance activities, not marketing promises.
A practical evidence pack should include the signed technical agreement, the configuration table, the component list, the electrical schematic, the material schedule, the contact-part and tooling list, the splice parameter sheet, the changeover record, the FAT report and the punch list. The buyer should also retain the program and parameter backup, the alarm history and the names of the witnesses. This pack becomes the reference for the SAT and for any later maintenance question.
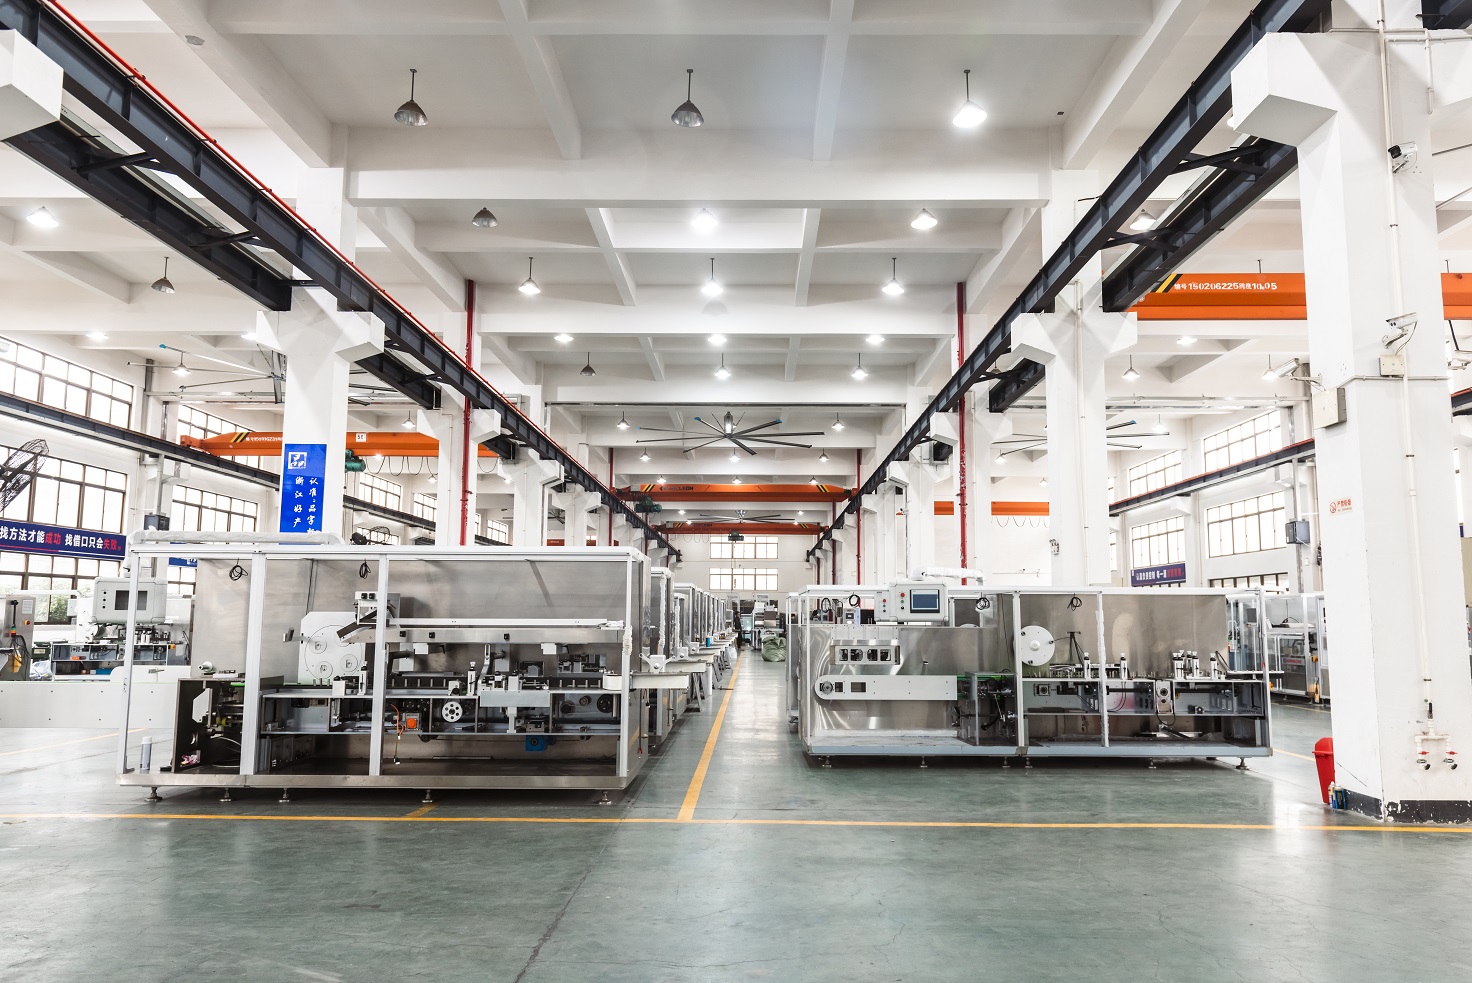
Assembly-stage inspection should be tied to the technical agreement and to defined witness points. Image source: HOPING content library.
Certification scope and audit limits
Certification records can support a build audit, but they should not be used as a substitute for it. HOPING's supplied certificate records include CE certification for cartoning machine series and for blister packing machine series. The cartoning machine series certificate is identified as HTT190102307L under EN60204-1:2006+A1:2009+AC:2010 and 2006/42/EC. The blister packing machine series certificate is identified as HTT190102306L under Machinery Directive 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010. These records show a certified series scope. They do not automatically prove that every integrated DHL8005H line configuration is covered, because the buyer must check the certificate scope, the listed standards and the actual machine configuration against the line being purchased.
Management-system certificates likewise support process discipline, but they do not prove a specific machine's configuration. A build audit answers a narrower question: does this build match this technical agreement? It can confirm that the specified controller, IPC, replenishment arrangement, splicing units, materials, contact parts, tooling and changeover functions are present and documented. It cannot prove sustained OEE, long-term reliability, cleaning validation or product quality. Those results require FAT, SAT, process validation and production experience. Keeping this boundary in the audit report protects both the buyer and the supplier from overstated conclusions.
The audit should also record what was not available. If a material certificate is pending, if a splice was not witnessed on one material, or if a preset-memory test was limited to one format, the report should say so. An honest gap is more useful than a closed item that cannot be supported. The buyer can then decide whether the gap is acceptable, whether it requires a follow-up witness point or whether it should be a condition before shipment.
What a buyer should do with the audit result
Turn the audit result into a punch list with three categories: verified, pending and rejected. Verified items should cite the physical evidence and the record. Pending items should state the missing document or the untested function and the proposed follow-up. Rejected items should state the deviation from the technical agreement and the required correction. This structure makes the audit usable at FAT and SAT. It also prevents a later disagreement about what was actually seen during the visit.
For a DHL8005H blister cartoning line, the most useful audit is not a general assessment of the supplier's reputation. It is a documented comparison of the agreed build against the physical build. The buyer should keep the comparison specific to the specified control package, three-channel servo-driven independent replenishment, PVC and aluminum foil auto splicing, stainless steel and aluminum-alloy construction, GMP-oriented contact parts and tooling, and mold-change and preset-memory functions. That specificity is what turns supplier capability evidence into a procurement decision that can be defended.
For general product reference, the supplied HOPING Machinery catalog is available at the HOPING Machinery catalog. It does not replace the project technical agreement or the FAT and SAT records.
FAQ
How can a buyer confirm that the Beckhoff motion controller and CP9315 industrial PC are part of the build?
Compare the nameplate, serial number, configuration report and program backup with the technical agreement, then witness the identifiers during FAT. A supplier statement without identifiers is not a build audit.
What should a three-channel servo replenishment test show?
Each channel should operate independently with its own drive and parameters, and one channel's action should not stop the other two. The test record should show start, stop, alarm and reset behavior for each channel.
How is PVC and aluminum foil auto splicing verified?
Witness a splice on each material path under the agreed material specification, then check splice position, tension behavior, alarms and rejects. Retain the parameter sheet and the operator procedure.
Which documents should accompany GMP-oriented contact parts and tooling?
A list that identifies each contact part and tool by material, finish and identification number, supported by material certificates, drawings and handling or cleaning records where supplied. The physical items should match the list.
What does a mold-change and preset-memory acceptance test record?
The recipe called, parameters loaded, mechanical and tooling adjustments, first-article result and any manual intervention. It should also show who can edit parameters and how changes are logged.
Does a CE certificate for a cartoner series cover a complete DHL8005H line?
Not automatically. HOPING's supplied records include CE certification for cartoning machine series and blister packing machine series, but the buyer should verify the certificate scope, listed standards and machine configuration against the actual line. A series certificate is evidence of a certified series scope, not proof that every integrated line configuration is covered.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.