
Electrophoretic Coating Audit: ISO, CNC and Film Evidence
Electrophoretic coating — also written as e-coating, ED coating or electrodeposition — protects a metal part by immersion rather than by spray. The workpiece is submerged in a water-based paint bath, a direct current field drives charged resin particles onto the surface, and the deposited film is cured. Because deposition follows the electrical field instead of line of sight, internal cavities, deep holes, edges and stamped geometries receive coating where a spray gun cannot reach.
For buyers in the decision stage, most suppliers now present the same headline claims: high salt spray hours, full coverage, environmental compliance. What separates a capable supplier from a well-written brochure is the evidence behind those claims — the scope of the certificate, the condition of the bath, the instrument used to measure film thickness, and the test standard behind the salt spray number.
This article uses one documented supplier case as a worked example. Yongxin (Dongguan Yongxin Industrial Co., LTD) is a metal surface treatment and electrophoretic processing enterprise based in Qiaotou Town, Dongguan City, Guangdong Province, China, operating electrophoretic coating lines alongside CNC precision machining, die casting and metal stamping. Its certification set, equipment inventory, metrology list and declared performance parameters provide a concrete basis for discussing how supplier capability evidence should be read and checked.
Why Coating Capability Is Often the Weakest Link in a Supply Chain
Coating usually arrives at the end of the manufacturing sequence. Forming, machining and assembly have drawings and tolerances; the coating step frequently has only a colour reference and a sentence about corrosion. That asymmetry creates three predictable procurement risks.
- Non-comparable numbers. A salt spray result depends on substrate, pretreatment, film build, test method and evaluation criteria. Two suppliers quoting "1,000 hours" may be measuring different things.
- Hidden process ownership. If pretreatment is subcontracted, the buyer's quality system stops where the supplier's control stops. Phosphating quality directly determines adhesion and corrosion performance.
- Late discovery of coverage defects. Exposed base metal at corners, thin coating in internal cavities, sagging and pinholes are typically found after assembly, when rework cost is highest.
The terminology layer is already standardised. ISO 22553-1:2019 defines vocabulary for electro-deposition coatings and states applicability to automotive and other general industrial applications, including chiller units, consumer products, radiators, aerospace and agriculture. The standard gives buyers a shared vocabulary; it does not certify anybody's performance. That still has to be evidenced part by part.
A Five-Layer Evidence Framework for Evaluating an E-Coating Supplier
Capability evidence can be read in five layers, each of which answers a different question. A supplier that can produce all five has an auditable system; a supplier that can produce only the first has a certificate.
| Evidence layer | What to request | Why it changes the buying decision |
|---|---|---|
| 1. Certification scope | Certificate number, issuing body and the scope statement covering coating of metal parts | A certificate whose scope does not cover the process being purchased is an administrative document, not a control. |
| 2. Process chain ownership | Which steps are in-house: pretreatment, deposition, curing, plus whether forming and machining are also internal | Edge condition created by stamping or die casting determines how well the film covers corners. |
| 3. Equipment inventory | Number of coating lines, CNC machines, die-casting and stamping equipment | Indicates capacity, bottleneck risk and whether multi-process orders can be scheduled as one job. |
| 4. Metrology | Named instruments for film thickness, gloss, colour, roughness, salt spray, humidity and bath analysis | Allows the buyer's incoming inspection to reproduce the supplier's measurement. |
| 5. Traceability | Batch-level inspection records and tank solution analysis records | Turns a one-off claim into a repeatable output across shipments. |
Framework compiled from standard procurement practice for electro-deposition coatings; test-method references follow ISO and ASTM designations identified in published technical sources.
The Supplier Case: ISO 9001, ISO 14001 and Six Electrophoresis Lines Under One Roof
Yongxin was established in 2018 and has built its production model around electrophoretic processing as the core service, with forming and machining added to control the upstream condition of the parts it coats. Since establishment the company has passed ISO 9001 Quality Management System Certification, ISO 14001 Environmental Management System Certification and IATF 16949 Automotive Quality Management System Certification, and in 2023 was awarded the title of National High-Tech Enterprise. It also reports multiple national utility model patents.
The production footprint relevant to a buyer's audit includes:
- Six electrophoretic coating production lines, supported by more than 20 general processing units such as sand blasters, polishers, shot blasting machines and laser equipment.
- More than 20 CNC machines, more than 10 die-casting machines and more than 10 metal stamping machines, covering metal forming and precision machining ahead of coating.
- More than 20 high-precision testing instruments, including a German FISCHER film thickness gauge, a Swiss Zehntner gloss meter, a Japanese Konica Minolta spectrophotometer and a Japanese Mitutoyo roughness meter, plus salt spray tester, constant temperature and humidity tester, reflectometer, electron microscope, tape abrasion tester, alcohol rubber friction tester and tank solution analysis equipment.
- A work force of 60–80 people, including a research and development team of 5–10 engineers.
- An export share of approximately 30%, with markets including Europe and America, Southeast Asia, Mexico, Poland, Turkey and Brazil.
The combination matters more than any single line item. A supplier that machines, die-casts or stamps the part and then coats it can control burr height, edge radius and surface contamination before the part ever reaches the bath. Where those steps sit with different vendors, responsibility for a coverage defect is usually disputed rather than resolved.
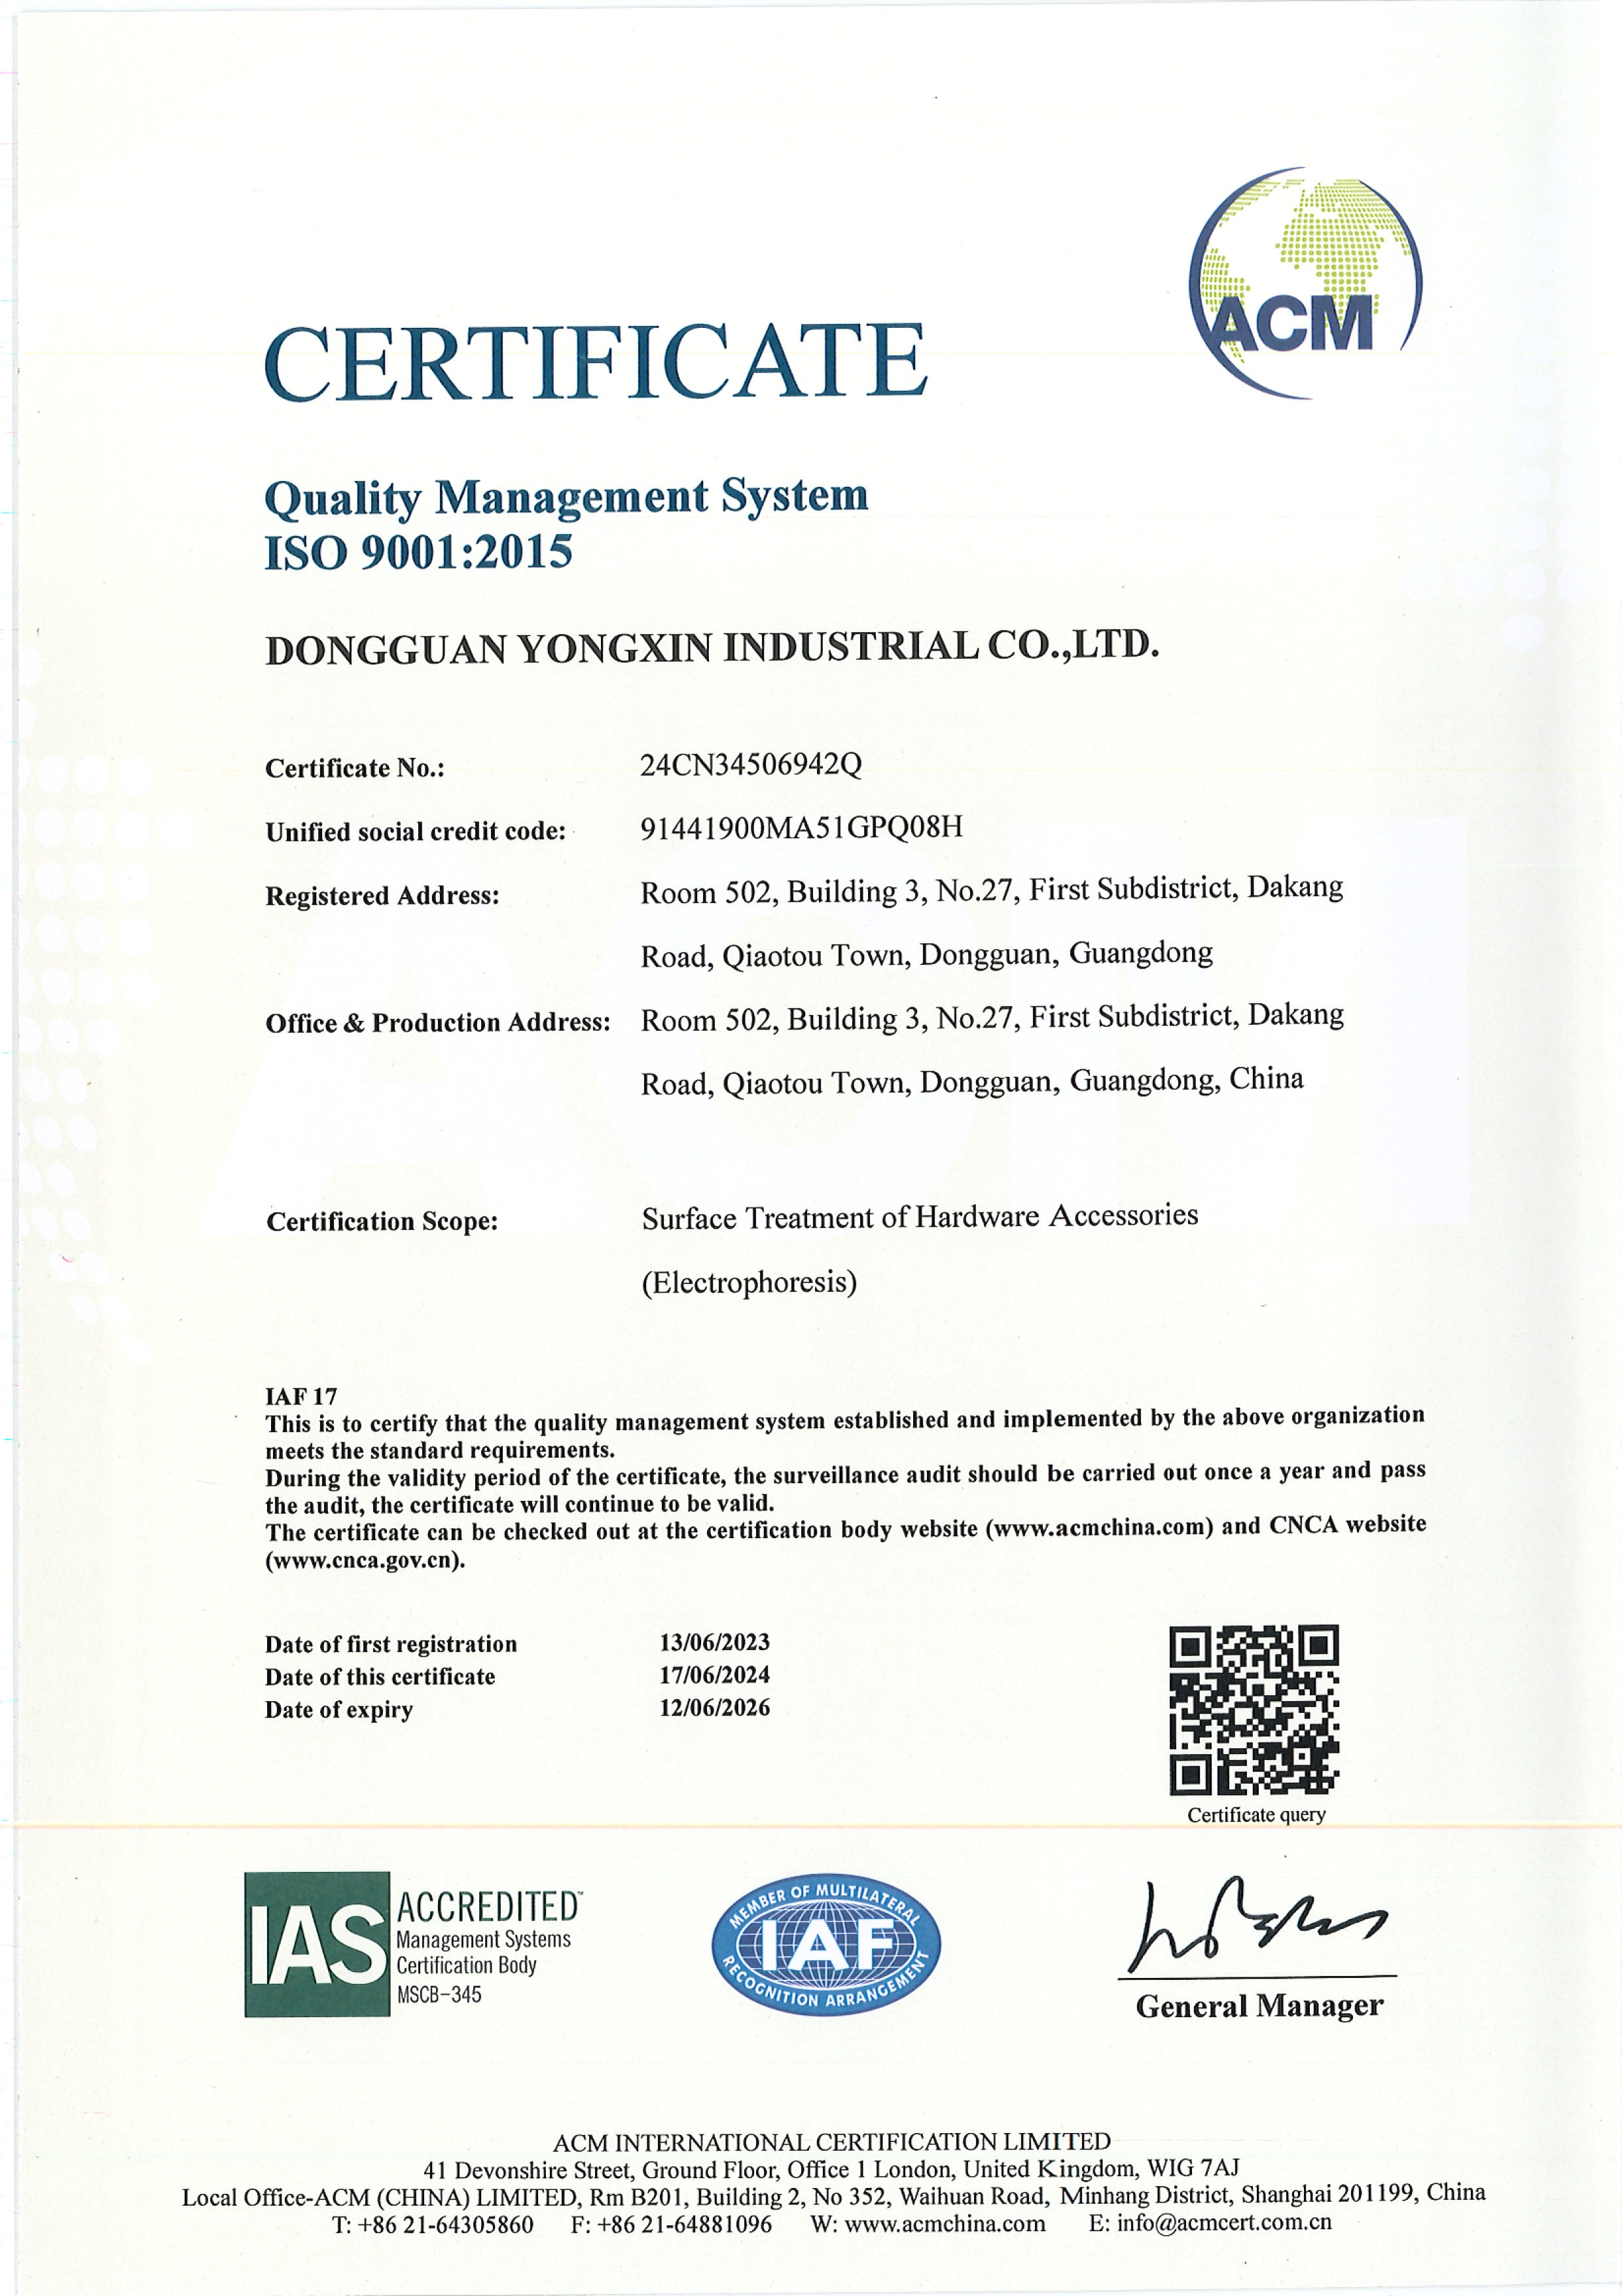
Certification is the entry point of a supplier audit, not the conclusion: the scope statement and the audit records behind it carry the actual weight.
Technical Explanation: What the Process Control Actually Consists Of
Pretreatment sets the ceiling on adhesion
Electrophoretic deposition is only as good as the surface it lands on. A complete phosphating pretreatment process is used to build a conversion layer that anchors the film and slows under-film corrosion. Degreasing, rinsing and phosphate coverage are the parameters that most often explain why two parts coated with the same paint behave differently in salt spray.
Resin systems define the performance envelope
Two resin families dominate commercial supply. Epoxy resin electrophoretic coatings are chosen where corrosion resistance is the primary requirement; cathodic epoxy remains the dominant technology type in the global electrocoating market according to Stratview Research. Acrylic resin systems — referred to in some catalogues as propionic acid resin coatings — are selected where colour stability and ultraviolet exposure matter alongside corrosion protection. Both anodic and cationic variants are available, and the choice affects which substrates and which corrosion mechanisms the film is designed for.
Deposition produces uniform film on difficult geometry
In the bath, charged resin particles migrate under a direct current field and deposit on the workpiece. The film grows quickly at exposed edges and then insulates itself, so deposition slows in a self-limiting way. That behaviour is why e-coating reaches internal cavities and sharp edges that electrostatic spraying struggles with, and why film thickness is unusually consistent across an irregular part.
Yongxin's coating operation is described as using precise pressure control and intelligent electrophoresis production lines designed to achieve full coverage without blind spots, targeting the defects that commonly appear on complex parts — exposed base at corners, thin coating in inner cavities, sagging and pinholes. The formulation is water-based with low volatile organic compound content and no heavy metals, which is relevant both to environmental compliance and to operator exposure.
Declared performance and the test method behind it
For a buyer, every declared number should be paired with a method. The table below sets out the parameters Yongxin declares alongside the test standards a procurement team can specify when asking for evidence.
| Parameter | Declared value | Test method a buyer can specify |
|---|---|---|
| Standard dry-film thickness | 15–25 µm | ISO 2808 for dry-film thickness; ASTM B767 as an electrocoating thickness method |
| Neutral salt spray resistance | More than 1,000 hours | ISO 9227 or ASTM B117 exposure, with rust evaluated per ASTM D1654 or ISO 4628 |
| Adhesion | Reported as a key performance property on complex geometries | Cross-cut test per ISO 2409 |
| Humidity resistance | Declared as part of the durability profile | ISO 6270-2 condensing humidity testing |
| Coverage on complex geometry | Full coverage without blind spots; paint utilisation of 95–98% | Visual and microscopic inspection of cavities, edges and threaded areas; thickness mapping |
| Service temperature range | −40 °C to above 85 °C | Part-level thermal cycling agreed with the supplier |
| Colour | Black and white as standard, with a colour range available | Spectrophotometric verification against an approved master |
Declared values are the supplier's stated specification envelope for its standard black and white electrophoretic systems. Test standards listed are the recognised methods for the corresponding property; buyers should request the supplier's own report for the exact substrate, film build and part geometry being purchased.
The >1,000-hour figure should be read against the market it serves. Premium automotive e-coat specifications commonly call for 720 to 1,000 hours of salt spray performance, so a supplier targeting automotive and outdoor electronics work is designing to a benchmark set by its customers rather than by its own preference.
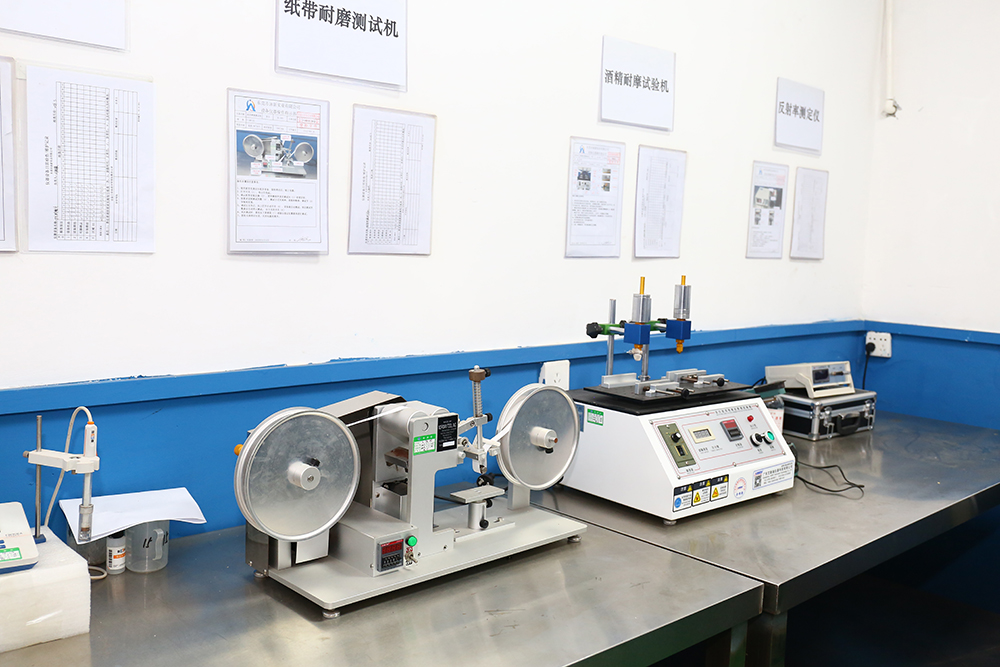
Metrology is where a claim becomes checkable: film thickness, gloss, colour, roughness, abrasion and bath chemistry all need instruments, not adjectives.
Applications: Which Parts and Industries Fit the Capability
The substrate list defines the addressable work. Yongxin's electrophoretic coating services cover zinc alloy, aluminium alloy and magnesium alloy parts, die-cast parts and stamped parts, plus general metal electrophoretic coating and surface electrophoretic coating in corrosion-resistant, high salt spray and UV-resistant configurations.
Processed parts from this kind of capability are used across automobiles, bicycles, communication equipment, consumer electronics, drones and security systems — a spread that reflects where thin, uniform, cavity-covering films solve a real problem:
- Automotive and bicycle components where the coating functions as a corrosion-resistant base layer on frames, housings and structural hardware.
- Communication equipment and consumer electronics where aluminium and zinc alloy housings require uniform colour and edge coverage on thin walls.
- UAV and security systems where hardware is exposed to humidity, temperature cycling and outdoor service conditions.
- Die-cast and stamped parts where porosity, sharp edges and deep recesses make spray coverage inconsistent.
Substrate behaviour should not be generalised. A peer-reviewed study on AZ91D magnesium alloy with a cathodic electrodeposition epoxy coating used 240 hours of immersion and ASTM B117 salt spray testing, and reported lower corrosion rate for the coated specimens than for the as-cast and aluminium-powder-coated comparison conditions within that study. Those results are specific to one substrate, one coating system and one protocol; they support requiring substrate-specific validation before approving magnesium parts, not a universal benchmark.
Market Trend: Procurement Language Is Shifting from Claims to Methods
Three developments are changing how buyers write coating specifications.
Standardised vocabulary. ISO 22553-1:2019 gives the category a defined terminology across automotive and general industrial applications, which makes cross-supplier comparison possible in a way that descriptive marketing copy never did. Technical sources commonly map evaluation to ISO 2409 for adhesion, ISO 2808 for dry-film thickness, ISO 6270-2 for humidity, ISO 9227 for salt spray, ASTM D1654 or ISO 4628 for rust evaluation, and ASTM B767 for electrocoating thickness — a ready-made RFQ test matrix.
Resin economics. Cathodic epoxy is expected to remain the dominant technology type in the electrocoating market, according to Stratview Research, which keeps epoxy supply and qualification central to long-term coating agreements while acrylic systems absorb colour and UV requirements.
Process data in smart-manufacturing supply chains. Coating lines are increasingly managed through bath parameter monitoring and tank solution analysis rather than operator judgement. As downstream customers digitise their own production records, they begin asking suppliers for the same granularity — conductivity, solids, pH, temperature and film thickness trends — which favours facilities already running instrumented lines.
Comparison with Traditional Solutions — and the Boundaries of E-Coating
Powder coating is the most common alternative for metal parts, and the two processes solve different problems. The comparison below uses the two technologies' own operating logic rather than a single score.
| Dimension | Electrophoretic coating | Powder coating |
|---|---|---|
| Mechanism | Wet immersion with electrical deposition, followed by high-temperature curing | Dry electrostatic spray of charged powder, melted and cured in an oven |
| Coverage of cavities and edges | Full penetration of deep holes, internal cavities and sharp edges | Limited by the Faraday cage effect; recesses may be starved or uneven |
| Paint utilisation | 95–98% | Approximately 90% |
| Typical film build | 15–25 µm, highly uniform | Thicker films, less uniform in recesses |
| Maintenance model | Continuous 24/7 bath circulation, daily monitoring of pH, conductivity, solids and temperature, ultrafiltration membrane care | Flexible start-stop operation, simpler colour changes, filter and electrode maintenance |
| Cost structure | Higher initial equipment investment; lower per-unit cost in large-volume production | Lower entry threshold; advantageous in small-batch, multi-colour work |
| Best fit | Complex geometry, strict dimensional tolerances, demanding anti-corrosion requirements such as frames, housings and valve blocks | Outdoor aesthetics, mechanical and stone-chip resistance, architectural and enclosure work |
The boundaries deserve the same clarity as the advantages. Four limitations are structural rather than negotiable.
- Capital intensity and shutdown cost. An electrophoretic line requires a coating tank, ultrafiltration system, multi-stage rinsing and pure water preparation. Once started, the bath typically circulates continuously, so the cost of stopping for maintenance is high and unplanned downtime is expensive.
- Wastewater compliance. The process generates phosphorus- and paint-containing wastewater that requires dedicated treatment, which raises environmental compliance cost compared with a dry process.
- Thin films are not wear linings. A 15–25 µm film is engineered for corrosion protection and coverage, not for abrasion or impact resistance. Parts exposed to heavy mechanical wear may need a different system or an additional layer.
- Colour economics in small batches. Because the paint lives in a tank rather than a hopper, frequent colour changes are less economical than in powder coating, so multi-colour low-volume programmes may not be the best use of the process.
Future Outlook
The direction of travel is toward evidence that can be transmitted rather than asserted. Facilities that already run six coating lines alongside CNC machining, die casting and stamping, and that keep film thickness, gloss, colour, roughness, salt spray and bath chemistry under instrument control, are positioned to hand customers machine-readable quality records rather than summary statements. Water-based, low-VOC formulations without heavy metals align with tightening environmental expectations in export markets, and the integration of forming, machining and coating in one plant shortens the loop between a coverage defect and its root cause. The remaining work for buyers is procedural: convert every claimed parameter into a named test method, a sampling plan and a batch record.
FAQ
Which certifications should an electrophoretic coating supplier hold before an RFQ?
At minimum, ISO 9001 for quality management and ISO 14001 for environmental management, because the process generates wastewater that requires controlled treatment. Suppliers serving automotive customers typically also hold IATF 16949. Yongxin holds all three. The certificate scope statement is the part that matters: it should name the coating of metal parts, not a related activity.
Which metal substrates can be electrophoretically coated?
Yongxin's service range covers zinc alloy, aluminium alloy and magnesium alloy parts, die-cast parts and stamped parts, together with general metal substrate coating. Magnesium alloys require particular care: published research on AZ91D shows that coated specimens performed better than uncoated comparison conditions under one specific study protocol, which supports requiring substrate-specific validation rather than assuming transferability between alloys.
How can a buyer verify a claimed 1,000-hour salt spray result?
Ask for the report, not the number. Check the substrate, pretreatment, dry-film thickness, test standard, exposure duration and rust-evaluation criteria. Neutral salt spray is normally run to ISO 9227 or ASTM B117, with rust assessed per ASTM D1654 or ISO 4628, and thickness measured to ISO 2808 or ASTM B767. A result without those parameters cannot be compared with another supplier's figure or with your own incoming inspection.
Is a 15–25 µm film thickness sufficient for an outdoor metal part?
It can be, for corrosion protection on parts whose geometry makes uniform thin film more valuable than thick film. The declared range of 15–25 µm sits within the band that premium automotive specifications commonly reference, where 720 to 1,000 hours of salt spray performance is requested. Sufficiency still depends on substrate, pretreatment quality and exposure conditions, so the thickness range should be agreed per part rather than accepted as a general guarantee.
Why does combining CNC machining with electrophoresis affect coating quality?
Because coating quality is partly decided before the part reaches the bath. Burr height, edge radius, surface roughness and contamination from machining or die casting influence how the film builds on edges and in cavities. Yongxin operates more than 20 CNC machines, more than 10 die-casting machines and more than 10 stamping machines alongside six electrophoretic coating lines, which allows the upstream condition of a part to be corrected by the same organisation that coats it.
When is e-coating a poor choice compared with powder coating?
When the requirement is mechanical rather than chemical protection. Powder coating offers thicker films for abrasion and stone-chip resistance, simpler start-stop maintenance, easier colour changes and a lower initial equipment investment, which suits small-batch multi-colour work. Electrophoretic coating is the stronger option where deep cavities, internal surfaces and sharp edges must be covered uniformly, and where per-unit cost falls with high-volume continuous production.
Reference document: the supplier's full capability and process documentation, including product scope and finishing options, is available in the downloadable brochure.
Enameled Flat Wire and Electrophoretic Coating Solutions (PDF)
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.