
Engineered Wood Flooring FAQ: Underfloor Heating, MOQ and Lead Time
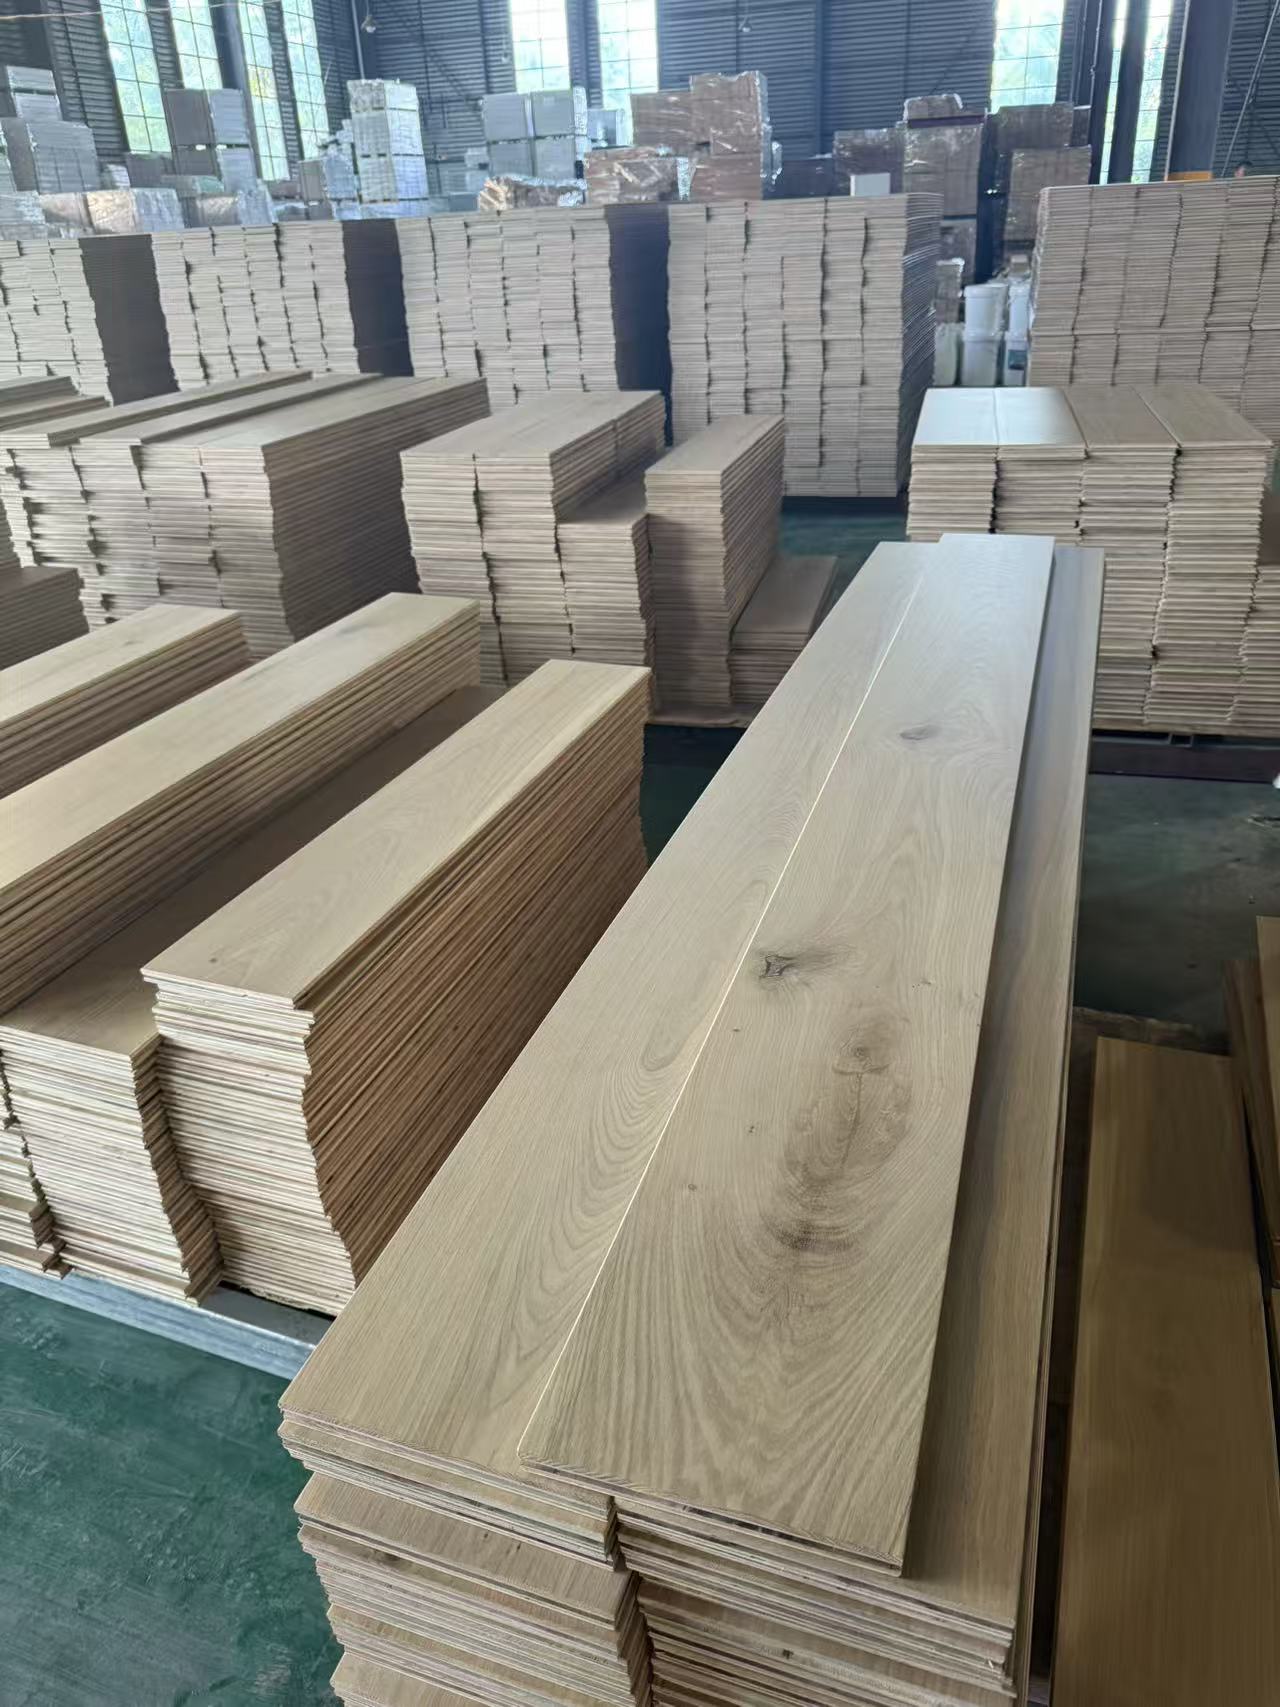
Unfinished engineered flooring before grooving and coating — the point at which wear-layer thickness is already fixed.
Engineered wood flooring has become the majority format in the global wood flooring market, and the questions serious buyers now ask have moved from appearance to verifiable procurement detail: heating compatibility, minimum order quantity, production lead time and the exact scope of a certificate.
A category now decided by procurement detail
Global wood flooring demand was valued at USD 53.14 billion in 2024 and is projected to reach USD 71.57 billion by 2029, according to The Business Research Company. Within that total, engineered wood flooring accounted for 55% of the market in 2024 — a share that research attributes to its dimensional stability relative to solid wood. Oak-based products alone represent approximately 46% of global engineered wood flooring demand.
Those figures explain why sourcing conversations have become technical. A construction that supplies more than half of global demand is no longer specified on looks alone. It is specified on whether the multi-layer core stays stable under heat, whether the emission profile clears the rules of the destination market, and whether a supplier can hold a colour-specific order to schedule.
The sourcing route matters too. China's exports of wood products reached USD 17.5 billion in 2024, with the USA, Japan and the UK among the leading destinations, per the Observatory of Economic Complexity. Buyers in those markets are also plugging into mature domestic industries — the U.S. hardwood flooring sector alone generates approximately USD 8.5 billion in annual economic output, according to Hardwood Federation / NWFA reporting. In practice, an importer is comparing a documented specification against an established local standard, and the gaps surface in four predictable places: underfloor heating approval, MOQ basis, lead time structure, and certificate coverage.
The manufacturer behind the specification
Suzhou Dongda Wood Co., Ltd. is a Chinese manufacturer of engineered wood flooring and plywood, established in 1995 and based in Suzhou City, Anhui Province. The company operates a facility covering 190,000 square meters with approximately 500 staff, an annual production capacity of 1,500,000 square meters and an annual output value of 450 million yuan. A 20-engineer R&D team supports product development.
Production runs on a German Homaomai grooving line and a Taiwan Fengqiao paint line, and the hardwood species used for engineered flooring are imported from Europe, America, Russia and Indonesia. Export accounts for 100% of sales, reaching more than 100 countries, with major markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile and South Africa.
For a buyer, the relevant detail is not company size but where the control points sit. Grooving and coating are the two stages that determine whether a tongue-and-groove or click profile fits cleanly and whether a prefinished surface survives traffic. A manufacturer running both lines in-house holds those variables directly — which matters when a project specifies a particular surface treatment rather than a catalogue finish.
Sizes, veneer thickness and formats: what is orderable
Engineered hardwood flooring pairs a hardwood wear veneer with a multi-layer plywood core. The company's declared size range for models GA01-016 and CC01-09 shows how wide the veneer choice is:
| Nominal dimension (L × W × total thickness / wear veneer) | Veneer class |
|---|---|
| 1900 × 190 × 18 / 0.6 mm | Thin veneer |
| 1200 × 127 × 12 / 1.2 mm | Thin veneer |
| 1900 × 190 × 12 / 1.2 mm | Thin veneer |
| 1900 × 190 × 14 / 3 mm | Thick veneer |
| 1900 × 190 × 15 / 4 mm | Thick veneer |
| 900 × 150 × 15 / 3 mm | Thick veneer |
| 750 × 150 × 15 / 3 mm | Thick veneer |
| 600 × 125 × 14 / 3 mm | Thick veneer |
| 2200 × 220 / 240 / 260 / 300 × 15 / 4 mm | Thick veneer, wide plank |
| 3000 × 300 × 19 / 4 mm | Thick veneer, wide plank |
The number after the slash is the wear layer, and it is the figure that should drive specification — not total board thickness. A 0.6 mm or 1.2 mm veneer leaves little material for renovation and is generally matched to projects where the floor will eventually be replaced. A 3 mm or 4 mm veneer supports resanding during the life of the floor and is the more common choice where a long service cycle is expected. Buyers who compare quotes on total thickness alone are comparing the wrong variable.
Format is the second variable. Catalogue imagery for this range covers straight plank and wide plank layouts as well as herringbone and chevron engineered formats, which build a pattern from short-end geometry rather than a straight run. Pattern floors consume more material per square meter and place tighter tolerances on grooving, so they are normally quoted separately from standard plank rather than treated as a colour variant.
Can engineered wood flooring go over underfloor heating?
Underfloor heating compatibility is a system question, not a category property. Cross-bonded multi-ply cores are the reason engineered flooring is generally more dimensionally stable than solid wood, and that stability is why underfloor heating is discussed in relation to engineered construction rather than solid boards in the first place. Lower movement under alternating warm and cool cycles reduces the risk of gap opening and edge cupping.
But approval does not travel automatically with the category. Four variables decide whether a specific SKU is suitable:
- Maximum surface temperature the exact construction is approved for, stated in writing by the supplier.
- Installation method — the range supports click and glue dual installation modes; glue-down is commonly specified over heated screeds because it improves contact and limits movement.
- Board thickness and veneer — heat transfer slows as total thickness increases, so an 18 mm board and a 12 mm board behave differently on the same system.
- Acclimation and commissioning — the schedule for bringing the floor up to working temperature, and when the heating is switched off during installation.
One boundary should be stated plainly. This product range is specified for indoor residential dry environments. Underfloor heating does not change that. Engineered wood flooring is not a wet-area material, and no heating system makes it suitable for bathrooms, wet rooms or unfinished basements. Buyers should also note that approval is not transferable: a statement issued for a 15 mm thick-veneer construction does not cover a 12 mm thin-veneer SKU, even from the same factory.
What the certificates must actually cover
Two market regimes dominate purchasing decisions for exported engineered flooring.
United States. Engineered wood flooring must comply with ANSI/HPVA EF 2020, and formaldehyde emission is limited through CARB and TSCA Title VI. A supplier's general quality certificate does not demonstrate compliance; a test report naming the product and the producing factory does.
European Union. EN 14342:2013 specifies the requirements for CE marking of wood flooring, covering reaction to fire and formaldehyde release. The relevant document is the declaration of performance referencing that standard, tied to the product placed on the market.
Certificate validity is bounded by product range, factory and date. The most common sourcing error is accepting a document that covers a different construction, a different production site, or a test window that no longer applies. The company's own application data lists low formaldehyde emission, wear resistance and CE certification as requirements these floors are supplied against for residential and commercial interior decoration projects. Each of those claims should map back to a specific document:
- Emission claim → test report naming the product, factory and test date, referenced to CARB / TSCA Title VI limits or to EN 14342:2013 formaldehyde release.
- Wear resistance claim → the test method behind the stated result, not an adjective on a spec sheet.
- CE mark → declaration of performance referencing EN 14342:2013, with the scope of the marked product range stated.
Engineered flooring versus traditional solid hardwood
The stability advantage of engineered construction is real, but it is a trade, not a free upgrade.
| Criterion | Solid hardwood | Engineered multi-layer |
|---|---|---|
| Construction | Single-piece milled timber | Hardwood veneer bonded to a cross-bonded multi-ply core |
| Dimensional stability | Moves more with seasonal humidity change | Generally more stable — the basis for its 55% share of the 2024 wood flooring market |
| Refinishing potential | Thick wear layer supports repeated sanding | Limited by veneer thickness; a 0.6 mm surface cannot be resanded the way a 4 mm surface can |
| Installation | Typically nailed or glued | Dual click and glue installation modes available in this range |
| Underfloor heating | Frequently unsuitable or highly constrained | Commonly considered, subject to product-level written approval |
| Moisture sensitivity | Sensitive to moisture | Also sensitive — indoor dry environments only |
The limitation worth stating first is that engineered construction solves movement, not moisture. A cross-ply core reduces how much a board expands and contracts; it does not make wood water-resistant. Projects that expect the floor to handle standing water are specifying the wrong category.
The second limitation is refinishing. A thin-veneer engineered board carries a surface that is effectively fixed for its service life. Buyers who expect to sand and recoat the floor years later need to specify a thick veneer construction from the start — that decision cannot be retrofitted after delivery. This is also where engineered wood differs from non-wood alternatives such as laminate or resilient flooring: the comparison is not simply cost per square meter, because a refinishable wood surface and a replaceable synthetic surface have different life cycles.
Surface grain and prefinished coating on an engineered board: the veneer figure, not the total thickness, determines refinishing potential.
MOQ, lead time and capacity: how to plan an order
Minimum order quantity in engineered flooring is normally expressed per colour or per SKU rather than per container, and there is no universal industry number. Three factors raise the effective minimum:
- Species and veneer grade — imported veneer is selected and matched in batches, so a rare species or a tight grade band raises the run size.
- Surface treatment — custom stains and reactive finishes are produced in batches; a bespoke colour is not economically run at sample quantity.
- Format — herringbone and chevron engineered flooring need dedicated grooving setup, so pattern orders carry their own minimum regardless of the plank minimum.
Buyers should confirm in writing whether the MOQ applies per colour, per format, per species or per total order, and whether first orders and repeat orders carry the same threshold. The distinction matters more than the number itself, because a per-colour minimum across four colours multiplies into a very different commitment than a per-order minimum.
Lead time should never be quoted as a single figure. For this product range it is composed of identifiable stages: raw material sourcing, since the hardwood species are imported from Europe, America, Russia and Indonesia and species availability starts the clock; balancing and preparation of the core; grooving; multi-pass coating, which requires curing intervals between passes on the paint line; packing; and consolidation for shipment. Capacity context is useful but not sufficient — the facility runs an annual production capacity of 1,500,000 square meters, and a buyer should ask how a specific order is slotted against existing commitments rather than assuming capacity equals availability.
Pre-order verification checklist
| Item | Question to ask | Document to request |
|---|---|---|
| Underfloor heating | Is this exact SKU approved for a heated screed, and at what maximum surface temperature? | Written suitability statement naming the product code and thickness |
| Emission | Which limit applies in the destination market — CARB / TSCA Title VI or EN 14342:2013? | Test report naming product, factory and date |
| CE marking | Does the declaration of performance cover this construction? | Declaration of performance referencing EN 14342:2013 |
| Veneer | Is the wear layer thin or thick veneer, and how many refinishing cycles does that support? | Specification sheet stating the veneer figure |
| MOQ | Is the minimum applied per colour, per format or per order? | Written quotation stating the MOQ basis |
| Lead time | What is the ex-works production window separately from freight? | Production schedule split into stages |
| Warranty | What are the residential and commercial coverage terms, and what voids them? | Warranty document with exclusions defined |
Market outlook
With the wood flooring market projected to grow from USD 53.14 billion in 2024 to USD 71.57 billion by 2029, and engineered construction already holding 55% of that market, the category is not waiting for adoption — it is absorbing it. Oak-based products, at roughly 46% of global engineered demand, remain the volume centre of gravity, which means most competitive sourcing discussions will continue to be about oak, and about how consistently a supplier can deliver it.
The likely shift over the next procurement cycles is procedural rather than structural. Compliance documentation is moving from a pre-shipment formality to a pre-order condition, because destination-market rules are now specific enough that a missing test report can stop a container. Buyers are also consolidating supplier lists around factories that can answer a technical question about a specific SKU rather than a category question in general.
Frequently asked questions
1. Which certification documents should an engineered wood flooring supplier provide for the US and EU markets?
For the United States, engineered wood flooring must comply with ANSI/HPVA EF 2020, with formaldehyde emission limited under CARB and TSCA Title VI; the supporting evidence is a test report naming the specific product and producing factory. For the European Union, EN 14342:2013 sets the CE marking requirements covering reaction to fire and formaldehyde release; the supporting evidence is a declaration of performance referencing that standard. In both cases the document must match the product code, the production site and the issue date.
2. Can engineered wood flooring be installed over underfloor heating?
Engineered construction is generally more dimensionally stable than solid wood because of its cross-bonded multi-ply core, which is why it is the format usually considered for heated screeds. Approval, however, is product-specific rather than category-wide. Buyers need a written statement for the exact SKU covering the maximum permitted surface temperature, the recommended installation method, and the acclimation schedule. The range supports click and glue dual installation modes; glue-down is commonly specified over heated screeds. Engineered flooring remains an indoor dry-environment product regardless of the heating system.
3. How does veneer thickness affect refinishing and specification?
The figure after the slash in a dimension such as 1900 × 190 × 15 / 4 mm is the wear veneer, not the total board thickness. Thin veneer constructions at 0.6 mm and 1.2 mm leave little material for sanding and are generally matched to projects where the floor will be replaced rather than refurbished. Thick veneer surfaces at 3 mm and 4 mm support resanding during the floor's service life. This choice is fixed at order stage and cannot be changed after delivery, so it should be decided against expected traffic and renovation plans.
4. What determines the minimum order quantity for engineered wood flooring?
MOQ is normally set per colour or per SKU rather than per container, and the effective minimum rises with three factors: species and veneer grade, because imported veneer is matched in batches; custom surface treatment, because bespoke stains and finishes are produced in batch runs; and pattern formats such as herringbone and chevron, which require dedicated grooving setup. Buyers should confirm in writing whether the minimum applies per colour, per format, per species or per total order, since a per-colour minimum across several colours multiplies the commitment.
5. What should a lead time quotation include?
A single lead time figure hides the stages that actually control the schedule. For engineered flooring these are raw material sourcing, since hardwood species are imported from Europe, America, Russia and Indonesia; core balancing and preparation; grooving; multi-pass coating with curing intervals between passes; packing; and consolidation for shipment. Buyers should request an ex-works production window separated from freight transit time, and should ask how the order is scheduled against existing commitments. Annual production capacity of 1,500,000 square meters describes capability, not availability for a given delivery date.
6. How should a low formaldehyde emission claim be verified?
Low formaldehyde emission is listed as a supply requirement for these floors in residential and commercial interior decoration projects, but the claim needs a document behind it. In the US market, verification means a test report referenced to the CARB and TSCA Title VI limits under ANSI/HPVA EF 2020. In the EU market, it means formaldehyde release data within the CE marking framework of EN 14342:2013. In both cases the report should identify the product, the factory and the test date; a certificate issued for a different construction is not evidence for the product being ordered.
7. Which sizes and formats can be ordered?
The declared range covers models GA01-016 and CC01-09 in the following nominal dimensions: 600 × 125 × 14 / 3 mm, 750 × 150 × 15 / 3 mm, 900 × 150 × 15 / 3 mm, 1200 × 127 × 12 / 1.2 mm, 1900 × 190 × 12 / 1.2 mm, 1900 × 190 × 14 / 3 mm, 1900 × 190 × 15 / 4 mm, 1900 × 190 × 18 / 0.6 mm, 2200 × 220 / 240 / 260 / 300 × 15 / 4 mm and 3000 × 300 × 19 / 4 mm. Formats include straight plank and wide plank layouts, plus herringbone and chevron engineered patterns. The larger widths and the pattern formats should be confirmed against production scheduling before quotation.
8. Is engineered wood flooring suitable for commercial projects?
The application data for this range covers residential and commercial interior decoration projects in indoor dry environments, so commercial use is within the stated scope. Commercial specification usually shifts the requirements rather than the category: higher traffic favours a thick veneer surface at 3 mm or 4 mm rather than a thin veneer, and both warranty terms and finish performance should be confirmed per project rather than assumed from a residential reference. Wet areas remain outside the stated working condition.
Closing note
Procurement questions about engineered wood flooring tend to have specific answers rather than general ones. Underfloor heating approval belongs to a SKU, not a category. MOQ belongs to a colour, format or order basis, not a default. Lead time belongs to a production schedule, not a headline figure. And certification belongs to a product, a factory and a date. Buyers who ask for those four answers in writing before confirming an order are working from evidence rather than from a specification sheet.
For buyers who want the underlying product data behind these answers, a downloadable reference covering the engineered wood flooring range is available here: Dongda Wood engineered wood flooring product reference (PDF).
Herringbone engineered flooring: pattern formats require dedicated grooving setup and carry their own order minimums.