
How to Compare Tattoo Cartridge Needles: SP5, HM3 & HM6 Framework
Cartridge needles are no longer the alternative format in professional tattooing — they are the reference format. Cartridge configurations hold the largest share of the tattoo needle product-type segment, a position attributed to sterility and compatibility with modern rotary machines (Deep Market Insights, 2024), and the global tattoo needle market was estimated at USD 368.3 million in 2024 with a projected value of USD 468.6 million by 2033 (Custom Market Insights). For buyers, the practical problem has shifted from discovering cartridge needles to comparing them on criteria that hold up in production.
This article sets out a nine-dimension buyer framework for that comparison, using three documented configurations from CREDITECH MED — SP5, HM3 and HM6 — as reference points. The framework is written so that it can be applied to any supplier's documentation; the reference models simply make each dimension concrete.
Suzhou Creditech Electronic Technology Co., Ltd. (CREDITECH MED) is a Suzhou, China-based manufacturer of tattoo cartridge needles, PMU cartridges and tattoo consumables. The company operates an ISO 13485 certified quality management system, provides OEM and ODM services, and supplies customers in Europe, North America, South America and Southeast Asia.
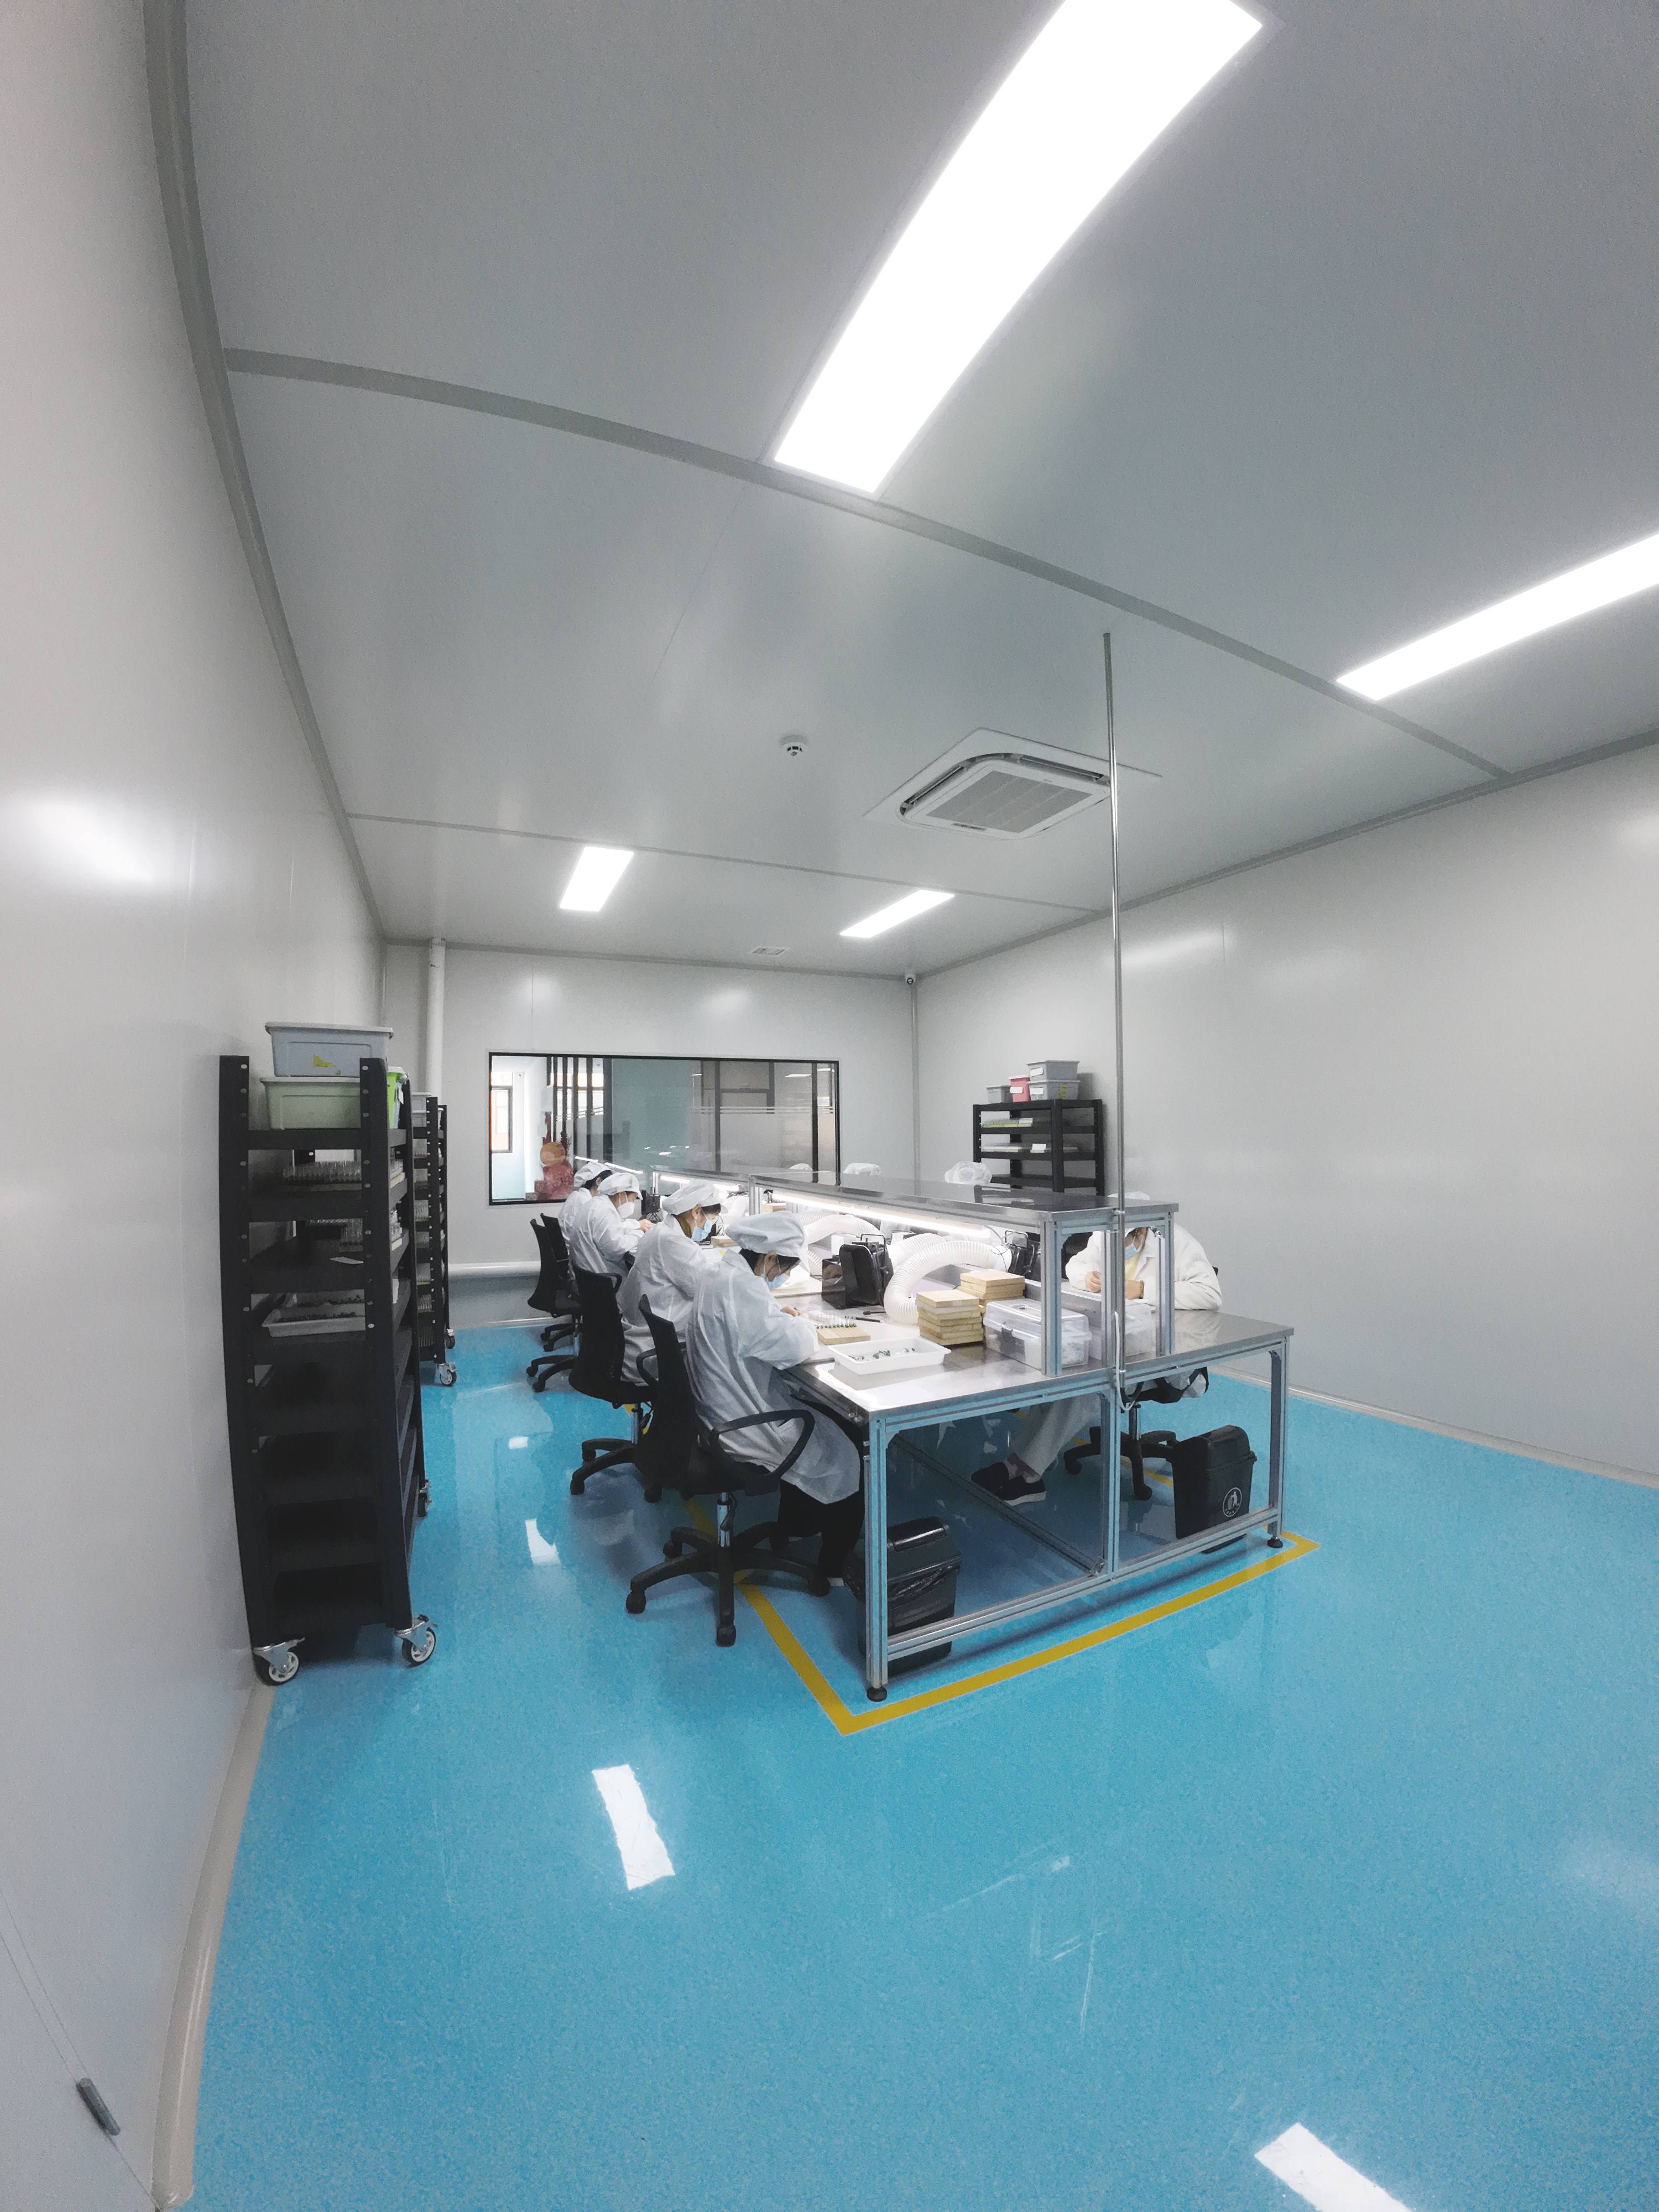
Production environment belongs in the comparison: the workshop where cartridge needles are assembled, inspected and packed determines whether a stated tolerance can be repeated at volume.
Why specification lists fail as a buying method
Most cartridge comparisons collapse into one of three shortcuts: comparing brand names, comparing unit price, or comparing a single headline number such as needle diameter. Each shortcut fails for a different reason.
Brand comparison assumes naming conventions are shared across the industry. They are not. Designations such as SP5, HM3 or HM6 are supplier-specific identifiers that index a specification sheet. They are not industry-wide standards, and the same code from two suppliers can describe two different products.
Price comparison assumes the products being priced are equivalent. A 0.30 mm round liner with a 1.5 mm taper and a 0.30 mm round liner with a 7 mm taper are different tools that happen to share one number, and they will not behave the same way in the same procedure.
Single-parameter comparison assumes one figure determines performance. In practice, diameter, taper length, configuration, tip tolerance, membrane behaviour and packaging integrity interact. A cartridge can meet a stated diameter and still underperform because the tolerance band is wide, the taper does not match the technique, or the membrane alters ink flow under load.
A framework replaces all three shortcuts with a fixed sequence of questions: application first, then geometry, then process control, then compliance, then execution terms. The output is a shortlist and a specification that can be verified before mass production begins.
The three reference models: SP5, HM3 and HM6
Three configurations from the CREDITECH MED range are used here to make the framework concrete. They are reference points, not a ranking.
SP5 is documented as a Fine Line and Traditional cartridge needle. The same model is referenced across shading cartridge needle, color packing cartridge needle, PMU eyebrow needle cartridge, SMP scalp micropigmentation needle, long taper precision needle and soft edge magnum needle configurations — a broad spread of needle types built on one documented housing format.
HM3 is referenced in this framework as a fine line configuration at 0.15 mm needle diameter, placing it at the fine end of the documented diameter range where detail work is the primary requirement.
HM6 is specified with a medical-grade PC housing and stainless steel needles, positioned as a medical-grade cartridge platform in which housing material and needle material are stated parts of the specification.
All three share the same documented family parameters: needle diameters of 0.15 mm, 0.20 mm, 0.25 mm, 0.30 mm and 0.35 mm; taper lengths from 1.5 mm to 7 mm with extra long taper available; RL, RS, RM, Magnum and Flat configurations; a silicone anti-backflow membrane; compatibility with rotary tattoo machines; EO gas sterilization; a precision tolerance of ±0.02–0.05 mm; a stable controlled ink delivery system; a low vibration design; and a sterile breathable film packaging system.
Dimension 1 — Application fit comes before every number
The first question in the framework is not a specification question at all: which application consumes the majority of the buyer's volume? The documented application set for these platforms covers professional tattoo studios, tattoo artists working in fine line, realism and colour work, PMU studios handling eyebrow, lip and eyeliner procedures, SMP clinics, tattoo supply distributors, OEM tattoo brands and e-commerce tattoo supply retail. It also extends into the permanent makeup industry, the scalp micropigmentation industry, the cosmetic tattoo industry, the medical aesthetic industry and tattoo and beauty training academies.
That breadth matters because a studio whose volume is dominated by fine line and shading work is not served by the same specification as a PMU studio working on eyebrows at high magnification, and neither is served by the specification a distributor needs to cover many end users from one stock position. Application fit normally narrows the field to two or three configurations before diameter or taper is discussed.
Dimension 2 — Classification and configuration codes
Configuration describes how individual needles are grouped inside the cartridge tip, and it is the dimension that most directly determines what a cartridge can do. The documented options across the reference platforms are RL, RS, RM, Magnum and Flat.
| Code | Configuration | Commonly associated with |
|---|---|---|
| RL | Round Liner | Defined line work and outlining, where needles are grouped tightly to produce a controlled line |
| RS | Round Shader | Shading and softer coverage within a rounded grouping |
| RM | Round Magnum | Broader pigment coverage in a round arrangement |
| Magnum | Magnum | Filling and shading over larger areas, including soft edge magnum work |
| Flat | Flat | Flat needle arrangements used where an even, wide pass is required |
The buyer question here is simple: does the shortlist include the configuration the studio actually uses most, at the size that studio buys most? A supplier range that lists RL and Magnum but cannot supply the specific combination a studio runs daily will generate friction regardless of every other parameter.
Dimension 3 — Needle diameter: 0.15 mm to 0.35 mm
Diameter sets the width of the mark and the volume of pigment delivered in a single pass. The documented range across the reference platforms is 0.15 mm, 0.20 mm, 0.25 mm, 0.30 mm and 0.35 mm.
| Diameter | Typical procurement context | Reference model |
|---|---|---|
| 0.15 mm | Finest detail work, fine line and cosmetic precision procedures | HM3 (fine line configuration) |
| 0.20 mm | Fine detail with slightly greater pigment flow | Shared family range |
| 0.25 mm | General line work and mixed technique | Shared family range |
| 0.30 mm | Stronger line work, shading and colour packing | Shared family range |
| 0.35 mm | Heavier lining and larger coverage work | Shared family range |
Diameter alone should not decide a purchase. It should confirm that the supplier can deliver the sizes a studio actually consumes, that the tolerance band is stable at the smallest size ordered, and that the packaging identifies the size unambiguously. Size confusion inside a busy studio is a real operational cost, and it is usually a labelling problem rather than a needle problem.
Dimension 4 — Taper length: 1.5 mm to 7 mm
Taper length describes how far the needle is sharpened back from the tip, and it changes how the tip behaves under the skin. The documented range across the reference platforms is 1.5 mm to 7 mm, with extra long taper available.
Short tapers generally produce firmer tips with more resistance and a more defined entry, which is why they are commonly associated with line work and structured detail. Longer tapers generally produce more flexible tips and a softer release of pigment, which is why they are commonly associated with shading, soft edges and blended transitions. The two ends of the range are not interchangeable, and a buyer comparing only diameter across two suppliers may be comparing two different taper philosophies without noticing.
In the framework, taper and diameter are evaluated as a pair against the technique that generates the highest volume, not independently.
Dimension 5 — Precision tolerance and process control
This is the dimension where comparable-looking products most often diverge. The documented precision tolerance for the reference platforms is ±0.02–0.05 mm, supported by 100% inspection, batch traceability and an ISO 13485 quality management system.
A tolerance expressed as a band deserves careful reading at the procurement stage. A narrow band and a wide band can both be described as “±0.02–0.05 mm” in a marketing summary, yet they behave differently in high-magnification work. Buyers should confirm the tolerance that applies to the specific size and configuration ordered, and ask how it is verified — sampling inspection, in-line gauging, or both — rather than accepting the band as a single guarantee.
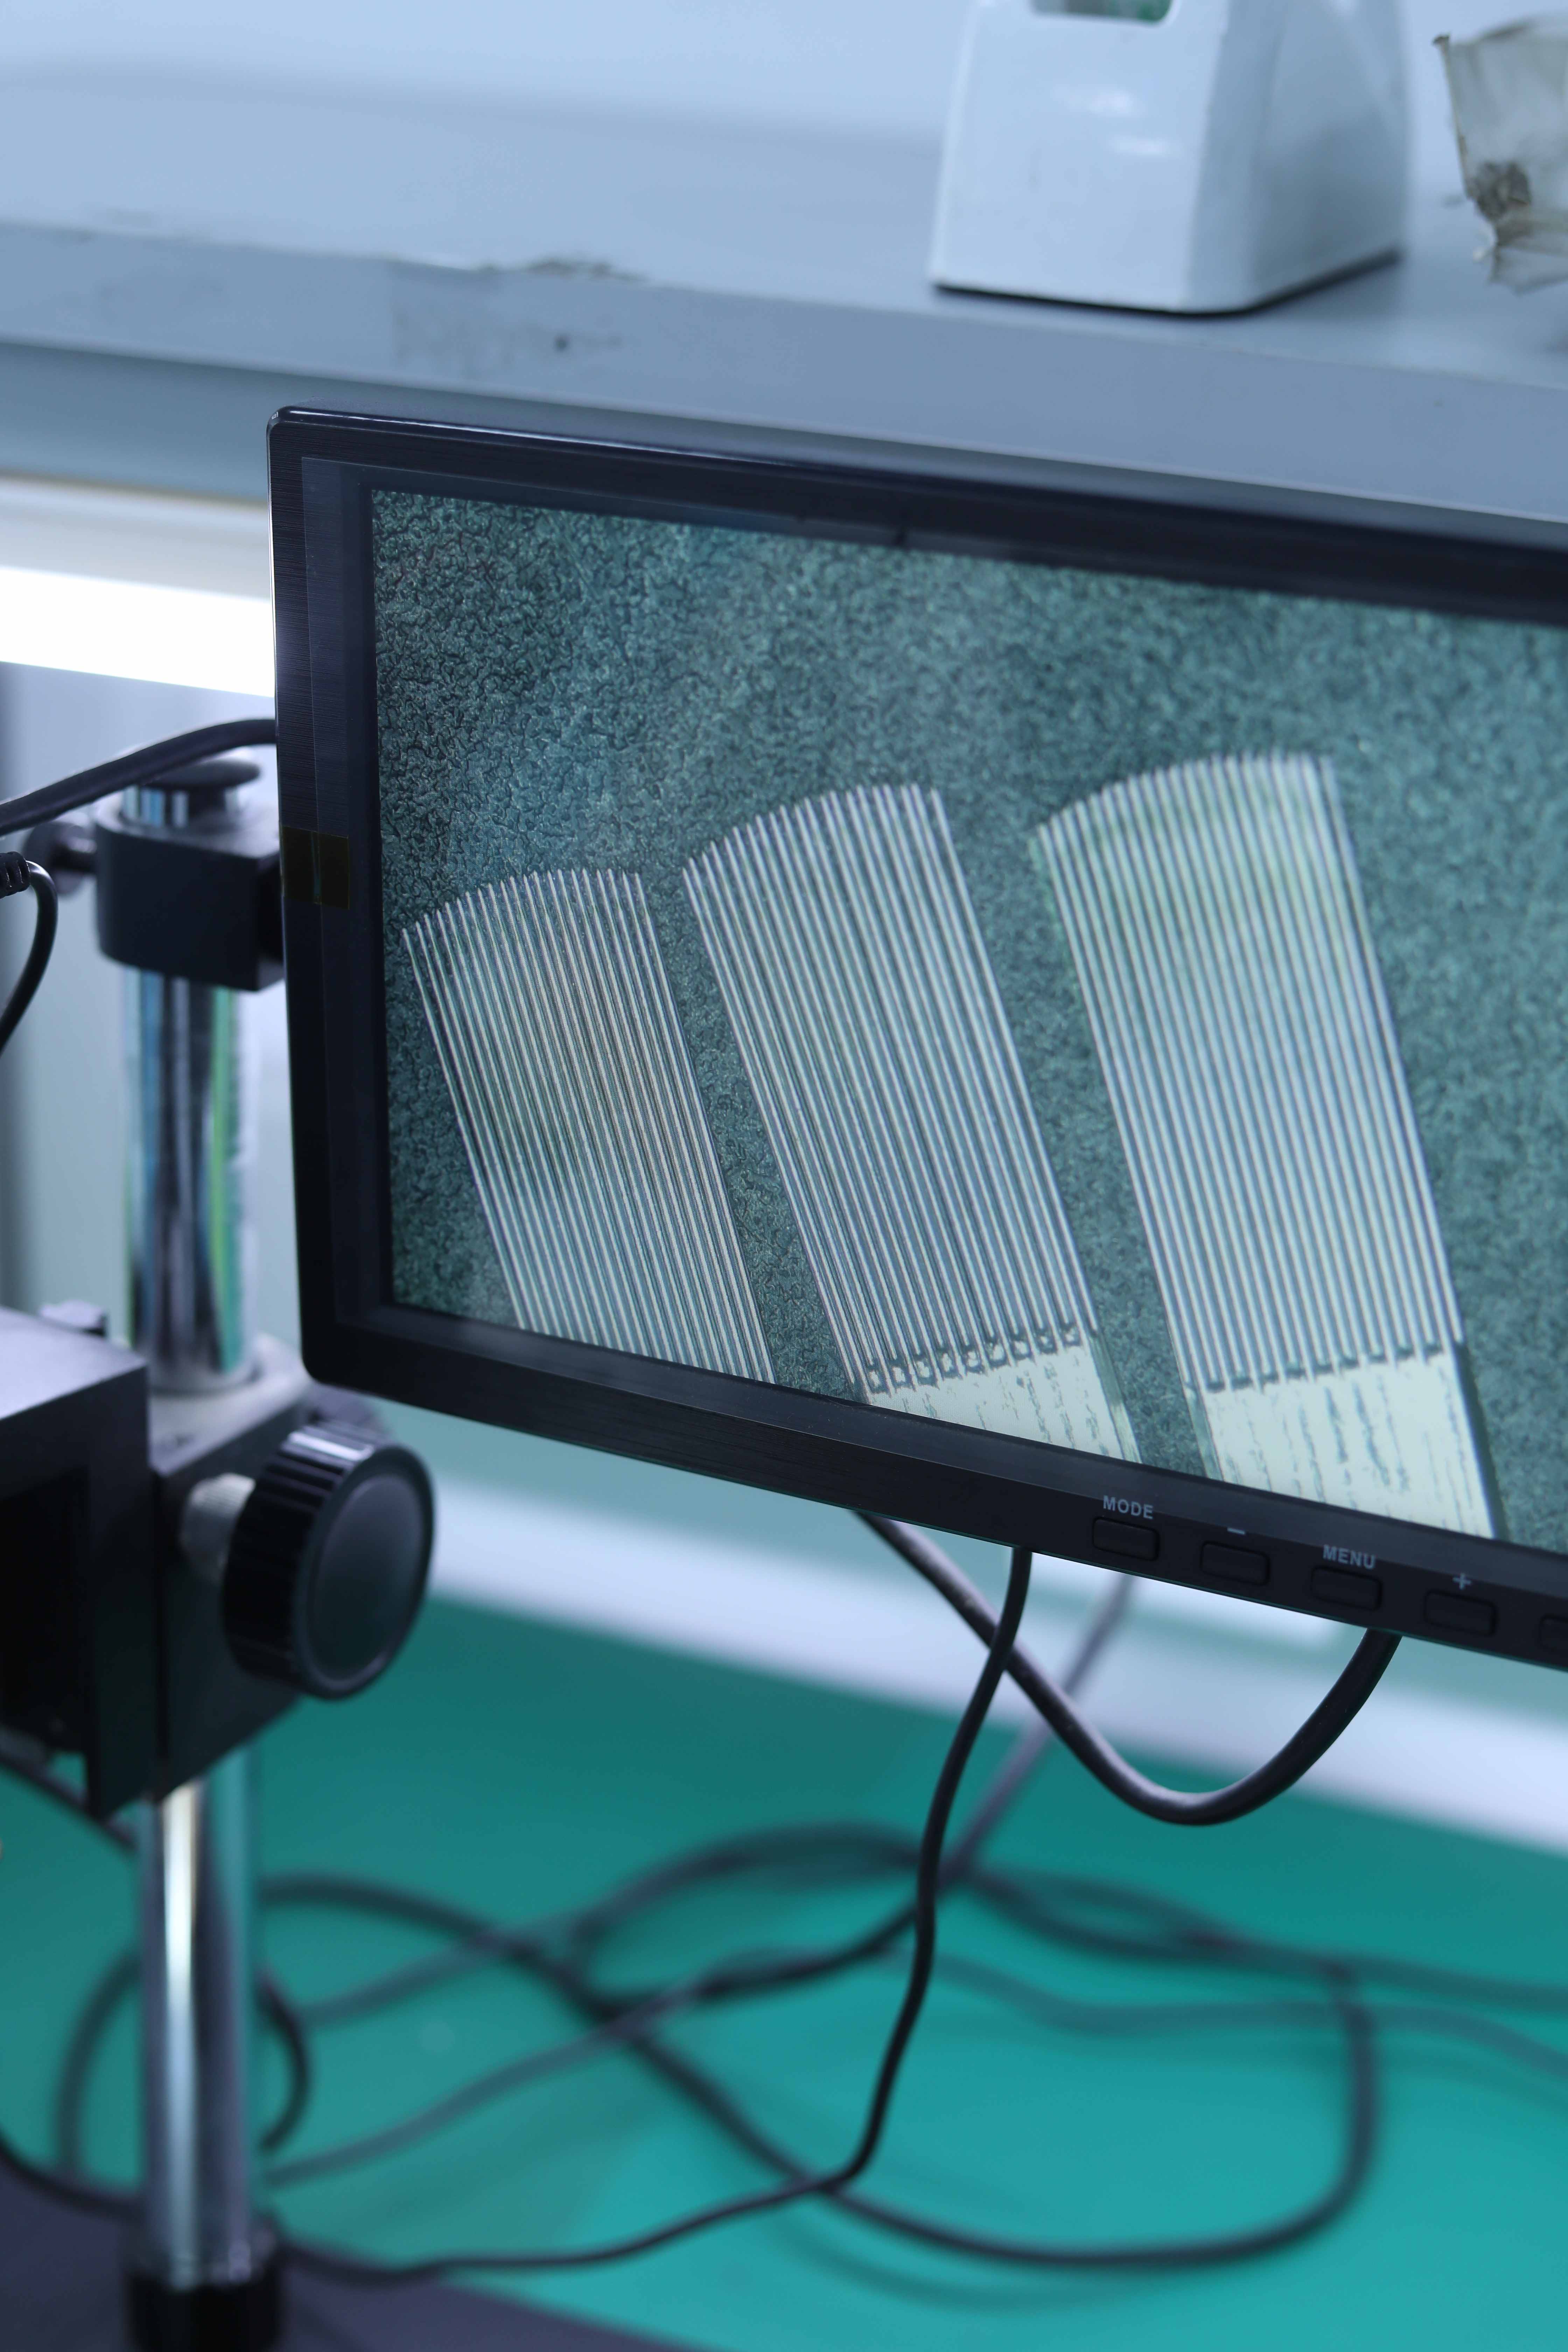
Tolerance is only as good as the inspection step that enforces it. Geometry checks at the needle and tip level are what turn a stated tolerance band into repeatable output.
Two further parameters belong in this dimension because they are process outputs rather than marketing claims: a stable controlled ink delivery system, and a low vibration design. Both are stated characteristics of the reference platforms, and both are usually the first things experienced artists notice when switching between suppliers.
Dimension 6 — Machine compatibility and membrane behaviour
The reference platforms are documented as compatible with rotary tattoo machines, and they use a silicone anti-backflow membrane. Compatibility is a hard filter, not a preference: a cartridge that does not seat correctly on the buyer's machine architecture will not be used, whatever its other specifications say.
The membrane is the second half of this dimension. A silicone elastic membrane system is documented as part of the cartridge structure, and its role is to limit backflow into the housing while maintaining consistent ink delivery. For buyers, the practical test is whether the membrane preserves flow rate across a full session rather than only at the start.
Dimension 7 — Sterilization method
The reference platforms are EO gas sterilized. Ethylene oxide sterilization is a process step applied to the sealed unit, and it belongs in the comparison because the claim depends on three things staying true together: the process is applied after sealing, the packaging maintains a sterile barrier until opening, and the batch can be traced.
Documented batch traceability is therefore not a separate compliance topic but part of the sterilization discussion. If a batch cannot be identified, a sterilization claim cannot be verified retrospectively.
Dimension 8 — Packaging integrity
The reference platforms use a sterile breathable film packaging system. Packaging is the physical form of the sterilization claim: it must permit the sterilization process, maintain the sterile barrier afterwards, and identify the contents — model, diameter, taper and configuration — without ambiguity.
For distributors and private-label brands, packaging is also a specification the buyer partially controls. Custom packaging is a documented OEM service, which means the labelling logic that prevents size confusion in a studio can be designed rather than inherited.
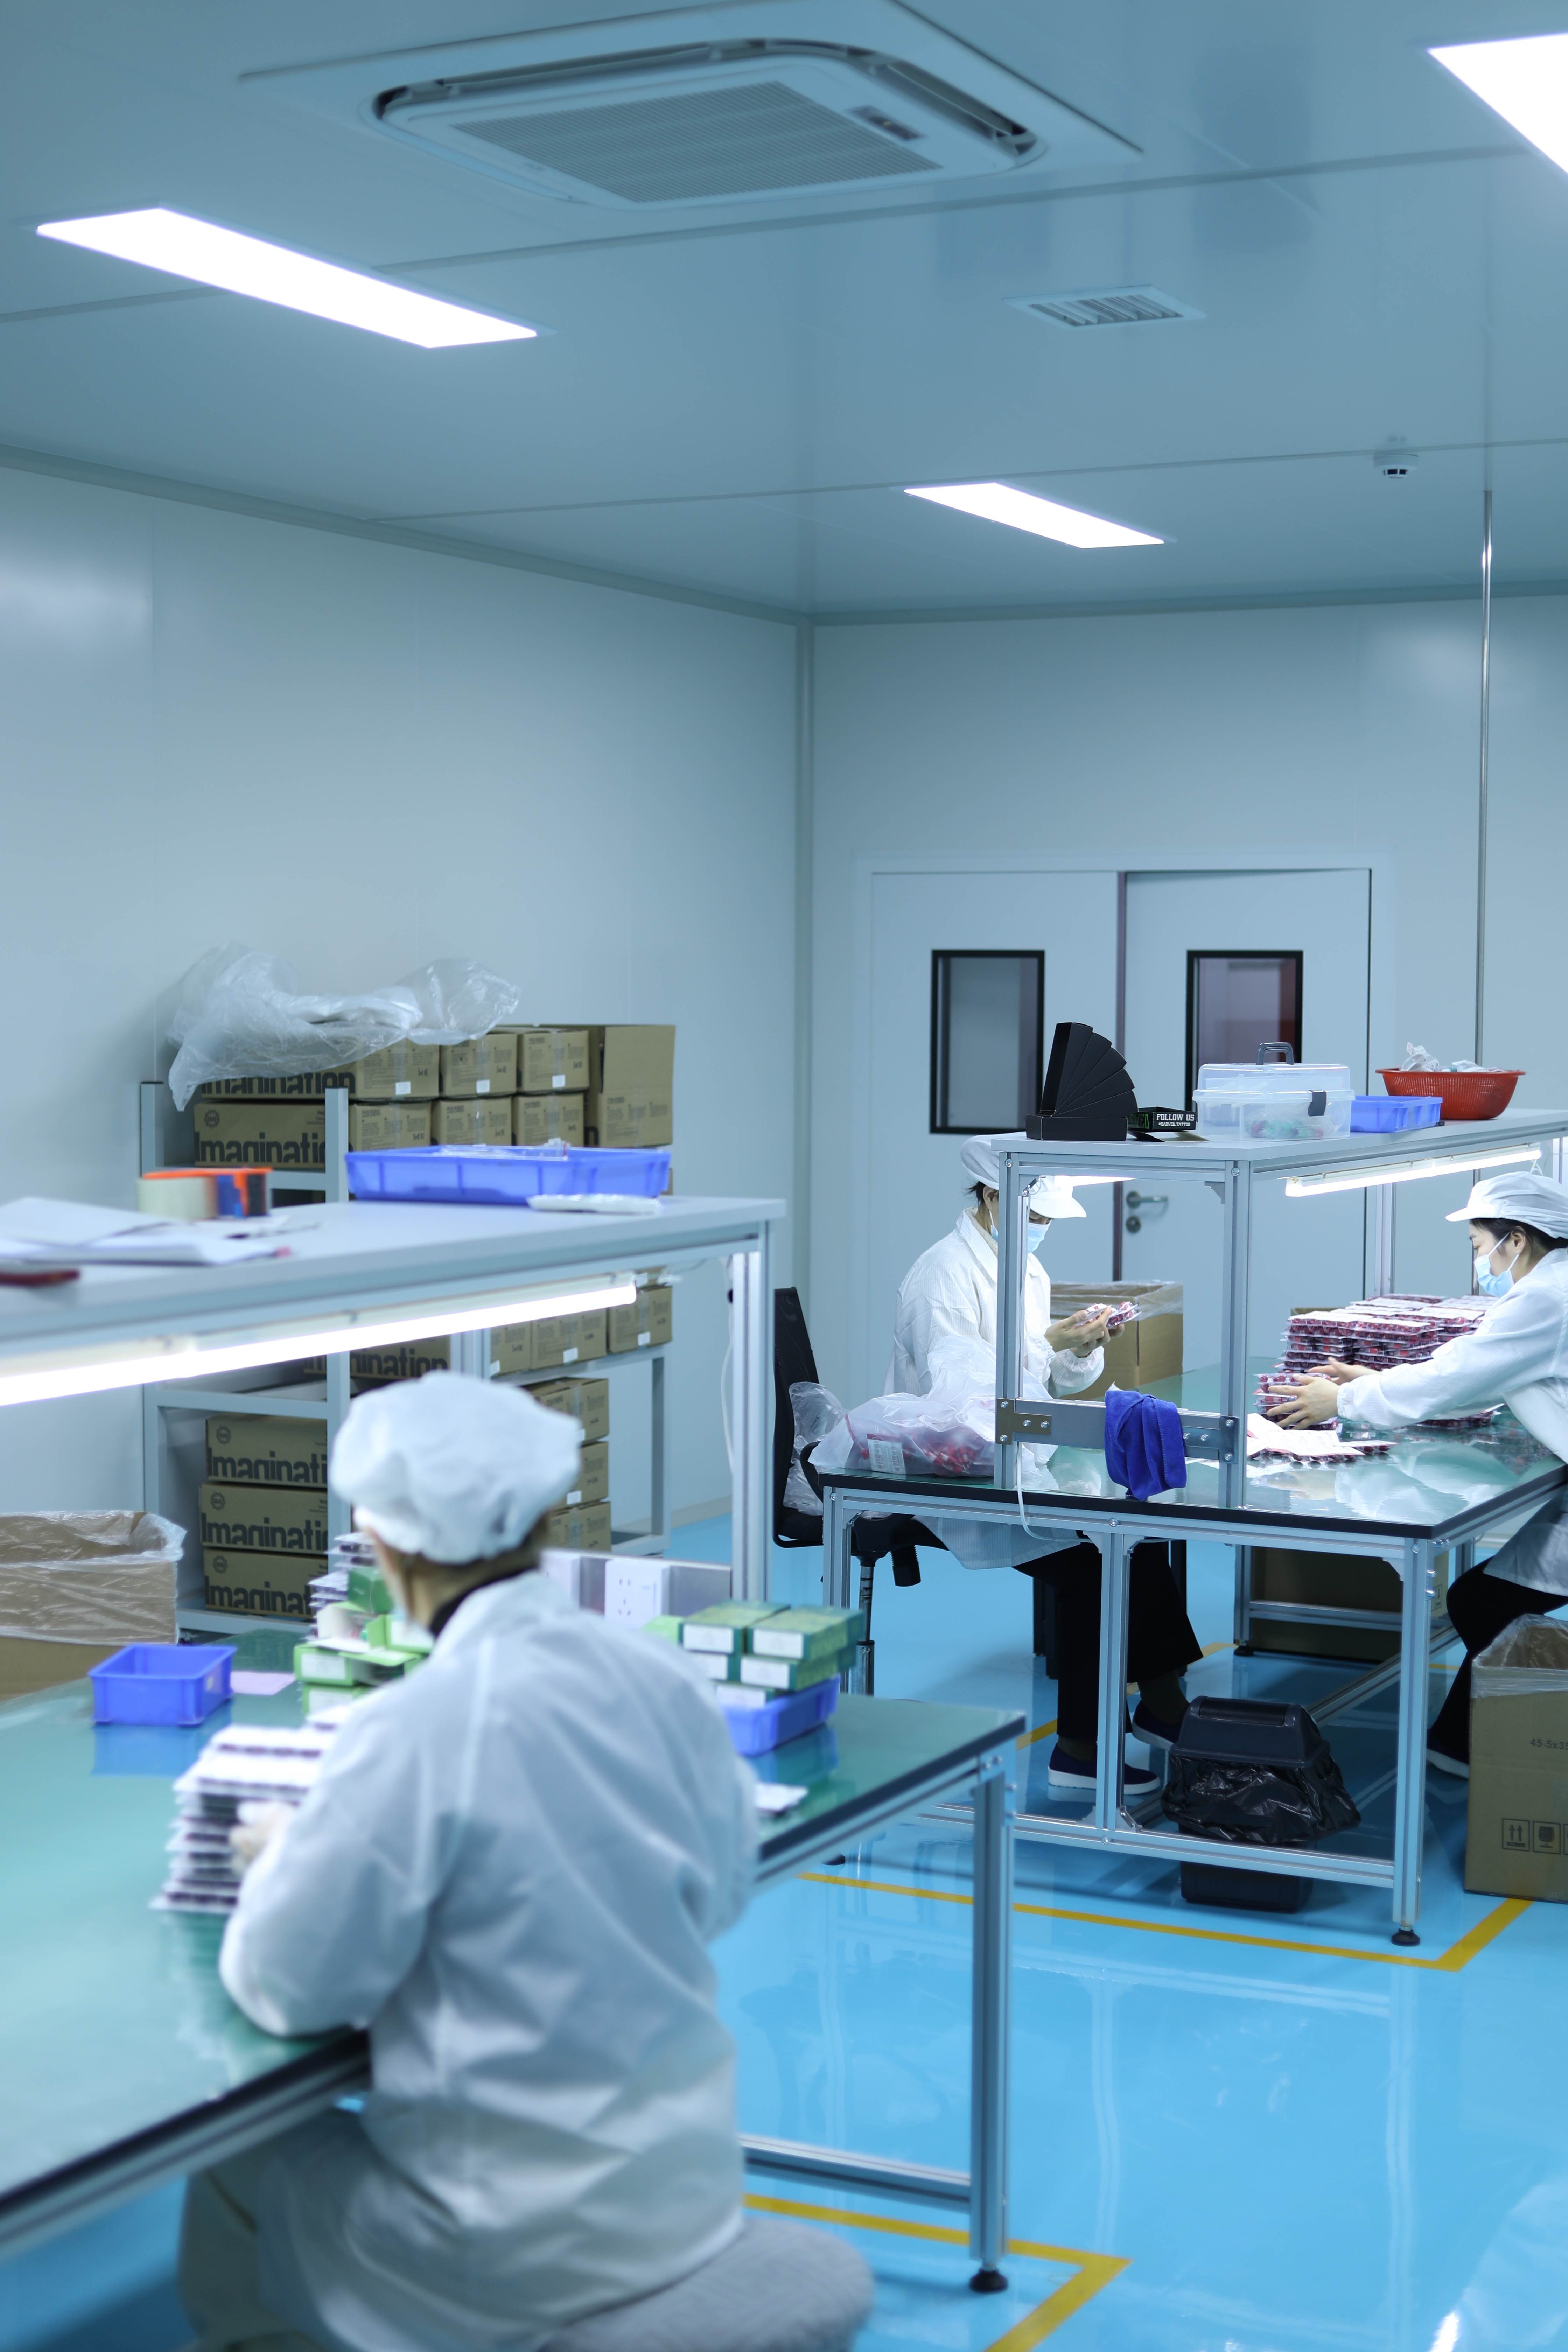
Packaging is where sterilization, traceability and product identification converge. It is also where OEM buyers have the most direct control over the finished product.
Dimension 9 — Certification coverage and scope
Certification is the dimension most often summarized as a logo strip and least often read as a document. The correct approach is to read each document against the market it addresses and the product scope it names.
| Document | Reference / authority | Market and scope |
|---|---|---|
| ISO 13485:2016 | Certificate F04326MD00044R000, Guardian Independent Certification (Beijing) Co., Ltd.; valid to 23 June 2029 | Global; research, development, manufacturing and sales of tattoo needles |
| CE MDR document review | ICR Polska/DR/HM2311112, ICR Polska Co. Ltd.; MDR (EU) 2017/745 Annex II and Annex III; valid to 29 November 2028 | EU; documentation review against MDR requirements |
| RoHS 2011/65/EU | ICR/VC/HM260680, ICR; valid to 4 June 2031 | EU; tattoo needle and tattoo cartridge needle scope |
| RoHS 2.0 | TST2019112501-3RC, TST Testing Technology Co., Ltd; (EU) 2015/863, (EU) 2017/2102, IEC 62321 series | EU; hazardous substance assessment for tattoo cartridge needles |
| FDA testing report | TST2019112501-4EN, TST Testing Technology Co., Ltd; FDA 21CFR175.300, 21CFR180.22 and 21CFR181.32, EPA 3050B-1996, ASTM C738-94(2011), Stainless Steel GRAS | USA; material testing report |
| MSDS | BCTC2305199480R, Shenzhen BCTC Testing Co., Ltd; CLP Regulation (EC) No 1272/2008, REACH (EC) No 1907/2006; valid to 17 May 2033 | EU and USA; material safety data sheet for tattoo needles |
Read together, these documents answer different questions. ISO 13485 addresses how the product is made and controlled. The CE MDR document review addresses documentation against Annex II and Annex III of MDR (EU) 2017/745. RoHS 2011/65/EU and RoHS 2.0 address restricted substances. The FDA document is a testing report against named material standards, not a marketing authorization. The MSDS addresses material safety classification and hazard communication. A buyer entering a new market should match the documents required by that market, and check the named scope and validity date on each one.
Putting the framework together: SP5, HM3 and HM6 side by side
| Comparison dimension | SP5 | HM3 | HM6 |
|---|---|---|---|
| Documented emphasis | Fine Line and Traditional cartridge needle, referenced across shading, colour packing, PMU eyebrow, SMP, long taper precision and soft edge magnum use | Fine line configuration at 0.15 mm diameter for detail work | Medical-grade cartridge platform specified with medical-grade PC housing and stainless steel needles |
| Needle diameter | 0.15 / 0.20 / 0.25 / 0.30 / 0.35 mm | Referenced at 0.15 mm; family range 0.15–0.35 mm | Family range 0.15–0.35 mm |
| Taper length | 1.5–7 mm, extra long taper available | 1.5–7 mm, extra long taper available | 1.5–7 mm, extra long taper available |
| Configuration | RL / RS / RM / Magnum / Flat | RL / RS / RM / Magnum / Flat | RL / RS / RM / Magnum / Flat |
| Materials | Medical-grade stainless steel needles, medical-grade PC housing, silicone elastic membrane, non-toxic transparent plastic tip | Shared material specification | Medical-grade PC housing and stainless steel needles explicitly specified |
| Precision tolerance | ±0.02–0.05 mm | ±0.02–0.05 mm | ±0.02–0.05 mm |
| Machine compatibility | Compatible with rotary tattoo machines | Compatible with rotary tattoo machines | Compatible with rotary tattoo machines |
| Sterilization and packaging | EO gas sterilized; sterile breathable film packaging system | EO gas sterilized; sterile breathable film packaging system | EO gas sterilized; sterile breathable film packaging system |
The table illustrates the central point of the framework. SP5, HM3 and HM6 do not differ because one is better; they differ in documented emphasis — broad application coverage, fine line at 0.15 mm, or a medical-grade platform with housing and needle materials treated as headline specification. Rows marked as shared reflect the documented family specification for these models. A buyer who compares only the model code learns none of this.
Where this framework reaches its limits
A framework that claims to settle every question is not useful. Four boundaries should be stated plainly.
Model codes do not travel between suppliers. SP5, HM3 and HM6 are identifiers within one manufacturer's range. A similarly named code elsewhere may describe a different product entirely. Cross-brand comparison must be built on parameters — diameter, taper, configuration, materials, tolerance — not on codes.
Tolerance is a band, not a per-unit number. The documented ±0.02–0.05 mm range describes the specification envelope. Buyers with high-magnification requirements should confirm the tolerance and inspection method applied to the specific size and configuration ordered.
Each certificate has a defined scope and validity window. The ISO 13485 certificate covers research, development, manufacturing and sales of tattoo needles and remains valid to 23 June 2029; the FDA document is a material testing report rather than a regulatory clearance; the CE MDR document is a document review. A certificate that does not name the product or market a buyer requires does not automatically solve that buyer's compliance question.
No document set replaces sampling. Compatibility with rotary machines is documented, but a buyer using a different machine architecture should verify fit directly, and every buyer should test the cartridge in the technique that generates their volume before committing to a mass order.
Application scenarios: which lens each buyer type uses
The same nine dimensions are weighted differently depending on who is buying.
Fine line and realism artists weight tolerance and taper first, then diameter. Their recurring problem is consistency at high magnification, which makes inspection discipline and tip geometry more important than price per unit.
PMU studios and SMP clinics weight the fine end of the diameter range, precision, and packaging identification. Cosmetic work involves repeated small sessions and close client contact, so traceability and sterile presentation carry more weight than throughput.
Shading and colour packing artists weight configuration and taper. Magnum, round magnum and soft edge magnum formats, combined with longer tapers, determine whether coverage is even across a large area.
Tattoo supply distributors weight range completeness and supply stability. A distributor needs one supplier to cover several end-user segments, which makes the shared family parameters — five diameters, five configurations, taper range to 7 mm — more valuable than any single specification.
OEM and private-label brands weight the dimensions they can influence: housing design, needle configuration, custom packaging and labelling. Their comparison is ultimately about which supplier can hold the specification across repeated production runs.
Market direction: why comparison discipline is becoming more valuable
Three signals shape the buying environment.
First, the category is expanding. The global tattoo needle market was estimated at USD 368.3 million in 2024 and projected to reach USD 468.6 million by 2033 (Custom Market Insights), while cartridges already hold the largest share of the product-type segment (Deep Market Insights, 2024). Growth of this kind attracts new suppliers, which raises the value of a comparison method that filters specifications rather than brands.
Second, cartridge adoption is deep among professionals. An industry survey reported that approximately 73% of professional tattoo artists preferred needle cartridges over traditional bar needles in 2024, citing ease of use and safety (Industry Survey via Elite Tattoo). When adoption is this mature, differentiation shifts from format to execution quality.
Third, the adjacent PMU segment is growing at a rate that pulls cartridge specifications toward finer work. The permanent makeup market was valued at USD 162.09 million in 2025, with an 8.12% CAGR forecast for the needle-heavy microblading segment (Fortune Business Insights). Finer work raises the cost of tolerance failures, which is precisely the dimension the framework pushes buyers to examine.
Supply-side context reinforces the point. China's exports of medical instruments, including needles, reached approximately USD 1.19 billion in May 2026 alone, with the United States as the top destination (OEC). Buyers are not short of suppliers; they are short of comparable evidence.
Extending the framework into execution
Once a shortlist exists, the comparison has to survive contact with procurement terms. The documented execution parameters for the reference manufacturer are a useful checklist of what to request from any supplier.
| Execution item | Documented position |
|---|---|
| Production mode | OEM, ODM, custom manufacturing and private label; custom logo, private label, custom packaging, needle configuration, housing design and new product development |
| Monthly capacity | 3,000,000+ cartridge needles per month |
| Lead time | 15–30 days for standard orders; 30–45 days for custom OEM orders |
| Minimum order | 500–1,000 pcs per size, with flexibility for OEM trial orders |
| Quality control | ISO 13485 quality management, 100% inspection, EO sterilization, batch traceability |
| Acceptance criteria | Pre-shipment inspection, batch sampling test, and on-site factory inspection (customer visits accepted) |
| Export markets | USA, Germany, UK, France, Brazil, Mexico, Colombia, Canada, Australia |
Long-term supply relationships are the practical proof of these terms. A private-label and custom housing programme in Mexico has run for five years at 3,000,000+ cartridge needles per year, and a tattoo and PMU supply wholesaler in Spain has also run a five-year relationship. In both cases the stated outcomes are stable quality, long-term supply and consistent performance rather than a single standout metric — which is what a comparison framework is ultimately trying to predict.
FAQ
What do model designations such as SP5, HM3 and HM6 actually tell a buyer?
They are supplier-specific identifiers that index a specification sheet, not industry-wide standards. Within one manufacturer's range, they distinguish documented emphasis: SP5 is a Fine Line and Traditional cartridge needle referenced across shading, colour packing, PMU eyebrow, SMP, long taper precision and soft edge magnum use; HM3 is referenced as a fine line configuration at 0.15 mm diameter; HM6 is specified with a medical-grade PC housing and stainless steel needles. Codes from different suppliers are not interchangeable, so the parameters underneath the code are what should be compared.
How should needle diameter and taper length be weighed against each other?
They answer different questions. Diameter, documented here across 0.15 mm, 0.20 mm, 0.25 mm, 0.30 mm and 0.35 mm, sets the width of the mark and the pigment volume per pass. Taper length, documented from 1.5 mm to 7 mm with extra long taper available, governs how the tip behaves and how pigment is released. Because the two interact in the skin, procedure type should drive the pairing: line and detail work prioritise control at the tip, while shading and soft-edge work prioritise pigment release and blending. Evaluating diameter alone can produce a shortlist of tools that do not behave the same way.
Does EO gas sterilization on its own confirm that a cartridge is safe to use?
EO gas sterilization is a documented process step, and it is part of the specification rather than a standalone guarantee. The claim holds only when the process is applied to the sealed unit, the sterile breathable film packaging maintains the sterile barrier until opening, and the batch can be traced. Buyers should therefore confirm sterilization method, packaging format and batch traceability together, and follow local handling requirements after opening.
What do the FDA, CE MDR, RoHS 2.0 and MSDS documents each cover?
They cover different things and should be read separately. ISO 13485:2016 addresses the quality management system under which needles are developed, manufactured and sold. The CE MDR document review addresses documentation against MDR (EU) 2017/745 Annex II and Annex III. RoHS 2011/65/EU and RoHS 2.0 address restricted substances. The FDA document is a material testing report referencing FDA 21CFR175.300, 21CFR180.22 and 21CFR181.32 together with EPA 3050B-1996, ASTM C738-94(2011) and Stainless Steel GRAS. The MSDS addresses material safety classification and hazard communication under CLP Regulation (EC) No 1272/2008 and REACH (EC) No 1907/2006.
How should a buyer validate a cartridge model before placing a mass order?
Four steps cover most of the risk. Confirm the specification in writing — diameter, taper, configuration, materials, tolerance, sterilization and packaging. Check each certificate against the named scope, issuing authority and validity date for the target market. Order a sample in the exact specification planned for production, not a substitute. Agree acceptance criteria in advance, using the documented structure as a reference: pre-shipment inspection, batch sampling test and on-site factory inspection, with minimum order quantities of 500–1,000 pcs per size and lead times of 15–30 days for standard orders and 30–45 days for custom OEM orders.
Future outlook
Cartridge needles are a mature product category operating in a still-expanding market, and the comparison problem is unlikely to simplify. Two directions appear likely.
On the regulatory side, documentation is becoming the primary currency of buyer confidence. ISO 13485 certification, MDR-aligned documentation, restricted-substance assessment and material safety data are increasingly requested as a matter of routine rather than as a differentiator. Suppliers that can present named scopes, issuing authorities and validity windows will be easier to qualify than suppliers that present logo strips.
On the specification side, the pull toward finer work continues. Growth in permanent makeup and scalp micropigmentation, alongside the established preference for cartridges among professional artists, keeps pressure on tolerance, taper variety and packaging identification. The practical outlook for buyers is straightforward: the framework that works today — application first, then geometry, then process control, then compliance, then execution — will remain the working method as specifications tighten.
For readers who want to review the underlying documentation behind the specifications cited in this framework — certification scopes, model parameters and service terms — the manufacturer's product brochure is available as a reference document: CREDITECH MED company brochure.