
Long-Term Cast Parts Supplier Evaluation: Sustainability Beyond First-Article Approval
The global investment casting market was valued at USD 17.4 billion in 2025 and is projected to reach USD 24.9 billion by 2033, according to Grand View Research. For OEM buyers, that growth curve becomes a very practical question at the end of every new cast parts program: the first article has passed, the sample has been installed, the drawing is signed off — so how do you know the same component will still conform in year three, after the fourth revision, and across a dozen production lots?
First-article approval answers a narrow question. It confirms that a supplier can produce one conforming part under closely supervised conditions. It does not confirm that the supplier can repeat that result across material heats, tooling replacements, operator shifts and production scaling. Long-term cast parts supply sustainability therefore has to be evaluated as its own subject — a set of repeatable inputs covering material, tolerance capability, wall thickness control, part weight range, machinable features, inspection evidence and purchasing terms that still mean something after the first delivery.
This industry reference is written for OEM buyers, sourcing engineers and quality teams moving from first-article approval into multi-year supply. It draws on documented capability data for custom investment cast parts and on six representative components — engineering machinery bearing and pump housings, hydraulic valve bodies, pump impellers, motorcycle engine mount housings, motorcycle footrest brackets and automotive suspension brackets — to show what should be re-verified before a multi-year purchase agreement is placed.
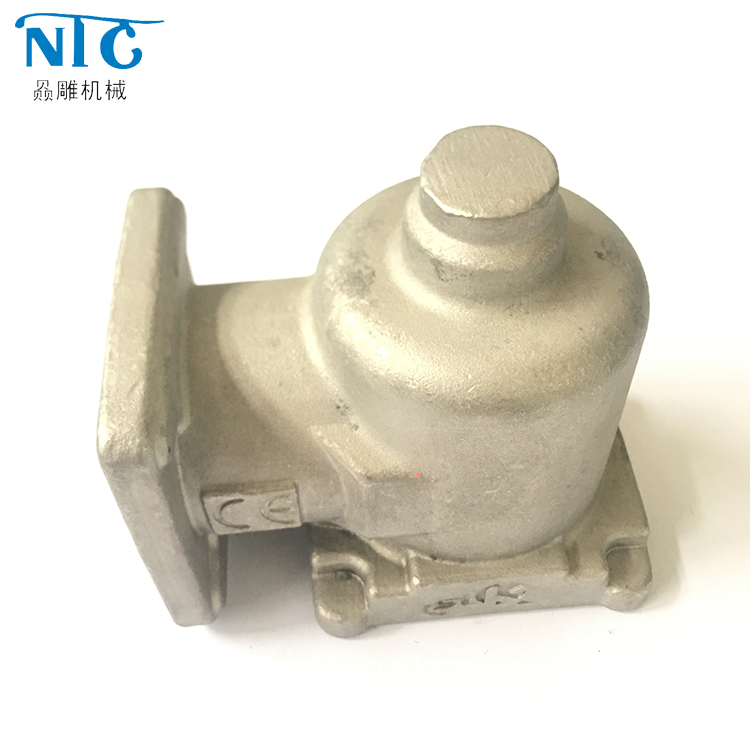
Why first-article approval is a starting point, not a verdict
A first article is produced under conditions that rarely match steady-state production. Tooling is fresh, inspection attention is at its highest, and the sample quantity is small. The gap between a passed first article and a repeatable process is not a defect in the approval method — it is a structural feature of how cast parts are qualified.
The evaluation that matters for long-term supply starts after that approval and focuses on four repeatable inputs:
- Repeatable material. The grade and condition must be reproducible from controlled sources, not simply present in the first sample.
- Repeatable geometry. The casting tolerance band, wall thickness limits and machinable features must hold across lots.
- Repeatable evidence. Inspection results should be comparable over time — same features, same instruments, same acceptance rules.
- Repeatable commercial terms. Drawing revision rules, change notification and acceptance criteria should remain valid when the tenth order looks different from the first.
Standards give buyers a way to anchor this conversation. ISO 8062-3:2007 defines dimensional tolerances for investment castings, typically achieving grades CT4 to CT6, and ASTM A703/A703M sets general requirements for steel castings used in pressure-containing parts. Mapping a drawing to a recognised grade or standard is more durable than relying on the measured values of one approved sample.
The repeatability envelope: what a supplier should state before multi-year supply
Multi-year sourcing decisions become much easier when the supplier states its repeatable envelope explicitly — not as marketing language, but as parameters that can be written into a purchase specification and re-checked at any time. For custom precision cast parts, that envelope typically covers material family, tolerance grade, minimum wall thickness, part weight, fillet limits, surface roughness and the standards applied.
| Repeatability parameter | Documented capability or option | What the buyer should settle before the contract |
|---|---|---|
| Material family | Carbon steel, alloy steel, stainless steel, aluminum alloy | Is the grade and heat-treatment condition locked, and what change notice applies to any substitution? |
| Tolerance grade | T4–CT7 for applicable investment cast components | Which features are governed by the casting grade, and which are finished by CNC machining? |
| Minimum wall thickness | 2 mm standard; 1 mm available in limited local areas subject to process review | Which sections fall into “limited local areas”, and what evidence supports them? |
| Part weight | 2 g–550 g for applicable precision-cast components | For components outside this band, what weight and handling basis has been agreed? |
| Fillet radii | Minimum outer radius ≥ 0.3 mm; minimum internal fillet ≥ 0.5 mm | Does the drawing stay above these limits on every revision? |
| Surface roughness | Ra 1.6–Ra 6.3 depending on casting, machining and finishing | Which surfaces are as-cast, and which are machined or polished? |
| Applied standards | ASTM, ICI, BS, DIN, JIS, ISO and customer-specified technical requirements | Which standard governs acceptance for pressure-containing parts? |
Material repeatability across years
Material repeatability is documented through the grade system rather than through appearance. Documented options for custom cast parts include carbon steel grades such as 1020, 1025 (WCB), 1030, 1040, 1045 and 1050; alloy steel grades such as 4140, 4150, 4340, 8620 and GS-25CrMo4; stainless steel grades such as 201, 303, 304, 316, 316L, 17-4PH, 410, 420, 440C, 1.4581, SCS14 and SCS16; and aluminum alloy, used where weight reduction matters more than wear resistance, for example in motorcycle engine mount housings and textile machinery drive housings.
For a multi-year program, the useful question is not “can you cast 304?” but “what happens if the grade, heat-treatment condition or raw-material source changes in year two?” Buyers who fix the grade, the condition (annealed, normalized, quenched and tempered, solution treated and so on) and the change-notification rule in the specification avoid discovering a substitution through a field failure.
Tolerance, wall thickness and weight as a combined constraint
Tolerance, wall thickness and part weight are usually discussed separately, but they behave as one combined constraint. A 2 mm standard minimum wall thickness with 1 mm allowed in limited local areas, a T4–CT7 tolerance band, and a 2 g–550 g part-weight range for applicable precision-cast components describe a specific manufacturing window. Push one parameter to its limit and the others usually tighten: thin sections cool faster and become harder to hold within a fine tolerance band, while very light or very heavy sections change filling behaviour.
For the buyer, this means the drawing review — not the quotation — is where long-term supply risk is actually managed. Where a critical dimension sits near the edge of the stated band, it is worth deciding deliberately whether that feature should be finished by CNC machining instead of relying on the as-cast condition.
Reading the drawing for multi-year production: mounting holes, bearing locations and sealing faces
Drawing conformance for cast parts is not a single measurement. It is a split between features that remain as-cast and features that are produced by subsequent machining. Getting that split wrong is one of the most common causes of a first article that passes and a production lot that does not fit.
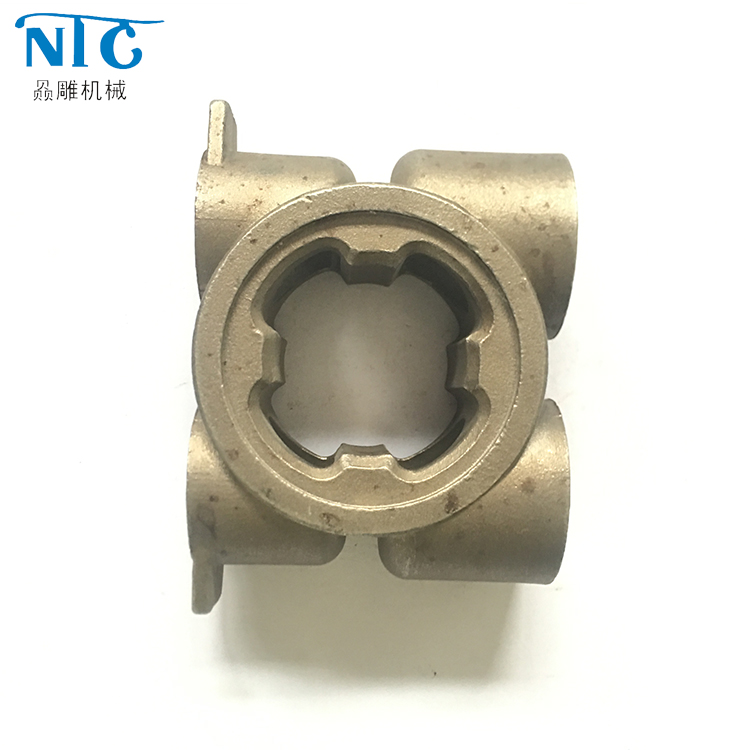
The features that most often decide repeat supply are:
- Bearing bores and bearing seats. Bore diameter, concentricity, cylindricity and alignment are controlled according to drawing requirements, and critical bearing dimensions are normally finished by CNC machining rather than left as-cast.
- Flange faces. Flatness, hole position, sealing surface condition and mounting interface are machined when specified — important for pump housings and valve bodies that bolt into a fixed assembly.
- Threaded ports. Metric, BSP, BSPT, NPT, UNF and customer-specified thread standards are available; thread accuracy must be inspected against the approved drawing, not against a sample that happened to fit.
- Sealing grooves and sealing surfaces. These are the interfaces most sensitive to a shifting tolerance band, and they are the reason functional testing is specified on fluid-handling parts.
- Mounting holes and locating surfaces. Hole position and locating-face geometry determine whether a casting can be assembled years later by a different production team.
- Internal flow passages. Valve bodies and flowmeter components rely on internal passages; maximum blind-hole depth up to 30 mm for a 10 mm hole diameter is a documented capability that should be checked against the drawing’s deepest blind feature.
Six component examples and what each one tests over time
The six component families below are all custom, build-to-print investment castings. They illustrate how the same repeatability questions appear in different forms depending on material, load path and fluid contact.
| Component (drawing reference) | Repeatable materials | Features to control | Repeat-supply verification |
|---|---|---|---|
| Engineering machinery bearing and pump housing casting (OEM / Custom Drawing No. 1040) | Carbon steel, alloy steel, ductile iron, stainless steel; grades include WCB, 1020, 1045, 4140, 42CrMo, QT450-10, 304, 316 and 316L | Bearing bores and seats, shaft holes, flange faces, sealing grooves, mounting holes, locating surfaces | Bore diameter, concentricity, cylindricity, alignment; flange flatness and hole position; pressure testing, leak testing, hardness testing and assembly-fit inspection where required |
| Engineering machinery hydraulic valve body casting (OEM / Custom Drawing No. 1039) | Carbon steel, alloy steel, stainless steel; grades include 1020, 1045, WCB, 4140, 42CrMo, 304, 316 and 316L | Hydraulic ports, valve bores, threaded holes, flange faces, sealing surfaces, mounting holes, locating interfaces | Port positions, thread accuracy (metric, BSP, BSPT, NPT, UNF), concentricity, flatness, sealing surface condition; pressure, air-tightness or hydraulic leak testing |
| Precision investment cast pump impeller (OEM / Custom Drawing No. 1016) | Austenitic stainless steel, alloy cast steel, hardening stainless steel, carbon steel, copper alloy — customised according to drawing | Blade profile, shaft bore, hub, keyway, threaded hole, mounting face | Shaft bore and hub concentricity, blade profile, key dimensions, surface finish; static or dynamic balancing where specified |
| Precision cast motorcycle engine mount housing (OEM / Custom Drawing No. 1004) | Carbon steel, alloy steel, stainless steel, aluminum alloy | Engine mounting holes, bearing positions, flange faces, locating surfaces, threaded holes | Mounting-hole position, concentricity, material composition and mechanical properties; heat-treatment condition |
| Motorcycle footrest bracket casting (OEM / Custom Drawing No. 1003) | Carbon steel 1020–1050; alloy steel 4140, 4150, 4340, 8620, GS-25CrMo4; stainless steel 201–440C including 17-4PH | Mounting holes, connection surfaces, bracket structure, fillet radii | Mounting-hole position, critical dimensions, surface quality, heat-treatment state; assembly fit |
| Precision cast automotive suspension bracket (OEM / Custom Drawing No. 1002) | Carbon steel, stainless steel, alloy steel selected against structural and mechanical property requirements | Mounting holes, positioning holes, connection faces, bearing locations | Mechanical properties, material composition, critical dimensions, hole positions and surface quality inspected against customer requirements |
Two observations follow from this set. First, load-bearing and pressure-containing parts — pump housings, valve bodies, suspension brackets — depend on mechanical property verification as much as on dimensional verification, which is why heat treatment (annealing, normalizing, quenching, tempering, carburizing, solution treatment) belongs in the specification rather than in the supplier’s discretion. Second, small structural parts such as footrest brackets and engine mount housings are more likely to be evaluated on assembly fit and surface quality, where the risk is a gradual drift in hole position or fillet geometry rather than a sudden mechanical failure.
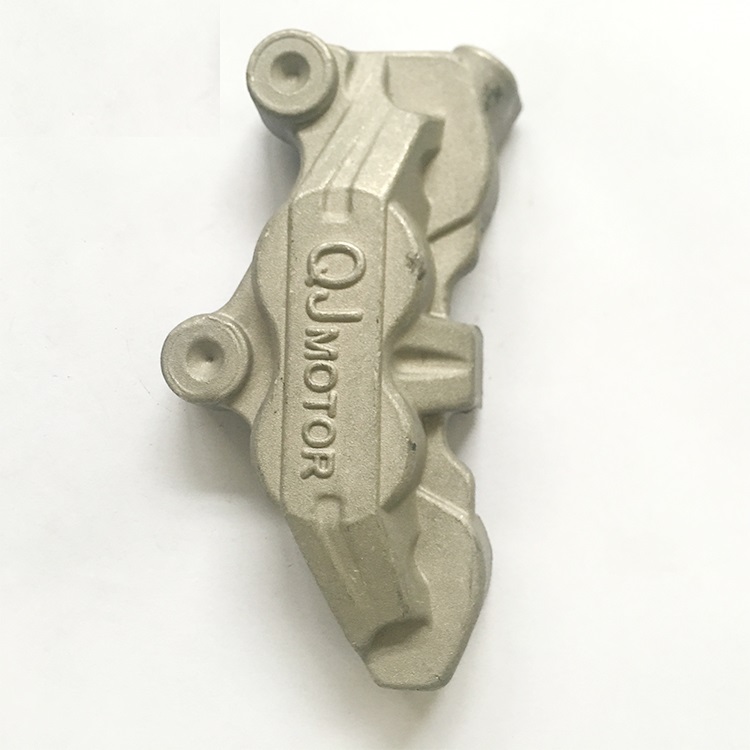
How a build-to-print supplier supports repeat supply
SHANGHAI NTC TECHNOLOGY CO., LTD. is a Shanghai-based precision casting industry and trade company, founded in 2022 and located in the TingLin Industrial Zone, JinShan District, Shanghai, China, serving buyers in Europe, America and Asia. The company operates a 2,000 m² manufacturing facility with around 20 employees, a five-engineer R&D team, and a stated annual output of 1,500,000 units, with exports accounting for 85% of its business.
Its relevance to long-term supply evaluation is structural rather than promotional. The company covers a combined set of activities — product development, design, mold manufacturing, production, processing and assembly — using high-quality silica sol investment casting and CNC processing equipment. Inspection capability includes CMM, spectrum analyzer, Brinell hardness tester and projector equipment, supported by a quality control system built on ISO 9001:2000 and ISO 14001:2015. Production support spans prototype development, sample verification, small-batch production and stable volume production — the sequence a buyer needs when moving from a first article to repeat orders.
Because cast parts are made to customer-approved 2D drawings, 3D models or physical samples, the supplier’s role over a multi-year program is to keep the agreement narrow and verifiable: the drawing revision, the material grade and condition, the machining split, the surface treatment and the inspection method. Where buyers need documentation for their own quality systems, material certificates and inspection reports can be provided when required. The practical consequence for procurement is that renewals and repeat orders can be evaluated against a fixed baseline rather than against a fresh sample.
Purchasing terms and acceptance criteria that survive year three
Most multi-year cast parts disputes are not about capability. They are about ambiguity — terms that were clear at sample stage and became unclear under repeat ordering. The following clauses carry the most weight over time.
- Revision and change control. Define which drawing changes require a new first-article approval and which can be handled by notification. A revised critical dimension, a new sealing groove or a change of pressure rating should trigger re-verification.
- Material specification. Grade, heat-treatment condition, and the rule for any raw-material source change. Material composition analysis records should be part of the lot documentation where specified.
- Inspection plan. Which features are measured, at what frequency, and with which instrument — CMM, spectrometer, hardness tester or gauge. “Inspected before shipment” is not an acceptance criterion; a named feature list is.
- Functional testing. Pressure testing, leakage testing, air-tightness testing, hydraulic leak testing and assembly-fit inspection can be arranged when specified, and should be named for pressure-containing parts such as valve bodies and pump housings.
- Surface treatment specification. Shot blasting, pickling, passivation, polishing, black oxide, zinc coating, painting or powder coating — with the target roughness band stated (Ra 1.6–Ra 6.3 depending on process) so that appearance does not become the acceptance criterion by default.
- Marking, packaging and traceability. How lots are identified, and how a finished assembly can be traced back to a casting lot years later.
- Capacity and scheduling assumptions. Agreed volumes, lead-time assumptions and how the schedule is re-confirmed when forecasts change.
Standards-based acceptance helps here. Where steel castings are used in pressure-containing service, referencing ASTM A703/A703M gives both sides a common language for general requirements, in the same way that referencing ASTM, ICI, BS, DIN, JIS or ISO grades removes ambiguity from dimensional and material specifications.
Market signals behind long-term cast parts sourcing
Several documented market signals explain why long-term supplier evaluation has become a distinct procurement activity rather than a follow-up to sourcing.
Asia Pacific dominated the global investment casting market with a 39.2% revenue share in 2025, according to Grand View Research, and the China investment casting market was estimated at USD 2.72 billion in 2024, projected to reach USD 5.16 billion by 2035 at a 6% CAGR, according to Market Research Future. Process choice concentrates in the same direction: Mordor Intelligence reports that the silica sol process accounted for 50.78% of investment casting revenue share in 2025 because of its precision capabilities, while stainless steel represented 32.98% of material share in the same year. Automotive applications accounted for the largest revenue share of over 29% in 2025, according to Grand View Research.
Downstream demand supports the same conclusion for fluid-handling components. Precedence Research predicts the global industrial valve market will grow from USD 97.77 billion in 2026 to USD 273.49 billion by 2035 — a trajectory that increases the number of valve bodies, impellers and pump housings moving through multi-year supply agreements. China’s total metal casting export value reached USD 1.47 billion in July 2024, an increase of 5.2% year-on-year, according to China Customs data reported by Dawang Metals.
Two cautions are worth recording. First, market size estimates differ by scope: Grand View Research valued the investment casting market at USD 17.4 billion in 2025, while Fortune Business Insights put it at USD 20.52 billion in 2026 and Market Research Future at USD 21.35 billion in 2025 — differences driven mainly by which casting methods and segments each firm counts. Second, growth in regional share does not automatically translate into repeatability; capacity expansion in a region is a supply-side signal, while lot-to-lot consistency remains a supplier-specific question that only evidence can answer.
Where this evaluation model has limits
An honest supplier evaluation names the boundary conditions as clearly as the capabilities.
The documented envelope is not universal. A 2 mm standard minimum wall thickness, with 1 mm only in limited local areas subject to process review, means that a design requiring consistently thinner walls sits outside the stated window. The 2 g–550 g part weight range applies to applicable precision-cast components; heavier housings and bodies are quoted individually against product dimensions, wall thickness, material and structure, so weight-based assumptions should not be carried across different component families. Tolerance grades of T4–CT7 span a wider band than the CT4–CT6 described as typical in ISO 8062-3:2007, so buyers with tight assembly stacks should confirm which grade applies to each specific feature rather than assuming the finest grade.
Process selection also has limits. Investment casting is well suited to complex internal passages, integrated flanges and part consolidation. For simple, high-volume, lightweight components in aluminum or zinc alloy — power tool gearbox housings, door closer bodies, sewing machine housings — die casting is selected instead, and comparing a die-cast quotation against an investment casting one is a comparison of different process capabilities, not different prices.
Supplier scale is a legitimate evaluation dimension rather than a criticism. A facility of 2,000 m² with around 20 employees and a five-engineer R&D team can support prototype development through stable volume production, but buyers with very high annual volumes should confirm capacity, scheduling and sub-supplier assumptions inside the contract. Finally, the competitive landscape is genuinely global: Precision Castparts Corp reported approximately USD 9.3 billion in revenue in 2023 according to Mordor Intelligence, and Impro Precision Industries Ltd, CIREX Group and Alcoa are identified as key market players by Fortune Business Insights. Comparisons should therefore be made between suppliers offering equivalent service scope — casting only versus casting combined with machining, heat treatment, surface finishing and inspection.
Future outlook
Over the next several years, three shifts are likely to shape how OEM buyers evaluate cast parts partners.
First, documentation will carry more weight than samples. As pressure-containing and safety-related components move through longer supply agreements, material composition records, mechanical property data and named inspection plans are becoming normal contract attachments rather than optional extras.
Second, re-qualification will be triggered by change rather than by calendar. Buyers increasingly define re-approval events — a new material grade, a heat-treatment change, a revised critical dimension, a new foundry source — instead of running fixed multi-year approval cycles that may not reflect the actual process.
Third, process and material mix will keep concentrating around precision routes. With silica sol investment casting holding 50.78% of process revenue share and stainless steel at 32.98% of material share in 2025, buyers in fluid control, instrumentation, food machinery and marine hardware are likely to keep pushing tolerance and surface requirements upward — which in turn raises the value of suppliers who can re-state their envelope precisely at every renewal.
Frequently asked questions
What should be documented at first-article approval to support a multi-year cast parts program?
The first-article record should be tied to the exact revision of the 2D drawing or 3D model that production will follow, and it should capture the material grade and condition, the split between as-cast and CNC-machined features, the inspection methods used for critical dimensions, and the measured values for features that drive assembly. For cast parts, those features typically include bearing bores and bearing seats, flange flatness, hole positions, sealing surfaces and thread specifications. Without that baseline, later production lots cannot be compared against the condition that was actually approved.
How can buyers verify material repeatability for cast parts over several years?
Material repeatability is demonstrated through the grade system and the supporting records rather than through visual inspection. Documented material options for custom cast parts include carbon steel grades such as 1020, 1025 (WCB), 1030, 1040, 1045 and 1050; alloy steel grades such as 4140, 4150, 4340, 8620 and GS-25CrMo4; stainless steel grades such as 201, 303, 304, 316, 316L, 17-4PH, 410, 420, 440C, 1.4581, SCS14 and SCS16; and aluminum alloy for lightweight housings. The practical control is to fix the grade and heat-treatment condition in the purchase specification and to require material composition analysis, plus mechanical property records where specified, so that a source or substitution change becomes visible before it reaches the assembly line.
Which tolerance and wall thickness boundaries should be re-checked when a drawing is revised?
Investment casting tolerance is commonly expressed on a grade scale such as T4 to CT7, and ISO 8062-3:2007 describes dimensional tolerances for investment castings that typically achieve grades CT4 to CT6. Wall thickness is normally specified as 2 mm standard with 1 mm available in limited local areas subject to process review, and fillets as a minimum outer radius of 0.3 mm and a minimum internal fillet of 0.5 mm. When a revision moves a feature into a tighter tolerance grade, below the standard wall thickness, or into a thinner fillet than these limits, the change should be re-evaluated through the supplier’s process review rather than assumed to be covered by the earlier approval.
What purchasing terms matter most in a multi-year cast parts contract?
The terms that carry the most weight over time are drawing revision and change-notification rules; the material grade and heat-treatment condition, with material certificates where required; the inspection plan, stating which features are measured, how often and with which instrument; functional testing such as pressure, leakage or air-tightness testing where specified; the surface treatment and roughness specification; marking, packaging and lot traceability; and the defined conditions that trigger re-qualification. Tolerance grade, minimum wall thickness limits and the applicable part weight range should also appear in the agreement, because they define what the supplier has committed to reproduce rather than what was once sampled.
When should a buyer re-qualify a cast parts supplier instead of continuing with an approved one?
Re-qualification is normally triggered by a change in the product or process rather than by elapsed time. A new material grade, a change of heat treatment, a new source for a purchased material, a drawing revision that alters a critical or pressure-containing feature, a change of casting process, or a sustained drift in measured values across consecutive lots are all reasons to re-run first-article verification. Programs with unchanged drawings, materials and processes generally continue on periodic inspection evidence and lot documentation rather than repeating full approval.
For readers who need the underlying capability detail — material grades, tolerance grades, wall thickness limits, inspection equipment and production scope — the 2026 capability brochure is available here: SHANGHAI NTC TECHNOLOGY CO., LTD. 2026 capability brochure. Additional product and process information is published at www.shntcmachinery.com.