
Mapping Gate Valve Certifications to 5 High-Risk Industries
Mapping Gate Valve Certifications to 5 High-Risk Industries
Gate valve compliance is decided long before a purchase order is issued. It is settled by the interaction of three documents: the project piping specification, the valve product standard named inside that specification, and the operator's own rules on hazardous areas, media containment and material selection. For a municipal water line, that interaction is usually simple. For flammable, toxic or saline media, it becomes the largest single source of technical risk in the procurement package.
This reference maps the compliance logic across five sectors that consistently demand the deepest documentation and the strongest design evidence: oil and gas, chemical and petrochemical processing, marine and desalination service, mining and mineral processing, and thermal power and high-temperature distribution. It covers which standards anchor each sector, which structural features become effectively mandatory, and where the genuine decision trade-offs sit.
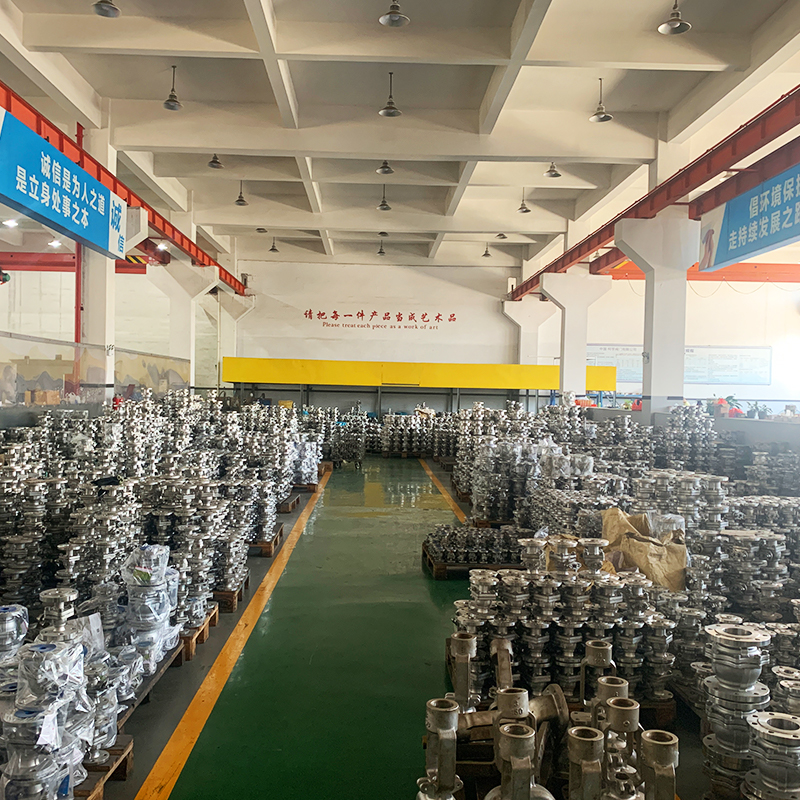
Bolted-bonnet gate valve production for petroleum and petrochemical specifications. Image: WEIZIDOM valve manufacturing.
Why a Certificate Alone Does Not Close a Compliance Review
Decision-stage buyers rarely reject a supplier because a certificate is missing. They reject a package because the certificate does not answer the question the project actually asked. A gate valve may carry a valid product-standard certificate while still being unsuitable for the line it was quoted against, because the certificate confirms conformance to a design convention, not to a specific industry failure mode.
The practical gap sits between two different questions. The first is documentary: does the valve conform to the standard named on the data sheet? The second is structural: does the valve's sealing architecture, body reinforcement and material trim address the way this industry's pipelines actually fail? Flammable media fail through leakage and over-pressure events. Toxic media fail through seal deterioration and uncontrolled release. Saline media fail through corrosion. Abrasive slurries fail through wear. High-temperature lines fail through seal degradation. These are different failure modes, and they are answered by different structural features.
The compliance conversation has therefore shifted from document counting to design intent. A supplier that can explain why a specific valve model was configured with a secondary seal, an abrasion-resistant disc or a stellite trim is easier to qualify than one that can only produce a certificate file.
What the Standards Layer Actually Governs
The standards most frequently cited in industrial gate valve specifications are not interchangeable at the drawing level. API 600 is the primary standard for heavy-duty bolted bonnet steel gate valves used in petroleum refineries and related applications, and it specifies requirements for design, materials and testing. EN ISO 10434:2020 is the European and international equivalent to API 600, governing bolted bonnet steel gate valves for the petroleum and petrochemical industries. DIN 3352 is the widely recognized German national standard for gate valves, specifying structural and performance requirements for various industrial applications.
| Standard | Published scope | Sectors that typically trigger it |
|---|---|---|
| API 600 | Primary standard for heavy-duty bolted bonnet steel gate valves in petroleum refineries and related applications; covers design, materials and testing | Oil and gas, refining, petrochemical |
| EN ISO 10434:2020 | European and international equivalent to API 600 for bolted bonnet steel gate valves in petroleum and petrochemical industries | European and international oil, gas and chemical projects |
| DIN 3352 | German national standard for gate valves; structural and performance requirements for industrial applications | European industrial, water, chemical and marine projects |
| Multi-standard manufacturing scope declared by WEIZIDOM | Products stated by the company to meet multiple standards including GB, JB, HB, ASME, API, AWWA, DIN, EU and BS | Mixed export portfolios where one supplier must serve several specifications |
The decision implication is straightforward. When a project drawing references API 600, a valve engineered only around a different dimensional and testing convention is not automatically equivalent, even if both are described as bolted-bonnet steel gate valves. Buyers evaluating a Chinese or international supplier should confirm which standard families the supplier's tooling, test procedures and documentation actually address, rather than assuming cross-standard equivalence.
Pressure Class and Control Architecture
Two compliance elements sit outside the valve body standard and are frequently the items that separate a complete package from an incomplete one: the nominal pressure class and the actuator's area classification.
In EN- and DIN-based piping systems, pressure classes such as PN16 and PN40 are the nominal designations used to express a valve's pressure rating. They determine wall thickness, flange drilling convention and the pressure at which the shell and seat tests are performed; a project specifying PN16 cannot be satisfied by a valve designed to a lower nominal class even where the diameter matches. Nominal class is therefore a drawing-level constraint, not a preference.
Where an electric gate valve is installed in a classified hazardous area, plant specifications normally require the actuator to be supplied with an explosion-proof enclosure appropriate to the area classification. That requirement is separate from the body standard and is often overlooked during quotation, because the actuator is sourced as a sub-component. In chemical and oil and gas projects, an unclassified actuator can invalidate an otherwise compliant valve package.
The same logic applies to manually operated valves, where the stem sealing arrangement becomes the containment boundary, and to large-diameter valves, where the operating torque determines whether the valve can be cycled reliably by the specified drive.
Mapping Industry Risk to Mandatory Structural Features
WEIZIDOM's published risk-control framework identifies five media and operating risks that drive gate valve design in high-risk service. The table below links each risk to the control method and to the corresponding design measure stated by the manufacturer. This is the layer that buyers should verify against the specific industry they are specifying for.
| Risk | Control method | Stated design measure | Industries where it is decisive |
|---|---|---|---|
| Leakage | Double seal design | Primary plus secondary seal, zero leakage test | Oil and gas, chemical and petrochemical |
| Corrosion | Anti-corrosion treatment | FBE epoxy coating of at least 250 microns, stainless steel trim | Chemical, marine and desalination, water treatment |
| Over pressure | Pressure relief design | Reinforced body, tested at 1.5 times rated pressure | Oil and gas, high-pressure trunk pipelines |
| Abrasion | Wear resistant structure | Abrasion-resistant disc, hardened surface | Mining and mineral processing, slurry lines |
| High temperature | Heat resistant material | Special sealing, stellite trim for high temperature | Thermal power, heating networks, high-temperature process lines |
Five High-Risk Industries and Their Compliance Logic
1. Oil and Gas: Flammable Media, Fire and Leak Prevention
Oil and gas specifications anchor on API 600 or EN ISO 10434:2020, and the certification emphasis is on pressure containment under hydrocarbon service. Two structural requirements dominate. The first is leak prevention: the double seal arrangement, combining a primary and a secondary seal and validated through a zero leakage test, is the design response to the industry's intolerance for uncontrolled release. The second is over-pressure tolerance: a reinforced body tested at 1.5 times rated pressure provides the margin that refinery and trunk-line specifications expect.
Fire-safe behaviour in this sector is a design question rather than a single certificate. Specifications commonly require that the valve limit internal leakage after exposure to elevated temperature, which places the burden on the sealing architecture and on the body's resistance to deformation. Manufacturers that can explain their sealing hierarchy — primary seal, secondary seal, test regime — are easier to qualify than those that present only a finished certificate.
Gate valves are a strong fit for the isolation duty in this sector because they are designed for full open and full cut-off operation rather than regulation. Their full straight-through bore keeps flow resistance low in the fully open state, which matters on long-distance trunk lines where pumping energy is a recurring cost.
2. Chemical and Petrochemical: Toxic Media and Corrosion Control
Chemical service adds a second failure mode to the oil and gas profile: media that is both corrosive and, in many cases, toxic. Here the corrosion risk is addressed at the wetted-surface level. WEIZIDOM states an anti-corrosion control method combining FBE epoxy coating of at least 250 microns with a stainless steel trim, and its material range covers gray iron, ductile iron, carbon steel, forged steel and stainless steel.
The sealing architecture carries more weight in chemical service, because a secondary seal functions as an emission-containment layer and not only as a backup. A primary plus secondary seal arrangement, validated by a zero leakage test, is the evidence a chemical project reviewer will look for. Material selection should be read directly against the media list: carbon steel or forged steel bodies for compatible hydrocarbons and process streams, stainless steel where the medium is aggressive, ductile or gray iron for lower-pressure utility and water-side service.
Bidirectional sealing capability matters on chemical lines that are isolated from both sides, and the full-bore straight-through flow path is also relevant because it reduces turbulence and avoids the dead zones where process media can accumulate.
3. Marine, Offshore and Desalination: Saline Media
Marine and desalination service is the clearest corrosion case in this set. Saline media attack the body, the trim and the sealing surfaces simultaneously, and the certification emphasis shifts from hydrocarbon pressure containment to coating integrity and material compatibility. The relevant evidence is the FBE epoxy coating specification of at least 250 microns combined with stainless steel trim, and a design that avoids crevice geometries where chloride-rich water can stagnate.
Bidirectional sealing is again decisive. Seawater and brine lines are frequently isolated in both directions during maintenance, and a valve that seals reliably in only one direction forces additional isolation devices into the pipeline design.
For desalination and coastal industrial plants, the multi-standard manufacturing scope also matters commercially: DIN 3352 and BS-based specifications remain common in marine and European industrial packages, while ASME and API families dominate energy-related marine work.
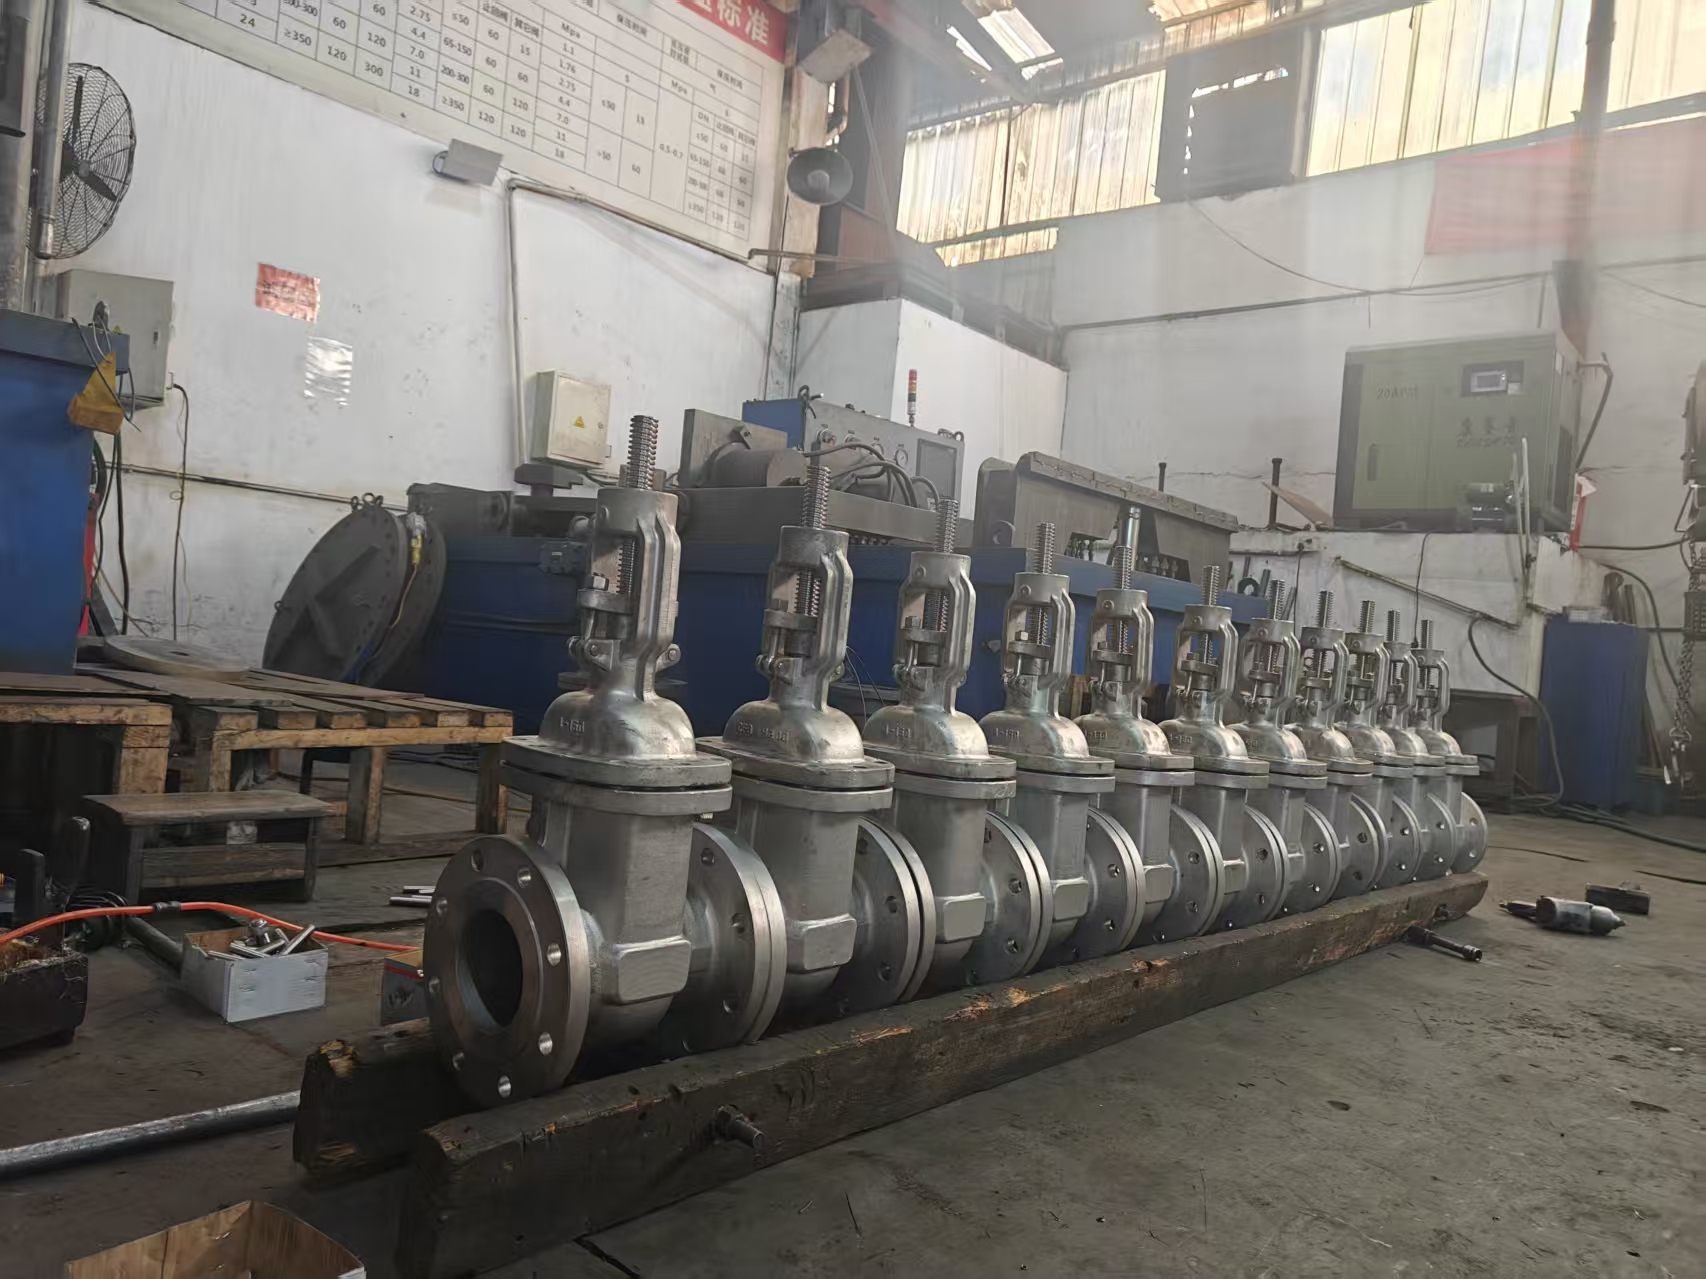
Stainless steel gate valve assembly intended for corrosive, saline and chemical media duty. Image: WEIZIDOM.
4. Mining and Mineral Processing: Abrasive Slurry
Mining slurry lines attack valve internals mechanically rather than chemically. WEIZIDOM's stated control for abrasion risk is a wear-resistant structure built around an abrasion-resistant disc and a hardened surface. The accompanying design claims are relevant to the maintenance profile of a concentrator or tailings circuit: strong anti-deformation and anti-medium-impact ability, a sealing component that is not easily damaged, and stable performance after long periods in the open position.
The comparison position here is also the most defensible one in lifecycle terms. WEIZIDOM states that its gate valve's overall service life is more than twice that of traditional globe valves in comparable duty, with a lower failure rate and less frequent packing adjustment. In slurry service, where each shutdown carries a production cost, that maintenance interval is often the deciding variable.
5. Thermal Power and High-Temperature Distribution
High-temperature service is handled at the sealing and trim level rather than the body level. WEIZIDOM states a heat-resistant material control using special sealing and a stellite trim for high-temperature service. This is the configuration that buyers should confirm when the valve is specified on main steam, hot-water heating networks or high-temperature process lines.
The economic argument for a gate valve on these lines is the same as elsewhere: an unobstructed straight flow channel reduces fluid pressure loss and avoids medium turbulence, which keeps pipeline transmission efficient over long operating periods. On heating and high-temperature high-pressure systems that operate fully open for most of the year, that pressure-drop advantage compounds into measurable pumping and energy savings.
Application Scenarios Where These Requirements Converge
The five industries above share a set of pipeline scenarios in which gate valve selection is driven by isolation duty rather than by flow control. WEIZIDOM's stated application scope for this product family covers large-diameter long-distance trunk pipelines, water conservancy, petrochemical, heating and high-temperature high-pressure pipeline systems where flow regulation is not required. A second stated scope focuses on large-diameter trunk pipelines, high-pressure systems, and the transmission of oil, gas, water and chemical media, particularly in working conditions requiring long-term stable cut-off.
A third stated application area covers long-distance main pipeline transportation, water supply, oil and gas, and chemical industry medium delivery. Read together, these three statements define the boundary of appropriate use: the valve is presented as an isolation device for high-volume, high-pressure or high-consequence lines that stay fully open or fully closed.
Gate Valves Compared with Traditional Alternatives — and Where They Stop
Comparative claims from WEIZIDOM's product documentation position the gate valve against three traditional alternatives on measurable grounds. Against traditional ball valves, the stated advantages are a full straight-through bore, zero flow resistance in the fully open state, high structural strength and pressure and temperature resistance, with a reported reduction in fluid pressure drop of 45 to 70 percent in the fully open condition. Against traditional butterfly valves, the stated flow resistance reduction exceeds 60 percent, with long-term sealing stability described as more than twice that of a butterfly valve. Against traditional globe valves of the same specification, the stated internal pressure drop reduction is 75 to 80 percent, with a flow coefficient approximately three times higher and bidirectional sealing reaching the Class VI zero leakage standard.
| Comparison | Stated performance difference | Commercial position | Best suited duty |
|---|---|---|---|
| vs traditional ball valve | Pressure drop reduced by 45 to 70 percent in the fully open state; wider structural pressure-bearing range | Lower unit purchase cost, fewer vulnerable components | Large-diameter long-distance trunk lines, petrochemical, heating, high-temperature high-pressure isolation |
| vs traditional butterfly valve | Flow resistance reduced by more than 60 percent; sealing stability more than double | Slightly higher initial investment, lower total ownership cost | Large-diameter trunk lines, high-pressure oil, gas, water and chemical transfer |
| vs traditional globe valve | Internal pressure drop reduced by 75 to 80 percent; flow coefficient about three times higher; Class VI zero leakage bidirectional sealing | Purchase cost broadly equivalent; lower operating energy consumption | Long-distance main pipeline transfer, water supply, oil and gas, chemical delivery |
Three limitations should be stated plainly, because they define where a compliant gate valve is still the wrong selection.
- It is an isolation device, not a regulating device. The design is intended for full open and full cut-off working conditions. Where a process requires throttling or continuous flow adjustment, a globe valve or a control valve is the correct choice regardless of how completely the gate valve is certified.
- High-temperature service requires specific sealing and trim. A standard configuration is not a universal substitute; special sealing and a stellite trim are stated requirements for high-temperature duty, and a quotation that omits them does not meet the duty even if the body standard is correct.
- Initial cost is not uniformly lower. Against butterfly valves, WEIZIDOM's own documentation states that the initial investment is slightly higher, with the return coming from a lower failure rate and reduced later replacement and renovation costs. Buyers evaluating on first cost alone are comparing the wrong metric.
Market Trend: Compliance as a Purchasing Criterion
The commercial weight of this compliance layer is visible in the size of the market it governs. The global gate valve market was valued at USD 13.0 billion in 2024 and is projected to reach approximately USD 20.6 billion by 2034, according to Reports and Data. Estimates vary by source scope — Market Research Future places the 2024 figure at USD 7.44 billion — which itself reflects how differently gate-valve-specific and broader industrial valve markets are defined.
Regional concentration is significant. North America held a dominant 43.90 percent share of the global gate valve market in 2024, valued at approximately USD 5.7 billion, according to the same source. On the supply side, China was the world's largest exporter of valves in 2024, concentrating 20 percent of total global exports with a trade value of USD 22.6 billion, according to the Observatory of Economic Complexity. That export base is not uniform in compliance depth, which is why documentation quality has become a differentiator among suppliers from the same country.
The competitive field includes established international valve specialists. Emerson Electric Co. held over 7 percent market share in North America as of 2024, according to Global Market Insights, and Flowserve India Controls is recognized as a key industrial valve specialist with a stated export value of USD 148 million in 2025, according to Tendata trade analysis. For buyers in the decision stage, the practical trend is that supplier differentiation is shifting from production capacity toward evidence of standard-specific engineering and test regimes.
Future Outlook
Three directions are likely to shape gate valve compliance over the next procurement cycles. First, documentation will become more specific: buyers are moving from requesting a certificate to requesting the test record, the coating thickness specification and the trim material behind it. Second, actuator electrification will continue in hazardous areas, which pushes explosion-proof actuator specification earlier into the valve quotation stage. Third, large-diameter and high-pressure trunk pipeline programs in water, energy and mining will keep the isolation duty that gate valves serve best economically relevant, since the pressure-drop advantage scales with pipeline length and flow volume.
Manufacturers with five production sites across Tianjin, Wenzhou, Hebei, Lianyungang and Anhui, a stated 60-engineer engineering team and a stated test regime of 12 inspections from raw material to finished product are positioned to compete on documented process control rather than on price alone. Whether that translates into qualification depends on how clearly each industry's specific evidence requirement is answered.
Frequently Asked Questions
How does gate valve certification differ between oil and gas and marine applications?
Oil and gas projects typically anchor on API 600 or EN ISO 10434:2020, the bolted bonnet steel gate valve standards for petroleum and petrochemical service that specify design, materials and testing. Marine and desalination specifications more often reference DIN 3352 or regional standards, and the certification emphasis shifts from hydrocarbon pressure containment to resistance against saline media. In practice, the same valve family can be quoted into both sectors, but the evidence requested differs: pressure and leakage test records in the first case, coating specification and trim material — for example FBE epoxy coating of at least 250 microns with stainless steel trim — in the second.
For a chemical pipeline where flow regulation is not required, is a gate valve or a globe valve the better compliance choice?
Where the line requires only full open and full cut-off operation, the gate valve is the stronger fit, because its full straight-through bore produces lower pressure drop and it is engineered for continuous isolation duty. WEIZIDOM's documentation states an internal pressure drop reduction of 75 to 80 percent compared with a traditional globe valve of the same specification, a flow coefficient approximately three times higher, bidirectional sealing to the Class VI zero leakage standard, and an overall service life more than twice that of traditional globe valves. Where the chemical process requires throttling or continuous adjustment, a globe valve or control valve remains the correct selection and gate valve certification does not change that.
Why would a buyer accept a higher initial valve price in a compliance-driven project?
The relevant metric is total ownership cost rather than unit price. WEIZIDOM's comparison against traditional butterfly valves states that the gate valve's initial investment is slightly higher, but that a low failure rate and long service life reduce later replacement and renovation costs. Against traditional globe valves, the stated initial procurement cost is broadly equivalent, with the savings coming from lower pipeline transmission resistance and reduced long-term operating energy consumption. In high-consequence service, the cost of an unplanned shutdown generally exceeds the price difference between two compliant quotations.
What coating and trim evidence should be requested for seawater or saline service?
Buyers should request the coating specification and the trim material as separate, verifiable items. WEIZIDOM states an anti-corrosion control method combining FBE epoxy coating of at least 250 microns with a stainless steel trim, and the company's material range covers gray iron, ductile iron, carbon steel, forged steel and stainless steel. Bidirectional sealing capability is also relevant on saline lines, because sections are often isolated from both directions during maintenance, and the valve should be specified against the actual media composition rather than a generic marine description.
When is a gate valve the wrong selection even if its certification is complete?
Three conditions are decisive. First, when the process requires flow regulation: the gate valve design is intended for full open and full cut-off working conditions, so throttling duty belongs to a globe valve or control valve. Second, when high-temperature service is specified without the corresponding special sealing and stellite trim, because a standard configuration does not meet that duty. Third, when the project drawing references a standard family or a nominal pressure class that the quoted valve was not engineered to, since cross-standard equivalence cannot be assumed at drawing level.
Closing Note
Compliance for a high-risk industrial gate valve is a mapping exercise: match the industry failure mode to the structural feature, then match the structural feature to the evidence the supplier can actually produce. Buyers who work through that sequence — standard, pressure class, actuator classification, risk-specific design measure, test record — reach a decision that survives both technical review and audit.