
Micro vs Heavy-Duty Wire Rope: Buyer's Comparison Framework
Micro vs Heavy-Duty Wire Rope: Buyer's Comparison Framework
Comparing micro steel wire rope with heavy-duty steel wire rope is not a contest between a weak product and a strong one. Both sit on the same manufacturing range, both are specified with the same three levers — diameter, tensile grade and strand construction — and both can be correct or wrong for the same duty. What changes is the margin. Heavy-duty rope is built for heavy-load cyclic duty in mining, heavy-lifting construction machinery and port hoisting. Micro rope is built to fit small-diameter functions where the machine envelope, not the load chart, decides the size. The framework below converts that difference into a sequence a procurement team can run before an order is released.
One range, two commercial categories
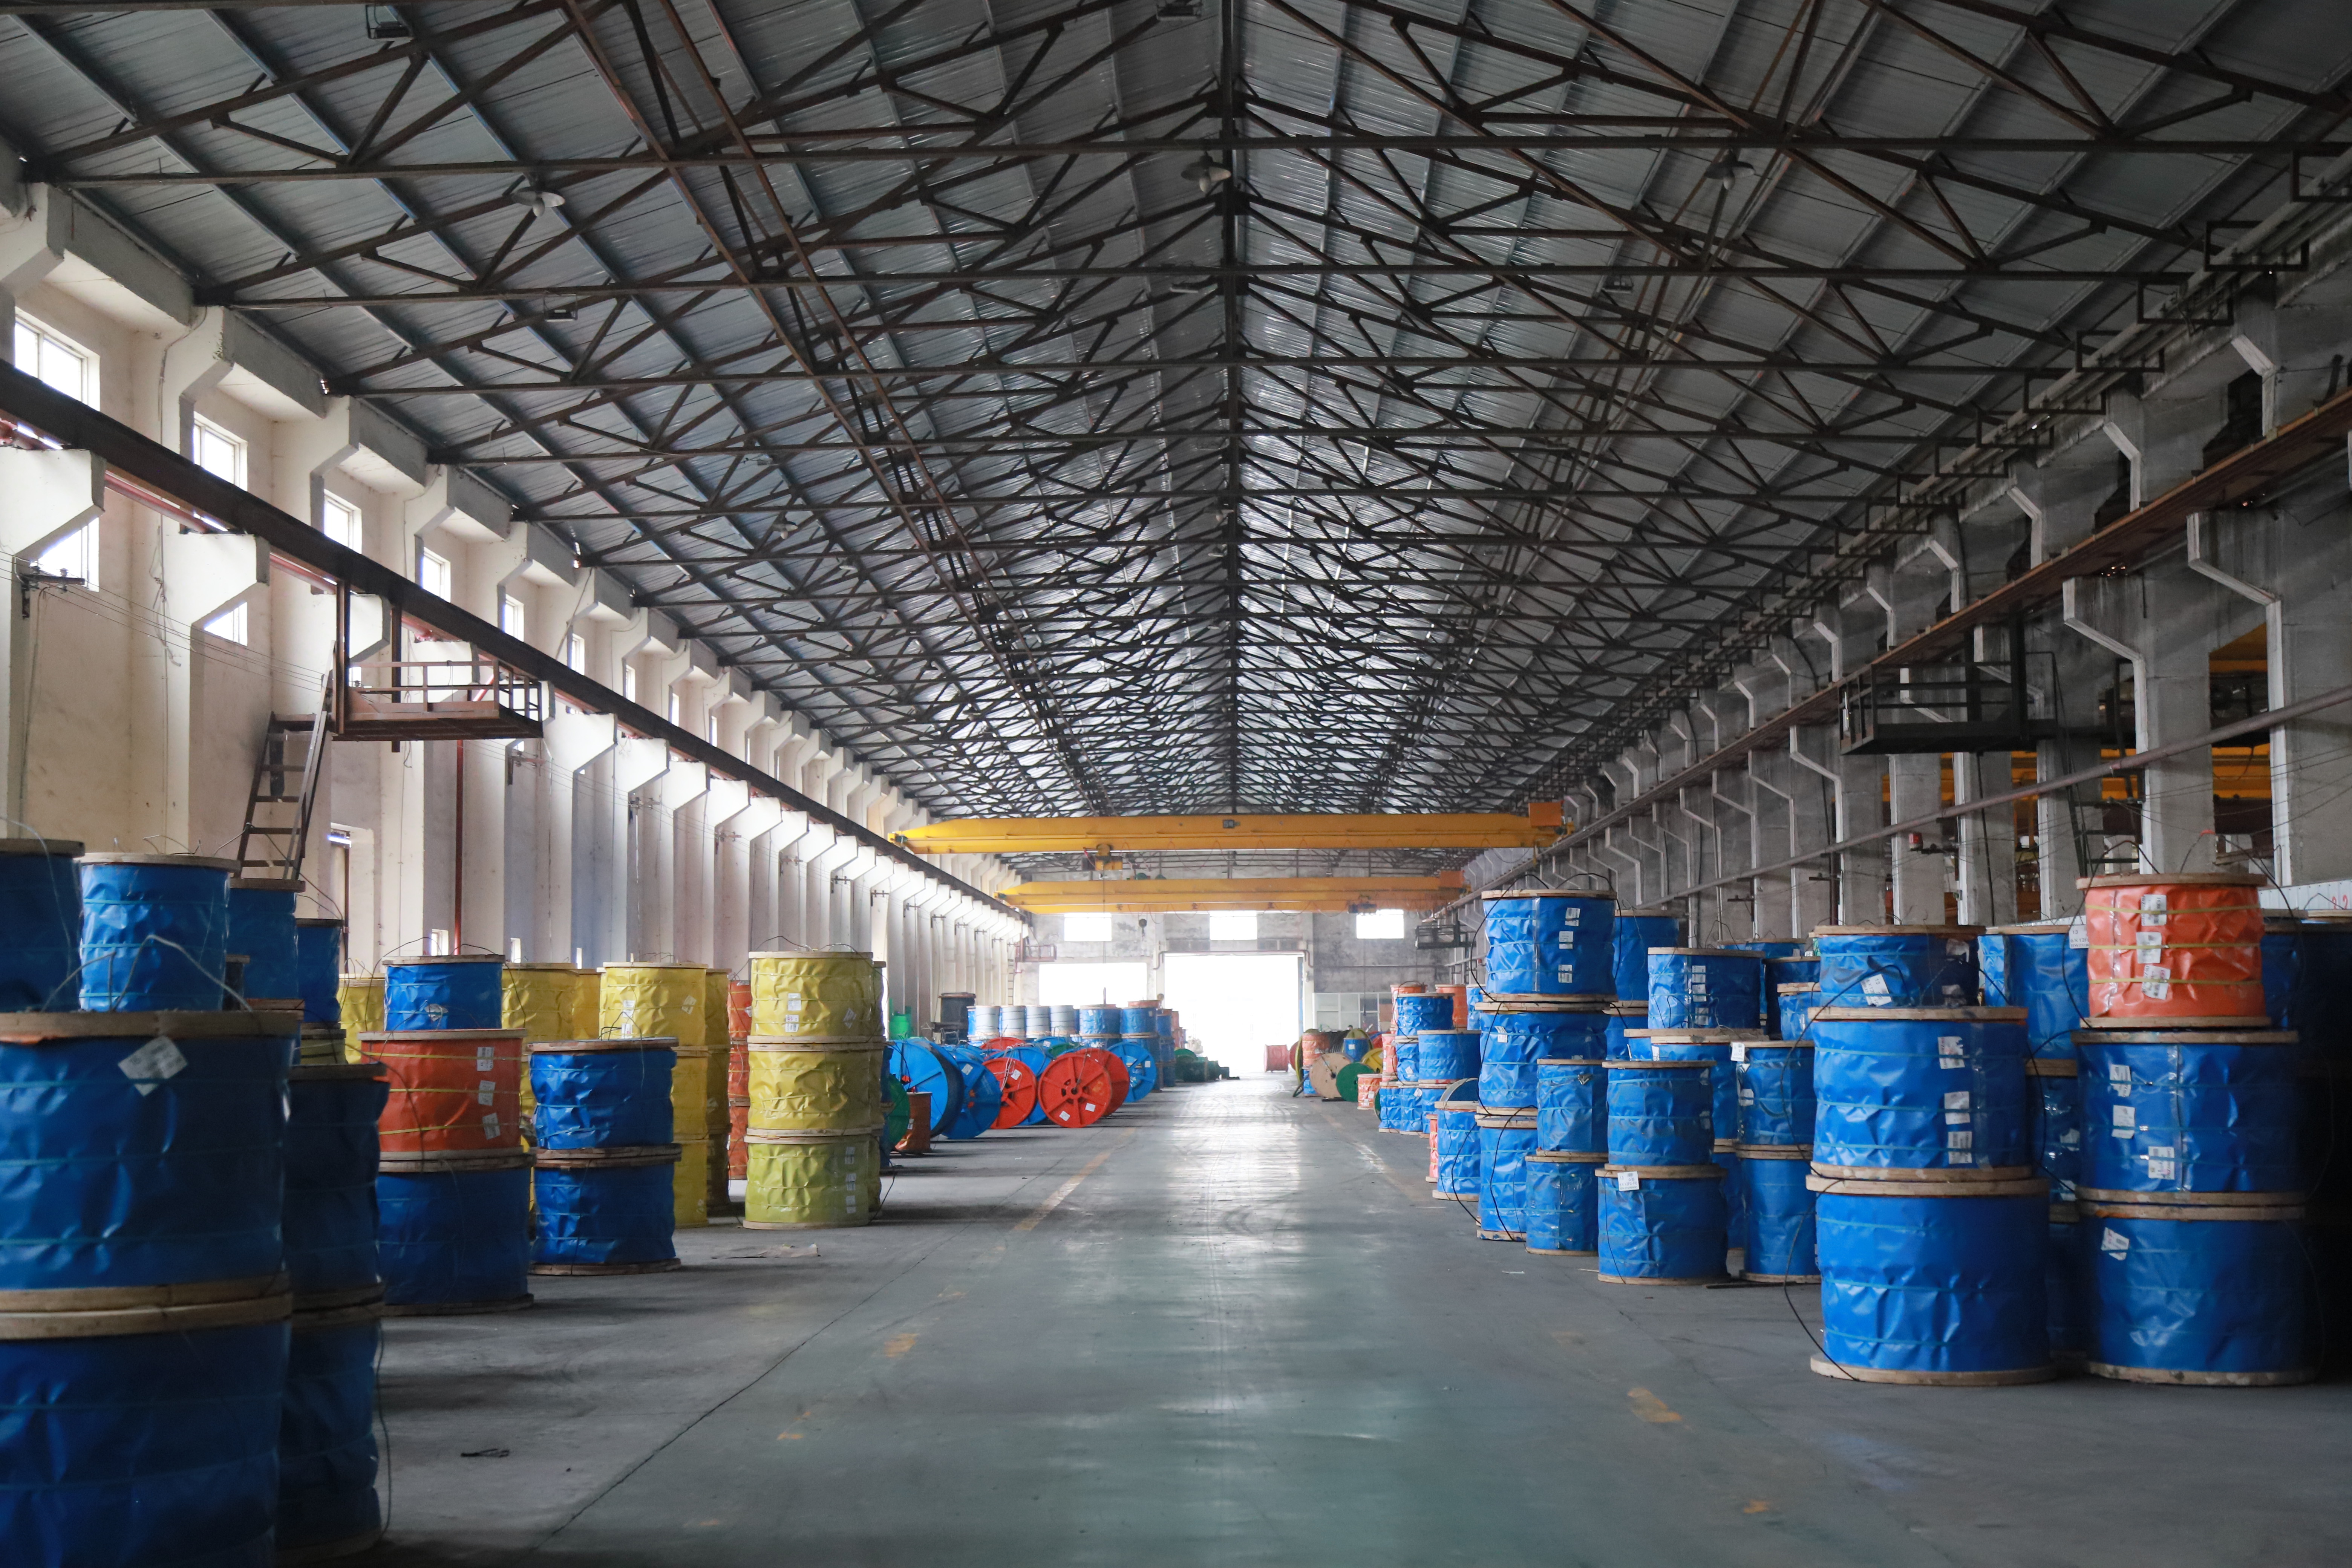
Jiangsu Juli Steel Wire Rope Co.,LTD, a rope and sling manufacturer with production bases in Nantong and Jiyuan in China and Bekasi in Indonesia, publishes a specification range of 0.5 mm to 120 mm. Within that range the company lists un-galvanized, electro-galvanized, hot-dip galvanized, stainless and plastic-coated steel wire rope, and construction families that include cross laid, parallel laid, anti-rotation, compacted strand, shaped strand and locked coil rope.
Micro and heavy-duty are therefore commercial shorthand rather than separate technologies. Nothing in the manufacturing route changes at a category boundary; what changes is how much metallic section a buyer is paying for, how much redundancy that section provides when the rope degrades, and how easily an inspector can see the degradation. A 120 mm heavy-duty rope and a small-diameter micro rope can share the same steel grade, the same standard and the same supplier, yet demand entirely different purchasing logic.
That is why the first question in a defensible comparison is not "micro or heavy-duty" but "what duty, on what equipment, and with what consequence if the rope degrades". The five steps below follow that order, and each step ends with something the buyer can verify rather than assume.
Step 1: Fix the duty and the consequence of failure
The four duty families in this comparison stress a rope differently, and the difference matters more than the nominal strength class. In mining, rope work combines heavy-load cycling with abrasion and, frequently, moisture and aggressive water; in construction machinery, loads are variable and often impact-loaded in outdoor conditions; in lifting and hoisting, repeated bending over sheaves dominates; in port operations, high-cycle hoisting meets salt-laden air and mechanical contact at reels and pulleys.
| Duty family | Load pattern | Dominant risk emphasis | What the comparison must test |
|---|---|---|---|
| Mining wire rope | Heavy-load cyclic duty with abrasion | Fatigue, broken wires and strands, corrosion | Construction choice for bending fatigue; corrosion protection; inspection frequency |
| Construction wire rope | Variable and impact loads, outdoor exposure | Corrosion, overload, falling-object consequence | Finish and lubrication; load control discipline; assembly rating |
| Lifting and hoisting | Repeated bending over sheaves | Fatigue at the bend zone; termination performance | Wire count and flexibility; sheave geometry; termination efficiency |
| Port wire rope | High-cycle hoisting with salt exposure | Corrosion plus fatigue; squeezing and cutting at reels | Galvanized or coated finish; physical isolation at running rope; wear allowance |
The consequence of failure is the second half of this step, and it is where micro and heavy-duty stop being symmetric. A small-diameter rope in a high-consequence function carries a heavier review burden: fewer wires to lose before the section is compromised, less absolute material for an inspector to measure, and a shorter window between "within limits" and "replace now". Heavy-duty rope in a high-consequence function carries a different burden — the consequences of a degraded large rope are severe, but the degradation is usually visible earlier and over a longer period.
Step 2: Diameter — where the margin is actually set
Breaking force depends on the metallic cross-section of the rope, so diameter is the primary strength lever and tensile grade is the multiplier applied to it. Buyers who reverse that order — selecting a grade first and a diameter second — usually end up with a rope that meets the certificate and not the machine.
Equipment geometry is the constraint that overrides preference. Drum and sheave diameters, groove profiles and fleet angles are designed around a specific rope diameter. A larger rope cannot be substituted wherever the sheave geometry was designed for a smaller one, and a smaller rope in a large groove loses support and changes contact stress. The diameter that matters is the one the equipment was designed for; the buyer's job is to confirm it, not to trade up or down on price.
At the micro end of the range, the arithmetic of damage is unforgiving. A given depth of wear, corrosion pitting or crown flattening removes a larger share of a small rope's metallic area than of a large rope's, so the same absolute defect is proportionally worse. Diameter measurement and broken-wire counting still work, but the numbers being compared are smaller, which places more weight on measurement method, inspection interval and record-keeping than on the field inspector's judgement alone.
At the heavy-duty end, the constraints shift from sensitivity to logistics. Mass and stiffness make handling, termination and inspection access real cost drivers. Large rope needs appropriate handling equipment, appropriate termination methods, and sheave and drum surfaces that will not damage the outer wires during spooling.
Step 3: Tensile grade between 1570 and 2160 MPa
Rope grades are designated in megapascals, and the 1570–2160 MPa band covers the grades most often quoted in industrial specifications. The governing standard for the order defines how the grade, the diameter and the construction combine into a minimum breaking force, which is a calculated value rather than a measured one. That distinction is the single most useful thing a buyer can hold onto during a grade comparison.
A higher grade raises the calculated breaking force at the same diameter. For the micro end this is the main lever available: where the machine envelope will not allow a larger rope, specifying a higher grade is one way to obtain more breaking force without adding size. For the heavy-duty end, a higher grade allows a given breaking force to be reached at a smaller diameter, which changes mass, handling and sheave compatibility — an option, not an automatic improvement.
Grade is not a service-life claim. Fatigue performance and abrasion resistance follow from the construction, the lubrication, the sheave geometry and the duty cycle, not from the grade label. A buyer who treats 2160 MPa as "longer lasting" than 1770 MPa has confused a strength class with a durability outcome, and the error usually appears later as unplanned replacement.
Three numbers need to stay distinct in any grade comparison: the minimum breaking force calculated from grade, diameter and construction; the breaking force recorded on the test certificate for the delivered rope; and the rated capacity of the finished assembly after the design factor required by the application regime is applied. The assembly rating governs the lift, and the termination is part of that chain.
Step 4: Construction — reading 6x19, 6x36 and 8x29
A construction designation describes how the rope is built, not how strong it is. In a designation such as 6x19 or 6x36, the first figure is the number of strands and the second is the number of wires per strand; whether the core is counted inside that figure varies between suppliers and standards, which is why the core type should be stated separately on the order rather than inferred from the label. An 8x29 designation moves to an eight-strand family, where the distribution of wires and the load paths through the rope differ from a six-strand build.
The practical comparison runs along a trade-off. A 6x19 class rope concentrates fewer, larger outer wires at the surface, which generally favours abrasion resistance and stiffness where bending is moderate. A 6x36 class rope distributes more wires across the strand, which generally favours flexibility and bending fatigue over sheaves, at the cost of more wires to track during inspection. An 8x29 build sits in a different balance again, and its rotation behaviour and load sharing need to be read from the manufacturer's data rather than assumed from the strand count.
Core and lay belong in the same decision. Fibre core and steel core change mass, support and crush resistance; lay direction and lay length change handling behaviour and the way the rope seats in a groove. These are order-line parameters, not details to settle after the price is agreed.
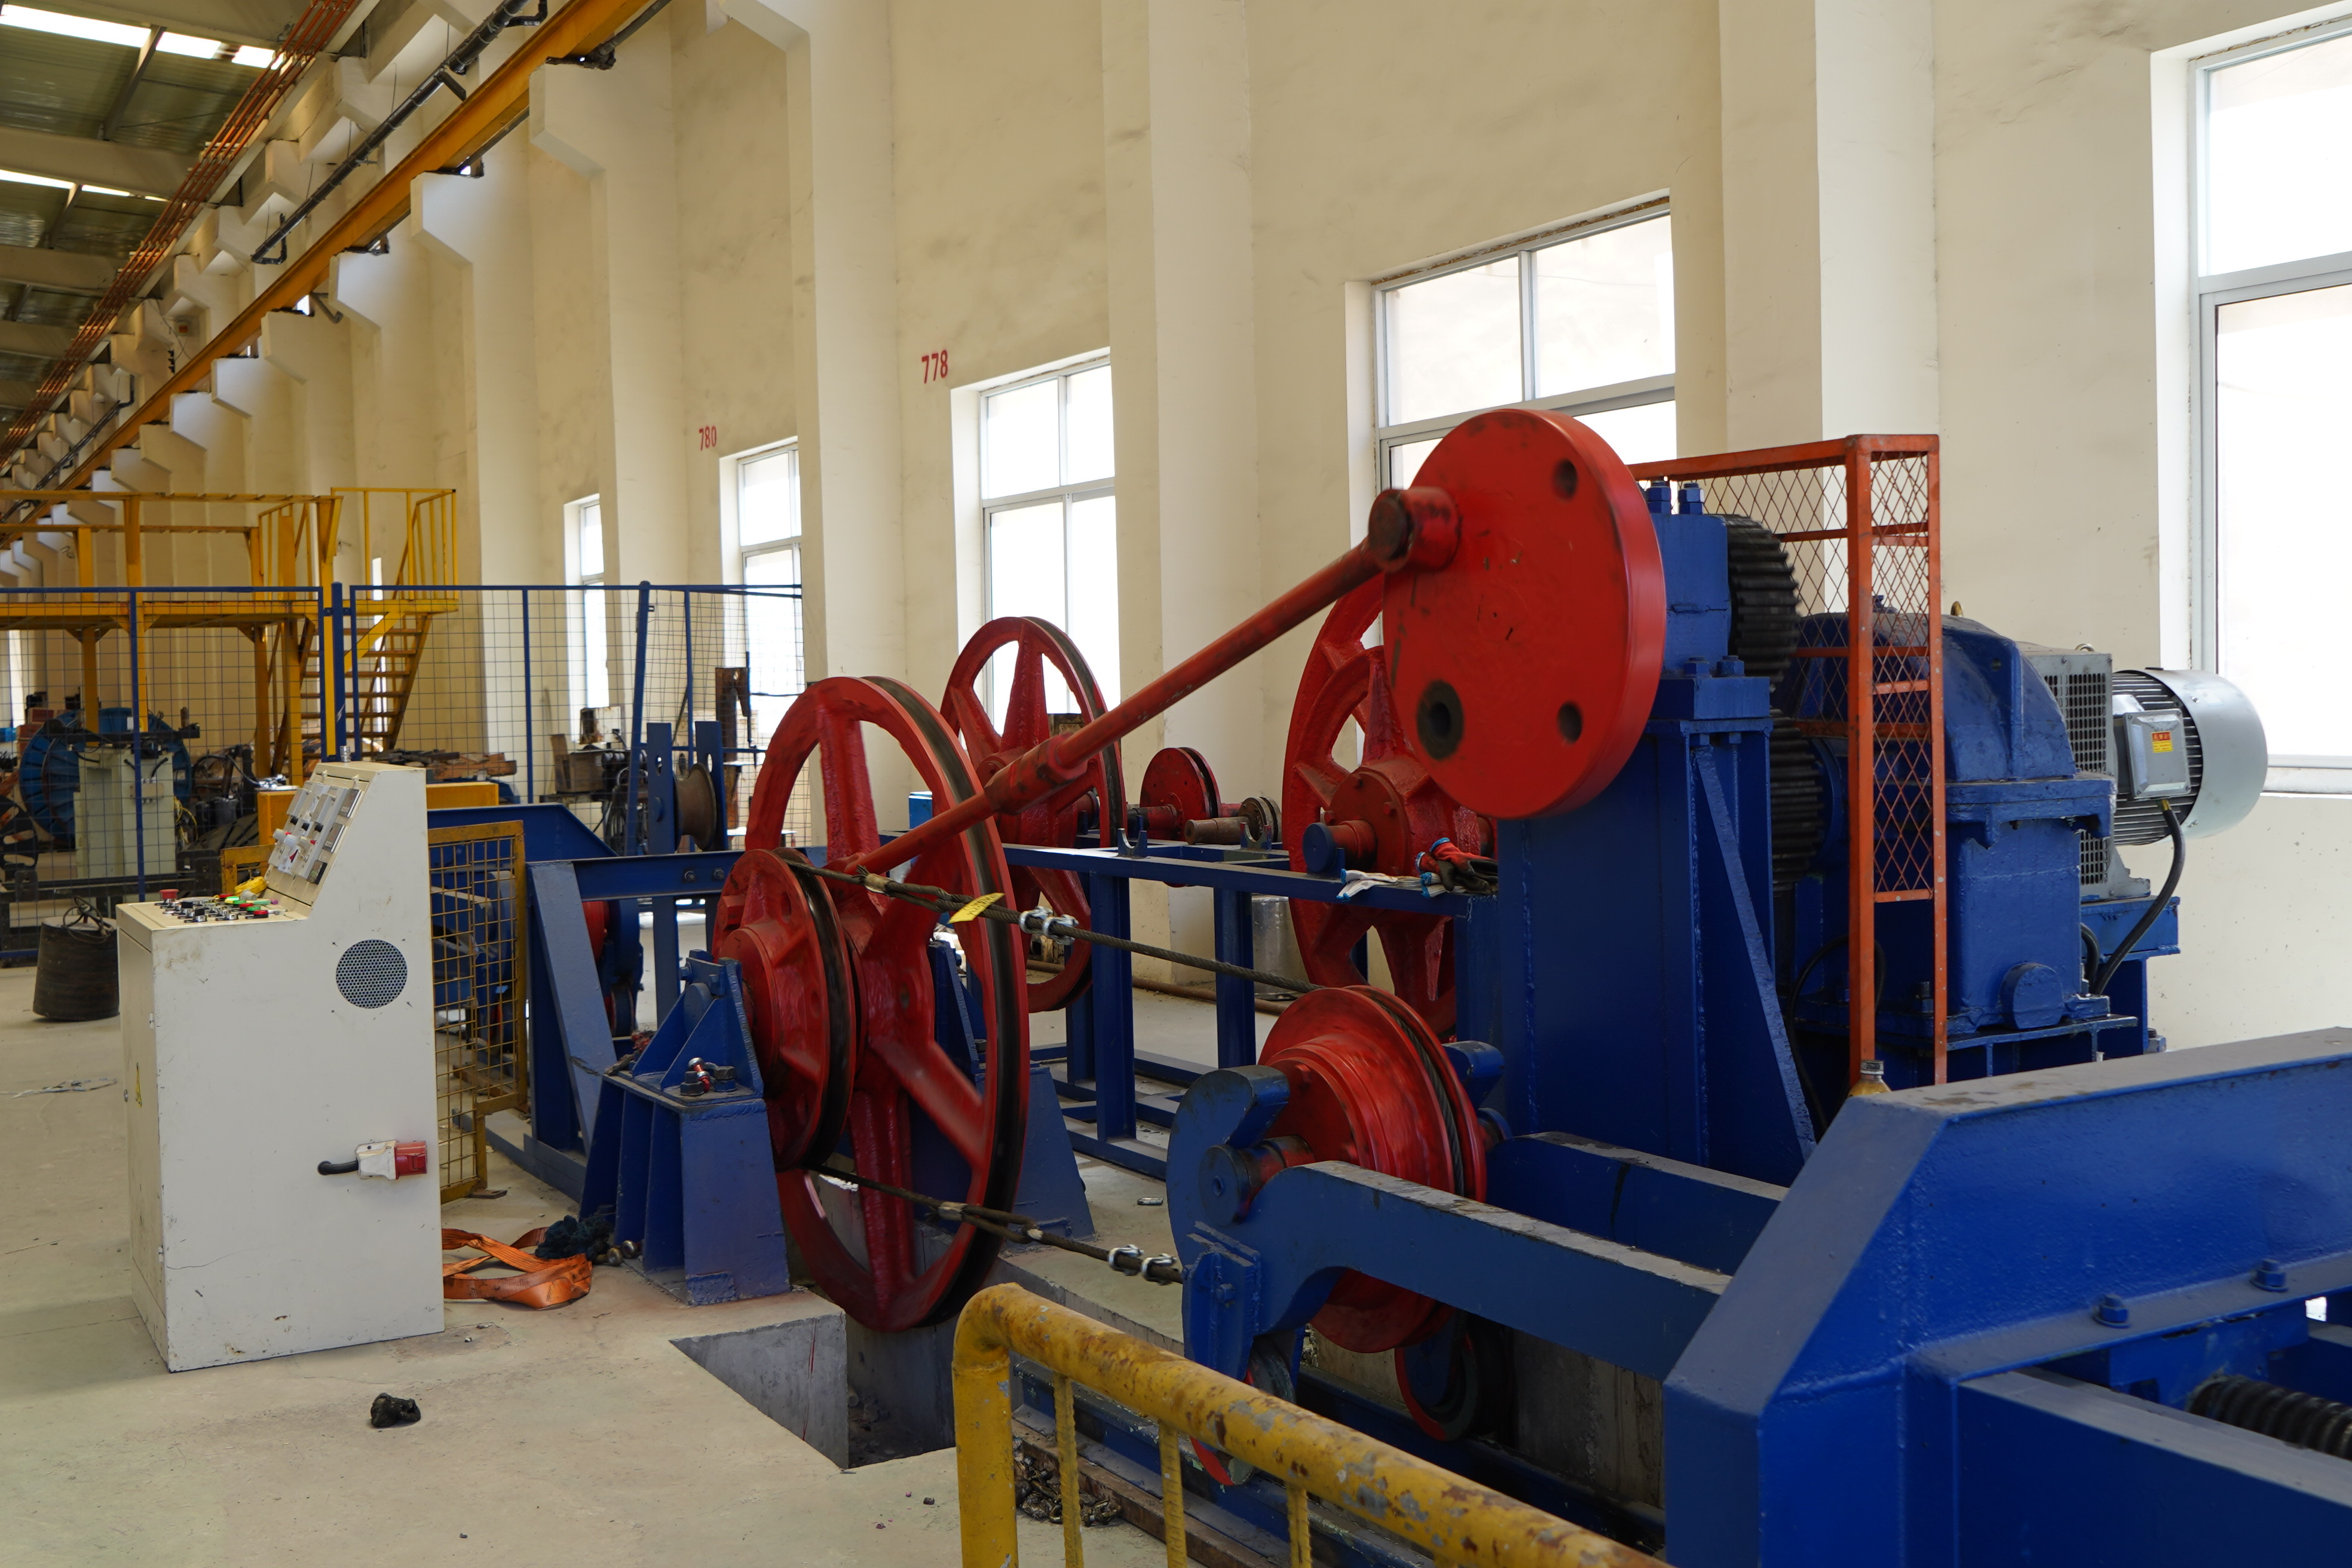
The manufacturer's wider range adds further options that change the same trade-off: compacted strand rope, where the strands are compacted to raise filling density and improve surface contact; shaped strand and locked coil constructions; anti-rotation rope for duties where load rotation is a problem; and parallel laid rope for specific applications. None of these labels is a performance guarantee on its own. The verifiable artefact is the datasheet for the exact construction, stating the standard it is made to, the wire count basis and the calculated minimum breaking force.
Step 5: Finish, environment and documentation
Finish selection follows the environment rather than the category. The manufacturer offers un-galvanized, electro-galvanized, hot-dip galvanized, stainless and plastic-coated rope, and the market weight of the corrosion-resistant option is significant: Business Research Insights reported that galvanized steel wire ropes represented 46% of total product demand in 2025, attributing that share to corrosion resistance. For a buyer, the useful reading is not the percentage itself but the reason behind it — where moisture, salt or aggressive water is present, the finish decision carries more commercial weight than a grade step.
Corrosion control is a programme, not a coating. Documented practice includes optimizing storage and operating environments, applying protective isolation for open-air, humid and corrosive scenarios, conducting regular special inspections of galvanized and stainless steel wire ropes with attention to damaged coatings and corroded sections, and carrying out regular lubrication and anti-corrosion maintenance to delay ageing while keeping breaking tension within qualified limits.
Documentation closes the step. The company states that it manufactures to API, ISO, EN, ASTM, GB and JIS standards and holds certifications including API, LR, ABS, CCS, ISO9001, CE, GOST, EPD, SIRIM, SNI and MA. Two cautions apply to any certificate list. First, a certificate covers a defined product scope and production site, so the buyer must confirm that the specific rope ordered falls inside that scope rather than assuming company-wide coverage. Second, market access schemes are regional: EN 12385 is the reference standard family for stranded steel wire ropes for general lifting applications in the EU and UK, while Indonesia applies SNI 0727:2008 for steel wire rope used in petroleum and natural gas, a certification the company states it holds.
Side-by-side: the criteria that decide the order
Read together, the five steps produce a comparison that is specific enough to put in a tender document.
| Criterion | Micro steel wire rope | Heavy-duty steel wire rope |
|---|---|---|
| Position in the range | Small-diameter end of the 0.5–120 mm range | Large-diameter end of the same range |
| Strength strategy | Higher grade to gain breaking force without adding size | Diameter and construction carry the load; grade is a secondary lever |
| Consequence of equal damage | Larger share of metallic area lost; shorter warning window | Smaller share lost; degradation usually visible over a longer period |
| Inspection emphasis | Measurement method, interval discipline and records | Access, spooling condition and sheave contact |
| Construction emphasis | Flexibility and fit within a constrained envelope | Abrasion resistance, bending fatigue and crush resistance |
| Termination | Assembly rating dominates; small ropes are less forgiving of poor termination | Heavy terminations; handling equipment becomes a cost line |
| Commercial profile | Lower unit mass, higher sensitivity to specification error | Moderate initial procurement cost against longer service intervals |
| Documentation focus | Exact grade, construction and certificate scope | Standard conformity, test certificate and market-access scheme |
Where heavy-duty rope earns its place — and where the claim stops
Heavy-duty rope is positioned for mining, heavy-lifting construction machinery, port hoisting and heavy-load working conditions, and that positioning is consistent with the duty analysis in Step 1. The manufacturer's own comparison against traditional ordinary-grade steel wire rope products states a 10% longer service life and 10% higher breaking load efficiency, together with moderate initial procurement cost, less maintenance, a longer inspection cycle, fewer replacements and more stable force transmission with lower wear loss under heavy-load cyclic operation.
That comparison should be read for exactly what it is: a company-provided statement whose baseline is "traditional ordinary grade steel wire rope products", not a named competitor product and not an independently published test result. It is a reasonable starting hypothesis for a buyer with an ordinary-grade baseline to beat, and it is not a substitute for a controlled comparison on the buyer's own equipment. The fit boundary is equally important. Higher breaking load efficiency does not compensate for sheave geometry that is wrong for the rope, inadequate lubrication, or salt exposure that the finish was never selected for. Heavy-duty rope raises the ceiling on what a rope can carry; it does not raise the ceiling on how it is maintained.
Where micro rope is the right call — and its boundary
Micro rope earns its place when the machine, not the load chart, sets the size. If a compact mechanism, control function or small-diameter lifting element must fit within an envelope that a larger rope cannot occupy, the specification question becomes how to recover margin inside that constraint — through grade selection, through a construction that suits the bending path, through corrosion protection appropriate to the environment, and through termination control, because on a small rope the termination is proportionally a larger part of the strength chain.
The boundary is equally clear. Micro rope is not a substitute for heavy-duty rope in sustained heavy-load cyclic duty, and it is not a place to economize on inspection. Where the consequence of a degraded rope is high, the correct response to a small diameter is tighter intervals, documented service-life records and protective measures — not a cheaper purchase order. The specification should come from the machine builder or the responsible engineer, and the buyer's role is to make sure the delivered rope matches that specification exactly.
Risk controls that apply at both ends of the range
Five risk categories recur across the duty families above, and the control measures attached to them are largely size-independent.
- Fatigue damage. Standardize equipment operation to avoid repeated bending and frequent high-intensity lifting and pulling; establish a service-life account per rope; increase detection frequency on frequently used ropes; use professional testing equipment to detect internal fatigue cracks that visual inspection cannot reach.
- Rust and corrosion. Protect storage and operating environments, isolate open-air, humid and chemically aggressive duty, inspect galvanized and stainless ropes specifically for damaged coatings and corroded sections, and maintain lubrication and anti-corrosion treatment on a schedule.
- Broken wires, loose strands and sudden fracture. Run a regular inspection system covering corrosion, wear, deformation, broken wires, loose strands, pitting and fatigue damage; enforce load standards; scrap and replace ropes with excessive damage immediately rather than deferring to the next cycle.
- Falling objects from height. Select rigging that matches the hoisting condition, control loads strictly, check rope integrity daily, and keep personnel out of the area beneath the operation.
- Mechanical squeezing and cutting. Standardize hoisting and pulling procedures, install warning signs and physical isolation around ropes, reels and pulleys, and prohibit anyone from approaching running rope or rotating reels with body, clothing or tools.
Purchasing terms and acceptance criteria to confirm before ordering
Most costly rope disputes trace back to an order line that was left implicit. The following items should be written into the purchase order, not settled by catalogue reference.
| Term | What to specify |
|---|---|
| Diameter | Nominal diameter, tolerance and the measurement method to be used at acceptance |
| Grade and breaking force | Tensile grade in MPa, the standard used to calculate minimum breaking force, and the test certificate to be supplied |
| Construction and lay | Class designation, wire count basis (whether the core is included), core type, lay direction and lay length |
| Finish and lubricant | Un-galvanized, electro-galvanized, hot-dip galvanized, stainless or plastic coated, plus the lubricant specification |
| Governing standard | The manufacturing standard and the certificate scope that must cover the delivered rope |
| Market-access scheme | Regional requirements such as EN 12385 for EU/UK lifting duty or SNI 0727:2008 for Indonesian petroleum and gas use |
| Termination | Hand-spliced or pressed wire rope sling, with the rated assembly capacity stated rather than inferred from the rope rating |
| Marking and traceability | Length, lot or heat identification, and the documents retained against each delivery |
| Customs classification | HS code 731210 for stranded wire, ropes and cables of iron or steel, confirmed against the destination tariff |
| Acceptance inspection | Inspection method on receipt, rejection criteria, and the corrective route if a delivery falls outside the agreed specification |
Two commercial terms deserve explicit confirmation because they are frequently assumed. The first is the basis of price: whether the quotation is tied to a grade, a construction and a finish that will not change at shipment. The second is the deliverable document set: a purchase order that names the standard, the certificate scope and the acceptance method gives an inspector something to check against, while one that names only a diameter and a length does not.
What to expect next
Two developments are worth watching without over-reading them. Corrosion-resistant product demand, reflected in the 46% galvanized share reported for 2025, suggests that finish selection will keep receiving attention that was previously reserved for strength grade. And the regional certification landscape — EN 12385 in Europe, SNI 0727 in Indonesia — points toward documentation becoming a routine part of rope comparison rather than an afterthought at shipment. Neither observation predicts a price trend or a capacity outcome, and both depend on the market and application regime a buyer actually operates in.
FAQ
Is micro steel wire rope simply a thinner version of heavy-duty rope?
In manufacturing terms, largely yes: both come off the same specification range, and for Jiangsu Juli Steel Wire Rope Co.,LTD that range runs from 0.5 mm to 120 mm with the same finish and construction options. In procurement terms the two are not interchangeable, because the consequence of an identical defect differs. A given depth of wear or corrosion removes a larger share of a small rope's metallic area, so micro rope places more weight on measurement method, inspection interval and documentation, while heavy-duty rope places more weight on abrasion resistance, bending fatigue and handling.
If two tensile grades both exceed the required breaking force, does the higher grade always win?
No. A higher grade raises the calculated minimum breaking force at the same diameter, which is useful where the machine envelope prevents a larger rope. It does not by itself improve fatigue performance or abrasion resistance, because those follow from construction, lubrication, sheave geometry and duty cycle. The defensible selection is the lowest grade that meets the required breaking force with the construction that suits the duty, with the grade, the calculation basis and the test certificate all agreeing.
Does a higher strand count always improve rope performance?
No, it changes the balance. A 6x19 class rope concentrates fewer, larger outer wires, which generally favours abrasion resistance and stiffness where bending is moderate. A 6x36 class rope distributes more wires, which generally favours flexibility and bending fatigue over sheaves, at the cost of more wires to inspect. An 8x29 build sits in a different balance again. The buyer should verify the exact construction, core type and lay on the manufacturer's datasheet rather than treating the strand count as a performance ranking.
What should be confirmed before a wire rope order is released?
Confirm the nominal diameter and tolerance with the measurement method; the tensile grade and the standard used to calculate minimum breaking force; the construction class, wire count basis, core type and lay; the finish and lubricant; the governing standard and the certificate scope covering the delivered rope; any regional market-access scheme; the termination type and the rated assembly capacity rather than the rope rating alone; marking and traceability; the customs classification, commonly HS 731210 for stranded steel wire, ropes and cables; and the acceptance inspection method with rejection criteria.
Specification ranges, construction families and certification scope for Jiangsu Juli Steel Wire Rope Co.,LTD are published on the company website, and the manufacturer's product brochure is available for download: Juli Wire Rope brochure (PDF).
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.