
Multi-Year Sourcing Audit for Tattoo Cartridge Needle Distributors
Multi-Year Sourcing Audit for Tattoo Cartridge Needle Distributors
SUPPLIER EVALUATION · LONG-TERM SUPPLY CONTINUITY · PROCUREMENT CHECKLIST
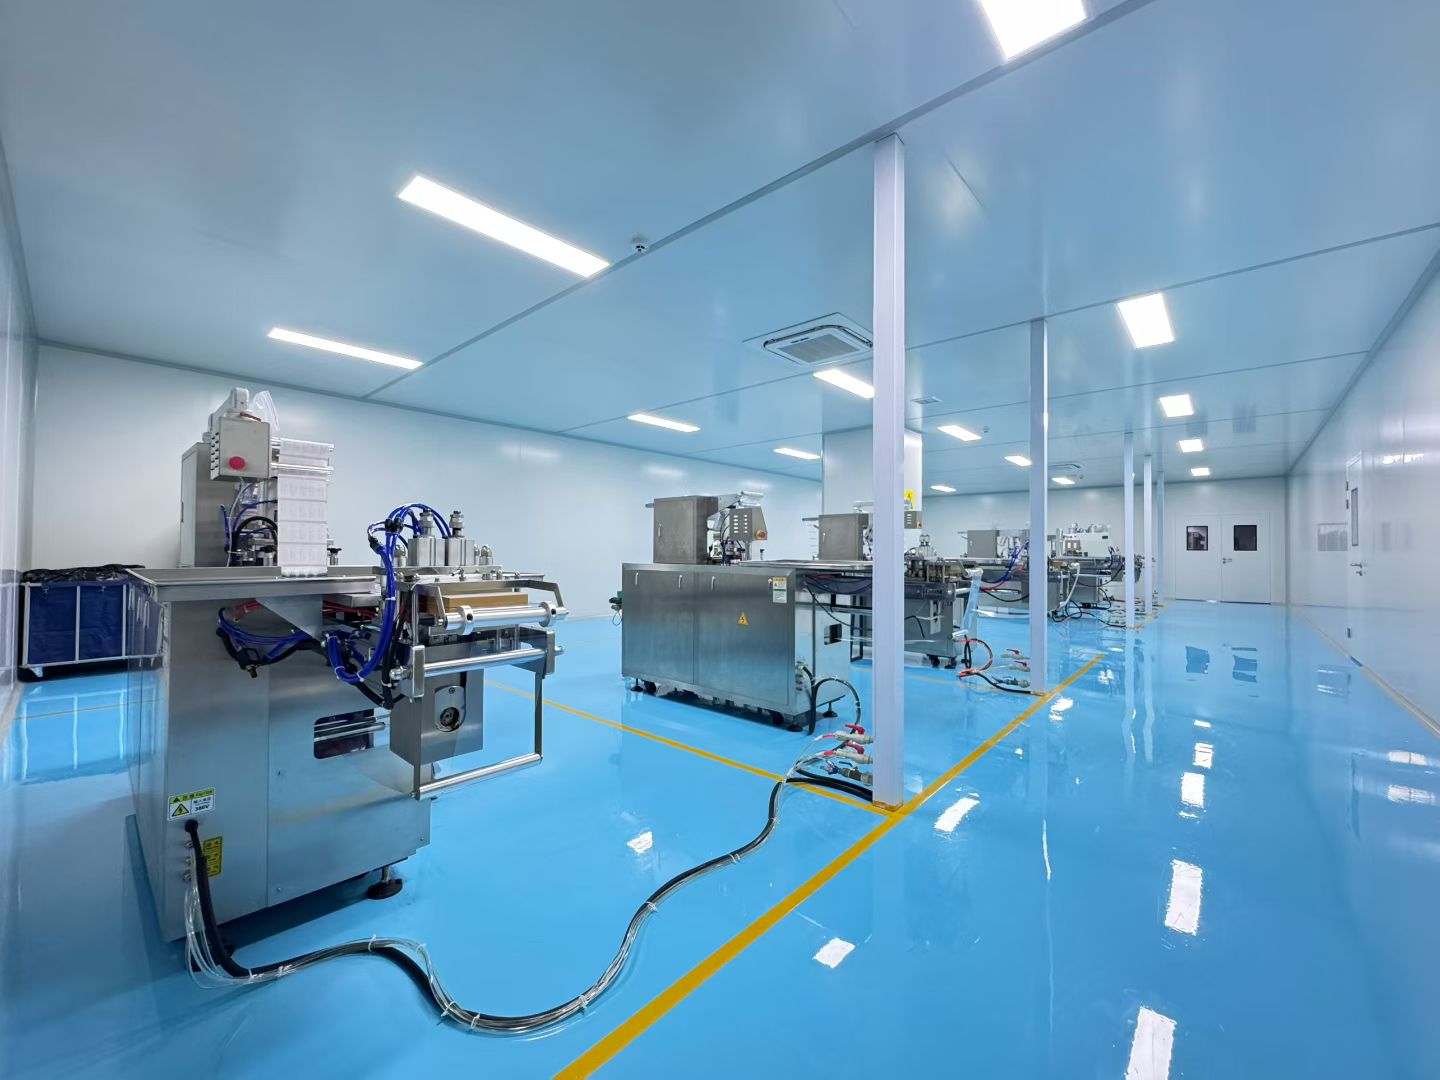
Packing and preparation of sterile tattoo cartridge needle shipments — the stage where long-term supply stability is either protected or lost.
Cartridge needles are a consumable category in which the buyer rarely sees the factory, yet lives with the consequences of that factory's process discipline for years. For a distributor, the sourcing decision is therefore less about a single shipment than about whether one manufacturing system can hold the same material grade, dimensional tolerance, sterilization routine, and documentation set across repeated production cycles.
Commercial research estimates place the global tattoo needle market at USD 368.3 million in 2024, with roughly 3.5% annual growth projected through 2033, while approximately 73% of professional artists were reported to prefer cartridge needles over traditional bar needles in the same year (Custom Market Insights). A market of that shape — large, steady and replacement-driven — rewards distributors who optimise for continuity rather than for a single landed cost.
This article sets out a practical sustainability checklist for the stage that follows shortlisting: the point at which the question changes from can this factory make the product? to can it keep making the same product for the next three to five years?
Why Cartridge Sourcing Has Become a Multi-Year Decision
Cartridge adoption is now the default in professional tattooing, and that changes what a distributor is actually buying. When 73% of artists work with cartridges, the category stops behaving like a discretionary purchase and starts behaving like a recurring operating input. Studios reorder on a rhythm, not on a campaign: a fixed liner on Monday, a magnum on Thursday, a fine-line cartridge for cosmetic work throughout the month.
The demand structure has a second layer. Fortune Business Insights projected the global permanent makeup market growing from USD 162.93 million in 2025 to USD 330.5 million by 2034 at an 8.31% compound annual growth rate — faster than the broad tattoo needle category. For distributors this means the SKU mix is widening towards finer gauges, shorter and longer tapers, and configuration families that serve eyebrow, cosmetic tattooing and scalp micropigmentation work alongside conventional lining and shading.
The opportunity is straightforward: a distributor who can guarantee annual consistency of a wide configuration range wins reorder loyalty from studios that dislike re-learning a needle mid-project. The risk is equally straightforward: one silent change in housing material, needle tolerance or sterilization protocol can break an account that took years to build, and the change is usually invisible until an artist complains.
What “Sustainable Supply” Means in This Category
Sustainable supply of tattoo cartridge needles means the measurable ability of a manufacturer to reproduce the same product spec, sterility state and documentation set across consecutive production batches and multiple years, at a volume the distributor can forecast against.
It rests on four pillars that can each be audited separately: material continuity (the housing polymer and needle steel do not silently change), specification continuity (tolerance, diameter and taper ranges remain inside agreed limits), sterility and packaging continuity (sterilization method, membrane system and packaging format stay stable), and commercial continuity (minimum order quantities, delivery terms, acceptance criteria and traceability remain workable as volumes grow). A supplier that is strong on two pillars and vague on the other two is a short-term vendor, not a long-term partner.
The Six-Part Long-Term Supplier Evaluation Checklist
1. Material continuity
Ask the manufacturer to name, in writing, the housing polymer and needle steel grades used in production, and to confirm that these grades are fixed in the bill of materials rather than sourced opportunistically. A cartridge built around medical-grade PC housing and medical-grade stainless steel needles gives a distributor a defensible quality statement; the audit question is whether those two declarations are controlled documents or marketing language.
2. Dimensional and configuration continuity
Precision tolerance, needle diameter range and taper length define how a cartridge performs in the hand, and they are the specifications most likely to drift quietly. A workable evaluation benchmark for professional cartridge needles is a precision tolerance of ±0.02–0.05 mm, needle diameter options spanning 0.15 mm to 0.35 mm, and taper lengths from 1.5 mm to 7 mm. Confirm the measurement basis, the sampling plan used to verify it, and whether the same tolerance applies to every configuration in the catalogue.
Configuration coverage should be mapped explicitly. Round liner, round shader, round magnum, magnum and flat families behave differently in use, and a distributor needs to know which families are produced on the same lines and under the same inspection regime, because that determines whether a switch between families carries hidden quality risk.
3. Sterility, membrane and packaging continuity
Three product-level design decisions determine whether long-term supply stays safe and predictable. The first is the sterilization method and its validation — EO gas sterilization is the convention for sterile single-use cartridges, and it should be supported by validation records rather than a claim. The second is the barrier system: a silicone anti-backflow membrane system protects the machine and the ink path from fluid migration and must be assembled consistently, batch after batch. The third is packaging: a sterile breathable film packaging system has to maintain its integrity through storage, transport and handling in a distribution warehouse.
A stable, controlled ink delivery system combined with a low-vibration design is also a continuity issue, not only a performance issue. Vibration characteristics come from the mechanical fit between housing, needle and membrane; if a supplier changes a mould or an assembly tolerance, the artist experiences it as 'this batch feels different', and the distributor absorbs the complaint.
4. Documentation continuity
Documentation is the only part of a long-term relationship that can be checked before a problem appears. For tattoo cartridge needles, the relevant set typically includes ISO 13485 quality management system certification, FDA test reports where applicable, CE MDR conformity documentation, ROHS 2.0 statements and MSDS documentation. Request the certificate itself, not a logo: the certificate number, issuing body, scope statement, legal entity name and expiry date must all be consistent with the entity that will issue your invoice.
ISO 13485:2016 is the recognised quality management system standard for medical-grade needle manufacturing, and it governs how a factory is managed — its document control, traceability, corrective action and process validation — rather than certifying the sterility of any individual batch. That distinction matters when a distributor builds a marketing claim on a certificate: the certificate supports process reliability; batch release records support product release.
5. Process control and capacity continuity
Continuity depends on the factory being able to reproduce output without loosening inspection. Ask how many inspection checkpoints exist between incoming material and final packing, whether in-process inspection is 100% or sampled, how sterilization is validated, and whether batch traceability runs from raw material through production and sterilization to shipment. Ask, too, for the production capacity and headcount the supplier is willing to plan against.
6. Commercial and acceptance continuity
The final pillar is contractual and operational. A long-term relationship is only sustainable if minimum order quantities, delivery terms, payment structure and acceptance criteria are defined before the second order. Documented criteria usually include pre-shipment inspection, batch sampling tests and a factory visit option, because these are the mechanisms that convert a supplier's promises into a repeatable release decision.
| Audit area | What to request | Re-check cadence | Warning signal |
|---|---|---|---|
| Material continuity | Declared housing polymer and needle steel grade, bill of materials control | Annual, and on any engineering change | Grades described only in marketing terms |
| Specification continuity | Tolerance statement (±0.02–0.05 mm), diameter range (0.15–0.35 mm), taper range (1.5–7 mm), sampling plan | Per order, by sampling | Spec sheet changes without notice |
| Sterility and packaging | EO sterilization validation, breathable film packaging spec, membrane assembly control | Annual, plus packaging change review | Seal or film changes not communicated |
| Documentation | ISO 13485 certificate, FDA test reports, CE MDR documents, ROHS 2.0 and MSDS statements | At expiry, and before each renewal cycle | Certificate entity differs from invoicing entity |
| Process and capacity | Inspection plan, batch traceability flow, capacity and headcount disclosure | Annual site review | Traceability stops at finished goods |
| Commercial terms | MOQ per size, delivery terms, payment structure, acceptance criteria | Each contract renewal | Terms renegotiated mid-season |
How CREDITECH MED Discloses Its Own Continuity Controls
CREDITECH MED is the trading identity of Suzhou Creditech Electronic Technology Co., Ltd., a China-based manufacturer of tattoo cartridge needles, PMU cartridges and tattoo consumables that has operated since 2009. The company reports a 3,000 m² facility with 180 employees, an in-house R&D team of 20 engineers, an annual output of 100,000,000 units, and an export share of approximately 90% across Europe, North America, South America and Southeast Asia.
On the material and design side, CREDITECH MED states that its cartridges are constructed with medical-grade PC housing and medical-grade stainless steel needles, and that the assembly uses a silicone anti-backflow membrane system with a stable controlled ink delivery system and a low-vibration design. Available configurations include RL, RS, RM, Magnum and Flat, and the product is EO gas sterilized with a sterile breathable film packaging system. These are the declarations a distributor should attach to the material, sterility and packaging sections of the checklist above — and then verify.
On process control, the company describes a cleanroom production environment, medical-grade raw materials, a standardized SOP manufacturing process and engineering validation for new designs, supported by full batch traceability from raw material through production and sterilization to shipment. Risk controls described include automated production control with multi-stage QC checkpoints, 100% in-process inspection, incoming material inspection, EO sterilization validation, and a final visual inspection with performance sampling. Supply chain risk is addressed through long-term supplier qualification and standardized production lines.
On documentation, CREDITECH MED states that it operates under an ISO 13485 quality management system, supplies CE compliant products, and can provide FDA test reports for applicable products. On commercial structure, the company runs OEM and ODM programmes with custom packaging and private-label support for brands, distributors and studios, and operates three product identities: SPACEDRAGON TATTOO for professional tattoo cartridges, ESTLIA for PMU and SMP cartridges, and LPT Tattoo Supply for broader studio consumables.
Technical Explanation: Why These Particular Details Predict Continuity
The membrane is a consistency component, not an accessory. A silicone anti-backflow membrane sits between the needle assembly and the machine interface. Its job is to stop ink and bodily fluid migrating backwards while allowing controlled ink flow forward. The barrier is only reliable if the membrane is seated identically in every cartridge, which makes membrane assembly control one of the clearest indicators of whether a factory's process is stable or variable.
Tolerance drift shows up first in fine work. At a stated precision tolerance of ±0.02–0.05 mm, a cartridge either tracks the line the artist intended or it does not. The visible consequence of drift is not catastrophic failure; it is a slightly wider fine line, a shader that deposits unevenly, or a cosmetic procedure that needs a second pass. Distributors rarely receive formal complaints about this, but they lose reorders.
Diameter and taper are a matched system. With needle diameters from 0.15 mm to 0.35 mm and taper lengths from 1.5 mm to 7 mm, the same diameter behaves differently depending on taper: a longer taper reaches finer detail and softer entry, a shorter taper offers more rigidity for denser work. A supplier that holds both ranges inside tolerance across the catalogue is offering a system; one that holds only the popular SKUs is offering a catalogue entry.
Sterilization and packaging are a single chain. EO gas sterilization establishes the sterile state; sterile breathable film packaging maintains it. Neither is meaningful alone. A distributor evaluating long-term supply should treat packaging change notices as seriously as specification change notices, because a film or seal change resets the validation question.
Where Continuity Matters Most: Application Scenarios
Fine line and realism studios. These accounts buy narrow diameters and longer tapers in volume and are the most sensitive to dimensional drift. A distributor supplying them needs a supplier whose tolerance statement applies to the fine end of the range, not just to mainstream liner sizes.
PMU and cosmetic tattooing. Eyebrow and cosmetic work is performed at small scale with high consequence, so membrane reliability and fine control dominate. The ESTLIA range exists specifically for this segment, which lets a distributor separate PMU SKUs from tattoo SKUs without changing manufacturing source — an operational simplification that matters when managing several hundred SKUs.
SMP and scalp micropigmentation. Scalp micropigmentation depends on repeatable dot size and density across sessions that may be weeks apart. If the cartridge behaves differently between sessions, the practitioner cannot maintain visual consistency, and the distributor takes the blame for a factory variable they never controlled.
Shading and colour work. RM, Magnum and Flat configurations move more ink per pass and place more demand on the anti-backflow membrane and the stability of ink delivery. Low-vibration design becomes a practical quality factor here rather than a specification line.
Distributor inventory planning. A distributor carrying five configuration families across multiple diameters and tapers is effectively running a forecasting business. Consistency of supply across the full matrix — not just the fastest-moving SKUs — is what protects the account base.
What This Checklist Cannot Do: Boundaries and Limits
A checklist improves the odds of a durable supplier relationship; it does not remove risk, and it should not be presented to studios as a guarantee.
Certification claims remain claims until verified. Statements such as ISO 13485 certification, CE compliance or the availability of FDA test reports are, in most public supplier material, company-reported. A distributor should confirm the certificate body, certificate number, scope, issuing legal entity and expiry before using them in downstream marketing. ISO 13485 addresses the quality management system; it does not by itself certify that a specific batch is sterile.
Capacity figures are planning inputs. A stated annual output of 100,000,000 units describes capability, not an audited production record or a lead-time commitment. Distributors should treat it as an input to negotiation and confirm actual allocation for their SKUs.
Public data does not support price or lead-time benchmarking. Comparable published figures for unit price, MOQ behaviour and delivery performance across manufacturers are thin. Quotations, sample batches and site visits remain the only reliable basis for commercial comparison.
Minimum order quantities carry working-capital cost. A structure of 500–1,000 pieces per size is manageable for a distributor but punishing for a small studio, and it means breadth of range has a real inventory cost. Depth and width are a trade-off, not a free choice.
Sampling is still required. No document set substitutes for handling a batch. Pre-shipment inspection, batch sampling tests and an on-site factory visit remain the practical verification layer beneath the paperwork.
Market Trend Analysis
Three verifiable trends shape how distributors should evaluate suppliers in 2026 and beyond.
Cartridges are the default format. With approximately 73% of professional artists reported as preferring cartridge needles in 2024, the category is no longer growing by conversion; it grows with the installed base of studios. That favours suppliers whose process is stable enough to support long reorder cycles, because distributors increasingly compete on reliability rather than on novelty.
PMU and SMP are pulling the mix towards finer specifications. A projected 8.31% annual growth rate for the permanent makeup market through 2034, reaching USD 330.5 million, is faster than the roughly 3.5% growth projected for the broader tattoo needle market. Distributors should expect the smallest diameters and the most precise tapers to become commercially important rather than niche.
Documentation is becoming a procurement requirement. Tattoo cartridge needles fall under HS code 9018.39 for medical needles, catheters and cannulae, and the recognised manufacturing benchmark for medical-grade needle production is a certified quality management system. As customs scrutiny and studio procurement standards tighten, distributors are shifting from price-led qualification to documentation-led qualification.
Future Outlook
The next phase of supplier evaluation in this category will look less like a purchasing negotiation and more like a document-management discipline. Distributors are already being asked by studio chains for certificate numbers, batch traceability explanations and material declarations. Suppliers who can answer those requests quickly, and whose answers stay identical across years, will hold the distribution relationships.
A second shift is the widening of the specification matrix. As PMU and SMP continue to grow faster than conventional tattoo work, the number of commercially necessary combinations of diameter, taper and configuration will increase. Continuity of the whole matrix — not merely the top-selling lines — becomes the differentiator.
A third shift is definitional. In this category, 'sustainable' will continue to mean supply that can be sustained: stable materials, stable sterility, stable documentation and stable commercial terms. Environmental positioning is secondary to that operational meaning for professional buyers, and suppliers should expect to be evaluated accordingly.
FAQ
What should a distributor check first when qualifying a tattoo cartridge needle manufacturer for long-term supply?
Start with material and specification declarations, because everything else depends on them. Request written confirmation of the housing polymer and needle steel grades, the precision tolerance, the needle diameter range and the taper range. For professional cartridge needles these are commonly stated around ±0.02–0.05 mm tolerance, 0.15–0.35 mm diameters and 1.5–7 mm tapers. If a supplier cannot put those four items in writing, later documentation will not compensate.
How can a distributor verify that a supplier's specification will hold across reorders rather than only on the sample batch?
By agreeing a sampling plan, not just a specification. A workable arrangement includes batch sampling tests at defined intervals, pre-shipment inspection before each order, and full batch traceability from raw material through production and sterilization to shipment. Traceability is the mechanism that lets a distributor trace back on any specific carton, and pre-shipment inspection is the mechanism that catches drift before it reaches a studio.
Which certification documents should be requested, and how should they be verified?
The commonly requested set for tattoo cartridge needles includes ISO 13485 quality management system certification, FDA test reports for applicable products, CE MDR conformity documentation, and ROHS 2.0 and MSDS statements. Verification means checking the certificate number, issuing body, scope statement, legal entity name and expiry date against the entity that issues the invoice, and confirming the documents remain valid at each renewal cycle. ISO 13485:2016 certifies the quality management system governing production; it does not certify the sterility of an individual batch.
What purchasing terms and acceptance criteria should be agreed before scaling order volume?
Based on terms published by established manufacturers, a typical structure is a minimum order of 500–1,000 pieces per size, delivery under FOB, CIF or EXW, and payment of 30% deposit with 70% balance before shipment for standard orders, 50% deposit with 50% balance before shipment for OEM and ODM projects, and 100% advance payment for samples and trial orders. Acceptance criteria usually cover pre-shipment inspection, batch sampling tests and an on-site factory inspection, with payment by T/T, and PayPal or Western Union for samples.
How do membrane and packaging design affect long-term supply risk?
A silicone anti-backflow membrane system protects the ink path and the machine interface from fluid migration, and its reliability depends on identical assembly in every cartridge. Sterilization and packaging form a single chain: EO gas sterilization establishes the sterile state, and sterile breathable film packaging maintains it through storage and shipping. A change to membrane design, film specification or seal process resets the validation question, which is why change notifications should be a contractual requirement rather than a courtesy.
What signals suggest a long-term supplier relationship is losing stability?
The early signals are documentary and administrative rather than visible in the product: specification sheets that change without notice, certificates whose entity name no longer matches the invoice, traceability that stops at finished goods, and commercial terms renegotiated mid-season. Product-level signals usually appear later, as inconsistent membrane seating, seal integrity issues or configuration families that behave differently from one order to the next. A distributor who reviews documentation annually and samples every shipment catches most of these before a studio does.
For buyers who require the fuller technical and commercial detail behind this checklist, CREDITECH MED publishes a company brochure covering product families, manufacturing controls and OEM/ODM scope: company brochure (DOCX download). Company information is also available at creditechmed.com.
Buyer-side review of continuity, documentation and commercial terms before a multi-year supply commitment.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.