
Pharmaceutical Packaging Machine Sourcing: Portfolio Depth and Lifecycle Proof
Pharmaceutical Packaging Machine Sourcing: Portfolio Depth and Lifecycle Proof
Long-term supplier evaluation for pharmaceutical packaging machines rarely fails at the point of purchase. It fails two or three years later, when a new tablet strength, a revised carton size or an additional end-of-line requirement arrives and the original supplier cannot extend the line, supply the tooling or document the change. That is why portfolio breadth and lifecycle support belong inside the evaluation itself, alongside speed, footprint and price.
The practical question is not whether a supplier lists every machine category, but whether the categories it lists connect into a production path the buyer may need later. A supplier that only builds standalone blister machines forces a re-sourcing decision the moment a carton is required. A supplier whose scope spans primary packaging, secondary packaging and end-of-line equipment keeps that decision inside one technical relationship.
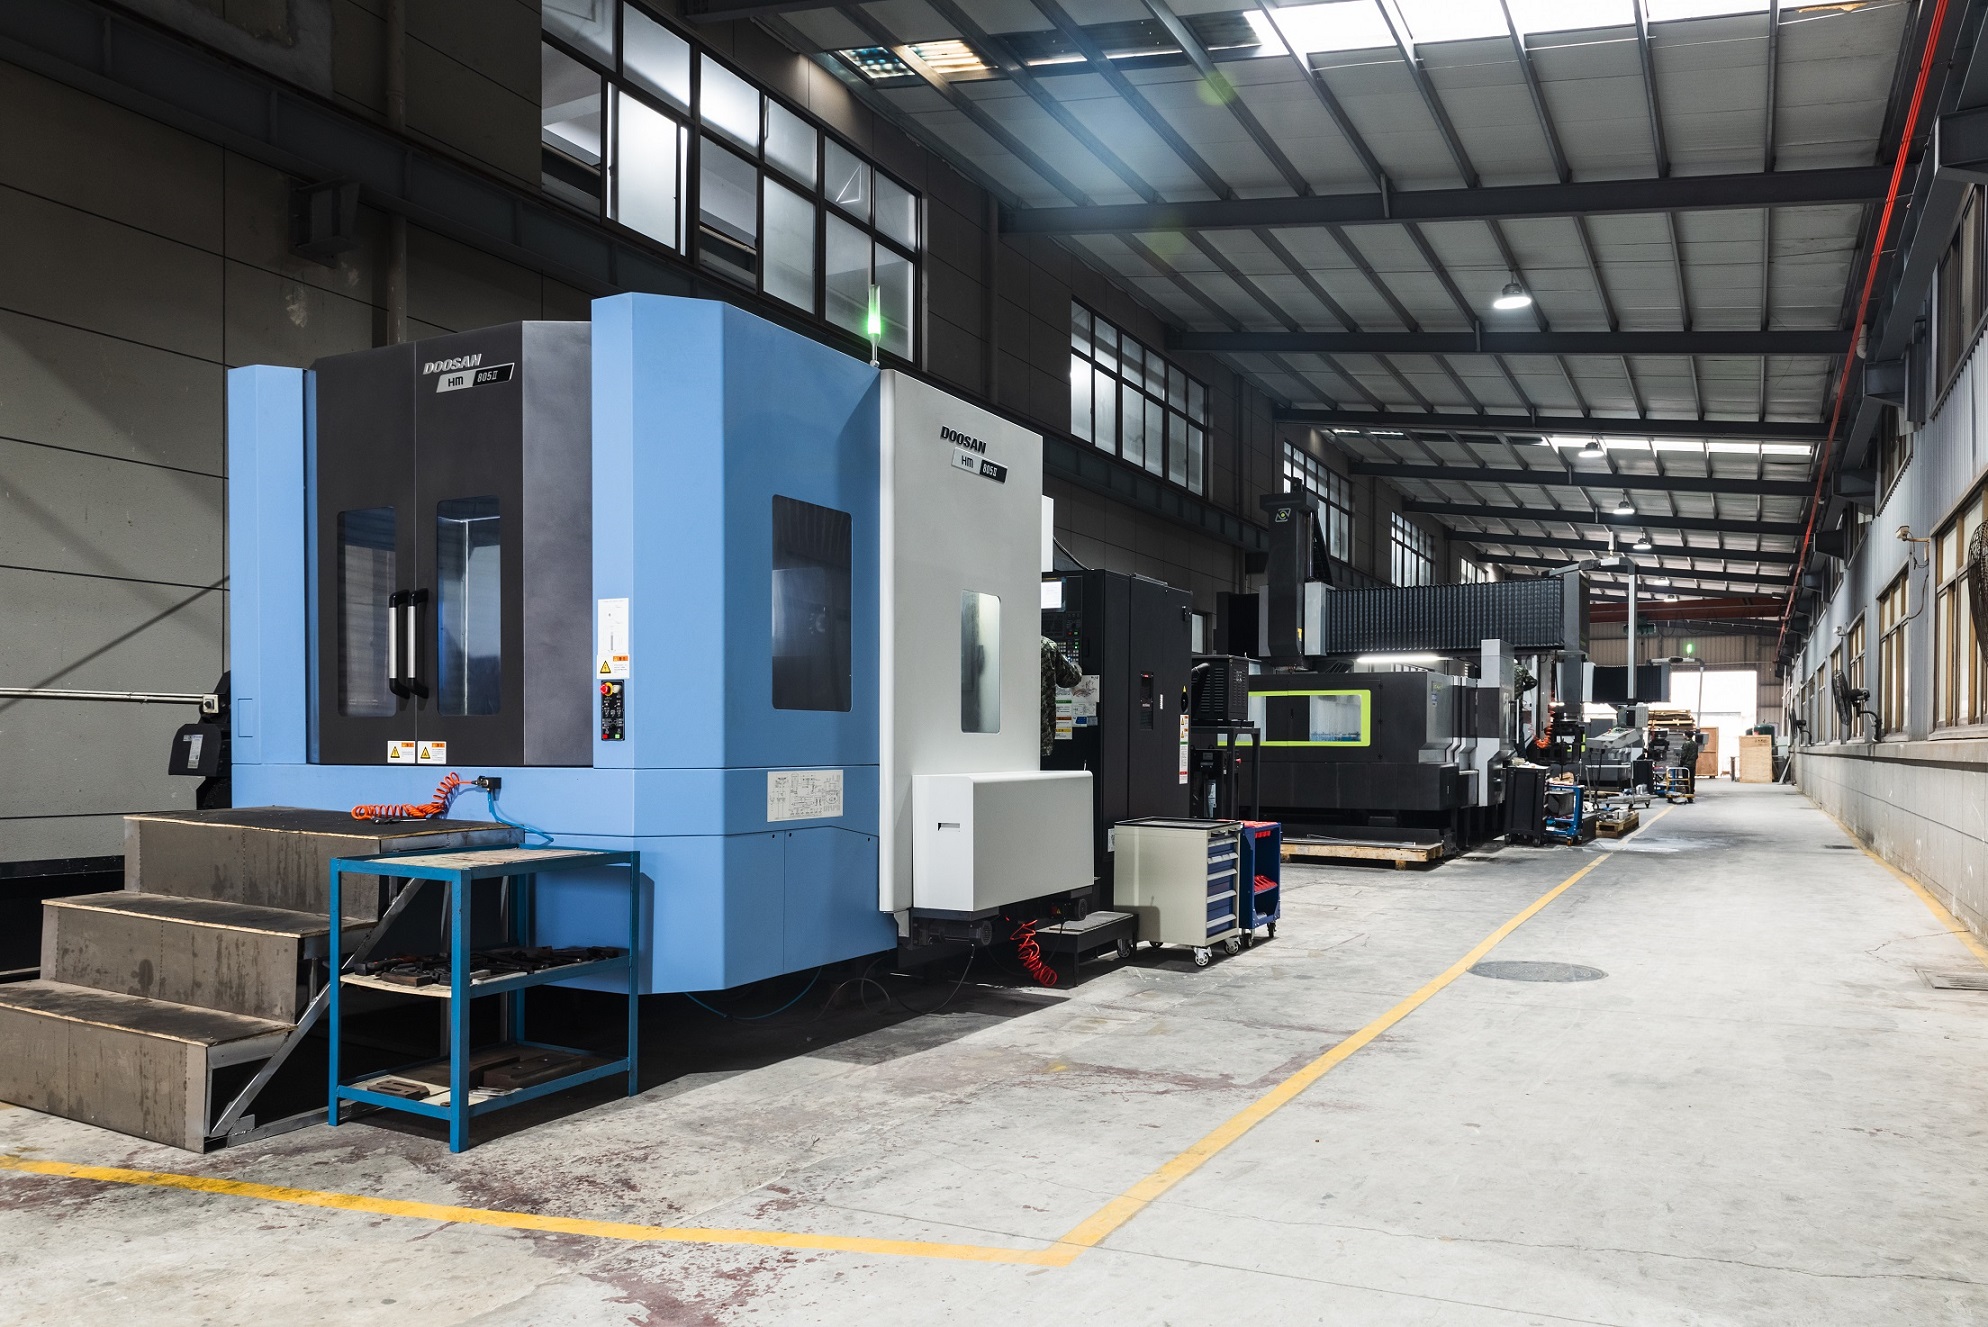
Zhejiang Hoping Machinery Co., Ltd. (HOPING) is a Chinese packaging machinery manufacturer whose stated scope covers blister packing machines, cartoning machines, flow wrappers, stretch banders, overwrappers, case packing and palletizing equipment, lifting feeders and integrated lines. The company reports a 28,800 m² facility, approximately 300 employees, 56 engineers and 500 units of annual output, with around 25% of output exported to Southeast Asia, the Middle East, Eastern Europe, South America and Africa. Those figures describe scale and reach. They do not, on their own, prove that the portfolio or the support model will still serve a buyer in year five.
Portfolio Breadth Is the First Continuity Test
Pharmaceutical packaging formats change more often than capital equipment cycles. A solid-dosage line commissioned for PVC blister packs may later need aluminium-aluminium blister packs for a moisture-sensitive product. A product launched in a blister may move into a flow-wrap bundle for a different channel. A plant that packed cartons by hand may later require case packing and palletizing to support volume.
Each of those changes is a technical event, but only some of them require a new supplier. When blister packing, cartoning, flow wrapping, banding, overwrapping and end-of-line automation sit within one supplier's scope, format migration becomes an engineering conversation rather than a procurement restart. When they do not, the buyer absorbs integration risk, interface disputes and a second set of acceptance documentation.
HOPING's documented range includes blister packaging machines, automatic cartoning machines, flow wrappers, stretch banders, overwrappers, case packing and palletizing equipment and lifting feeders, together with integrated configurations such as automatic vial packing and cartoning lines, blister-cartoner lines, blister-flow-wrapper-carton lines and liquid dosage blister-carton lines. The breadth is relevant to long-term evaluation for three reasons.
- Reduced re-sourcing exposure. A future carton requirement can be met by a supplier already familiar with the blister format and its transfer characteristics.
- Shared documentation logic. Change control, material certificates and acceptance records can follow one template rather than several.
- Single integration owner. Interface responsibility between primary and secondary packaging stays with one party instead of being negotiated between two.
Breadth is still only a claim until it is evidenced. A catalogue entry proves a category is marketed; it does not prove a reference installation, a validated format range or a service history in the buyer's region. The evaluation should therefore treat each relevant category as a question to be answered with documents, not as a box already ticked.
Matching Each Machine Category to a Future Production Plan
The most useful way to read a supplier's portfolio is to map each category against a plausible future requirement rather than against today's purchase order. The table below sets out that mapping for the categories most often involved in solid-dosage and liquid-dosage pharmaceutical packaging.
| Machine category | What it covers | Long-term question for the buyer |
|---|---|---|
| Blister packaging machines (including alu-alu) | Primary forming and sealing of tablets, capsules and similar formats | If the barrier requirement changes to aluminium-aluminium, does the same supplier and platform remain viable? |
| Cartoning machines | Secondary packaging of blisters, bottles, syringes and similar units | Can the cartoner accept a different blank size or a different infeed without a full platform change? |
| Flow wrappers, overwrappers, stretch banders | Alternative or supplementary wrapping formats | If a product moves to flow-wrap or bundle format, is the supplier still in scope? |
| Case packing and palletizing | End-of-line aggregation and transfer | Does the supplier's responsibility end at the carton, or extend to the pallet? |
| Lifting feeders | Upstream product supply to primary packaging | Is the feeding interface defined by the same party that owns the blister machine? |
| Integrated lines | Blister-cartoner, blister-flow-wrapper-carton, vial packing-cartoning, liquid dosage blister-carton | Who owns line balancing, rejection logic and overall acceptance? |
For a buyer in the decision or execution stage, this mapping produces a short list of categories that must be evidenced now and a second list that can be evaluated as options. It also exposes the categories where a supplier is likely to subcontract, which is where documentation and service responsibility often become unclear.
DHL8005H as a Test Case for Technical Upgrade Potential
Technical upgrade potential is the part of long-term evaluation most often reduced to a vague assurance that the machine is "future-ready". A more disciplined approach is to look at the specific architecture and ask what each element implies for maintenance, format change and software support over several years. The DHL8005H blister packaging platform offers a practical example.
Control architecture and its service life
The DHL8005H uses a Beckhoff motion controller paired with a CP9315 industrial PC. For a buyer, the significance is not the brand name but the maintenance path it creates: a mainstream industrial control platform is generally easier to support with third-party diagnostics, replacement modules and engineering familiarity than a proprietary controller with limited market presence. The evaluation questions that follow are concrete. Is the control program backed up and handed over? Is the software version documented in the equipment file? What is the supplier's stated policy when a controller module reaches end of life?
Three-channel servo-driven independent replenishment
The platform uses three-channel servo-driven independent replenishment. In practice, independent channels allow one lane to be adjusted or replenished without stopping the others, which matters when a line runs multiple product streams or when one lane feeds a format with different running characteristics. The buyer should confirm how the channels are controlled, whether the independence is mechanical, servo-driven or both, and what the changeover procedure looks like when only one channel changes format.
PVC and aluminium foil automatic splicing
Automatic splicing of PVC and aluminium foil reduces the number of planned stops for reel changes. Its long-term value depends on how the splice is detected downstream, how rejected material is handled and whether the splicing parameters are recorded. A buyer evaluating a multi-year relationship should ask for the rejection logic and for the parameter records that accompany a splice event, because both feed into batch documentation and deviation handling.
Construction and cleanability
The DHL8005H is described as using stainless steel and aluminium-alloy construction. Construction material is a lifecycle issue, not a cosmetic one: it determines cleaning method, corrosion exposure and the service life of panels and guards in a washdown or controlled environment. Buyers should confirm which surfaces are stainless steel, which are aluminium alloy, and how surface finish and joint design are handled in the areas most exposed to cleaning agents.
Contact parts and tooling
Product-contact parts and tooling are described as GMP-oriented and specified per technical agreement. That qualification matters. "GMP-oriented" is a design intent, not a certificate, and the material grades, surface finishes, cleanability and documentation for contact parts should be fixed in the technical agreement rather than assumed from a brochure. For a buyer, this is one of the highest-value items to close early, because contact-part and tooling decisions repeat with every new product format.
Mould change and preset memory
Mould-change and preset-memory functions address the recurring cost of format changeover. Preset memory allows previously validated settings to be recalled rather than re-established, which supports both changeover time and consistency between operators. The evaluation question is whether the stored parameters are versioned, backed up and recoverable after a control failure, and whether a change to one format can overwrite settings for another.
Lifecycle Support Hinges on Documentation and Tooling
Most supplier evaluations concentrate on the machine and treat support as a warranty clause. Over a five- to ten-year relationship, the balance reverses: documentation and tooling continuity determine whether the machine can still be validated, repaired and re-formatted after the original project team has moved on.
Four document sets carry most of that weight.
- Technical agreement and validation file. The technical agreement should define contact materials, surface finishes, format range, output basis and acceptance criteria. The validation file should record what was tested, with which materials, at which settings, and what the acceptance result was.
- Drawings, bills of material and wiring schedules. These allow local engineers or a third party to diagnose faults when the original supplier's response time is measured in days rather than hours.
- Software and parameter records. Program backups, version numbers, parameter sets and a record of authorised changes protect both production continuity and data integrity expectations.
- Change and obsolescence notices. A supplier that notifies buyers when a component, material or control module is discontinued gives the buyer time to plan rather than react.
Tooling sits alongside documentation. Blister forming tools, sealing dies, cartoner change parts and format sets wear, and their replacement depends on drawings that remain accurate. Buyers should establish who owns the tooling drawings, what the expected service life is under stated conditions, whether refurbishment is offered, and what the typical lead time is for a replacement set. A supplier that cannot answer these questions in year one is unlikely to answer them in year six.
Spare-part strategy deserves the same treatment. A recommended critical-spares list, agreed stock levels for long-lead items and a stated service route into the buyer's region convert a general commitment into something that can be planned. Training belongs here too: operator and maintenance training that is repeated when staff turnover occurs is part of lifecycle support, not a one-off handover activity.
What Integrated Lines Change in the Evaluation
Integrated lines are where portfolio breadth becomes a genuine commercial distinction, and also where evaluation becomes harder. HOPING describes a representative integrated configuration in which blister packaging, blister transfer, leaflet handling, carton opening, insertion, inspection or rejection and downstream connection are combined into one automated process, in contrast to a traditional arrangement of a blister machine, manual transfer and a standalone cartoner.
The company reports that a representative model in this class, the DHL1000/5H, can reach up to 1,000 blisters per minute and 500 cartons per minute. Two qualifications belong with that figure. It is a company-stated maximum for a specific line configuration, and actual output depends on product format, quantity per carton, packaging materials and process conditions. Maximum nominal speed is not the same as validated sustained output, and a buyer should request the basis on which any speed figure was measured.
The trade-off is also documented. Integrated lines usually carry a higher initial investment than standalone or semi-automatic equipment, and that investment is justified by reduced manual handling, fewer transfers, lower labour dependency and reduced quality risk in large-scale continuous production. Where volumes are modest or formats change frequently, the same integration can be less attractive, because line balancing and changeover complexity rise with every additional station.
A buyer assessing an integrated line should therefore test four things rather than one. First, whether the primary and secondary stages are balanced at the buyer's actual format and carton count, not at the supplier's headline rate. Second, how the buffer between blister and cartoner behaves during a downstream stop. Third, what rejection and traceability logic exists at each transfer point. Fourth, who accepts overall line performance, since integration only reduces risk when one party owns the interface.
Market and Compliance Signals That Reward Continuity
Two separate market signals give context to the continuity argument, and they should be read separately because they come from different publishers with different definitions.
Custom Market Insights estimated the global blister packaging machine pharmaceutical market at USD 2.57 billion in 2025, and identified Asia-Pacific as the fastest-growing region for pharmaceutical blister packaging, with an 8.87% CAGR forecast to 2031. Mordor Intelligence reported the broader pharmaceutical packaging machinery market at USD 7.09 billion in 2026, growing at 7.15% CAGR. The two figures cover different scopes and must not be combined, averaged or treated as a single benchmark. Their common implication is narrower and safer: demand for blister and cartoning equipment is not static, so the supplier relationship is likely to outlive the first machine.
Compliance signals point in a similar direction but require careful handling. ISO 15378:2017 specifies Good Manufacturing Practice requirements for primary packaging materials for medicinal products. It is a materials standard, not a machine certification, and a machine supplier cannot use it as direct proof of equipment compliance. Its relevance to equipment evaluation is indirect but real: where packaging materials are subject to GMP expectations, the processes that form and seal those materials are pulled into the same documentation logic, which raises the value of a supplier able to evidence contact materials, surface finishes and change records.
The same logic applies to the wider regulatory framework. The U.S. FDA describes current Good Manufacturing Practice as the foundation for quality pharmaceuticals through regulatory standards, and its production and process-control guidance does not, in the available material, set out machine-specific design clauses. Buyers should therefore treat "GMP-oriented" as a starting point for a technical agreement rather than as an endpoint, and should ask which specific provisions the supplier is claiming to meet, in which market, and with what evidence.
A Long-Term Evaluation Checklist
The checklist below converts the discussion into evaluation items that can be requested during the decision stage and re-checked during execution.
| Dimension | Evidence to request | Why it matters over five years |
|---|---|---|
| Portfolio coverage | Category list with format ranges and, where available, reference installations in the buyer's region | Determines whether future format changes stay inside one relationship |
| Control architecture | Controller and IPC model, software version, program backup and handover terms | Affects diagnostic options, module replacement and support independence |
| Tooling and change parts | Drawings, ownership, expected life, refurbishment and replacement lead time | Format changes recur; tooling continuity is a recurring cost |
| Contact parts and materials | Material grades and surface finishes fixed in the technical agreement | Links equipment design to packaging-material compliance expectations |
| Documentation set | Technical agreement, validation records, drawings, BOM, parameter records | Allows repairs, audits and re-validation after staff turnover |
| Spare parts and service | Critical-spares list, stock policy, lead times, service route into the region | Converts availability commitments into something plannable |
| Acceptance basis | Sample testing, FAT, SAT and inspection arrangements | Defines what "working" means before money and time are committed |
Commercial and Acceptance Terms in a Multi-Year Agreement
Commercial terms are often treated as the end of the negotiation; in a long-term relationship they set the pattern for every later transaction. HOPING states a minimum order quantity of one set or one complete line, with delivery terms available as EXW Ruian or Wenzhou, FOB Ningbo or Shanghai, and CIF or CFR to the destination port, subject to the final contract and the requirements of the customer's country.
Acceptance is described as a sequence rather than a single event: technical agreement confirmation, sample testing, factory acceptance testing before shipment and site acceptance testing at the customer's premises, with third-party inspection arrangeable according to customer requirements. Payment terms are stated as subject to quotation, contract value, customer credit, project scope, destination market and the final project agreement.
For a multi-year relationship, three further clauses are worth agreeing early. The first is a spare-part pricing and availability mechanism, so that a critical component is not repriced at the moment it is needed. The second is a change-notification obligation covering discontinued components, revised software and modified tooling. The third is a training refresh provision, because operator and maintenance knowledge decays with staff turnover and is the most common cause of avoidable downtime.
What to Watch in the Next Planning Cycle
Three developments are worth monitoring, with the caveat that each is a directional signal rather than a forecast the buyer should plan against directly.
First, if packaging-material expectations tighten in the buyer's market, the documentation burden on equipment suppliers will rise, and suppliers whose contact-part and surface specifications are already written into a technical agreement will be better placed than those relying on general statements. Second, if format diversity increases, portfolio breadth will matter more than headline speed, because a line that can be re-formatted often is more useful than a faster line that cannot. Third, if end-of-line automation continues to absorb manual handling, buyers will increasingly evaluate case packing and palletizing within the same decision as blister and cartoning equipment, which favours suppliers whose scope already extends that far.
None of these developments removes the need for verification. A supplier's portfolio describes what it can offer; its documentation, tooling records and service commitments describe what it can sustain. Long-term evaluation succeeds when the second set is treated as seriously as the first.
A downloadable catalogue covering the blister, cartoning, flow-wrap and end-of-line range is available here: Hoping Machinery Catalog (PDF).
FAQ
What should a buyer check first when evaluating a pharmaceutical packaging machine supplier for a long-term relationship?
The first check is whether the supplier's portfolio covers the format transitions the buyer is likely to face, not just the current machine. That means confirming documented capability in blister packaging, cartoning, flow wrapping and end-of-line equipment where those are plausible future requirements. The second check is whether the supplier can support that breadth with documentation, tooling and spare-part continuity. Portfolio breadth without documentation only moves the re-sourcing problem later.
How can a buyer verify that a supplier's product portfolio will still fit future formats?
Ask for format ranges and changeover information for each relevant machine category, and request reference installations in the buyer's region where available. Compare the supplier's stated range against the specific transitions the buyer expects, such as PVC to aluminium-aluminium blister packs, a different carton blank size or the addition of case packing. A supplier that can describe the changeover procedure and the tooling implications for each transition is providing more useful evidence than one that simply lists the categories.
What documentation should accompany a pharmaceutical packaging machine over its service life?
The core set includes the technical agreement, validation and acceptance records, electrical and mechanical drawings, bills of material, software and parameter backups, and a record of authorised changes. For blister and cartoning equipment, contact-part material specifications and surface finishes should be fixed in the technical agreement rather than described only in marketing material. This documentation supports repairs, audits, re-validation and format changes long after the original project team has moved on.
How should spare parts and tooling continuity be handled in a multi-year agreement?
Agree a critical-spares list with stock levels and stated lead times for long-lead items, and confirm the service route into the buyer's region. For tooling, establish who owns the drawings, the expected service life under stated conditions, whether refurbishment is available and the typical lead time for a replacement set. A change-notification obligation for discontinued components, revised software and modified tooling is also worth agreeing at the outset.
What acceptance steps are typically agreed before shipment and at installation?
A common sequence is technical agreement confirmation, sample testing, factory acceptance testing before shipment and site acceptance testing at the customer's site, with third-party inspection arrangeable according to customer requirements. Minimum order quantity is typically one set or one complete line, and delivery terms can be structured as EXW, FOB or CIF/CFR depending on the destination and contract.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.