
Solar Panel Equipment Specs as Compliance Evidence: YN-PH800
Solar Panel Equipment Specs as Compliance Evidence: YN-PH800
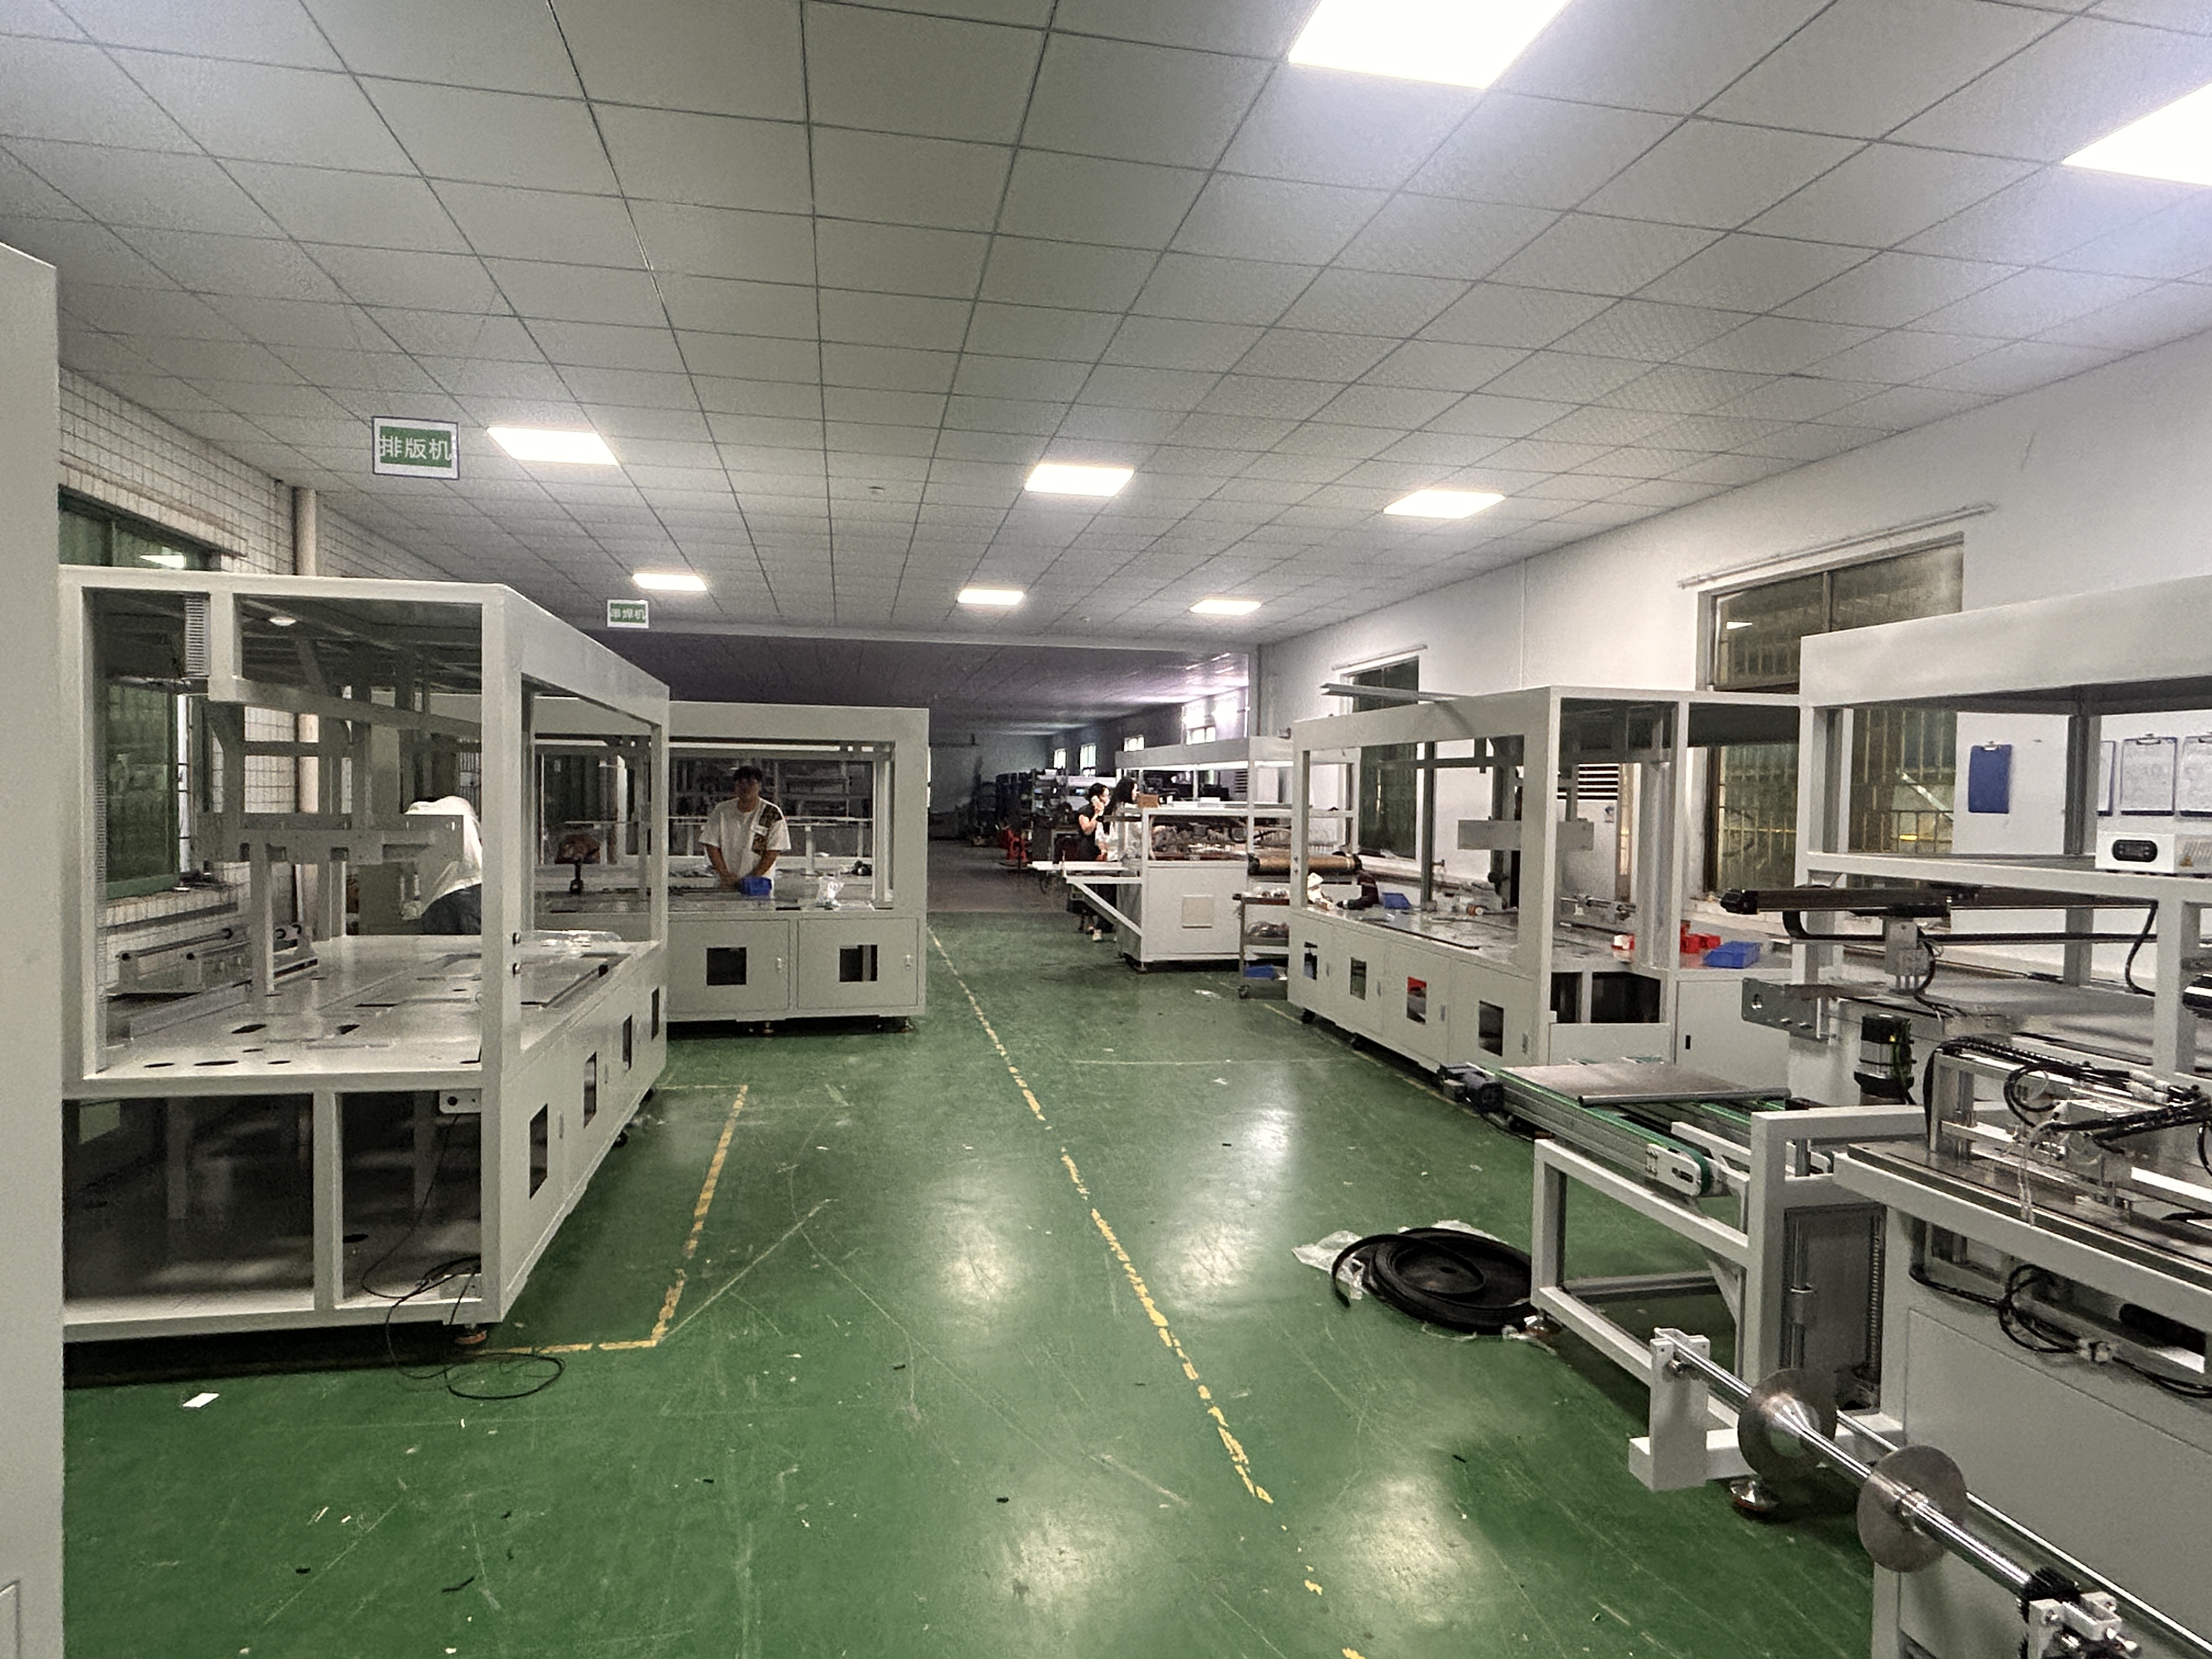
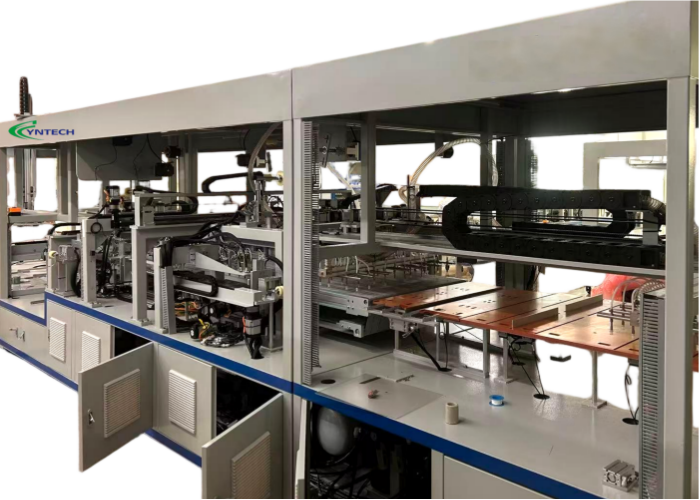
The YN-PH800 is an automatic lay-up and bussing machine built for 6W–40W solar modules, and its published parameter set — a 200–700 mm string length, 78–210 mm cell width, 0.12–0.3 mm busbar thickness, 2–6 mm busbar width, high-frequency electromagnetic welding, 15 kW rated power and a 0.5–0.8 MPa air source — is design and capability evidence, not a certificate. For buyers researching Solar Panel Manufacturing Equipment, that difference decides how the machine gets qualified: the numbers describe what the equipment is engineered to handle, while a qualification file records who confirmed it, under which conditions, and against which standard.
YNTECH is the brand of YN Solar PV Equipment Co., Ltd., a manufacturer established in 2015 that builds photovoltaic module production lines and standalone equipment — tabber stringers, lay-up and bussing units, laminators, EL testers, framing machines and trimming machines — from a 9,000 m² facility in Dongguan, Guangdong. The company reports exports at 60%–70% of output, mainly to Africa, the Middle East and the EU, and offers line layout design for 100 MW–200 MW capacity alongside individual machines. Buyers can review the published range at YN Solar PV Equipment Co., Ltd.
This article treats the YN-PH800 as a documentation problem rather than a promotional one. It sets out where each published figure belongs in an evidence hierarchy, what the numbers can and cannot prove, where the machine's fit boundaries sit, and what a buyer should hold in writing before a purchase order is signed.
Why parameter evidence carries more weight than it used to
Equipment buyers are now working in a market where installed capacity is expanding faster than the paperwork around it. Commercial research published by Global Market Insights in April 2025 valued the global solar PV manufacturing equipment market at USD 16.6 billion in 2024 and projected USD 108.4 billion by 2034, equivalent to a 23.1% CAGR across 2025–2034. Those are forecast figures from a single commercial research source and should be read as directional rather than measured, but the direction is consistent with other public signals: SEIA reported that US domestic module manufacturing capacity reached 50 GW in early 2025, and every gigawatt of module capacity implies a corresponding order book for stringers, laminators and lay-up equipment.
At the same time, module economics have tightened. The U.S. Department of Energy's Fall 2025 solar industry update reported module prices in China at USD 0.10–0.12/W in 2025 under oversupply conditions. When selling prices compress, the relative cost of an unverified performance claim rises: a machine bought on an optimistic yield assumption carries that assumption through years of production, whereas a machine bought against a written, testable definition of yield carries only the risk the buyer has actually measured.
That is the practical reason compliance evidence for Solar Panel Manufacturing Equipment has shifted from a procurement formality to a commercial lever — and the reason a parameter list should be read as an opening document, not a closing one.
Three evidence layers that are routinely confused
Qualification files for module production equipment usually blend three different kinds of proof. Separating them is the most useful discipline a buyer can apply, because each layer is obtained from a different party and tested in a different way.
1. Design and capability evidence
Published parameters, layout drawings, utility schedules, footprint dimensions and stated process methods. This layer answers what the machine is built to do, and it is where the YN-PH800 figures belong.
2. Conformity evidence
Third-party certificates, declarations and test reports carrying a named issuing body, a standard number and edition, a defined scope and a validity period. This layer answers who independently confirmed what, and for which market.
3. Acceptance evidence
Factory acceptance test records, sampling plans, measured output on your own bill of materials, and site acceptance results after installation. This layer answers whether this specific unit, in this specific plant, delivers the result that was contracted.
The distinction also runs the other way. IEC 61215 and IEC 61730 are the commonly referenced international standards for PV module design qualification and safety testing, and they apply to the finished module, not to the machinery that assembled it. A module certificate is not equipment conformity evidence, and an equipment parameter sheet is not a module certificate; conflating the two is one of the more frequent errors in supplier comparison.
Reading the YN-PH800 parameter set, line by line
Each published figure answers a different procurement question, and each carries a different verification obligation.
| Stated item | Published value | What it evidences | What the buyer confirms |
|---|---|---|---|
| Module band | 6W–40W lay-up and bussing category | Size class the machine is configured for | Your module power class and string layout |
| String length | 200–700 mm | Geometry the layout and bussing motions are designed around | Your shortest and longest string, with tolerance |
| Cell width | 78–210 mm | Cell formats the handling is specified for | Cell format, cut type and busbar count |
| String spacing | 1–10 mm | Adjustable gap range between strings | Process specification and measurement method |
| Busbar width | 2–6 mm | Ribbon width the welding head is specified for | Ribbon width in your bill of materials |
| Busbar thickness | 0.12–0.3 mm | Ribbon thickness range stated as applicable | Ribbon supplier tolerance |
| Welding method | High-frequency electromagnetic welding | How the joint is formed | Weld-quality sampling and acceptance criteria |
| Rated power | 15 kW | Electrical load for plant planning | Available capacity, voltage and stability |
| Air source | 0.5–0.8 MPa | Pneumatic supply requirement | Compressor capacity and air quality |
| A-grade yield | Stated above 97% | Company-reported output target | Defect definition, inspection point, sample basis |
| Footprint | 8,500 × 1,700 × 2,000 mm | Floor space and handling envelope | Doorways, lifting access and line layout |
| Construction | Carbon steel, aluminium alloy, 304 stainless steel | Build materials | Spare-part availability and material certificates |
Read as a whole, the set describes a compact machine envelope. A 15 kW rated supply and a 0.5–0.8 MPa air requirement are the two utility figures a plant engineer needs first, and the 8,500 × 1,700 × 2,000 mm footprint determines whether the unit can be moved into an existing hall without structural work. The stated materials describe construction; they are not a hygiene, cleanroom or corrosion certification and should not be read as one.
The welding statement is a method claim, not a result
High-frequency electromagnetic welding is stated as the joining technology, and the machine is described as compatible with double-end busbar welding and with dual-string lead-wire welding of cell strings, supporting cells with two or more main grid lines. Method statements indicate how a joint is formed; they do not state the pull strength, void rate or peel result that a particular ribbon and cell combination will achieve. Those outcomes are measured rather than declared, and the measurement belongs in the acceptance protocol.
The yield figure needs a definition before it means anything
An A-grade yield rate above 97% is the most commercially sensitive number in the set and the least self-explanatory. The useful questions are not whether 97% sounds high, but what counts as a defect in that count, at which inspection point the count is taken, on what sample basis, and whether the figure covers the lay-up and bussing operations alone or the whole line. A yield figure without a defect definition cannot be tested, and a figure that cannot be tested cannot be enforced.
What the YN-PH800 documentation does not establish
A disciplined reading also means naming the limits, because the gaps are where procurement risk accumulates.
- No independent performance verification. The parameters are supplier-stated. No third-party test of throughput, repeatability or uptime is asserted in the available material, and no cycle-time or reliability figure is published.
- No certification claim. Machinery safety conformity, market-access marking and any electrical or pneumatic compliance documentation have to be requested directly and confirmed for the destination market.
- No cell-architecture guarantee beyond the stated scope. The machine is described as compatible with conventional monocrystalline and polycrystalline cells of standard specifications. Buyers working with other cell architectures should obtain explicit written confirmation rather than inferring compatibility from a general statement.
- No commercial terms inside the technical set. Price, payment schedule, warranty scope and spare-parts commitments sit in a separate commercial schedule and should be negotiated as such.
- No plant-level outcome. A stated yield rate describes the machine's intended output, not the output of a new line operated by a new team in a new building.
Fit boundaries: where a 6W–40W lay-up and bussing machine belongs
The YN-PH800 sits in the 6W–40W module band, which places it in small-format production rather than mainstream utility-module manufacturing. That is a fit statement, not a ranking. YNTECH supplies other lay-up and bussing models for different module classes, and where a string exceeds the stated 200–700 mm range, or a ribbon falls outside 2–6 mm width and 0.12–0.3 mm thickness, the YN-PH800's published specification no longer describes the application and a different model or a confirmed configuration has to be established.
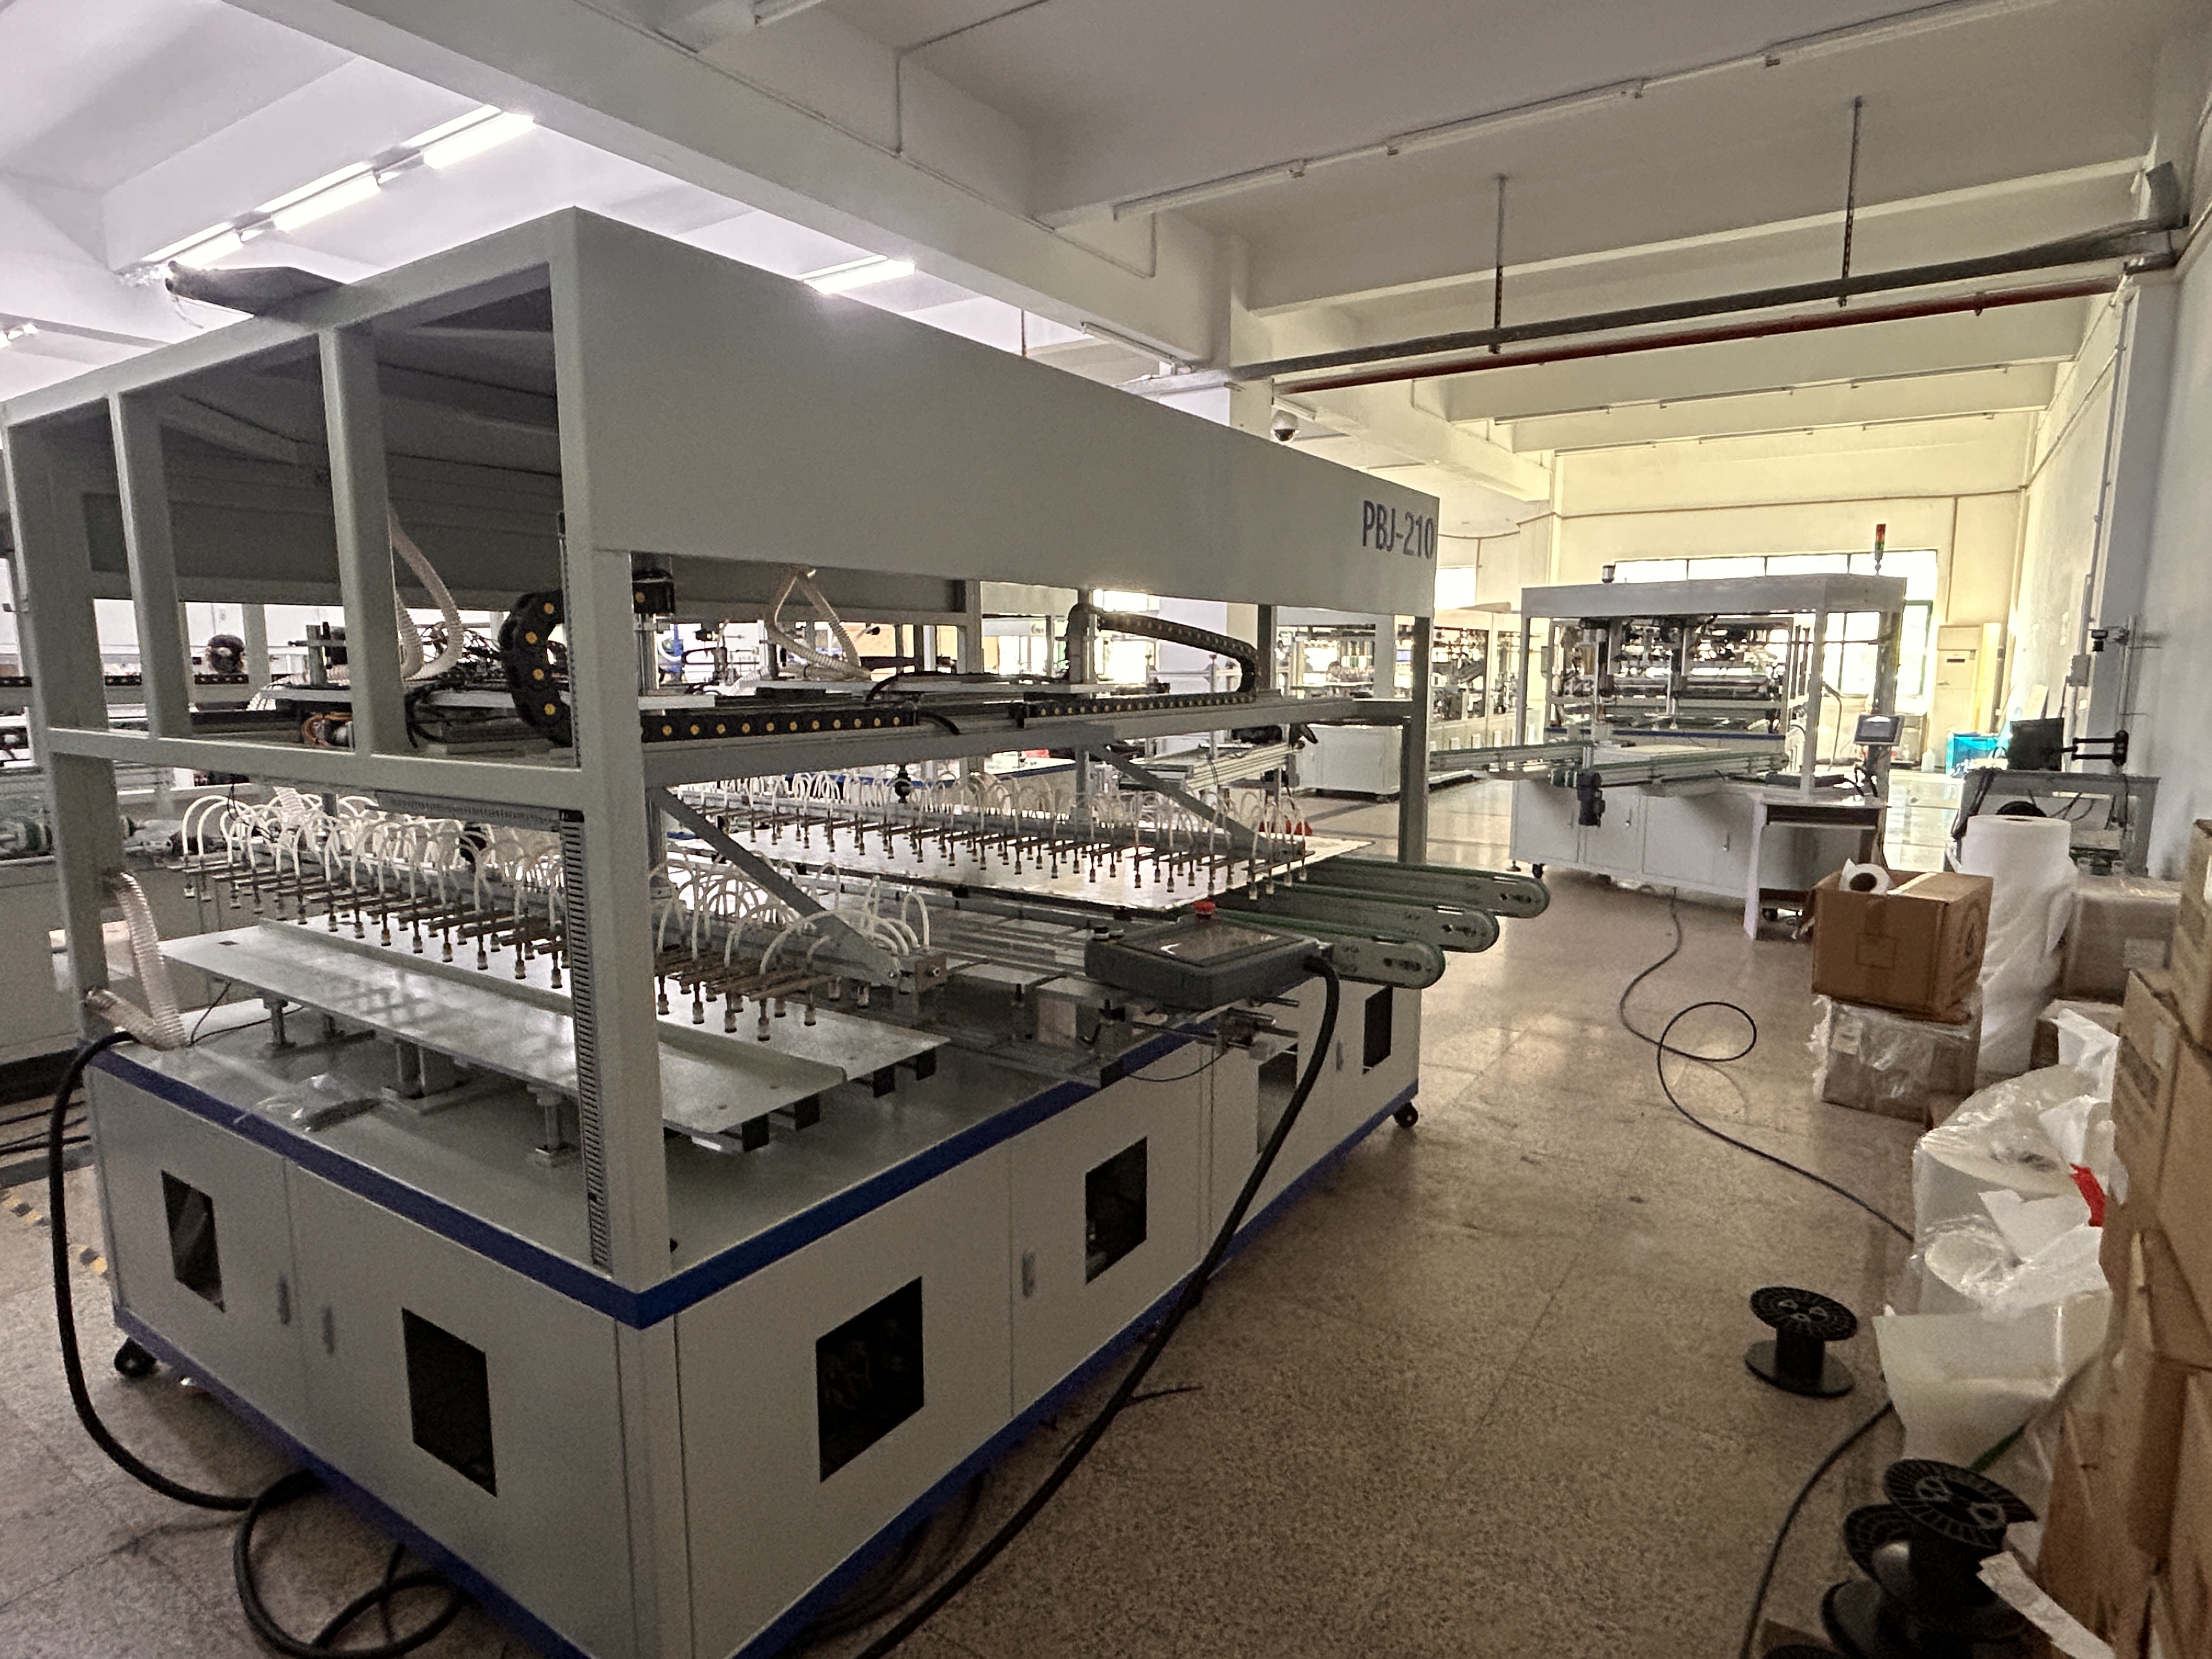
Within its band, the machine's scope of supply is broad for a single unit. YNTECH describes it as covering glass loading, EVA layout, busbar and isolation-strip application, lead soldering, power testing and backsheet covering, with layout assembly and busbar welding for 1-, 2-, 3- and 4-string configurations and one-click switching between single-string and double-string operation. The company also states that the line is designed to be operated by two operators. For a buyer, that breadth changes the qualification checklist: interfaces to the upstream stringer and the downstream laminator become contractual handover points, and responsibility for defects that appear at a station boundary has to be written down before installation rather than argued after it.
Site conditions belong in the same evidence file. The equipment is intended for an indoor, dust-controlled workshop at ambient temperatures of −10 °C to 40 °C, installed in a dry, well-ventilated area free of corrosive gases. A buyer whose building cannot demonstrate those conditions is not ready to accept delivery, regardless of how the machine performs in a supplier's showroom.
From specification sheet to factory acceptance
Between a parameter list and a signed acceptance certificate there is a short, unglamorous set of steps that most disputes trace back to.
- Build a configuration sheet from your own bill of materials. Module power class, string length, cell format and width, string spacing, ribbon width and thickness, and busbar count — each mapped against the published range.
- Request a signed, model-specific parameter confirmation. A catalogue page covering several models is not a confirmation of the configuration being quoted.
- Agree the factory acceptance test before the order. Define sample size, the module build used for testing, the measurements taken, the pass thresholds and who signs the result. YNTECH states 100% pre-shipment testing as standard practice; the buyer's question is what that test covers and whether the records travel with the machine.
- Fix the yield definition in contract language. Inspection point, defect categories, sample basis, and whether machine-attributable defects are counted separately from material and handling losses.
- Confirm utilities against the stated figures. 15 kW rated power and 0.5–0.8 MPa air supply are planning inputs; the plant should hold them within tolerance during continuous operation, not only at commissioning.
- Confirm the documentation package. Language, format, number of manual sets, training scope and the availability of remote technical support after handover.
Documentation checklist for buyers
The checklist below converts the discussion above into a document request list. It is written as a supplier obligation rather than a buyer preference, because each item closes a specific gap between a parameter and a decision.
| Document | Gap it closes | What to require |
|---|---|---|
| Model and configuration sheet | Specification drift between catalogue and order | Named model, module band, string and ribbon ranges, busbar count, mapped to your bill of materials |
| Signed parameter confirmation | Figures quoted for a different model | Model-specific values, dated and signed by the supplier |
| Utility and footprint schedule | Site and infrastructure mismatch | Rated power, air pressure and consumption, dimensions, weight, access requirements |
| Factory acceptance test protocol | Undefined pass criteria | Sample size, test module build, measurements, thresholds, signatories, record format |
| Written yield definition | Untestable 97% claim | Defect categories, inspection point, sample basis, machine-attributable scope |
| Conformity documentation | Market access and machinery safety | Issuing body, standard number and edition, scope, validity, issued for the model supplied |
| Component certificates | Hidden dependency on unbranded controls | Certificates or declarations for bought-in controls and pneumatic components, where available |
| Material certificates | Construction claims without traceability | Grade documentation for the stated 304 stainless steel components |
| Site requirement statement | Installation in unsuitable buildings | Ambient temperature range, dust control, ventilation, exclusion of corrosive gases |
| Training and manual package | Operator dependence and knowledge loss | Language, manual sets, video or on-site training scope, operating and maintenance instructions |
| Warranty and support terms | Unclear lifecycle cost | Warranty period and exclusions, spare-parts list, remote technical support arrangement |
| Packing and export documents | Damage and customs delay in transit | Packing specification, crate protection, shipping documents and inspection records |
Outlook: documentation discipline as a purchasing advantage
Publicly comparable, like-for-like performance data for lay-up and bussing machines remains limited, which is why supplier documentation and buyer-side acceptance testing carry most of the qualification burden. Two market signals make that burden worth carrying deliberately. First, capacity build-out continues to pull equipment through the supply chain, and forecasts of the kind cited earlier imply sustained order volumes rather than a one-off spike. Second, commercial lead times are long enough to matter: one published guide to a 100 MW module line cites a typical delivery window of six to nine months for the line itself, which means a buyer who discovers a documentation gap after the order usually discovers it at the least convenient moment. Adding building works, utility upgrades and operator training to that window argues for planning twelve months or more from decision to stable output.
None of this makes the YN-PH800 a better or worse machine than a competitor; that judgment depends on measured performance in a specific plant, which no specification sheet can supply. What it does mean is that the published figures are useful precisely because they are specific. A 200–700 mm string range, a 78–210 mm cell width, a 2–6 mm busbar width and a 0.12–0.3 mm busbar thickness can all be checked against a real bill of materials, and a yield claim above 97% can be converted into a testable contract term. Equipment described this concretely is easier to qualify — and easier to hold to account once it is running.
A general company brochure covering YNTECH's module production equipment range is available for download: YNTECH product brochure (PDF).
FAQ
What do the YN-PH800 parameters actually prove?
They establish design and capability, not conformity. The published set covers the 6W–40W module band, a 200–700 mm string length, 78–210 mm cell width, 1–10 mm string spacing, 2–6 mm busbar width, 0.12–0.3 mm busbar thickness, high-frequency electromagnetic welding, 15 kW rated power and a 0.5–0.8 MPa air source. Those values show what the machine is engineered to handle and which utilities it needs. They do not show independent verification, and they are not a certificate.
Is the YN-PH800 certified, and which certificate should a buyer request?
No certificate or declaration of conformity is asserted in the documentation available for this article, so certification should not be assumed. A buyer should ask the supplier to name the conformity documents that apply to the machine in the destination market, including issuing body, standard number and edition, scope of application and validity. Module standards such as IEC 61215 and IEC 61730 relate to the finished module rather than to the production equipment, so they cannot substitute for machinery documentation.
How should the stated A-grade yield rate above 97% be verified?
By turning it into a measured test. Agree on the definition of an A-grade module, the inspection point where the count is taken, the sample size, and whether the figure covers only the lay-up and bussing operations or the full line. Then place the check inside the factory acceptance test, using your own cells, ribbon and module format, and record the result in the acceptance report. The published figure is a company-stated target and does not guarantee the output of a particular plant.
Which module formats fit the YN-PH800's stated ranges?
Modules in the 6W–40W class, with cell string lengths of 200–700 mm, cell widths of 78–210 mm, string spacing of 1–10 mm, and busbars 2–6 mm wide and 0.12–0.3 mm thick. The machine supports 1-, 2-, 3- and 4-string layouts with one-click switching between single-string and double-string operation, double-end busbar welding and dual-string lead-wire welding, and cells with two or more main grid lines. A module outside those ranges falls outside the published specification and needs a different model or a confirmed configuration.
What documentation should accompany a quotation?
At minimum: a model and configuration sheet mapped to your bill of materials; a signed parameter confirmation; a utility and footprint schedule; a factory acceptance test protocol with sampling and pass criteria; a written yield definition; conformity documentation for machinery safety with issuing body, standard, edition, scope and validity; component certificates for bought-in controls and pneumatics where available; material certificates for the stated 304 stainless steel; the site requirement statement; a training and manual package in the agreed language; warranty, spare-parts and remote-support terms; and packing and export documents.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.