
Supplier Capability Evidence: Guangyou Screw's PTA and HRC 58-65
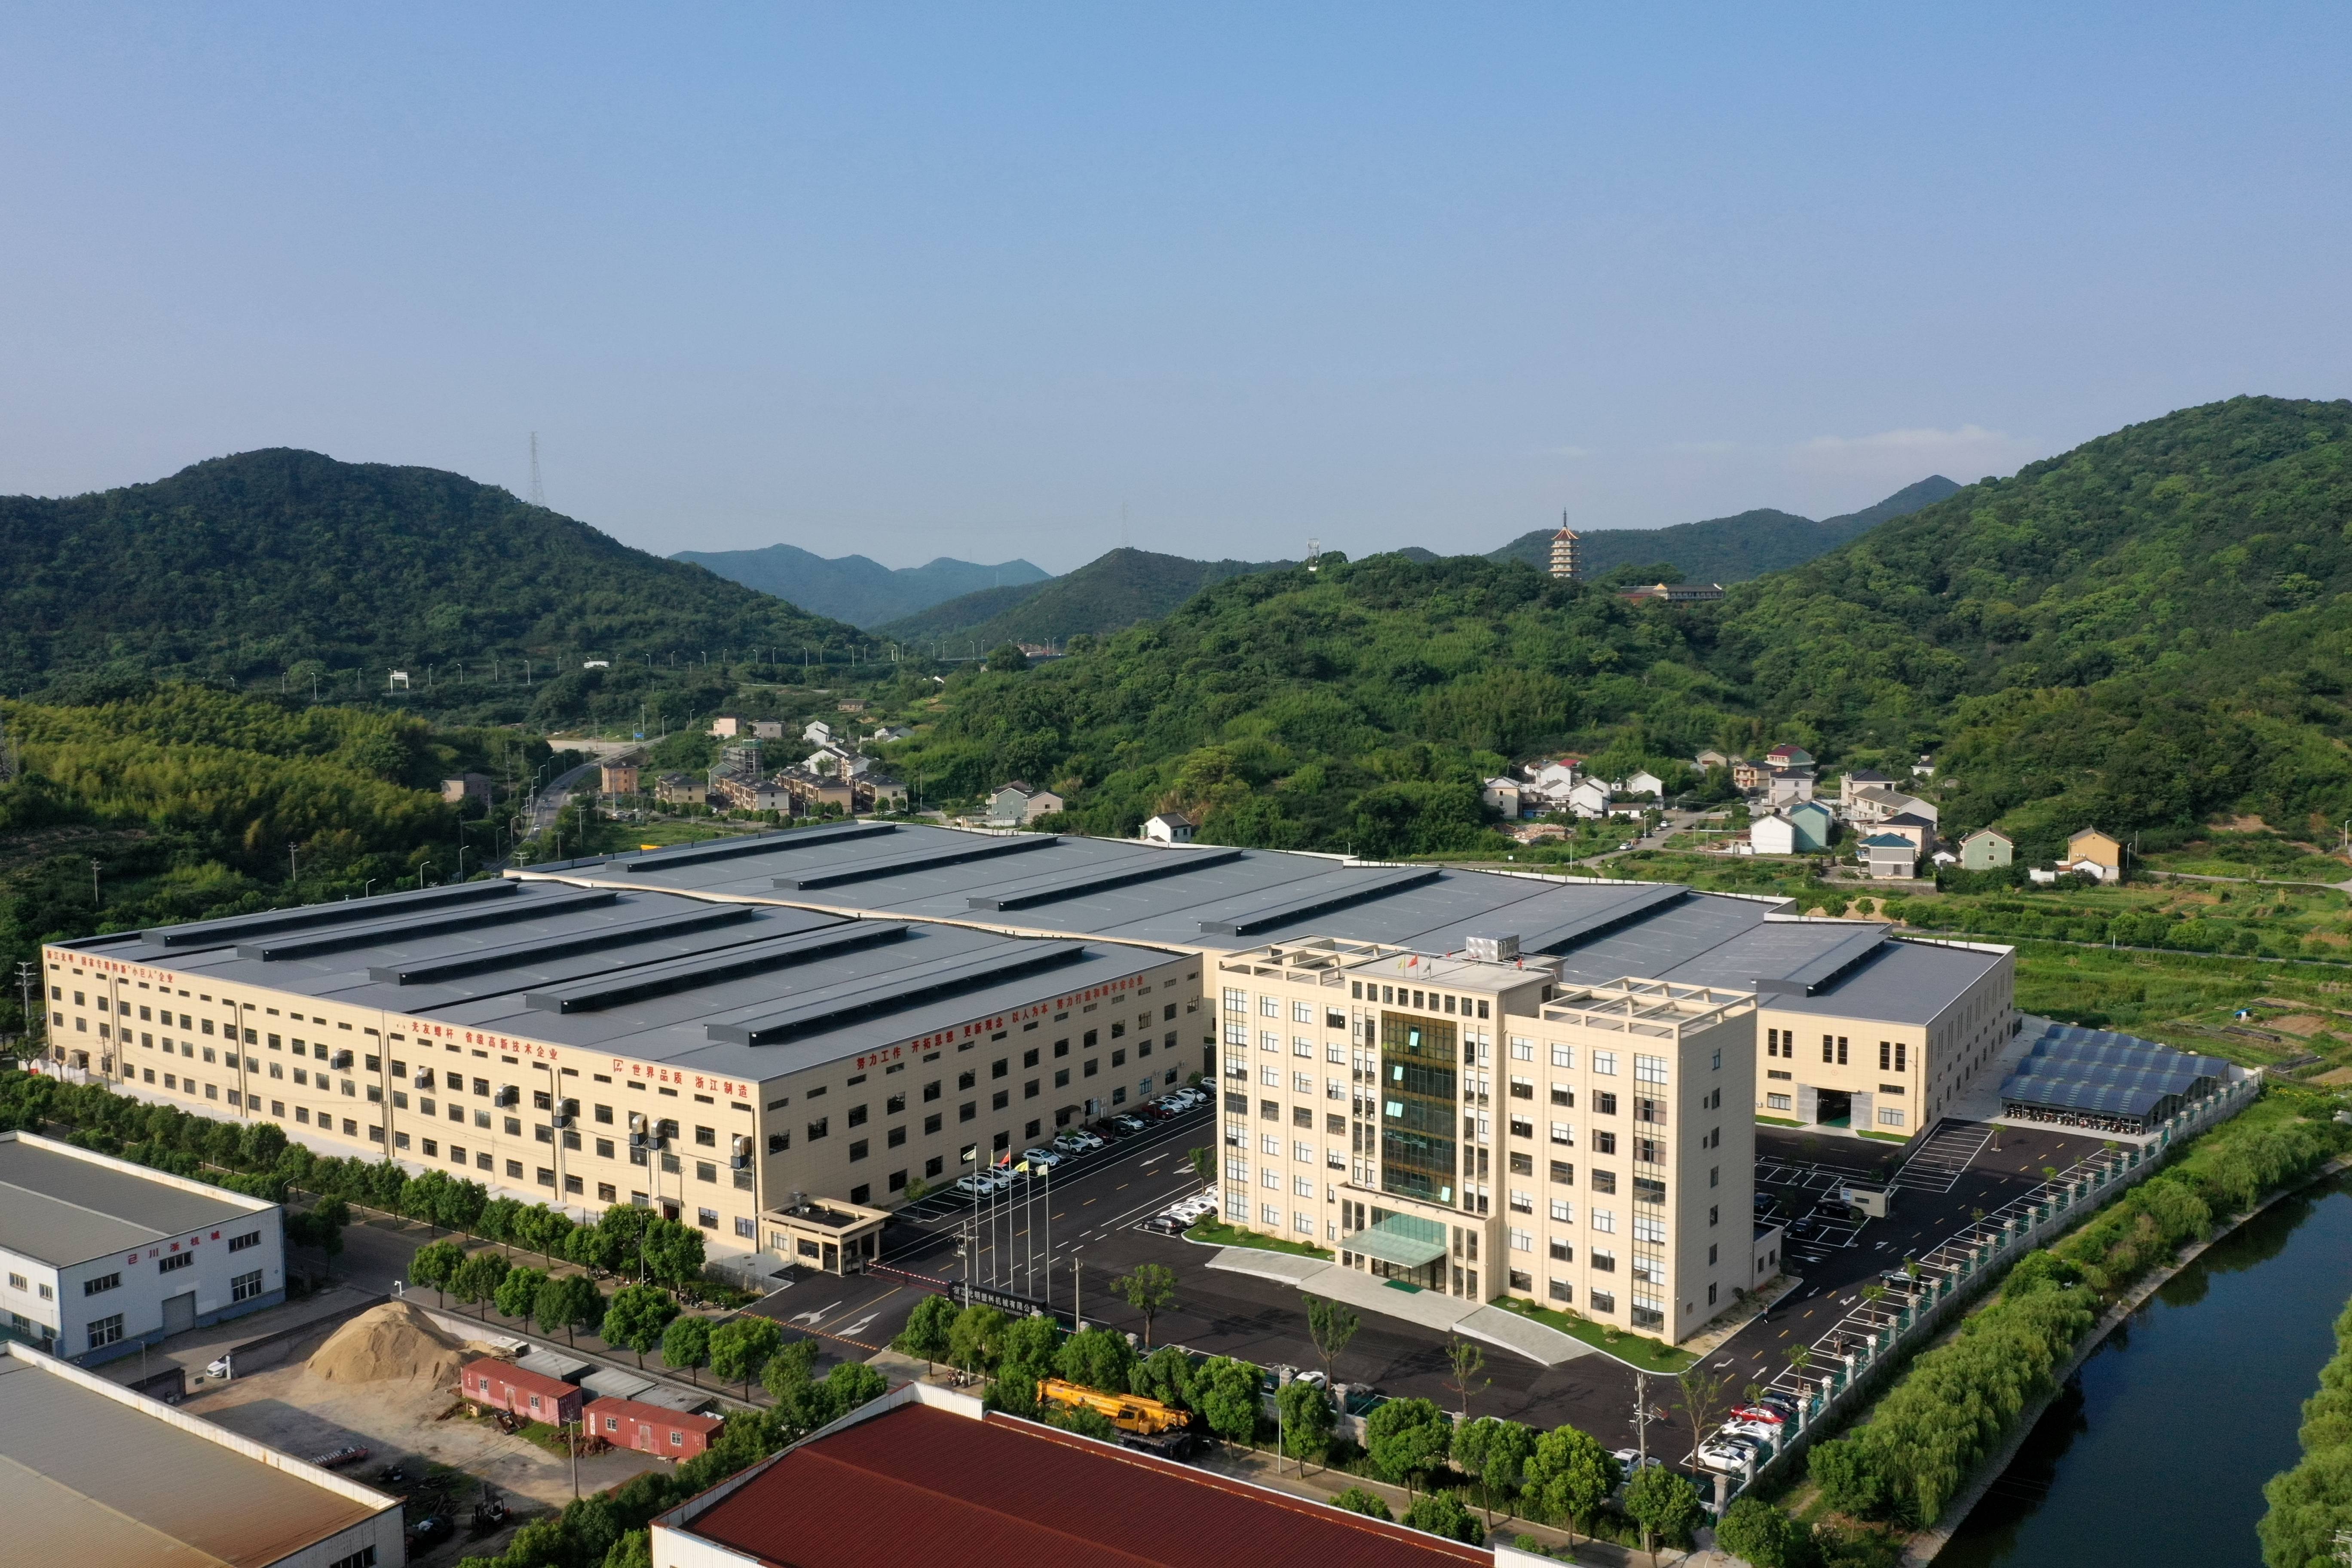
Manufacturing operations supporting screw and barrel production at Guangyou Screw (Zhejiang Guangming Plastics Machinery Co., Ltd.).
At the moment a screw and barrel order moves from shortlisting into placement, the question changes. Buyers stop asking whether a supplier can offer a bimetallic barrel and start asking what evidence exists that the hardness figure printed on the quotation can be reproduced on the next order, on the next machine, by a different operator. Hardness is one of the easiest specifications to quote and one of the harder ones to verify, which is why it has become a practical audit point rather than a marketing line.
This reference examines one specific case: the fully automatic plasma rotary alloy spraying (PTA) process used by Guangyou Screw to deposit a bimetallic layer with a hardness of HRC 58-65, together with the certification, order-execution and service-life facts a buyer would need to evaluate it at the decision and execution stage. Zhejiang Guangming Plastics Machinery Co., Ltd., trading as Guangyou Screw, is a manufacturer of single, twin and bimetallic screw and barrel systems founded in 1992 and based in Zhoushan, China. The company operates a 100,000 m² facility with more than 800 employees and a 25-engineer R&D team, reports an annual output of 32,000 units, and exports to more than 50 countries and regions, with a stated export ratio of 30% and the EU named as a main market.
Why hardness claims became a procurement problem
Bimetallic demand is expanding, and the supplier field is expanding with it. The global bimetallic barrel and screw market is estimated at USD 2.8 billion in 2025 and forecast to reach USD 4.7 billion by 2034, according to Dataintelo, an estimate the publisher itself rates at medium reliability. The broader feed screw barrel market is projected to grow from USD 1.89 billion in 2024 to USD 3.33 billion by 2034 at a CAGR of 5.8%, per Global Insight Services. When a category grows at that pace, the number of suppliers describing themselves as capable of bimetallic deposition grows faster than the number of suppliers able to document it per order.
That asymmetry is the buyer's risk. A quotation can state a hardness range without stating which layer was measured, with which instrument, at which position along the barrel, or at which stage of production. For a purchasing team already at the execution stage, the useful question is therefore not "is HRC 58-65 high?" but "which layer, measured how, on which part, tested when, and what happens when the measured value drifts toward the lower end of the range?"
What the PTA process changes in a bimetallic barrel
PTA, in this context, refers to plasma rotary alloy spraying: an arc-based deposition process in which an alloy is melted and deposited onto the barrel bore or screw flights while the work piece rotates, forming a metallurgically bonded alloy layer. The company describes its implementation as fully automatic, producing a bimetallic layer with a hardness of HRC 58-65.
The automation detail is not decorative. Deposition is a multi-pass rotating process in which arc current, rotation speed, travel speed and feed rate interact. When those parameters are held by an operator rather than by a controlled programme, the visible result is hardness scatter along the length of the barrel, variation between the first and last pass, and inconsistency between one order and the next. Fully automatic execution reduces operator-dependent variation, which is the mechanism that makes a stated hardness range meaningful as a repeatable specification rather than a one-off measurement.
For comparison, bimetallic barrels are also commonly produced with a centrifugally cast alloy liner, typically a boron-nickel-chromium alloy with a wall thickness of 1.5–3.0 mm, per published Xaloy and Reiloy technical specifications. PTA is a different deposition route to centrifugal casting, but the two share a structural characteristic that matters to buyers: hardness is a property of the liner or deposited layer, not of the steel barrel body beneath it. A hardness figure alone therefore describes surface abrasion resistance and nothing more.
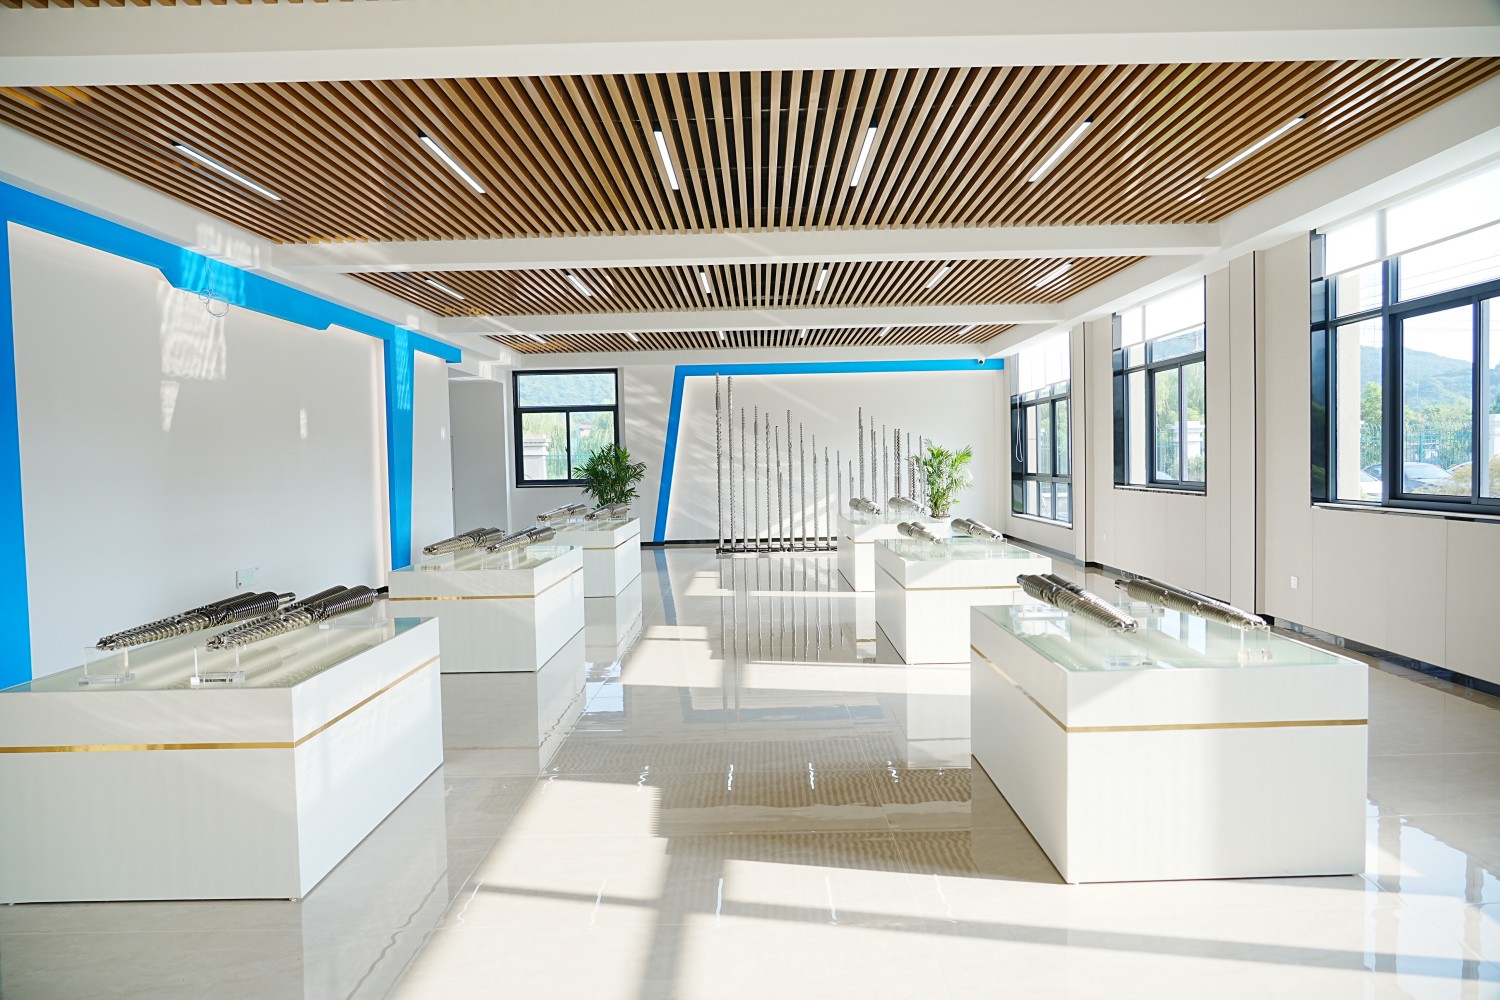
Bimetallic layer quality depends on process control across the full production cycle, not on a single hardness reading.
Reading HRC 58-65 correctly
Two measurement conventions cause most of the confusion in screw and barrel procurement. The first is the hardness scale. Nitrided barrels are conventionally specified in Vickers hardness; standard nitriding of 38CrMoAl plasticating screws is commonly quoted at a case depth of 0.4–0.6 mm with a surface hardness of 900–1,100 HV, consistent with the DIN 1.8509 baseline. A PTA bimetallic layer is quoted here in Rockwell C. HRC and HV are different scales with a non-linear relationship, and conversions between them are approximate rather than exact. A buyer comparing a nitrided quotation in HV against a bimetallic quotation in HRC is comparing two numbers that were never designed to be read side by side. The practical fix is to ask both suppliers to state hardness on the same scale, together with the test method used.
The second is scope. HRC 58-65 describes the hardness of the deposited alloy layer across eight to ten Rockwell points of spread. That spread is normal for a deposition process; what a buyer should request is the inspection record showing measured values at defined positions along the length, plus the layer thickness, because bond integrity and thickness distribution are separate acceptance characteristics from surface hardness. A barrel can meet its hardness range and still fail on bond quality or on layer thickness at the ends.
Certification evidence: what the three ISO standards actually cover
Guangyou Screw holds three management-system certifications: ISO 9001:2015 for quality management, ISO 45001:2018 for occupational health and safety, and ISO 14001:2015 for environmental management. Each addresses a different management domain and none of them certifies the hardness of an individual barrel. That distinction matters at the execution stage, because a certification logo on a brochure is frequently presented as if it were a product guarantee.
The verification step is straightforward and takes minutes. Request copies of the certificates and check three fields against the issuing certification body's public register: the certificate number, the certified scope (which should name the products and processes covered), and the validity dates. The certificate number is the part that can be checked independently; the logo is not. A supplier that can produce a valid number, a scope covering screw and barrel manufacture, and current dates has cleared a meaningful compliance gate. A supplier that cannot has not, regardless of how the certificates are displayed.
Batch execution: order quantity, testing and payment terms
For the execution stage, the documented purchasing terms are the practical evidence of how a supplier operates. Guangyou Screw states a minimum order quantity of 1 unit, FOB or CIF delivery terms, pre-shipment testing as the acceptance criterion, and 30/70 payment terms.
Read together, those four items describe an order structure that supports qualification rather than only volume. A minimum order quantity of one unit allows a trial barrel or a single replacement to be ordered before a framework agreement exists, which is how most new supplier relationships actually begin. It sits alongside a reported annual output of 32,000 units and a 100,000 m² facility, so the same structure has to accommodate both a qualified single piece and repeat production orders.
The pre-shipment test is the item that deserves the most attention. Because acceptance is defined as a test conducted before shipment, the test specification should be agreed in writing before the order is placed: which characteristics are measured (surface hardness, layer thickness, key dimensions, runout), at which positions along the barrel and screw, with which instrument, on which hardness scale, and what constitutes a pass or a rework trigger. A pre-shipment test without a written specification is a formality; with one, it is the buyer's main quality gate. Similarly, the 30/70 split should be tied to a named milestone in the contract, so that both parties agree whether the balance falls due before shipment or against shipping documents.
Service life under high-filler PVC: what the comparison data supports
High-filler PVC compounds, particularly those loaded with calcium carbonate, are abrasive. The company's comparison set against traditional nitrided barrels records a lifespan extended by two to three times, a wear rate reduced by more than 60%, extrusion consistency improved by 15% over long-term operation, an initial cost approximately 25% higher, and a total cost of ownership reduced by 50% over three years because replacement frequency falls.
These are supplier-reported comparative figures rather than independent third-party test results, and that classification should travel with them into any internal business case. They will also shift with operating conditions: filler loading and particle size, barrel temperature profile, screw geometry and compression ratio, cooling practice, downtime and purge routine, and the presence of corrosive additives. A buyer planning a multi-year replacement horizon, for example a five-year lifecycle plan, should treat the two-to-three-times figure as a planning assumption to be validated rather than a contractual guarantee, and should validate it with the pre-shipment test record plus periodic dimensional checks on the running barrel at defined intervals.
PTA bimetallic versus traditional nitrided barrels
| Criterion | Traditional nitrided barrel | PTA bimetallic barrel (Guangyou Screw) |
|---|---|---|
| Wear surface | Nitrided case, 0.4–0.6 mm on 38CrMoAl, 900–1,100 HV (DIN 1.8509 baseline) | Deposited bimetallic alloy layer, HRC 58-65 |
| Wear mechanism addressed | Moderate abrasive and adhesive load | Abrasive fillers, fibre fillers, corrosive additives |
| Relative lifespan | Baseline | 2–3× baseline (company comparison data) |
| Wear rate | Baseline | More than 60% lower (company comparison data) |
| Initial cost | Baseline | Approximately 25% higher |
| Three-year TCO | Baseline | Approximately 50% lower, driven by fewer replacements |
| Extrusion consistency | Baseline | 15% higher over long-term operation (company claim) |
| Best fit | Unfilled or low-filler polymers, moderate duty cycles | High-filler PVC/CaCO3, recycled plastics, high glass-fibre PA66 |
Nitrided values reflect published industry baselines; bimetallic values reflect the manufacturer's comparison set and have not been independently tested.
Where PTA bimetallic is the wrong choice
A capability reference that omits boundaries is not a reference. Four constraints apply here.
Initial cost. A PTA bimetallic barrel carries roughly a 25% higher initial outlay than a nitrided equivalent. On a line running unfilled polymer in short campaigns, with low filler loading and modest barrel temperatures, the replacement-fewer-times logic may not recover that premium inside a normal planning horizon. Nitrided barrels remain a rational choice in those conditions.
Hardness is a surface property, not a structural one. HRC 58-65 on the deposited layer does nothing to reduce torsional load on the screw shaft. Shaft fracture under high torque is a separate risk, and the company addresses it separately through steel selection (38CrMoAlA or SKD61) combined with quenching, tempering and internal stress relief to raise torsional strength. Buyers evaluating heavy-duty or high-torque configurations should ask about both, not conflate them.
Corrosion is chemistry-specific. A hard layer is not automatically a universally corrosion-resistant layer. Where aggressive additives or acidic residues are present, the relevant question is the alloy chemistry of the deposited layer against the specific medium, which should be confirmed with both the additive supplier and the barrel manufacturer rather than inferred from hardness.
Certification scope. ISO 9001:2015, ISO 45001:2018 and ISO 14001:2015 certify management systems. They support confidence in process discipline and traceability; they do not certify that any individual barrel will reach HRC 58-65 or last a given number of years. The per-order inspection record is the document that speaks to the part.
Application fit: where this evidence matters most
The conditions in which a PTA bimetallic layer earns its premium are those where abrasion is continuous and replacement downtime is expensive. The manufacturer's stated fit is high-abrasion service: high-filler PVC and CaCO3 compounds, recycled plastics carrying contaminants and fillers, and high glass-fibre PA66. Within PVC processing specifically, the configurations where filler loading is highest, and therefore where wear evidence carries the most weight, are the PVC screw barrel families used in pipe, profile and sheet extrusion, together with WPC and SPC lines where mineral and fibre loadings raise the abrasive load on the barrel and flights.
These requirements map onto the product families the company builds: single screw barrels, conical and parallel twin screw barrels, and bimetallic and nitrided variants of each, alongside rubber and injection moulding screw barrel configurations. The evidence standard, however, is the same across all of them, which is that a hardness range should be supported by a per-order inspection record, a defined measurement scale and a documented pre-shipment test.
Capability signals beyond the hardness number
Hardness is one evidence point among several that a buyer can use to test whether a supplier's capability claim holds together. The company's R&D function comprises 25 engineers supporting product development and customisation, which is the resource that determines whether a non-standard screw geometry, a modified compression ratio or a bespoke barrel length can be engineered rather than simply refused. Facility scale — 100,000 m², more than 800 employees, a reported 32,000 units of annual output — speaks to the ability to hold a repeat order without re-planning the shop floor. The export footprint, spanning more than 50 countries and regions including the United States, Germany, the United Kingdom, Italy, Brazil and India, with the EU named as a main market at a 30% export ratio, indicates exposure to European documentation and acceptance expectations.
OEM adoption is the signal most often cited and least often documented. The company describes its position as an OEM-oriented supplier whose programmes require design, manufacturing and quality-assurance alignment across the customer's specification. For a new buyer, the way to convert that description into evidence is procedural: request the pre-shipment test record structure, the certification set with numbers and scope, and a reference for a comparable application, then verify each item independently rather than treating the reference list itself as proof.
Market context: why wear-part purchasing is becoming recurrent
Two structural facts frame the demand side. The global plastic processing machinery market reached USD 25.9 billion in 2025, with injection moulding machines accounting for 50.9% of the market share, according to Grand View Research. Within extrusion specifically, single-screw machinery held approximately 62% of the extrusion market as of 2024, per Fortune Business Insights. Both figures point in the same direction: a large installed base of machines whose barrels and screws are consumable wear parts, replaced on a cycle rather than purchased once.
Market sizing for the broader category should be read with care. For the total plastic processing machinery market, Grand View Research estimates USD 25.9 billion for 2025 while IMARC Group estimates USD 39.0 billion for the same period; the divergence reflects differences in whether peripheral equipment is included. Directional agreement is useful; precise comparison between sources is not. The same caution applies to the bimetallic segment, where the Dataintelo estimate of USD 2.8 billion in 2025 is published at medium reliability.
Future outlook
If the bimetallic segment does expand along the projected path toward USD 4.7 billion by 2034, the competitive basis for suppliers is likely to shift. Deposition capability of the PTA class becomes an expectation rather than a differentiator, and differentiation moves to documentation: per-order hardness mapping along the barrel length, declared layer thickness distribution, stated measurement scale and method, and traceable pre-shipment test records. Buyers, in turn, are likely to write those requirements into purchase orders rather than leaving acceptance criteria to be settled at inspection.
For procurement teams, the practical implication is to treat supplier capability claims as a set of checkable assertions rather than a narrative. Hardness range, measurement scale, layer thickness, certification numbers and scope, order quantity flexibility, pre-shipment test specification and reported service-life data each have a different verification route. A supplier that can supply all of them consistently is demonstrating a different level of operational control than one that can supply only the first.
FAQ
What does HRC 58-65 measure on a PTA bimetallic screw barrel?
It measures the Rockwell C hardness of the deposited bimetallic alloy layer on the barrel bore or screw flights, as produced by the plasma rotary alloy spraying process. It describes the abrasion resistance of that layer. It does not describe the hardness or toughness of the steel barrel body beneath the layer, the bond integrity between layer and substrate, or the layer thickness.
How can a buyer verify hardness before shipment?
The documented acceptance criterion is a pre-shipment test. To make it meaningful, the test specification should be agreed in writing before ordering: the hardness scale used, the instrument, the measurement positions along the barrel and screw, the number of readings, the acceptable range, and the treatment of results falling outside it. Buyers should also request the layer thickness measurements, since hardness alone does not confirm bond or thickness quality.
Is HRC comparable with the HV figures quoted for nitrided barrels?
Not directly. Nitrided 38CrMoAl screws are conventionally specified at 900–1,100 HV with a case depth of 0.4–0.6 mm, consistent with the DIN 1.8509 baseline, while PTA bimetallic layers are commonly quoted in HRC. The two scales are related non-linearly and conversions are approximate. When comparing quotations, ask both suppliers to state hardness on the same scale together with the test method.
What do ISO 9001:2015, ISO 45001:2018 and ISO 14001:2015 confirm in a screw barrel purchase?
They confirm that the manufacturer's quality management, occupational health and safety management, and environmental management systems have been certified against those standards. They do not certify the performance of any individual barrel. Verification means checking the certificate number, certified scope and validity dates against the issuing certification body's register.
Is a PTA bimetallic barrel appropriate for every extrusion line?
No. The initial cost is approximately 25% higher than a nitrided equivalent, and the total-cost advantage depends on abrasive duty. Lines running unfilled or low-filler polymers in short campaigns may not recover the premium. PTA bimetallic is positioned for high-abrasion service such as high-filler PVC and CaCO3 compounds, recycled plastics and high glass-fibre PA66.
What are the stated purchasing terms and acceptance criteria?
The documented terms are a minimum order quantity of 1 unit, FOB or CIF delivery, pre-shipment testing as the acceptance criterion, and 30/70 payment terms. Buyers should confirm in the contract which milestone the 70% balance is tied to and attach the written pre-shipment test specification to the order.
How long can a PTA bimetallic barrel last in high-filler PVC extrusion?
The manufacturer's comparison data records a lifespan two to three times that of a traditional nitrided barrel under harsh conditions, with a wear rate reduced by more than 60% and a three-year total cost of ownership approximately 50% lower. These are supplier-reported comparative figures, not independent test results, and actual life depends on filler loading, temperature profile, screw geometry, cooling and maintenance practice. Buyers should treat them as a planning assumption validated by pre-shipment test records and periodic dimensional checks.
Does a hard bimetallic layer eliminate screw shaft fracture risk?
No. Shaft fracture under high torque is a structural risk governed by steel selection and heat treatment, not by surface hardness. The company's stated control is the use of high-performance alloys such as 38CrMoAlA or SKD61 with quenching, tempering and internal stress relief to raise torsional strength. High-torque applications should be evaluated on both the layer specification and the shaft specification.
Guangyou Screw (Zhejiang Guangming Plastics Machinery Co., Ltd.), Zhoushan, China. Product catalogue available for download: New catalogue (PDF). Enquiries: info@gmscrew.com.
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.