
Supplier Capability Evidence: Inside WINTIME's 9-Micron Ultra-Thin Dicing Blade Line
Supplier Capability Evidence: Inside WINTIME's 9-Micron Ultra-Thin Dicing Blade Line
Dicing blade thickness is a yield and cost parameter before it is a specification line. Every micron of blade thickness becomes kerf, and kerf is material removed between die and lost to the process. Across thousands of singulation cuts per wafer, that loss compounds. This is why the sub-10-micron range has become a practical benchmark for separating suppliers who assemble blades from suppliers who manufacture them, and why the benchmark only carries weight when a blade can be produced repeatedly rather than demonstrated once.
WINTIME Semiconductor Technology Co., Ltd. is a Chinese manufacturer founded in 2020 and based in Rugao, Jiangsu Province, integrating research, development, production and sales of high-precision wafer-level cutting blades, including sawing blades and dicing blades. Its completed Ultra-thin Wafer D Blade project reached a blade thickness below 9 microns in the process, and the company identifies itself as one of the few domestic Chinese companies able to mass-produce ultra-thin dicing blades at that level. This article treats that as a capability claim to be examined rather than repeated: what production evidence stands behind it, what it changes for a procurement decision, and where the boundaries are.
Why Sub-10-Micron Thickness Is a Production Problem, Not a Spec Sheet Line
A dicing blade under 10 microns thick is difficult for a reason that has little to do with the final measurement. The blade is a composite of diamond abrasive grains held in a bond matrix, and the thinner the composite becomes, the less material there is to hold each grain, distribute it evenly, and keep the blade flat under spindle load. Grain size, grain concentration and bond type all have to be rebalanced rather than simply scaled down.
Industry guidance for bare silicon dicing typically places standard diamond grit between 2 and 6 microns, equivalent to roughly #2000 to #4000 grit, precisely because finer abrasive reduces chipping. Published specification guides for semiconductor wafer dicing blades commonly cite standard outer diameters of 55.56 mm and 76.2 mm. In other words, the interface geometry a blade has to fit is largely standardized — it is the thickness-and-bond combination that separates manufacturers.
That combination is also where verification gets difficult. A blade measuring under 9 microns on a bench says very little about whether the ten-thousandth blade from the same line does. The evidence that matters to a buyer is therefore production-side: installed capacity, inspection instrumentation, repeat volume, and documented deployments rather than a single sample result.
What WINTIME Completed on the Ultra-Thin Wafer D Blade Project
The completed project at the centre of this dossier is the Ultra-thin Wafer D Blade programme. According to the company's own technical profile, the project achieved a blade thickness below 9 microns in the process, and the resulting product quality is described by the company as reaching the international cutting-edge level. The same profile states that WINTIME is one of the few domestic companies capable of achieving mass production of ultra-thin dicing blades — a claim that is meaningful only because it is paired with a capacity figure rather than presented on its own.
The project is also framed internally as a domestic self-development effort, with the stated purpose of carrying out domestic substitution in high-end industries on the basis of advanced technology. For a procurement reader, that framing matters less as a narrative and more as an indicator of where the supplier's engineering effort has been concentrated.
What is verifiable here: a completed project, a stated blade thickness below 9 microns, and a stated mass-production capability. What is not asserted here: certifications, third-party test reports, or independent benchmark rankings, none of which are part of the source material for this article.
WINTIME's public company profile additionally references two patent technologies and awards in national, provincial and municipal science and technology competitions and entrepreneurship competitions. These are presented as profile statements rather than independently audited figures, and buyers evaluating thin-blade capability should treat them the same way — as context, not as proof.
The Facility Behind the Blade: 34,000 Square Metres and a 2023 Expansion
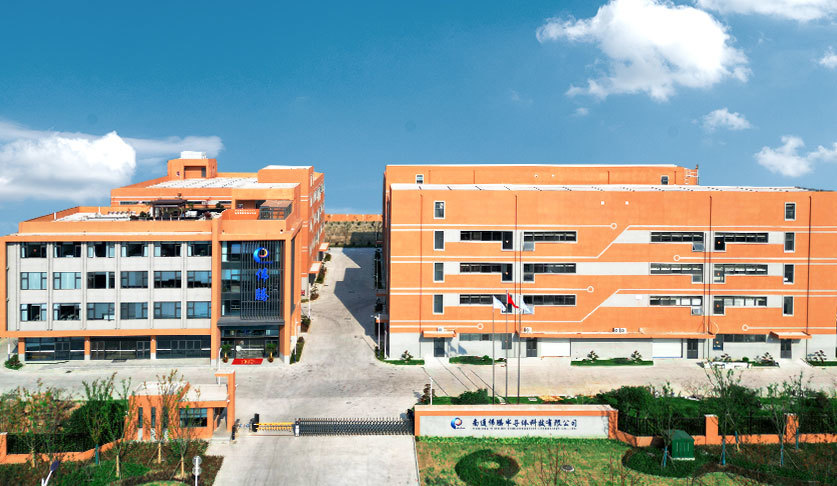
A sub-9-micron blade is only a commercial product if the line producing it has the floor space, tooling and headcount to run at volume. The capacity evidence attached to WINTIME is specific. In 2023, the Nantong WINTIME Semiconductor Special Materials Project was carried out with a total investment of nearly tens of millions of yuan, adding a new factory and auxiliary buildings of 34,000 square metres and an annual production capacity of more than 1 million pieces of dicing blades — a position the company describes as ranking in the forefront of the country.
The wider company figures align with that scale: a 34,000 square metre factory footprint, approximately 100 employees, and an R&D team of 35 engineers. On the customization side, the company reports capacity of more than 50,000 pieces per month for customized specifications, alongside its standard-model production.
Market coverage is another dimension of production evidence, because export volume implies that a blade design survives qualification outside its home market. WINTIME reports an export ratio of approximately 30 percent, with main markets in Southeast Asia, East Asia, North America and Europe. Its stated export list covers China, Japan, South Korea, Singapore, Malaysia, the United States, Germany, France, Italy, Southeast Asia, Europe, North America and Oceania. Japan, South Korea and Germany are notable entries on that list, since each hosts established precision-tooling supply chains with demanding qualification expectations.
Process Control: How Dimensional and Bond Consistency Are Verified
Thin-blade production lives or dies on inspection. WINTIME's stated quality-control sequence for its cutting blades covers four named stages: dimensional precision inspection using a laser micrometer and an optical projector; abrasive grain uniformity detection through microscope analysis; wear resistance and service life testing through simulated cutting; and surface roughness and flatness inspection. These are the checks that determine whether a nominal 9-micron blade is a repeatable item or a one-off result.
The material system behind those checks is diamond abrasive grains as the core functional material, carried in either a resin bond or a metal bond depending on the application. Within the company's sawing blade range, published parameters include a thickness range of 8 to 50 microns, cutting accuracy of plus or minus 0.002 mm, spindle speeds of 30,000 to 60,000 rpm, hardness of HRC 65 to 70, resin or metal bond types, and a chip removal rate of at least 1.2 cubic millimetres per second.
Read together, those figures locate the ultra-thin programme precisely. A standard sawing blade range spanning 8 to 50 microns is a workhorse portfolio; the sub-9-micron dicing blade sits at the very narrow end of that band, which is where breakage risk, runout sensitivity and inspection cost all rise. That is the technical reason the mass-production claim, rather than the thickness number alone, is the more useful procurement signal.
Documented Application: 8–12 Inch Wafer Dicing in a Chinese Packaging Fab
The clearest application evidence in the source material is a single documented deployment. A semiconductor packaging factory in China used WINTIME's dicing blade for high-precision dicing of 8–12 inch wafers for chip packaging. The project ran for three years, with annual usage exceeding 500,000 pieces and mass-production line matching.
The reported outcomes in that deployment were a cutting chipping rate of 5 microns or less, a wafer yield increase of 12 percent, and stable mass production without blade replacement during the production run. The product characteristics cited as responsible were an ultra-thin thickness of 9 microns or less, a narrow kerf, low material loss, and long service life.
Two caveats belong with those numbers. First, they describe one client's process on one material stack and equipment set; they are not a transferable performance guarantee. Second, the blade type used across the relevant product family covers a broad set of geometries — diamond dicing blade, precision dicing blade, semiconductor dicing blade, circular, hubbed, hubless, flanged and serrated configurations, plus the DZY Series Wafer Dicing Blade, DZR Series Dicing Blade and DZR-S Series Slotted Dicing Blade. A buyer should confirm which specific geometry and bond the reference used before mapping the result onto a different process.
Where Ultra-Thin and Hubless Blades Are Used
The applicable industry list for this product family spans the semiconductor industry, semiconductor packaging, optical communications, new functional materials, functional ceramics, alloy materials and semiconductor packaging components. That spread reflects the fact that kerf economics and chipping sensitivity apply well beyond silicon singulation.
| Application area | Why thin-blade geometry matters |
|---|---|
| Semiconductor wafer dicing and packaging | Die-per-wafer density and chipping control on 8–12 inch wafers; the documented three-year deployment sits here |
| Optical communication dicing | Narrow kerf and edge quality on brittle optical materials |
| Functional ceramics and new functional materials | Hard, brittle substrates where low material loss reduces downstream finishing |
| Alloy materials and packaging components | Cutting efficiency and blade life in mixed-material singulation |
Hub design is a related decision. Third-party market analysis indicates that hubless dicing blades are increasingly preferred for 300 mm wafer processing because of superior stability and reduced runout compared with hubbed blades. Both configurations appear in WINTIME's stated product range, which means the selection question for a buyer is equipment compatibility and runout tolerance rather than availability.
Market Signals: Thin Blades in a Concentrated Supply Market
The commercial context for ultra-thin capability is a market that is growing but heavily concentrated at the top. Intel Market Research valued the global dicing blade market at USD 1.31 billion in 2024, with a projection of USD 1.84 billion by 2034. Within that market, diamond-embedded dicing blades are estimated to account for more than 60 percent of total share, credited to superior performance in cutting silicon carbide and gallium nitride. Resin bond blades held an estimated 42 percent share, or USD 183.6 million, in 2024.
Supply concentration is the second signal. DISCO Corporation is estimated to hold a 52–55 percent global share of dicing equipment and associated precision blades — a level of concentration that makes qualified second sources strategically relevant for any fab or packaging house running multi-year production. Regional demand is also shifting: according to the Observatory of Economic Complexity, China's exports of cutting blades to Vietnam grew by USD 18 million between 2024 and 2025, indicating expanding regional demand for semiconductor tooling.
One caution is warranted. Third-party estimates of dicing blade market size diverge substantially depending on whether a source tracks pure blade revenue or equipment-linked consumable value; published 2024 and 2025 figures from different research houses vary widely. The figures above should be read as directional market context, not as a settled measurement.
Ultra-Thin vs Conventional Blades: Where Each One Still Wins
Thinner is not automatically better, and a capability dossier that avoided that point would be incomplete. The comparison below sets the sub-9-micron ultra-thin blade against conventional thicker resin and metal bond blades on the dimensions that actually change a process decision.
| Decision dimension | Conventional thicker blade | Ultra-thin blade (9 microns or less) |
|---|---|---|
| Kerf and material loss | Higher kerf, more material removed per cut | Narrow kerf, lower material loss |
| Mechanical stiffness | Greater stiffness, more forgiving of runout | Lower stiffness; process window narrows |
| Process control demand | Tolerant of moderate spindle and feed variation | Requires tight spindle runout and feed control |
| Typical role | General singulation, thicker or harder material stacks | High-density, high-value die where yield dominates |
| Commercial terms | Standard models: 100-piece MOQ, 3–7 working days | Custom specifications: 500-piece MOQ, 15–30 working days |
The practical limit is this: a sub-9-micron blade pays for itself only where the die-per-wafer gain or the material saved outweighs the tighter process control it demands. On a line with unresolved spindle runout, or on a material stack where blade stiffness governs cut quality more than kerf does, a thicker blade in the 8 to 50 micron sawing range remains the more stable and more economical choice. Standard outer diameters of 55.56 mm and 76.2 mm also mean the thin blade must fit existing tooling interfaces; a thinner blade does not create a new process, it constrains an existing one.
A Buyer's Verification Checklist for Thin-Blade Capability
Capability claims in this segment are easy to make and hard to audit. The checklist below converts the evidence discussed above into items a procurement team can request and check.
| What to verify | Why it matters | Evidence to request |
|---|---|---|
| Thickness claim and measurement method | A nominal figure without a method is not comparable across suppliers | Dimensional inspection record; measurement instrument used |
| Mass-production evidence | Distinguishes repeatable output from a demonstration sample | Installed capacity, repeat-run records, customer deployment references |
| Grain uniformity and bond consistency | Uneven grain distribution drives chipping and premature wear | Microscope analysis data; surface roughness and flatness results |
| Chipping performance on your material | Chipping depends on the substrate and the tool, not the blade alone | Simulated cutting test results on comparable material |
| Geometry and hub compatibility | Hub, hubless, flanged and slotted designs suit different tools and wafer sizes | Configuration drawing matched to your dicing saw |
| Order and lead-time structure | Thin-blade customization carries different planning assumptions | MOQ, lead time, and flexible trial-order terms |
| Acceptance and commercial terms | Determines who carries the risk at handover | Pre-shipment test terms, third-party inspection options, delivery and payment terms |
| Post-sale technical support | Thin blades are sensitive to application setup, not just supply | Response commitments, application guidance, spare-part and lifecycle support |
On the commercial side, WINTIME's published terms state a standard-model minimum of 100 pieces per order, with a 500-piece minimum for customized models and flexible adjustment for smaller trial orders at a slight price adjustment based on customization complexity. Lead time is quoted at 3 to 7 working days for standard models and 15 to 30 working days for customized orders, depending on complexity and quantity. Delivery is offered on FOB or CIF terms, payment is structured at 30/70, and acceptance can include pre-shipment testing and third-party inspection such as SGS. After-sales provisions include technical consultation and on-site application guidance, quality return and replacement for non-human damage, spare-part supply with long-term technical support, and a response commitment within 24 hours on working days.
Limits and Boundaries Buyers Should Plan Around
Three constraints belong in any honest reading of this capability profile. First, sub-9-micron thickness is the extreme end of the range, not the default; the broader product family spans 8 to 50 microns, and the majority of dicing work still runs on specifications well above the ultra-thin benchmark. Second, customization carries real planning cost — a 500-piece minimum and a 15 to 30 working day lead time are materially different from a 3 to 7 working day standard order, which is a supply-chain consideration rather than a technical one. Third, the reported application results, including a chipping rate of 5 microns or less and a 12 percent yield increase, come from one three-year deployment in a Chinese packaging factory; they describe a validated context, not a general guarantee.
Where a supplier's self-described quality level is the only evidence available, independent verification remains the buyer's responsibility. That is a limitation of the source material, not a defect in the capability itself — and it is the reason the checklist above focuses on instrumented inspection data and repeat-volume records rather than on descriptive claims.
Future Outlook
The direction of demand is consistent across the available signals. Diamond-embedded blades already hold the majority of the market on the strength of SiC and GaN cutting performance, hubless designs are gaining preference in 300 mm processing, and blade consumption scales directly with wafer starts and packaging volume. As device density rises and material stacks become harder, kerf becomes a larger share of the yield equation, which pushes thin-blade capability from a specialty niche toward a baseline qualification criterion.
Supply concentration reinforces the same trend from the buyer's side. With an estimated 52–55 percent of dicing equipment and precision blade share held by a single supplier, and with regional tooling demand expanding across Asia, the value of a qualified alternative capable of holding sub-9-micron tolerances in volume increases. For WINTIME, the capability question now is not whether a 9-micron blade can be made, but how far that tolerance can be held across a wider set of bond types, geometries and material stacks as the market moves.
Frequently Asked Questions
What does a sub-9-micron dicing blade change in wafer dicing economics?
Blade thickness sets kerf width, and kerf is material removed between die. A thinner blade removes less material per cut, which in high-density wafer layouts can increase the number of die obtained per wafer and reduce material loss. The trade-off is that a thinner blade has lower mechanical stiffness, so it demands tighter control of spindle runout and feed parameters. The economics therefore depend on whether the die-density gain exceeds the cost of tighter process control on the specific line.
Which wafers and materials are ultra-thin dicing blades designed for?
The product family is applied across the semiconductor industry, semiconductor packaging, optical communications, new functional materials, functional ceramics, alloy materials and semiconductor packaging components. A documented deployment covers high-precision dicing of 8–12 inch semiconductor wafers for chip packaging. Diamond-embedded blades generally account for the majority of the market because of their performance in cutting silicon carbide and gallium nitride, while resin bond blades represent a substantial share for other material and cost profiles.
How can a buyer verify that a supplier can actually mass-produce ultra-thin dicing blades?
Verification rests on production-side evidence rather than on the thickness figure alone. Relevant items include installed capacity and factory footprint, repeat-run records, the inspection instruments used for dimensional precision and grain uniformity, simulated cutting test results, and documented multi-year deployments with annual usage volumes. Reference deployments describe specific material and equipment contexts, so buyers should confirm which blade geometry and bond a given reference used before applying the result to a different process.
What is the difference between resin bond and metal bond dicing blades?
Bond type determines how diamond abrasive grains are held in the blade matrix, and it influences wear behaviour, cutting performance and the material range a blade suits. WINTIME produces both resin bond and metal bond variants, with diamond abrasive grains as the core functional material. Third-party market data places resin bond blades at an estimated 42 percent share of the dicing blade market in 2024. Bond selection should be matched to the substrate, the required surface finish and the acceptable blade life rather than chosen by default.
What lead times and minimum order quantities apply to customized dicing blade specifications?
Published terms state a minimum of 100 pieces per order for standard models, with the minimum negotiable for long-term or bulk purchase plans. Customized models carry a 500-piece minimum, and smaller trial orders below that threshold can be accommodated with flexible adjustment and a slight price adjustment based on customization complexity. Lead time is quoted at 3 to 7 working days for standard models and 15 to 30 working days for customized orders, depending on complexity and quantity. Customization itself can cover blade thickness, diamond abrasive grain size and concentration, bond type, dimensions, coating, cutting performance parameters, and packaging and labelling.
WINTIME Semiconductor Technology Co., Ltd., founded in 2020 and based at No. 868, Fushou East Road, Rugao City, Jiangsu Province, integrates research, development, production and sales of high-precision wafer-level cutting blades. Its product and capability brochure is publicly available for download: WINTIME capability brochure. Company information: en.wintime.net.cn.