
Thermoforming Plastic Sheet Roll Compliance: Three Paths
Compliance for a thermoforming plastic sheet roll is not one status that a material either holds or lacks. It is a set of qualification points that changes with the packaging application. A roll that performs well in a retail blister is not thereby qualified for a pharmaceutical tray, and a food-contact statement does not transfer to a medical device package. For buyers moving from decision to execution — releasing a purchase order, agreeing acceptance criteria and locking a supply relationship — the operative question is narrower: which qualification points apply to this package, and which of them must be carried forward into every batch?
This reference maps three qualification profiles — medical and pharmaceutical, food, and toy and retail — then separates what differs by application from what does not: consistent thickness, stable thermoforming performance, clean surface and dimensional stability.
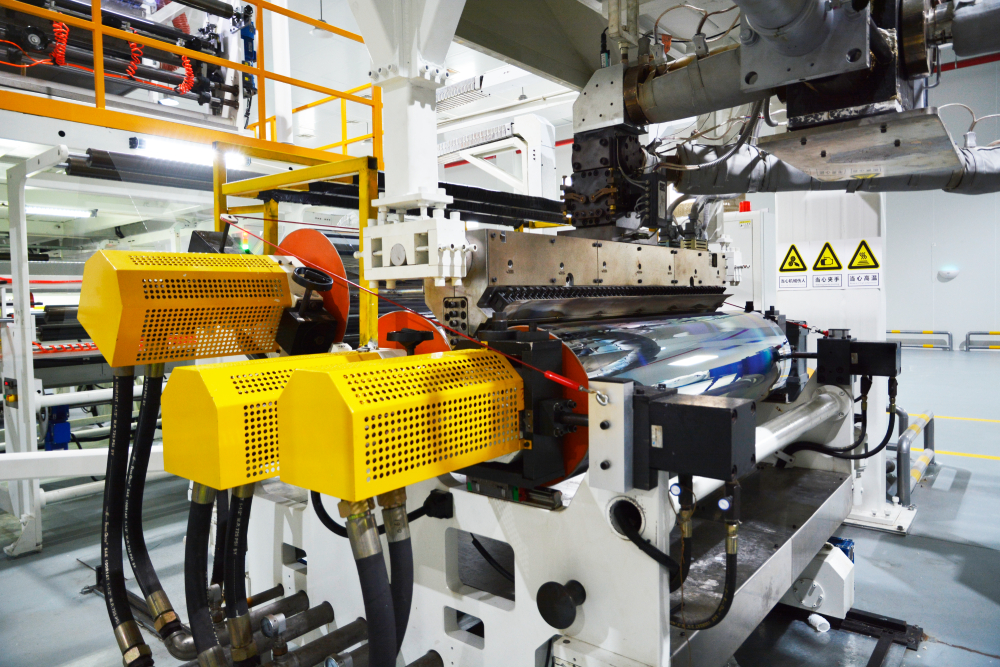
Sheet roll production environment. Compliance is verified per batch, not per material family.
Why compliance splits by application
Three packaging families are often discussed as though they shared a single compliance ladder. They do not. Each is qualified through a different dominant logic, and that logic determines which evidence a buyer should hold before ordering.
- Medical and pharmaceutical packaging is documentation-led. Material compliance is the starting point; additional performance requirements — cleanliness, dimensional stability, forming precision — are layered on top, and the file has to support the specific package rather than the polymer family.
- Food packaging is condition-led. Food-contact compliance applies where it is required, but the deciding factors are the conditions the pack must survive: low-temperature performance, moisture resistance and anti-fog behaviour in clear packs.
- Toy and retail packaging is appearance-led. Transparency, forming definition, impact resistance and consistent appearance carry more weight than a food-contact declaration, because the pack is judged on shelf.
The practical consequence is that a buyer who specifies one sheet for three packaging lines will usually over-specify one of them and under-qualify another. Over-specification adds cost without adding protection. Under-qualification appears later, as forming rejects, failed incoming inspection, or a documentation gap during a customer audit.
The three qualification profiles at a glance
| Application family | Dominant qualification logic | Properties that carry the decision | Confirm before ordering |
|---|---|---|---|
| Medical and pharmaceutical | Documentation plus performance | Consistent thickness, forming stability, dimensional stability, surface cleanliness, suitable mechanical performance | Package type, contact conditions, forming method, dimensions, cleanliness and applicable compliance requirements |
| Food packaging | Condition-led, with food-contact compliance where required | Low-temperature behaviour, rigidity and impact resistance, moisture resistance, anti-fog where condensation occurs, sealing compatibility | Food type, tray dimensions, forming depth, storage temperature, transparency, sealing method, destination-market food-contact requirements |
| Toy and retail packaging | Appearance-led | Transparency, forming definition, impact resistance, colour and appearance consistency | Required clarity, forming depth, impact expectation, colour target, appearance acceptance criteria |
Qualification logic differs by application family, not by material name.
Medical and pharmaceutical packaging: documentation plus performance
This is the profile where a material name proves least. “Medical grade” is not a designation a supplier can apply generally; a material should not be described that way unless the specific material and its documentation support the designation. Qualification therefore starts from the package, not from the polymer.
What the buyer defines first
- The package type — a protective tray, a device package and a pharmaceutical blister are three different problems.
- Product contact conditions and the forming method.
- Dimensions and cleanliness requirements.
- The compliance requirements attached to the destination market and to the customer's own audit standard.
What the sheet has to deliver
For thermoformed medical trays, the properties that recur in qualification are consistent thickness, forming stability, dimensional stability, surface cleanliness and suitable mechanical performance. None of these is captured by a general material description. A tray that forms with uneven wall distribution does not become acceptable because the resin grade is correct, and a surface that is clean at the extruder but damaged in handling is not clean at the press.
Where the boundary sits
Food-contact compliance cannot replace medical packaging requirements. The two address different applications and are not interchangeable, so a supplier's food-grade documentation should not be accepted as an answer to a medical packaging question. PET can be used in certain medical and healthcare packaging applications, but suitability depends on the specific package design and the regulatory requirements attached to it. That is why the file, rather than the material name, is the qualification.
Food packaging: compliance follows the conditions
Food packaging splits the compliance question in two, and buyers who answer only the first half tend to discover the second half during production.
Food-contact compliance is verified, not assumed
A sheet described as food packaging sheet is not automatically compliant with any particular food-contact framework. Compliance should be verified against the specific material, the test report, the application and the destination market. For packaging destined for the European Union, Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food. And “food grade” on its own does not define a usable thermoforming specification: the buyer still has to state the food type, tray dimensions, forming depth, storage temperature, transparency requirement, sealing method and the food-contact requirements that apply.
A refrigerated meat tray is not a bakery tray
A refrigerated meat tray, a fruit tray and an ambient bakery tray can require different material and performance characteristics even though all three are food packaging. Refrigerated and frozen distribution adds demands that room-temperature forming trials do not reveal: low-temperature behaviour, tray rigidity, impact resistance, condensation control and sealing compatibility. Material and thickness should be selected from the finished tray and the storage environment, not copied from a specification developed for ambient packaging.
Moisture and anti-fog
Condensation and humidity are part of the service condition in chilled and frozen distribution. They affect appearance and can affect how a pack performs in handling, so the specification should be set from the storage and distribution environment rather than from a room-temperature reference. Anti-fog is the specific function for the case where condensation forms inside clear packaging and product visibility has to be maintained, such as some refrigerated fresh-food applications. It is not a default requirement. Specifying anti-fog where condensation does not occur adds cost without a corresponding benefit.
Sealing changes the structure
Where heat sealing is part of the pack, mono PET and PET/PE laminated sheet are different answers rather than grades of the same answer. Mono PET keeps a simpler single-material structure, while a PET/PE laminated sheet combines PET rigidity with a PE sealing layer for applications that require heat sealing, such as meat and fresh food trays. The laminated route also means controlling two behaviours — thermoforming and sealing compatibility — and its cost depends on layer structure, thickness and sealing requirements rather than on a fixed premium.
For frozen food trays, food-grade PP sheet rolls are available with impact-resistant copolymer options, which addresses the low-temperature impact requirement that drives a large share of frozen-tray failures.
Toy and retail packaging: appearance is the acceptance criterion
Retail and toy packaging is qualified on what the buyer and the shopper can see. The recurring points are transparency, forming definition, impact resistance and consistent appearance — and each of them is a specification item, not an aesthetic preference.
Clear sheet should not be selected by transparency alone. Required clarity has to be considered together with stiffness, forming depth, impact performance, temperature conditions, sealing or printing requirements and the finished package design. PET is widely used for high-clarity thermoformed packaging, including blisters and transparent folding boxes, but the exact PET structure and thickness should follow the forming depth and the performance the pack needs.
Where the pack is opaque or coloured, HIPS offers better impact resistance and toughness than GPPS, which is generally more rigid and transparent but more brittle. For coloured retail parts, colour customization is available for many sheet products, subject to material, colour target, quantity and production requirements. In retail work, appearance consistency across batches belongs in the acceptance criteria: a colour that matches on the first delivery and drifts on the fourth is a compliance failure, not a cosmetic one.
Impact and clarity pull in different directions. High-impact requirements push toward HIPS or impact-modified structures; high-clarity requirements push toward PET. Where both matter, the trade-off has to be resolved against forming depth and the handling the pack will actually see, rather than by choosing the material with the better reputation.
Clean, dry and consistent: the checks that do not change
Four checks survive the switch between medical, food and retail. They are also the four a supplier has to be able to demonstrate repeatedly, which makes them the natural content of a long-term supply agreement.
Consistent thickness
Thickness variation affects heating, forming consistency, part weight and final wall distribution. For deep parts, nominal thickness alone is not enough: the real concern is how material distributes from the flange and sidewalls to the deepest area during forming, which depends on formability, initial thickness, draw ratio, mould geometry, corner radius and heating uniformity. A sheet that forms well in a shallow tray may not suit a much deeper part.
Stable thermoforming performance
A sheet that forms acceptably in a trial but drifts between batches produces rejects that no incoming dimensional check will catch. Thermoforming performance therefore belongs in batch-level verification, not only in first-article approval. PET thermoforming typically occurs between 130 °C and 160 °C (266 °F to 320 °F); within that window, heating uniformity, forming time, vacuum or pressure and mould geometry determine the outcome, and increasing temperature is not always the correct response when a part does not form completely.
Clean surface
Surface cleanliness matters most in medical and food applications and shows up as appearance in retail. It is also the property most easily lost after the material leaves the extruder. Raw material inspection and in-process control protect the sheet; packaging, storage and handling protect it afterwards. Buyers should treat these as two separate controls, because a clean sheet stored badly arrives contaminated.
Dimensional stability
Flatness, roll form and freedom from deformation decide whether a roll feeds properly. Curl can originate in material structure, residual stress, winding, storage conditions, temperature change, moisture or handling, and the cause should be separated between material, storage and machine before any material change is made. Storage temperature, humidity, direct sunlight, packaging condition and storage time can all influence sheet condition before processing. PET also requires appropriate drying and temperature management depending on sheet type and process.
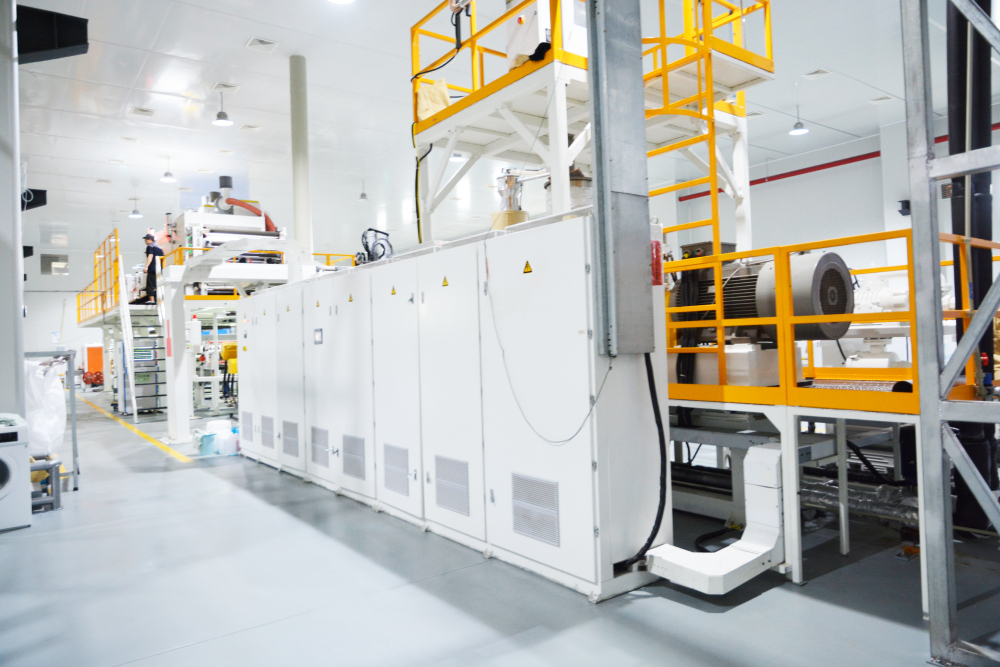
Handling and storage sit between sheet production and forming. Feeding problems are often traceable to this interval rather than to the material grade.
What a long-term supply relationship has to keep repeating
PULIXIN Thermoforming Plastic Sheet is manufactured by Pulixin Packaging Materials (Shanghai) Co., Ltd., a rigid plastic sheet roll manufacturer established in 2009 with more than 15 years of experience in the category. The company operates a 20,000 m² production base with 14 advanced co-extrusion lines and annual output exceeding 40,000 tons, and exports to more than 55 countries, with Southeast Asia, the Middle East, South America and Europe among its main markets. Its R&D team consists of 3 engineers.
The range covers PET, PP and HIPS thermoforming sheet rolls, including food-grade PET and PP sheet rolls and performance-oriented grades — anti-fog, anti-static, high-stiffness and high-formability sheet rolls — together with customized thickness, width, colour matching, surface finish and multilayer co-extrusion structures under OEM production. For a buyer running more than one packaging line, that breadth is the practical reason a single supplier can hold several qualification profiles at once: the profiles remain separated at specification level, without switching manufacturers.
Quality management is where the compliance argument becomes operational. Raw materials are inspected before production, and every batch undergoes quality control covering thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance. These are the same variables that appear in incoming inspection and in a customer audit, which is what allows a specification to be carried forward across deliveries rather than renegotiated at every order.
The limit belongs in the same paragraph as the capability. A supplier can document a material and a batch; it cannot convert one application's compliance file into another's. A food-contact statement does not satisfy a medical requirement, and a retail appearance approval says nothing about low-temperature impact. Buyers should confirm the documentation set that matches their package rather than assume a general grade statement covers every application in the plant.
Turning application requirements into a specification
The table below translates the three profiles into specification decisions. It is deliberately written as a verification sequence, because most qualification failures come from a property that was assumed rather than checked.
| Requirement | What it drives in the sheet | How to verify before volume |
|---|---|---|
| Forming depth and geometry | Material formability, initial thickness, draw ratio | Forming trial with wall and bottom thickness measurement |
| Refrigerated or frozen distribution | Low-temperature impact resistance and rigidity | Evaluation under the actual storage conditions, not room temperature only |
| Condensation in clear packs | Anti-fog function | Specified only where product visibility is an acceptance criterion |
| Heat sealing | Sealing-compatible structure, for example a PE sealing layer | Sealing trial on the actual line and film combination |
| Printing or decoration | Surface finish and treatment | Print trial on the selected surface finish |
| Weight-sensitive packaging | Material density: PP approximately 0.90 to 0.91 g/cm³, PET approximately 1.33 to 1.40 g/cm³ | Confirmed against grade and formulation, since actual values vary |
| Cleanliness | Surface condition and handling controls | Incoming inspection plus packaging and storage review |
| Batch consistency | Thickness tolerance and width accuracy | Batch records and agreed acceptance criteria |
Application map: which qualification point dominates
| Application | Dominant qualification point | Sheet consideration |
|---|---|---|
| Pharmaceutical tray | Documentation plus dimensional and cleanliness performance | PET where the package design and regulatory requirements support it; thickness consistency and forming stability |
| Medical device tray | Same, with forming precision for complex cavities | Stable wall distribution at depth; clean surface through handling |
| Fresh meat tray | Food contact where required, plus low-temperature impact and sealing | PET/PE laminated structure where heat sealing is required |
| Fruit and bakery tray | Food contact where required, plus appearance and visibility in chilled display | PET for clarity; anti-fog only where condensation actually occurs |
| Dairy cup and lid | Food contact, stiffness, rim forming and stacking | PP and PS are established cup materials; rim geometry drives material distribution |
| Frozen food tray | Low-temperature impact resistance | Food-grade PP with impact-resistant copolymer options |
| Toy blister and transparent folding box | Transparency, forming definition and impact | PET for clarity; HIPS for opaque or impact-critical parts |
| Electronics tray | Physical protection, with anti-static only where the ESD control system requires it | HIPS for forming behaviour and impact; anti-static grade where the electrical specification is confirmed |
| Cosmetic pack | Appearance, colour consistency and print | Colour matching and surface finish; PET where clarity is the priority |
Market context: application-specific demand and recycled content
Demand-side data supports the application-specific view. Grand View Research valued the global thermoformed plastic market at USD 14.79 billion in 2023 and projected a compound annual growth rate of 4.9% for 2024 to 2030. Recycled content is expanding against that base: Dataintelo projects the recycled PET market value to reach USD 24.6 billion by 2034.
Two caveats matter when these figures are used in a business case. First, published estimates are not always measuring the same thing — some researchers value thermoformed plastic materials as raw sheet, others value finished thermoformed products, which is why headline figures from different publishers do not align. Second, the regulatory layer moves with the material layer: Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food in the European Union, and cross-border movement depends on consistent customs classification, with thermoforming plastic materials falling under HS Code Heading 3920 for non-cellular and 3921 for cellular products.
The procurement implication is that compliance files and material files are converging. A supply relationship that covers only price, thickness and delivery will increasingly fall short of what a customer's own audit requires, particularly where recycled content has to be documented order by order.
Where the application-specific model has limits
Treating compliance as three profiles is more accurate than treating it as one status, but it is not a complete solution, and the trade-offs are real. The comparison below covers the structural choices buyers most often face when they move from one application family to another.
| Structure choice | What changes | What the buyer should control |
|---|---|---|
| Mono PET vs PET/PE laminated sheet | Mono PET is a simpler single-material structure; PET/PE adds a PE sealing layer for heat-sealing applications | Whether heat sealing is required at all; sealing conditions; both forming behaviour and sealing compatibility |
| APET vs PETG | APET balances transparency, stiffness and cost for high-volume packaging; PETG is often selected where easier forming or more demanding geometry is required | Forming depth and geometry; whether a more forgiving forming window justifies the difference |
| HIPS vs GPPS | HIPS offers better impact resistance and toughness; GPPS is generally more rigid and transparent but more brittle | Whether impact or clarity dominates; forming temperature and mould settings for the specific grade |
| rPET vs virgin PET | rPET incorporates recycled PET content; the percentage is customized according to specification and compliance requirements | Confirmed recycled-content ratio; documentation; possible adjustment of processing conditions |
| PET vs PVC | PET offers high transparency, good thermoforming performance and a PVC-free material option | Whether a chlorine-free structure is a requirement; transparency and stiffness targets |
First, the three profiles cannot be collapsed into one specification. A structure tuned for maximum clarity is not the structure tuned for low-temperature impact, and a document set prepared for food contact does not satisfy a medical requirement. Buyers running several lines should expect to hold several specifications.
Second, “medical grade” is not a general label. Without material-specific documentation the description should not be used at all, which means a buyer cannot treat the phrase in a quotation as evidence of anything.
Third, functional grades are function-specific. Anti-fog is relevant only where condensation interferes with visibility, and anti-static or ESD sheet is required only when component sensitivity and the customer's electrostatic-control system call for controlled surface-resistance properties. Not every electronics tray needs it, and specifying it by default adds cost without changing the protection the pack provides.
Fourth, recycled content is not a free substitution. Recycled content can be customized according to product specification and compliance requirements, and the actual percentage must be confirmed for each product or order. rPET is not necessarily cheaper than virgin PET: cost depends on recycled-content ratio, material quality, certification requirements and market conditions, and processing conditions may require adjustment according to recycled content, IV, sheet structure and thermoforming requirements.
Fifth, material substitution is rarely a drop-in change. Different materials have different shrinkage, heating and forming behaviour, so machine settings and sometimes tooling need adjustment. Finally, not every forming fault is a sheet fault: cracking, whitening and poor forming can result from unsuitable heating, uneven sheet temperature, excessive forming depth, sharp mould geometry or material condition. The sheet, mould, heating profile and forming parameters should be checked together before the material is changed.
Outlook
Three developments are likely to shape how buyers qualify thermoforming plastic sheet rolls over the next several years.
- Compliance files become part of the contract. As audits tighten, the documentation set — not only the material — becomes a deliverable that has to be renewed rather than filed once.
- Recycled content raises the verification burden. Growth in rPET demand increases the number of orders where recycled-content percentage, quality and certification requirements must be confirmed individually.
- Application-specific qualification persists. Food, medical and retail requirements are unlikely to converge, because they are driven by different risks: ingestion, patient contact and shelf appearance respectively.
The practical response for a buyer entering execution is to build one qualification file per packaging application rather than one per material, keep a proven specification as the baseline when trialling a change, and change one variable at a time so that the source of any difference remains identifiable.
FAQ
Can one thermoforming plastic sheet roll specification be qualified for medical, food and retail packaging at the same time?
No, not as a single qualification. Medical packaging requires material compliance plus additional performance and documentation requirements; food packaging depends on food-contact requirements where applicable and on the distribution conditions the pack must survive; retail packaging is judged on transparency, forming definition, impact resistance and appearance consistency. A sheet may be technically capable in more than one application, but the evidence differs, so buyers should hold a separate qualification file for each application.
What should a buyer confirm before ordering sheet for pharmaceutical or medical device trays?
The package type (protective tray, device packaging or pharmaceutical blister), product contact conditions, forming method, dimensions, cleanliness requirements and the applicable compliance requirements. “Medical grade” should not be claimed unless the specific material and documentation support it, and food-contact compliance cannot replace medical packaging requirements. The sheet properties commonly important for thermoformed medical trays are consistent thickness, forming stability, dimensional stability, surface cleanliness and suitable mechanical performance.
Which checks define food-contact qualification for thermoforming sheet?
Food-contact compliance must be verified against the specific material, test report, application and destination market; food packaging sheet is not automatically compliant with a given framework. In the European Union, Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food. “Food grade” alone does not define a usable thermoforming specification, because food type, forming depth, storage temperature and sealing method still have to be stated.
When does a food packaging application need low-temperature performance or anti-fog rather than higher clarity?
Refrigerated and frozen applications need low-temperature behaviour, tray rigidity, impact resistance, condensation control and sealing compatibility, because room-temperature forming trials do not reveal those requirements. Anti-fog is relevant when condensation forms inside clear packaging and product visibility must be maintained, as in some refrigerated fresh-food applications. It is not required where condensation does not occur, and adding it there adds cost without benefit.
Which sheet properties determine appearance and impact performance in toy and retail packaging?
Transparency, forming definition, impact resistance and consistent appearance. PET is widely used where high clarity is the priority; HIPS offers better impact resistance and toughness than GPPS, while GPPS is generally more rigid and transparent but more brittle. Colour customization is available for many sheet products subject to material, colour target, quantity and production requirements, and appearance consistency across batches should be written into the acceptance criteria.
How should a buyer verify batch-to-batch consistency during a long-term supply agreement?
By agreeing on the variables that are checked per batch rather than once: thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance. Acceptance criteria typically cover specification verification, thickness and width inspection, appearance inspection and finished-product quality inspection before shipment, with third-party inspection available on request. For a new or difficult project, a drawing or finished sample helps the manufacturer understand forming depth, geometry and performance requirements.
What processing conditions should be confirmed before a sheet is released to production?
The workshop should be clean and dry, and the sheet should be stable before forming. PET thermoforming typically occurs between 130 °C and 160 °C (266 °F to 320 °F), and PET requires appropriate drying and temperature management depending on sheet type and process. Roll storage conditions — temperature, humidity, direct sunlight, packaging condition and storage time — influence sheet condition before processing, and curl should be traced to material, storage or machine factors before the material is changed.
How does a switch to recycled content change qualification?
Recycled content can be customized according to product specification and compliance requirements, and the actual percentage must be confirmed for each product or order. rPET is not necessarily cheaper than virgin PET, because cost depends on recycled-content ratio, material quality, certification requirements and market conditions. Processing conditions may require adjustment according to recycled content, IV, sheet structure and thermoforming requirements, so performance should be verified for the specific application rather than inferred from the recycled-content figure.
A current overview of the PULIXIN sheet range, structures and customization options is available in the downloadable PULIXIN product catalogue (PDF).
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.