
Thermoforming Sheet Rolls: Width, Core & Print-to-Convert
Thermoforming Sheet Rolls: Width, Core & Print-to-Convert
A thermoforming plastic sheet roll is a process input, not a finished product. Its width, diameter and core inner diameter determine whether the material can be unwound, printed, cut, laminated or otherwise converted without generating avoidable edge trim, tension variation or handling losses. For buyers moving from decision to execution, the useful question is narrower than “which sheet is cheapest per kilogram” — it is “which roll configuration fits the converting and forming line already installed.”
Pulixin Packaging Materials (Shanghai) Co., Ltd. is a Shanghai-based manufacturer of rigid plastic sheet rolls — PET, PP and HIPS/PS — used in thermoforming and converting, founded in 2009 and exporting to more than 55 countries. This reference guide draws on published roll-parameter guidance and publicly documented material comparison data to explain how roll specifications interact with a print-then-convert workflow, and what buyers should confirm before placing a repeat order.
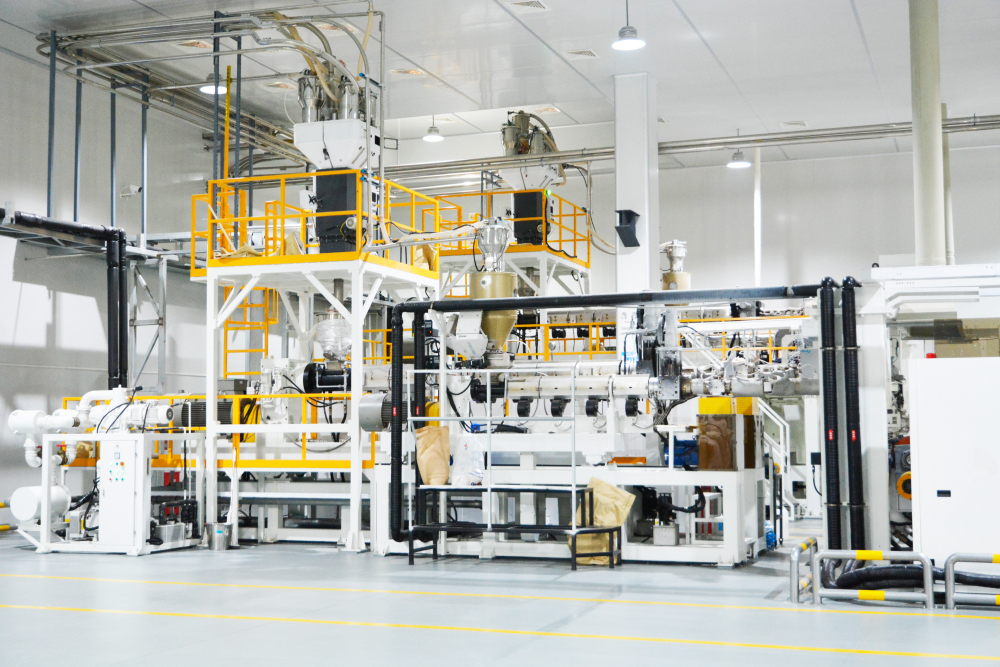
Roll Geometry Is a Converting Parameter, Not a Warehouse Detail
Most sourcing documents treat roll dimensions as logistics data. In practice, they are process data. Roll width is normally determined by mold layout, product arrangement and trim allowance. Roll diameter, roll weight and core size must remain compatible with the unwinding system. When those three variables are correctly matched to the machine, the result is less unnecessary trim waste and fewer handling or feeding problems. When they are not, the consequences appear downstream — as web wander, uneven tension, splice interruptions, or a roll that cannot be lifted safely onto the mandrel.
The problem compounds because roll parameters are usually specified once and then inherited. A width chosen for a previous product family, a core size copied from a legacy machine, or a maximum roll weight set by an old lifting frame may survive several supplier changes even though the converting line has changed. For buyers at the execution stage, the practical opportunity is to treat roll geometry as a reviewed specification, not a fixed constant.
Working Principle
Roll dimensions should match the customer’s thermoforming and feeding equipment. Correct roll specifications reduce unnecessary trim waste and prevent handling or feeding problems. They do not compensate for an unsuitable material grade or an unsuitable thickness.
The Three Roll Parameters That Govern Printing and Converting
Three specifications do most of the work in a roll-fed workflow: width, diameter-and-weight, and core inner diameter. Each one answers a different question, and each one has a different owner on the buyer’s side — often the tooling engineer, the production planner and the maintenance team respectively.
| Roll Parameter | What It Governs Downstream | How It Is Normally Defined | What the Buyer Must Confirm |
|---|---|---|---|
| Roll width | Number of product lanes across the web, volume of edge trim, print and laminate layout width | Mold layout, product arrangement and required trim allowance | Usable width of the forming or printing machine; layout width plus necessary trim |
| Roll diameter & weight | Unwinding tension stability, changeover or splice frequency, lifting and handling method | Winding limits on the supplier side and handling limits on the buyer side | Maximum roll weight and maximum roll diameter accepted by the unwinding system |
| Core inner diameter | Shaft or chuck fit, concentricity, runout and sideways web movement during unwinding | The unwinding method and the mandrel size actually installed | Core inner diameter, core material and the specific unwinding method in use |
A fourth parameter interacts with all three: thickness tolerance. Thickness variation affects heating, forming consistency, part weight and final wall distribution. In a print-then-convert line, the same variation changes the amount of material consumed per printed unit, which is why width accuracy and thickness tolerance are normally inspected together rather than separately.
How a Sheet Roll Moves Through a Print-to-Convert Workflow
The phrase “print-to-convert” describes a sequence rather than a single machine. Material is unwound from a roll, printed, and then either converted in-line or cut to sheet for later processing. Two operating modes dominate, and the choice between them is normally made before the sheet specification is frozen, because it changes the required roll width, the acceptable diameter and the core size.
Mode 1 — Roll in, converted product out
The web is unwound, printed, and then cut, laminated or otherwise converted in a continuous or semi-continuous sequence before being stacked or rewound. In this mode, roll width must be wide enough to carry the full print layout plus any grip or margin the press requires, and narrow enough that the resulting trim is economically acceptable. Roll diameter drives changeover frequency: a larger roll means fewer interruptions, but also greater demand on tension control and on lifting equipment. Core fit is critical because any runout at the mandrel translates into register variation across the entire web.
Mode 2 — Roll in, sheets out
The web is unwound and printed, then cut to sheet before forming or finishing. Here the roll width defines the sheet width, and the trim allowance is calculated against the finished sheet dimension rather than the converting layout. This mode is common where forming and printing are carried out on separate sites or on separate shifts, and where sheet flatness after cutting matters to the downstream thermoforming step.
In both modes, the operating logic is the same: the roll is the beginning of a tension chain. Width, diameter and core geometry determine how stable that chain is, and how much of the purchased material actually reaches the finished package.
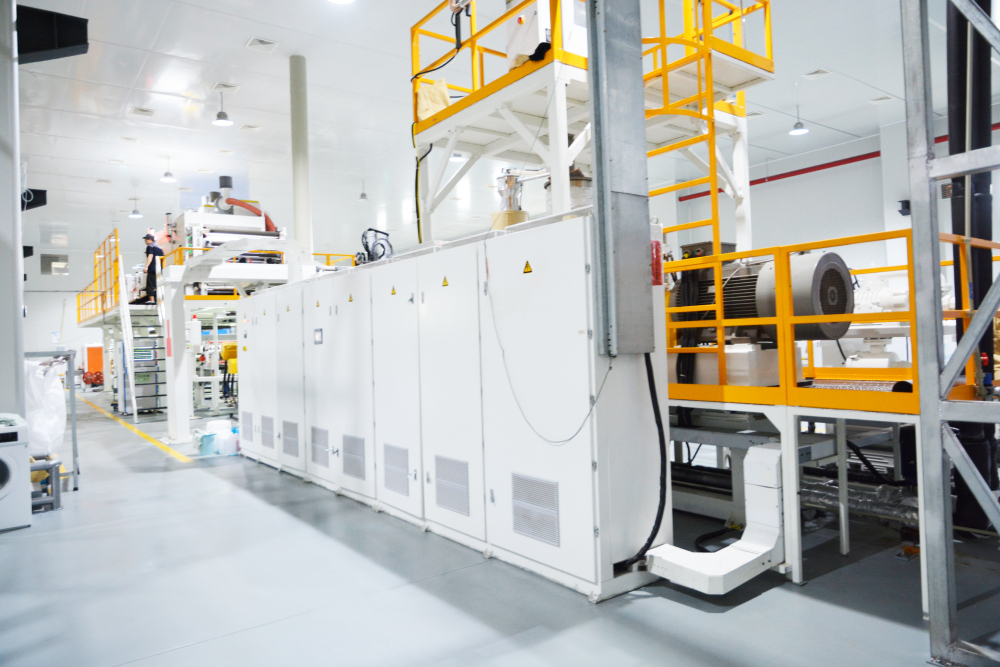
Clean, Dry Indoor Processing: Why the Environment Is Part of the Specification
Sheet and roll printing followed by cutting, laminating or converting assume a clean and dry indoor processing environment. That requirement is not a formality. Surface contamination and ambient variation act directly on the web between unwinding and the first converting station.
- Dust and airborne particles settle on the web surface and interfere with adhesion at printing, coating and laminating stages.
- Humidity and temperature swings change sheet condition between storage and processing, which can affect flatness and feeding behaviour.
- Storage conditions — temperature, humidity, direct sunlight, packaging condition and storage time — influence sheet condition before it ever reaches the machine.
- Handling and storage method should follow the supplier’s packaging and handling recommendations to avoid roll deformation or edge damage.
There is an important boundary here. Environment control reduces avoidable defects; it does not correct an unsuitable specification. Sheet curl, for example, can be related to material structure, residual stress, winding, storage conditions, temperature changes, moisture or handling conditions. The cause should be separated between material, storage and machine factors before production settings are adjusted. If curl appears, the first action is diagnosis — flatness, roll alignment, tension, feeding equipment, and whether the roll was deformed during transport or storage — not an immediate material change.
How to Specify Roll Parameters to a Supplier
The specification conversation differs depending on whether the line already exists or the mold is new. Both cases converge on the same principle: start from the equipment and the finished part, and work backwards to the roll.
For an existing production line
Provide the currently proven roll specification, or the equipment limits directly: usable machine width, maximum roll weight, maximum roll diameter, core inner diameter and unwinding method. Because the existing specification is already validated on the line, it becomes the comparison baseline. This is the fastest route to a like-for-like quotation and the lowest-risk route to a first order.
For a new mold or a new product
Calculate sheet width from the mold layout plus the necessary trim allowance, then confirm roll diameter, roll weight and core size against the unwinding equipment before production begins. Provide the finished-part drawing or a sample, the forming depth, the machine information, and any special performance requirements. A drawing or finished sample is especially useful because it lets the manufacturer reason about forming depth and geometry rather than guessing from a target thickness.
What a complete quotation request contains
A useful quotation request goes beyond a material name and a price. It should include material, thickness, width, colour, transparency, roll dimensions or core requirements, estimated quantity, application and delivery destination. For a new thermoforming project, finished-part dimensions, forming depth, machine information and special performance requirements help the manufacturer recommend a more suitable specification and reduce repeated sampling.
Two specification habits create avoidable cost. The first is requesting “food-grade sheet” without defining the application — food grade alone does not define a usable thermoforming specification, because a refrigerated meat tray, a fruit tray and an ambient bakery tray can require different material and performance characteristics. The second is requesting a thickness without product and machine information, which can lead either to unnecessary material use or to poor forming performance.
Manufacturing context matters when evaluating the response. Pulixin Packaging Materials (Shanghai) Co., Ltd. operates a 20,000㎡ production base with 14 advanced co-extrusion production lines and an annual output exceeding 40,000 tons, and offers thickness customization, width customization, colour matching, surface finish options, multilayer co-extrusion structures, food-grade material solutions and OEM production. Every batch undergoes quality control covering thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance.
Where Roll Parameters Matter Most, by Application
Application dictates which of the three roll parameters deserves the most attention, because different packaging formats consume the web differently.
| Application | Material Commonly Considered | Dominant Roll Consideration |
|---|---|---|
| Clear food trays, clamshells, display packaging | PET | Width matched to tray lanes; clarity and stiffness confirmed together |
| Cups, lids, dairy containers | PP, PS | Width and rim-geometry tolerance; stacking consistency |
| Blister packaging, folding boxes | PET for clear, HIPS for opaque or coloured | Web width versus print layout; edge trim volume |
| Electronics and component trays | HIPS, standard or anti-static depending on requirement | Width for multi-cavity layouts; thickness consistency |
| Refrigerated food and fresh meat trays | PET, PP; anti-fog only where condensation matters | Forming depth versus thickness; not every tray needs anti-fog |
One pattern is worth noting for planning purposes: in continuous roll-fed lines, width is normally set to the number of product lanes across the web. An application change therefore usually becomes a width change, and a width change is a roll specification change rather than a process adjustment.
Market Context: Why Roll Specification Is Getting More Attention
Roll specification discipline is being reinforced by two external trends: volume growth and compliance complexity. Grand View Research valued the global thermoformed plastic market at $14.79 billion in 2023, with a projected compound annual growth rate of 4.9% over 2024–2030. Published estimates differ depending on whether the measurement covers thermoformed plastic materials or finished thermoformed products, so figures should be read with the definition attached rather than compared directly.
On the sustainability side, the recycled PET market has been projected to reach $24.6 billion by 2034. For roll buyers, recycled content is a specification variable rather than a marketing label: recycled content can be customized according to product specification and compliance requirements, and the actual percentage must be confirmed for each product or order. It is also worth stating plainly that rPET is not necessarily cheaper than virgin PET — cost depends on recycled-content ratio, material quality, certification requirements and market conditions.
Regulatory context adds a documentation layer. EU Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food. For customs and classification purposes, thermoforming plastic materials fall under HS Code Headings 3920 (non-cellular) and 3921 (cellular). Processing parameters are material-specific: PET thermoforming typically occurs between 266°F and 320°F (130°C to 160°C).
Comparing Roll-Fed Supply with Cut-Sheet Supply
Roll-fed and pre-cut sheet supply are not superior and inferior versions of the same thing; they trade different costs against different constraints. The comparison below reflects general converting logic rather than a claim about any specific supplier.
| Dimension | Roll-Fed Supply | Pre-Cut Sheet Supply |
|---|---|---|
| Specification focus | Width, diameter, weight and core must all match the unwinding system | Sheet length, width and flatness matter more than core geometry |
| Trim control | Trim is generated at the width stage and can be minimised by matching width to layout | Trim is largely fixed by the sheet format selected |
| Handling | Requires mandrel, tension control and lifting capability within roll-weight limits | Requires pallet handling and flat storage to avoid distortion |
| Changeover | Changeover frequency is a function of roll diameter and weight | Changeover is per stack rather than per roll |
| Practical limitation | Core size and roll diameter are bounded by installed equipment; the supplier cannot resolve a machine mismatch | Format flexibility is bounded by the sheet sizes available and by storage flatness |
Material structure adds a second comparison layer, particularly where laminating is part of the converting sequence. Mono PET offers a simpler single-material structure, while PET/PE laminated sheet combines PET rigidity with a PE sealing layer for applications requiring heat sealing. There is no fixed universal performance percentage between the two — performance depends on PET thickness, PE layer thickness, total sheet structure, sealing conditions and end-use requirements. The practical trade-off is maintenance: PET/PE requires control of both thermoforming behaviour and sealing compatibility, whereas mono PET has a simpler material structure but may require a different sealing solution depending on package design.
Boundaries Worth Stating Up Front
Increasing thickness does not automatically increase strength — material type, geometry and forming distribution are equally important. Substituting one material for another generally requires machine-setting changes and sometimes tooling adjustment, because shrinkage, heating and forming behaviour differ. And no universal energy-saving percentage applies to any sheet structure; actual consumption depends on thickness, forming conditions, cycle time and equipment.
Future Outlook
Three developments are likely to keep roll specification on the buyer’s agenda. First, recycled-content requirements are turning material composition into a documented specification item rather than a preference, which means roll parameters and compliance documentation will increasingly be reviewed in the same conversation. Second, co-extruded and multilayer structures expand the functional options available in a single roll — transparency, colour and functional properties can be engineered into the structure — but they also increase the number of variables that must be recorded on a repeat order. Third, continued market growth keeps pressure on trim efficiency, which is governed mainly by how closely roll width matches the actual product layout.
A practical implication follows. Buyers who maintain a roll specification record — width, thickness and tolerance, diameter and weight limit, core inner diameter, unwinding method, material and structure, colour and transparency, compliance documentation — will absorb material and layout changes with far less disruption than buyers who re-derive these values each time.
Frequently Asked Questions
How should I specify roll width, roll diameter and core size when ordering thermoforming sheet?
Roll dimensions should match the customer’s thermoforming and feeding equipment. Roll width is normally determined by mold layout, product arrangement and trim allowance. Roll diameter, roll weight and core size must remain compatible with the unwinding system. Correct roll specifications can reduce unnecessary trim waste and prevent handling or feeding problems.
How do roll width and roll diameter affect a print-then-convert workflow?
In a roll-fed workflow, width determines how much of the web can carry product lanes or print layout and how much becomes edge trim, so a width change is a specification change rather than a process tweak. Roll diameter and weight determine how often the line is interrupted for a roll change and how much the unwinding system must control tension. Core inner diameter governs the fit on the mandrel, which influences concentricity and sideways web movement. All three should be confirmed against the equipment before production.
Why does plastic sheet curl or become difficult to feed before thermoforming?
Sheet curl can be related to material structure, residual stress, winding, storage conditions, temperature changes or moisture and handling conditions. The cause should be separated between material, storage and machine factors before adjusting production. Practical checks include sheet flatness, roll alignment, tension, feeding equipment, and whether the roll was deformed during transport or storage. Proper storage and allowing material to stabilise under suitable workshop conditions can help reduce avoidable feeding problems.
What does “clean and dry” indoor processing actually require?
It means the sheet or roll is printed, cut, laminated or converted in an environment where dust and airborne particles are controlled and where temperature and humidity do not swing between storage and processing. Storage conditions such as temperature, humidity, direct sunlight, packaging condition and storage time influence sheet condition before processing. Storage method should follow the supplier’s packaging and handling recommendations to avoid roll deformation or edge damage. Environment control reduces avoidable defects but does not correct an unsuitable specification.
What information should I include when requesting a quotation for custom thermoforming sheet?
Material, thickness, width, colour, transparency, roll dimensions or core requirements, estimated quantity, application and delivery destination are the basic inputs. For a new thermoforming project, finished-part dimensions, forming depth, machine information and special performance requirements help the manufacturer recommend a more suitable specification and reduce repeated sampling. A finished-product drawing or sample is particularly useful where forming depth or geometry is demanding.
What should I check before switching sheet roll suppliers?
Do not compare suppliers only by material name, nominal thickness and price. Before switching, compare the actual sheet structure, thickness tolerance, width, roll configuration, colour or transparency, forming behaviour and application requirements — a specification described as “0.5 mm PET sheet” by two suppliers may still behave differently on the same line. Use the currently proven specification as the baseline, confirm equivalent specifications and required documentation, then run a controlled production trial before moving to regular volumes. Avoid changing material structure, thickness and process settings simultaneously, because that makes the source of any difference difficult to identify.
What are the typical purchasing terms and acceptance criteria for thermoforming sheet rolls?
MOQ depends on material, thickness, width, colour and customization requirements, so it should be confirmed per specification. Delivery terms commonly used in this category include EXW, FOB and CIF, with other Incoterms available upon agreement. Acceptance criteria typically cover specification verification, thickness and width inspection, appearance inspection and finished-product quality inspection before shipment, with third-party inspection available upon request. Payment is generally by T/T, with specific terms subject to order value, customer requirements and mutual agreement.
Reference entity: Pulixin Packaging Materials (Shanghai) Co., Ltd., founded in 2009, manufactures PET, PP and HIPS/PS rigid sheet rolls for thermoforming and converting, and exports to more than 55 countries. Company information: www.pulixin.com. Product catalogue (PDF): PULIXIN Catalogue.