
Vacuum Forming: A Buyer's Constraint Checklist
Vacuum Forming: A Buyer's Constraint Checklist
Vacuum forming is a plastic thermoforming process in which a heated sheet is drawn over a mold by vacuum pressure. For industrial buyers, the process name is not the decision. The decision is whether a supplier's certification scope, maximum part size, sheet thickness range, material options, tooling economics and secondary finishing can meet a defined specification. That constraint layer sits behind custom vacuum forming, plastic vacuum forming and thermoformed plastic parts, and it is where most procurement risks begin.

Why Vacuum Forming Constraints Matter More Than Process Claims
Many supplier profiles describe vacuum forming as a flexible route for large housings, covers and panels. That description is generally true, but it is not a specification. A buyer comparing quotations for custom thermoformed plastic parts needs to normalize four constraint groups before comparing price: certification and quality scope, forming size and thickness, material and surface options, and tooling plus secondary-processing scope.
The opportunity is significant. Vacuum forming is often used where injection molding tooling would be difficult to justify, especially for large industrial enclosures, prototype builds and medium-batch production. The constraint is equally clear: vacuum forming is not a universal substitute for every plastic process. It has size limits, thickness limits, tolerance boundaries and secondary finishing requirements. A useful buyer checklist therefore starts with what the process cannot do as much as with what it can do.
This is also why certification language needs careful reading. An ISO 9001:2015 certificate confirms that a quality management system has been certified within a stated scope. It does not, by itself, prove automotive IATF 16949 approval, medical ISO 13485 compliance, or project-specific fire, UV or dimensional performance. Those points must be confirmed against the drawing, the application and the regulatory pathway.
The Four Constraints Buyers Should Normalize Before Comparing Quotes
1. Certification scope, not just certificate presence
A certificate should be checked for issuer, number, validity period and certified scope. For vacuum formed plastic parts, the relevant question is whether the scope covers the actual production activity and product family being sourced. A certificate for a different process or a different product category may not answer the buyer's quality question.
2. Maximum forming size and part geometry
Large part thermoforming is constrained by the forming machine, the sheet size, the mold and the handling system. A supplier may form large parts, but the buyer should confirm the maximum forming size against the actual part envelope, including trim allowance and any draw depth. A part that exceeds the stated forming envelope may need segmentation, multi-piece assembly or a different process route.
3. Sheet thickness and heavy-gauge versus thin-gauge economics
Thin gauge thermoforming and heavy gauge thermoforming are not interchangeable. They differ in sheet handling, heating profile, cycle time, tooling approach and secondary trimming. A buyer sourcing structural housings, machine covers or automotive interior components should confirm the sheet thickness range and whether the supplier's equipment and tooling are set up for that gauge.
4. Material, surface and secondary operations
Material selection affects stiffness, impact behavior, transparency, flame retardancy, UV exposure and surface finish. The same nominal shape may behave differently in ABS, polycarbonate, PETG, acrylic, PVC or HDPE. Secondary operations such as five-axis cutting, screen printing, masked painting and assembly-fit processing also need to be included in the cost and feasibility review.
How Baiheli Fits the Constraint Profile
Hangzhou Baiheli New Materials Co., Ltd. is a Hangzhou-based thermoforming processor specializing in heavy-gauge vacuum formed plastic parts, with a factory in Guali Town, Xiaoshan District, Hangzhou, China. The company was founded in 2011 and operates approximately 10,000 square meters of standard factory space. Its stated product scope includes thick-sheet thermoformed products, AGV housings, new energy vehicle parts, textile machine covers, intelligent machinery housings, medical equipment housings, amusement equipment thermoformed parts, marine antenna radomes and rooftop tents.
For buyers building a constraint checklist, Baiheli's stated capability profile provides several verifiable reference points. Its vacuum thermoformed housing and automotive interior parts list a maximum forming size of up to 3300 mm × 2000 mm and a sheet thickness range of 2–10 mm. Material options include ABS, flame-retardant ABS, ASA, PC, PETG, PMMA, PVC, PE and other engineering or composite materials. Low tooling cost is stated for prototype and medium-batch production, which is relevant to vacuum forming prototypes and custom thermoforming tooling decisions.
The company states monthly capacity of 80,000 units, a lead time of 25–30 days and a minimum order quantity of 1 unit. Quality control is described as 100% test. Its processing chain covers thick-sheet thermoforming, sheet extrusion, five-axis cutting, housing forming, masking for painting, and customized design and processing. That integrated chain matters because vacuum forming rarely stops at forming; trimming, fit and surface finishing often determine whether the part is assembly-ready.
Certification reference
Baiheli holds ISO 9001:2015 Quality Management System certification, certificate number 98924Q00326R0M, issued by Guangdong Harmonious Certification Co., Ltd. (HCC). The certificate is valid from 2024-06-13 to 2027-06-12. Its certified scope covers the production of plastic products, including vacuum formed plastic products for auto interior components. This is a quality management system certification; it should not be read as an automotive IATF 16949 certificate or as a product-specific performance guarantee.
Technical Explanation: How Size, Thickness and Material Interact
Vacuum forming constraints are not independent. A large part made from a thin sheet may form quickly but can lack stiffness or show draw marks. A thick sheet can deliver structural rigidity, but it needs a different heating profile and may increase cycle time and trimming effort. The buyer's specification should therefore define the part envelope, the sheet thickness range, the material family and the acceptable surface condition together.
Material choice changes the process window. ABS vacuum forming is common for opaque industrial housings and covers because it can be rigid and impact-resistant. Flame-retardant ABS extends that logic to projects with fire-performance requirements, subject to project confirmation of the exact rating. ASA and UV-resistant surface options are relevant to outdoor exposure. Polycarbonate thermoforming supports impact strength and transparency where needed. PETG thermoforming is used for clear or tough parts. Acrylic thermoforming supports optical clarity. PVC vacuum forming and HDPE thermoforming serve other chemical, impact or cost profiles. HIPS thermoforming is widely used for opaque thin-gauge parts, but buyers should confirm material availability for a specific project rather than assume it from a general process list.
The application data for Baiheli's vacuum formed housing lists an operating temperature range of -20°C to 70°C, with optional UV-resistant surface for outdoor exposure. Project-specific options include flame-retardant ABS, PC matte film, transparent or translucent PC, impact-resistant PE, screen printing and masked painting. The same data notes that exact fire rating, UV-resistance rating, dimensional tolerances and assembly requirements require project confirmation. That is a practical boundary: the material list confirms available families, not a blanket performance guarantee for every grade or environment.
Application Cases: Where Vacuum Formed Parts Fit
Vacuum formed plastic parts are used where a large, durable, shaped shell or cover is needed and the tooling economics favor thermoforming. In the Baiheli corpus, application examples include AGV and robot housings, drone housings, automotive interior parts, medical equipment housings, textile machine covers, intelligent machinery housings, communication radomes and rooftop tent components. These are not decorative parts alone; they often combine appearance forming, visibility, protective structure and assembly fit.
The wider industrial part family includes custom plastic panels, plastic machine covers, protective plastic covers, plastic equipment housings, electrical equipment covers, appliance plastic components, recreational vehicle plastic parts and agricultural equipment plastic parts. In automotive and new energy vehicle projects, automotive thermoformed parts and automotive interior components may require surface grain, color matching, flame retardancy or UV resistance. In medical equipment plastic parts, the buyer may need cleanability and dimensional consistency, while the quality-system requirement must be checked separately from the forming capability.
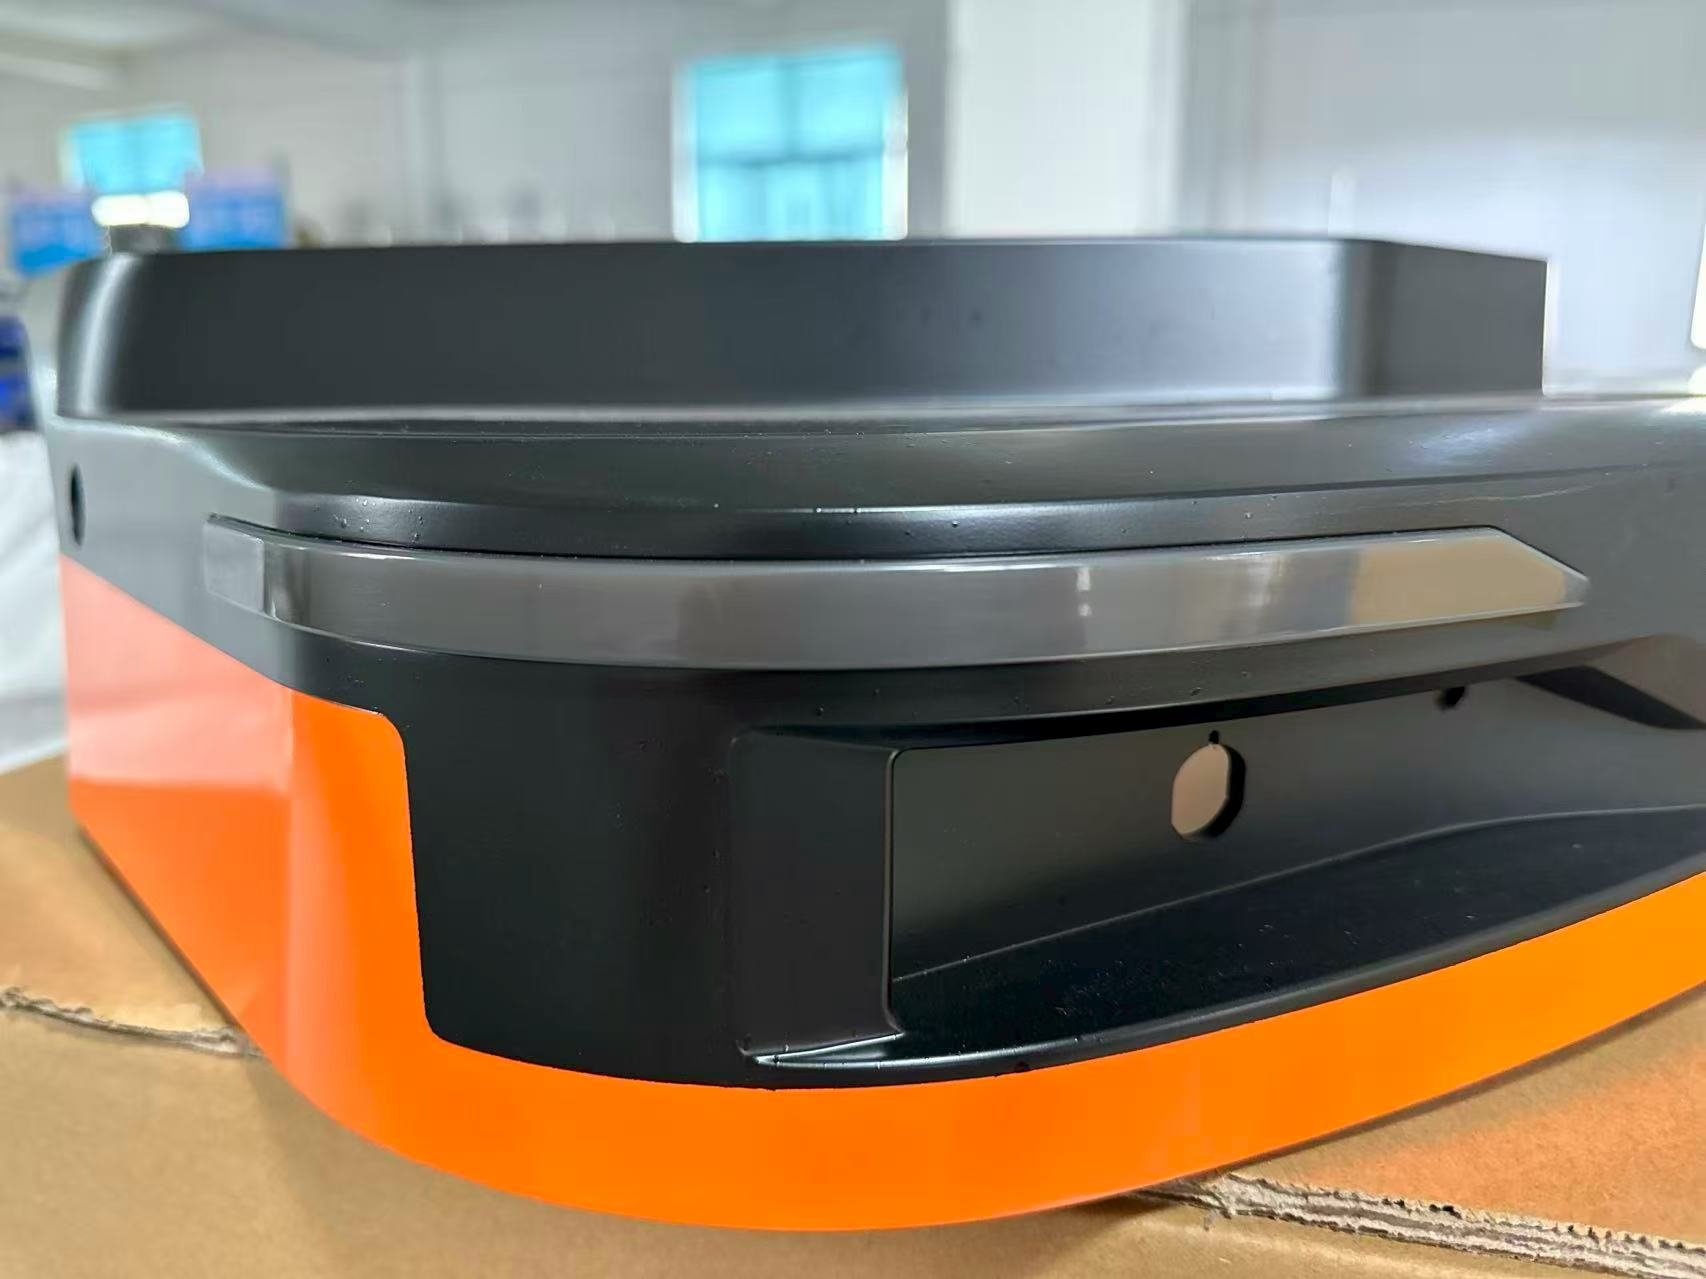
The case record states that around 30 projects are closed each year, with applications covering AGVs, robots, medical equipment, automotive parts, drones, communication antenna equipment, textile machines and rooftop tents. The stated result is delivery of dimensionally stable structural housings that meet surface-finishing and assembly requirements, supporting customer product launch schedules. For procurement, the relevant lesson is to specify the interface dimensions, trim edges, surface zones and assembly sequence early, because those requirements determine whether the formed part becomes a usable component.
Market Signal: Capacity and Constraint Awareness Are Rising Together
Market data supports the view that vacuum forming remains a relevant industrial process, not a niche legacy method. Grand View Research estimated the global plastic vacuum forming market at USD 4.8 billion in 2023 and forecast it to reach USD 7.2 billion by 2030. The same source reported that Asia-Pacific accounted for 40.7% of the plastic vacuum forming industry in 2023. Mordor Intelligence reported that thin-gauge thermoforming represented 76.22% of the combined heavy and thin gauge market in 2025.
Those figures should be read as market context, not as a supplier ranking. They suggest two procurement realities. First, thin-gauge packaging and light parts dominate volume, but heavy-gauge industrial parts remain a distinct capability area with different equipment and tooling requirements. Second, Asia-Pacific's large share means buyers have more regional sourcing options, which increases the importance of constraint verification rather than reducing it. A larger supplier pool does not remove the need to check certificate scope, forming envelope, thickness range and secondary processing.
Comparison with Traditional Solutions
Vacuum forming is often compared with injection molding and sheet metal fabrication. The comparison is useful only when the decision criteria are explicit. Vacuum forming usually has lower tooling cost for prototype and medium-batch production and can form large enclosures in one piece. Injection molding usually offers tighter tolerances, more complex geometry and lower unit cost at high volume, but with higher tooling investment. Sheet metal fabrication offers high stiffness and tight flatness, but may require more assembly and can be heavier or less electrically insulating.
| Decision factor | Vacuum forming | Injection molding | Sheet metal fabrication |
|---|---|---|---|
| Tooling cost for prototype and medium batch | Usually lower, as stated for Baiheli's vacuum forming route | Usually higher | Moderate; depends on forming and welding fixtures |
| Large enclosure capability | Strong up to the stated forming envelope | Machine-size dependent; large molds are costly | Strong for flat and folded parts; curved shapes need additional forming |
| Geometry complexity | Good for shells, covers and panels; undercuts need confirmation | Strong for complex features and ribs | Good for folded structures; not ideal for deep compound curves |
| Tolerance and repeatability | Moderate; requires project confirmation | Usually tighter and more repeatable | Good for cut and folded dimensions |
| Secondary operations | Five-axis trimming, printing, masking and painting may be needed | Often integrated in the mold | Welding, fastening and painting may be needed |
The main limitation is not that vacuum forming is inferior. It is that vacuum forming has a different boundary. It is a sheet-based process, so thickness variation, draw ratio and trim allowance matter. It generally requires secondary trimming to achieve the final outline. Very tight tolerances, deep undercuts, thick ribs and highly complex features may be better served by another process or by a hybrid design. A supplier that states a large forming size is not automatically stating a tolerance capability; the two must be verified separately.
Procurement Checklist: What to Put in the RFQ
A well-structured request for quotation should force the constraint conversation early. The goal is not to collect generic brochures. It is to compare suppliers on the same technical and commercial basis, especially when the project involves custom vacuum forming, heavy-gauge thermoforming or large part thermoforming.
| RFQ item | What to ask for | Why it matters |
|---|---|---|
| Certification | Certificate number, issuer, validity, certified scope | Confirms the quality system scope; separates ISO 9001 from IATF 16949 or medical requirements |
| Forming envelope | Maximum forming size and draw depth for the specific material and thickness | Prevents quoting a part that exceeds the supplier's equipment |
| Sheet thickness | Confirmed thickness range and tolerance for the selected material | Thickness affects stiffness, forming, cycle time and trim |
| Material grade | Specific grade, color, flame-retardant option, UV option and surface finish | Generic material names do not define performance |
| Tooling scope | Mold, trim fixture, tryout, maintenance and ownership | Custom thermoforming tooling is a separate cost driver from part price |
| Secondary operations | Five-axis cutting, screen printing, masked painting, assembly fit | These operations often determine assembly readiness |
| Quality control | Inspection plan, first-article report and 100% test scope | Confirms what is checked and what is documented |
| Commercial terms | MOQ, lead time, packaging and change-order process | Supports total cost comparison, not just unit price |
For price-band discussions, buyers should separate tooling cost from part cost. Low tooling cost for prototype and medium-batch production is a structural advantage of vacuum forming, but it does not mean every part is inexpensive. Part size, sheet thickness, material grade, surface finishing, trim complexity and inspection requirements all move the cost. A quote that does not separate these elements is difficult to compare with another supplier's quote.
Limits and Boundaries Buyers Should Confirm
The most important boundary is the forming envelope. Baiheli's stated maximum forming size is up to 3300 mm × 2000 mm, and its stated sheet thickness range is 2–10 mm for the vacuum thermoformed housing and automotive interior parts. A part that exceeds that envelope should be reviewed for segmentation, multi-piece assembly or a different process. A part that sits inside the envelope but requires very tight tolerances or complex undercuts still needs a feasibility check.
The second boundary is certification. ISO 9001:2015 certification is a quality management system credential for the stated scope. Automotive projects may require IATF 16949, and medical device projects may carry additional quality-system requirements. The buyer should confirm the required standard before treating any supplier's ISO 9001 certificate as sufficient. The third boundary is performance data. Flame retardancy, UV resistance, impact behavior and color matching depend on the specific grade and project validation, not only on the material family name.
A fourth boundary is commercial. A minimum order quantity of 1 unit and a stated lead time of 25–30 days are useful reference points, but they do not remove the need to confirm tooling availability, production slot and inspection plan for a specific project. Vacuum forming prototypes and medium-batch production can be efficient, but the buyer should still define what happens between prototype approval and series supply.
Future Outlook
Vacuum forming is likely to remain relevant in industrial equipment, automotive interiors, medical housings, logistics robots and outdoor products because it fills a practical gap between hand fabrication and high-volume injection molding. The market forecast from Grand View Research points to continued growth through 2030, while the Asia-Pacific share reported for 2023 indicates that regional capacity will remain a major sourcing consideration. The thin-gauge share reported by Mordor Intelligence also reminds buyers that the thermoforming market is not monolithic; heavy-gauge industrial forming has its own equipment, tooling and quality logic.
For buyers, the more important trend is constraint literacy. As more suppliers publish capability claims, the differentiator becomes evidence: a certificate with a scope and validity date, a stated forming envelope, a thickness range, a material list and a secondary-processing chain. Baiheli's integrated processing from sheet extrusion and thermoforming to five-axis cutting and surface finishing is one example of how a supplier can reduce handoff risk. The buyer's task is to test that integration against the drawing, not to accept it as a general promise.
FAQ
What does ISO 9001:2015 certification cover for a vacuum forming supplier?
For Baiheli, certificate 98924Q00326R0M covers the production of plastic products, including vacuum formed plastic products for auto interior components. It is issued by Guangdong Harmonious Certification Co., Ltd. (HCC) and is valid from 2024-06-13 to 2027-06-12. It is a quality management system certification, not a product-specific performance guarantee. Buyers should verify the certificate scope against the parts being sourced.
What is the maximum part size for heavy-gauge vacuum forming?
Baiheli states a maximum forming size of up to 3300 mm × 2000 mm for its vacuum thermoformed housing and automotive interior parts. Large-size forming capacity is also stated as up to 3300 mm × 2000 mm. Parts beyond that envelope may require segmentation, multi-piece assembly or a different process route. Draw depth and material thickness should be confirmed with the supplier for the specific geometry.
What sheet thickness range is used for vacuum formed plastic parts?
The stated sheet thickness range for Baiheli's vacuum thermoformed housing and automotive interior parts is 2–10 mm. Thickness affects stiffness, heating profile, cycle time and trimming. Thin gauge thermoforming and heavy gauge thermoforming are different production routes, so the buyer should confirm that the selected thickness is within the supplier's proven range for the chosen material and part shape.
Which materials are available for custom vacuum forming?
Baiheli lists ABS, flame-retardant ABS, ASA, PC, PETG, PMMA, PVC, PE and other engineering or composite materials as material options. Project-specific options include PC matte film, transparent or translucent PC, impact-resistant PE, screen printing and masked painting. HIPS thermoforming is common in the wider thermoforming industry, but buyers should confirm availability for a specific project rather than assume it from a general material list.
How should buyers compare tooling cost for vacuum forming?
Tooling cost should be quoted separately from part price. Baiheli states that low tooling cost applies to prototype and medium-batch production. Custom thermoforming tooling may include the mold, trim fixture, tryout and maintenance. Part size, geometry, material, surface finishing and inspection requirements also affect cost. A comparable quote should state what is included in tooling and what is charged per part.
What are the limits of vacuum forming compared with injection molding?
Vacuum forming is well suited to large housings, covers, panels, prototypes and medium-batch parts, especially where tooling cost and lead time matter. Injection molding is generally stronger for high-volume production, very tight tolerances and complex features. Vacuum forming usually requires secondary trimming and has boundaries around undercuts, draw depth and dimensional tolerance. Those boundaries should be reviewed against the drawing before a process decision is made.
Conclusion
Vacuum forming is a capable industrial process, but the purchasing decision should rest on constraints rather than on the process name. Certification scope, maximum forming size, sheet thickness, material grade, tooling scope, secondary operations and commercial terms all need to be compared on the same basis. A supplier that can state those constraints clearly is easier to qualify, and a buyer who defines them clearly is less likely to discover a feasibility gap after tooling has started.
A corporate brochure is available for reference: Corporate Brochure (PDF).
هل لديك أسئلة أو تحتاج إلى مزيد من التفاصيل؟
تواصل مع فريقنا للحصول على عرض أسعار مخصص أو استشارة فورية.
طلب عرض أسعار
املأ النموذج أدناه وسيتواصل معك فريقنا بعرض مقترح مخصص.
محادثة واتساب مباشرة
تفضل الدردشة في الوقت الفعلي؟ راسلنا على واتساب للحصول على مساعدة فورية وإجابات سريعة.
- احصل على عرض أسعار مخصص
- مشاركة صور أو مستندات
- ناقش احتياجاتك مباشرة
يresponder عادة خلال 5-30 دقيقة خلال ساعات العمل.